
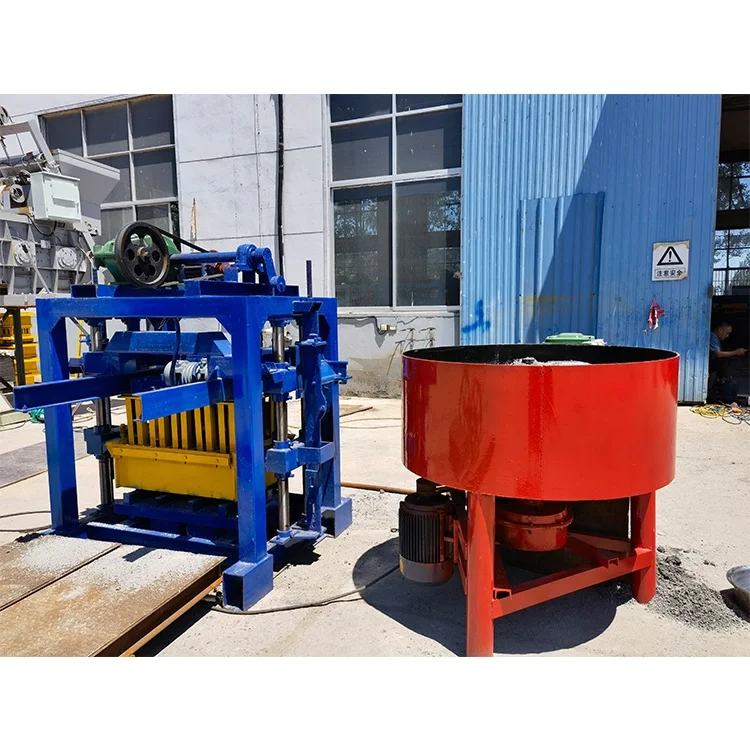
Line-Matched Flow — the QTJ4-40 press is specified together with its mixer, pallet supply and curing handling so that the 40-second moulding cycle is never left waiting for upstream or downstream stations.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QTJ4-40 |
| Product Type | Semi-Automatic Concrete Block Making Machine |
| Rated Power | 10.4 kW |
| Voltage & Frequency | According to buyer’s local standard (basis not stated in source — confirm voltage, frequency and phase) |
| Control System | Semi-automatic operation with top die push/pull and automatic scraper |
| Overall Dimensions (L×W×H) | 1350 × 1460 × 1800 mm |
| Net Weight | 1 T (source value — verify against manufacturer catalog) |
| Molding Cycle | 40 s |
| Theoretical Productivity (Hollow Block) | 360 pcs/h based on 400×200×200 mm, 4 pcs/mould |
| Theoretical Productivity (Solid Brick) | 800 pcs/h based on 225×112.5×60 mm, 9 pcs/mould |
| Pallet Size | 850 × 450 mm |
| Vibration System | Bed mould vertical vibration + upper mould compression vibration |
| Raw Materials | Concrete, sand, cement, fly ash, lime, gypsum |
| Automation Level | Semi-automatic (manual pallet handling assumed) |
Application Suitability
| Application | Material or Output |
|---|---|
| Small to medium concrete block plants | Hollow and solid blocks from crushed stone, sand and cement |
| On-site production for construction contractors | Interlocking bricks and wall blocks using locally available aggregates |
| First block production workshop for entrepreneurs | Paving blocks and kerbstones with fly ash or lime blends |
| Second press addition for existing producers | Formats matching current pallet and curing infrastructure |
Why "Cycles per Hour" Tells Only Half the Story
The true throughput of a Semi-Automatic Block Machine production line depends on every station keeping pace with the press, not just the press cycle itself.
A buyer receives a quotation stating so many cycles per hour and assumes the daily output is settled. On site, the mixer takes longer than expected to deliver a consistent batch, pallets are fed by hand one at a time, and finished blocks are stacked manually because no automatic stacker was included in the scope. The press sits idle between cycles, and real daily tonnage falls well short of the number on paper [NEED_CITE: common causes of block line throughput shortfall]. I saw this in Kenya with a small block machine that ran flawlessly but produced only a fraction of its nameplate capacity because the downstream handling was never part of the conversation.
Matching Each Station to the 40-Second Cycle
The QTJ4-40 completes one moulding cycle in 40 seconds, which sets the rhythm for the entire Semi-Automatic Block Machine production line. Upstream, the mixer must deliver a fresh batch within that same window or the press waits. Downstream, the operator must remove the loaded pallet and place an empty one before the next cycle begins. If any station is slower, the press becomes the most expensive idle asset on the floor. Line layout drawings should state the cycle time at each point, calculated for the specific block format the buyer intends to produce.
Pallet Size as the Dimension That Governs the Curing Yard
The 850 × 450 mm pallet is not an arbitrary number; it dictates curing rack spacing, forklift tine width and the layout of the entire curing yard. A buyer whose existing forklift is built for a different pallet dimension will face daily friction moving stacks from the press to the curing area. Confirming pallet size and material against the buyer’s current handling equipment before production avoids a mismatch that no amount of on-site adjustment can fix [NEED_CITE: pallet and forklift compatibility in block plants]. This is why pallet specification belongs in the initial line proposal, not as an afterthought.
Reading the Specs That Matter Beyond the Press
Dual vibration — bed mould vertical vibration combined with upper mould compression vibration — works together to compact the mix from both directions, which directly influences block density and compressive strength. The vibration force must be matched to the buyer’s mix design and local aggregate; a setting calibrated for fine sand may produce weak blocks with coarse crushed stone. The 10.4 kW rated power covers both the vibration motor and the hydraulic top die system, so the electrical supply must account for starting current peaks. Voltage and frequency confirmation in writing before production prevents the kind of three-week idle site I witnessed when a machine arrived with the wrong motor winding.
The Hidden Cost of Leaving Stations Off the Quotation
When pallet handling, stacking and curing are treated as optional extras, the buyer absorbs the cost in labour and lost output. Workers tire from manual pallet shuttling, breakage rises from inconsistent handling, and the curing yard becomes a bottleneck because loaded pallets pile up faster than they can be racked. These consequences do not appear on a machine spec sheet, yet they define whether the line runs at its intended pace or becomes a source of daily frustration [NEED_CITE: labour and breakage costs in semi-automatic block lines].
Why Source the Complete Line Here
Block machinery is the single focus, so the press, mould, pallet and handling equipment are specified as one matched system rather than assembled from separate suppliers. Configuration is set against the buyer’s actual mix design and target block format, not a catalogue default. Mould design covers the formats the buyer’s market sells, including custom drawings. Automation level is selectable, allowing a buyer to start with manual pallet handling and add an automatic stacker later. Installation and commissioning support includes operator training so the line runs correctly from the first shift.
Documentation & Verification
- Line layout drawing showing every station from mixer to curing rack with cycle time stated per block format
- Machine specification sheet confirming voltage, frequency and control language before production
- Pallet specification detailing size, material and thickness matched to the buyer’s curing yard
- Factory test record demonstrating actual cycle time and block density with the buyer’s target mix
- Mould drawing and format list for every block type included in the quotation
- Operation and maintenance manual with wear parts list and replacement intervals
Installation, Commissioning & Support
- Foundation plan sized to the 1350 × 1460 × 1800 mm footprint and 1 T operating weight of the QTJ4-40
- Dedicated electrical circuit rated for 10.4 kW with starting current allowance and confirmed voltage and phase
- Machine shipped as a single unit with vibration system pre-aligned; on-site assembly limited to pallet feeder and mixer connection
- First-run commissioning with the buyer’s local aggregate to verify 40-second cycle and block density
- Operator training covering mould change procedure, daily lubrication points and semi-automatic scraper adjustment
- Wear parts list for vibration springs, scraper blades and hydraulic seals with recommended stock quantities
What to Share Before Requesting a Quotation
To size the line correctly, provide the target block format and daily output, the local aggregate and cement type available, and the dimensions of the curing yard. Include the site voltage, frequency and phase, as well as the language required for the control panel. If existing pallets or forklifts are already on site, share their specifications so the new line integrates without modification.
Frequently Asked Questions
Q: How is daily capacity calculated across the whole line, not just the press cycle?
A: Daily capacity starts with the 40-second press cycle for a given block format, then factors in mixer batch time, pallet change time and any manual handling steps. The line layout drawing states the cycle at each station so the buyer can see where the bottleneck actually sits and whether additional automation is needed to reach the target output.
Q: Which supporting stations are included and which are optional?
A: The base quotation covers the QTJ4-40 press, mould and basic pallets. Mixing, pallet feeding, automatic stacking and curing rack handling are configured separately based on the buyer’s automation level and site layout. Each station is added to the line proposal with its own cycle time so the complete flow is visible before commitment.
Q: How must pallet size and material be matched to existing handling equipment?
A: The 850 × 450 mm pallet dimension must align with the buyer’s curing rack spacing and forklift tine width. Pallet material and thickness are selected based on the block weight and the vibration force applied during moulding. Confirming these details against the buyer’s current infrastructure avoids daily friction on site.
Q: What upstream and downstream cycle times keep the press from idling?
A: The mixer must deliver a batch within the 40-second window, and the operator or pallet feeder must swap pallets in the remaining seconds of each cycle. Downstream, loaded pallets must be moved to the curing rack before the next pallet exits the press. The line layout shows these intervals so every station is sized to the press rhythm.
Q: What line layout and utility plan is provided before shipment?
A: A scaled layout drawing shows the position of every station from raw material hopper to curing area, with electrical and water connection points marked. The document includes the confirmed voltage, frequency and control language, along with foundation load requirements based on the QTJ4-40 weight and operating vibration.



