
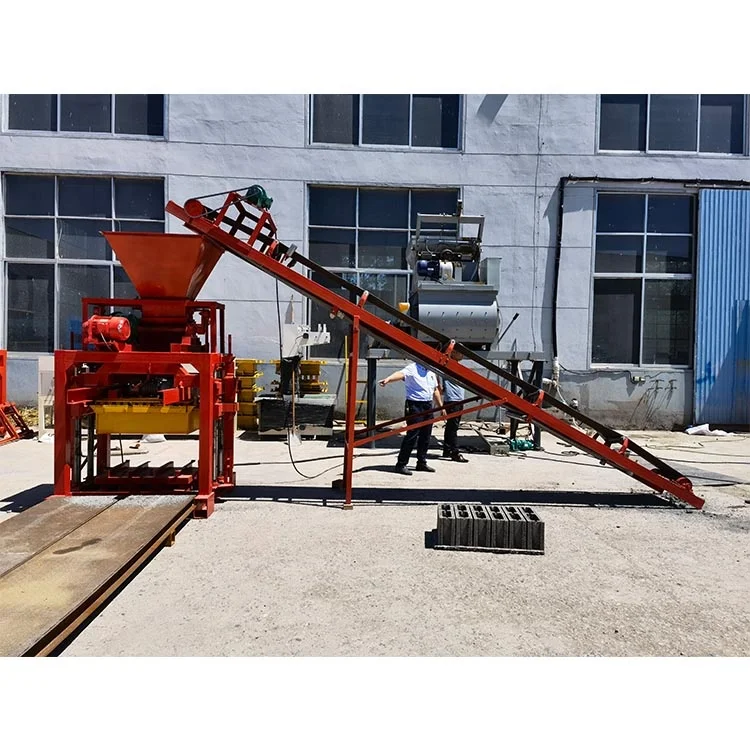
Matched System Sizing — every station from mixer to pallet trolley is calculated against the 35-second press cycle so material flow never stalls the host machine.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QTJ4-35 |
| Product Type | Semi-Automatic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 1350×1460×1800 mm |
| Molding Cycle | 35 s |
| Vibration Frequency | 2800 r/min |
| Exciting Force | 30 kN |
| Total Power | 11.15 kW |
| Mixer Model | JQ350 |
| Pallet Size | 850×450×20 mm |
| Net Weight | 1500 kg |
| Applied Products | Hollow block (8 inch, 6 inch), solid brick, paver, curbstone |
| Raw Materials | Crushed stones, sand, cement, fly ash, stone dust |
| Output Capacity (400×200×200 mm hollow block) | 4 pcs/mould, 408 pcs/hr, 3264 pcs/8hr |
| Output Capacity (400×150×200 mm hollow block) | 5 pcs/mould, 510 pcs/hr, 4080 pcs/8hr |
| Output Capacity (240×115×53 mm solid brick) | 18 pcs/mould, 2100 pcs/hr, 17000 pcs/8hr |
| Automation Level | Semi-automatic |
| Stacking Method | Manual trolley transport to curing area |
| Assembly State | Host machine + mixer + conveyor + pallets + trolley |
| Hydraulic Station | Equipped (pressure rating to be confirmed) |
| Control System | Configuration to be confirmed before production |
| Voltage & Frequency | To be confirmed against site supply |
Application Suitability
| Application | Material or Output |
|---|---|
| Small to medium block plant startup | Hollow blocks from crushed stone, sand, and cement |
| On-site construction block production | Solid bricks and hollow blocks using locally available aggregate |
| First-time block entrepreneur setup | Pavers and kerbstones by changing mould formats |
| Building material distributor format expansion | Multiple block types from one matched block production line equipment set |
Why the Line Layout Matters More Than the Press Alone
A host machine without matched supporting block machine equipment creates idle cycles that erase the capacity you paid for.
I have watched containers arrive at project sites where the block press sat silent because the mixer could not keep pace, or pallets ran out before the curing area could cycle them back. The QTJ4-35 completes its moulding stroke in 35 seconds, which means every upstream and downstream station must deliver within that same window. When quotations list only the press, buyers discover after arrival that material feeding, pallet handling, and curing transport were left as manual afterthoughts — and the real daily output falls well short of the headline number [NEED_CITE: common causes of block line throughput shortfall]. This supporting block machine equipment layout addresses that gap by specifying each station as part of one coordinated system.
How Station Pacing Keeps the Press Running
The JQ350 mixer and belt conveyor are selected so that fresh material reaches the hopper before the next 35-second cycle begins. If the mixer batch size or conveyor speed lags behind the press demand, the operator stands idle waiting for the next charge — a bottleneck that no amount of press speed can fix. This block production line equipment configuration sizes each station to the host cycle, verified during factory testing before dispatch.
Pallet Flow and Curing Area Compatibility
The 850×450×20 mm pallet dimension is matched to the mould formats this machine produces, but pallet quantity and material must also align with your curing area footprint and the forklift you already operate on site. A typical semi-automatic line requires a pallet pool of several hundred pieces so that pressed blocks can move to curing without waiting for empty pallets to return. Confirming these supporting block machine equipment details before production prevents the situation where blocks are stacked by hand because pallets are still occupied in the curing racks [NEED_CITE: pallet circulation requirements for semi-automatic block plants].
Reading the Numbers Behind Vibration and Pressure
The 2800 r/min vibration frequency and 30 kN exciting force work together with the hydraulic station to compact the mix into consistent block density. Higher vibration alone does not guarantee strength — the hydraulic pressure must match the specific aggregate gradation and cement ratio your local materials provide. The 11.15 kW total power covers the host press, mixer, and conveyor together, which matters when sizing your site electrical supply. Mould change between formats such as the 400×200×200 mm hollow block and the 240×115×53 mm solid brick requires manual bolting, so plan format changeovers at shift boundaries rather than mid-run to preserve daily output rhythm.
What Happens When Stations Are Specified Separately
When a buyer sources the press from one supplier and the mixer, conveyor, or pallets from another, nobody owns the responsibility for cycle-to-cycle pacing. The mixer may deliver too slowly, the conveyor belt may be too narrow for the aggregate size, or the pallets may not fit the curing racks already installed on site. These mismatches surface only after commissioning, when the line is expected to run at the block production line equipment capacity stated on paper [NEED_CITE: integration risks in multi-supplier block lines]. The cost of correcting them on site — rewiring, replacing pallets, repositioning conveyors — typically exceeds the savings of buying components separately.
Why Procurement Through a Single Line Supplier Changes the Outcome
Every station in this supporting block machine equipment package is specified against the same cycle-time calculation, so the mixer output rate, conveyor speed, and pallet circulation are all accountable to one layout document. The mould formats are selected based on what your market actually sells, not a catalogue default. Voltage, frequency, and control language are confirmed before production rather than discovered at the container door. Factory testing runs the full line — press, mixer, conveyor, and pallet feed — together, not each component in isolation. And the pallet specification is checked against your curing area dimensions and existing forklift capacity before the order enters production.
Documentation & Verification
- Line layout showing capacity per block format with cycle-time basis stated
- Machine specification sheet covering host press, mixer, and conveyor ratings
- Pallet dimension and material specification matched to mould format
- Hydraulic and electrical schematic for on-site connection planning
- Voltage, frequency, and control language confirmation record before production
- Factory test record demonstrating full-line run before packing
Installation, Commissioning & Support
- Foundation pad sized to the 1350×1460 mm host footprint with level tolerance specified
- Dedicated circuit for the 11.15 kW total load with voltage confirmed before wiring
- Host machine, mixer, and conveyor shipped dismantled for standard container loading
- First-run parameter setting with operator present for vibration and pressure adjustment
- Operator training on mould change procedure and daily lubrication points
- Wear parts list with reorder references for hydraulic seals and vibration components
What to Prepare Before Requesting a Quotation
Share the block formats your market demands and the daily volume you need for each, along with the raw materials available locally and their gradation. Provide your site voltage and frequency, the control panel language your operators read, and the dimensions of your curing area so that pallet quantity and supporting block machine equipment can be sized correctly from the start.
Frequently Asked Questions
Q: How is the line capacity calculated, and which block format does each output figure assume?
A: Each capacity figure is tied to a specific block dimension and mould cavity count. For example, 408 pieces per hour applies to the 400×200×200 mm hollow block at four cavities per mould, while 2100 pieces per hour applies to the 240×115×53 mm solid brick at eighteen cavities. A single headline number without format context does not reflect actual daily production.
Q: What happens if the mixer or conveyor cycle does not match the press timing?
A: The press waits idle for the next material charge, and the effective output drops below the rated cycle capacity. During factory testing, the full block production line equipment runs together to verify that mixer batch delivery and conveyor speed keep pace with the 35-second moulding cycle before the line is approved for dispatch.
Q: Are pallets, trolleys, and curing-area handling included in the quotation?
A: Pallets and manual trolleys are part of this supporting block machine equipment package. The recommended pallet pool size depends on your curing area dimensions and daily output target, so confirm these details during the configuration stage to avoid shortages during continuous production runs.
Q: Can the line start semi-automatic and later add automatic stacking?
A: The semi-automatic layout leaves space for future automation additions such as automatic pallet feeding or stacking stations. The electrical cabinet and hydraulic capacity are discussed during initial configuration so that upgrade paths remain open without replacing the host press or core supporting block machine equipment.
Q: What raw material conditions must be confirmed before the line is configured?
A: Your local aggregate type, maximum particle size, and available cement grade determine the mixer selection and vibration settings. A sample mix design helps verify that the exciting force and hydraulic pressure will produce the block strength your market requires, avoiding costly material substitutions after the line arrives.



