
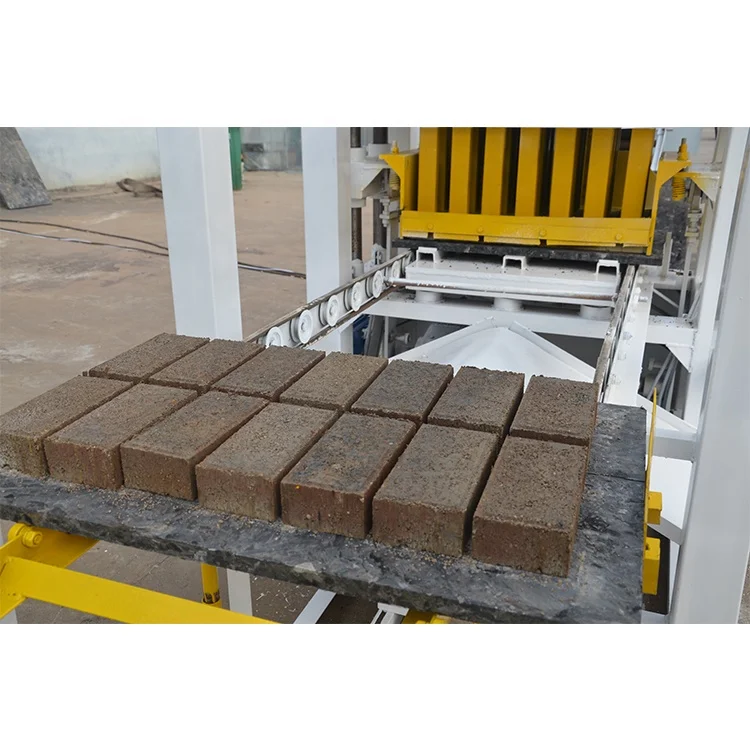
Line-Synchronized Station Design — Mixer discharge, conveyor speed and press cycle are matched so the QTJ4-24 is never left idle between molding strokes.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QTJ4-24 |
| Product Type | Semi-Automatic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 3600 × 1700 × 2560 mm |
| Total Mass | 3.5 T |
| Main Machine Power | 11.95 kW |
| Pallet Size | 900 × 450 mm |
| Molding Cycle | 24–26 s |
| Block Formats per Mould | 400×200×200 mm (4 pcs), 390×240×190 mm (3 pcs), 390×120×190 mm (6 pcs), 240×115×53 mm (21 pcs) |
| Feed Method | Manual feeding, two feed ways available |
| Vibration Type | Table vibration feeding, fluctuation vibration molding |
| Automation Level | Semi-automatic (mechanical + manual operations) |
| Control | Electrical control cabinet with mechanical interworking |
| Supporting Line Equipment | J350 Mixer, 6 m Belt Conveyor (composable) |
| Wiring Specification | Main machine 3×6 mm², Mixer 3×4 mm², Conveyor 3×2.5 mm² |
Application Suitability
| Application | Material or Output |
|---|---|
| Small-scale hollow block production | Crushed stone, sand, cement, water |
| Solid brick manufacturing | Fly ash, sand, cement blends |
| Standard brick runs for local masonry | Clay-free aggregate mixes with cement binder |
| On-site block production for contractors | Locally sourced gravel and sand with Portland cement |
| Entry-level plant setup for entrepreneurs | Low-capital raw material batches in limited footprint |
What the Cycle Time Figure Leaves Out When the Mixer Cannot Keep Up
A 24-second molding stroke only delivers rated output when material arrives at the hopper before the next cycle starts.
On paper, the QTJ4-24 presses a mould every 24 to 26 seconds. In practice, I have watched semi-automatic lines stall because the J350 mixer discharged its batch three or four seconds after the hopper ran empty. That gap adds up across an eight-hour shift and can shave a noticeable portion off expected daily volume. When the belt conveyor, mixer drum rotation, and press cycle are not synchronized from the layout stage, the Semi-Automatic Block Making Machine Production Line ends up running below its designed rhythm. [NEED_CITE: concrete batching cycle synchronization standards]
Station Sequencing from Raw Feed to Cured Block
The Semi-Automatic Block Making Machine Production Line begins with raw material proportioning at the mixer, where aggregate and cement are blended before discharge onto the belt conveyor. The conveyor delivers the mix into the QTJ4-24 hopper at a rate that must match or slightly exceed the press consumption per cycle. Pallets are fed manually into the molding station, and the finished blocks on pallets are pushed out to the curing area. Every station in this sequence is a potential bottleneck, so the line layout must be planned with the slowest station in mind rather than the press alone.
Vibration Sequence and Its Effect on Block Density
The QTJ4-24 uses table vibration feeding followed by fluctuation vibration molding. The first phase settles the mix into the mould cavity at lower amplitude, while the second phase applies higher-frequency vibration under mechanical pressure to compact the block. This two-stage sequence matters because a single vibration profile cannot handle both the initial fill and the final densification equally well. Consistent block strength depends on the vibration profile being matched to the specific aggregate grading and cement ratio the buyer is using. [NEED_CITE: vibration compaction effect on concrete block compressive strength]
Reading the Numbers That Actually Matter on Site
The 900 × 450 mm pallet size determines how many blocks cure per square meter in the yard, and whether the buyer’s existing forklift can handle loaded pallets without modification. The 11.95 kW main machine power dictates the dedicated circuit rating and cable cross-section — the specified 3×6 mm² main wiring leaves little margin if additional loads are tapped onto the same breaker. The four mould format options mean cycle output varies considerably: 21 standard bricks per stroke versus 4 large hollow blocks, so capacity planning must state which format the daily target assumes. Wiring specifications across the mixer (3×4 mm²) and conveyor (3×2.5 mm²) show that each station draws from its own circuit, reducing the risk of a single overload tripping the entire Semi-Automatic Block Making Machine Production Line.
The Hidden Cost of Quoting the Press Alone
When a quotation lists only the QTJ4-24 press without specifying the mixer model, conveyor length, and pallet handling method, the buyer often discovers that material delivery is too slow or pallets must be carried by hand. That missing line equipment turns a semi-automatic machine into a mostly manual operation. I have seen plants where the curing rack layout did not match the pallet dimensions, forcing a forklift change within the first month. These gaps are not visible in a single-machine spec sheet but surface quickly once production starts. [NEED_CITE: common causes of output shortfall in semi-automatic block plants]
Why Sourcing the Full Line from One Supplier Reduces Integration Risk
Block machinery is our single focus, so the QTJ4-24, its moulds, pallets, and supporting conveyors are specified as a matched system rather than assembled from separate vendors. Configuration is set against the buyer’s actual mix design and local aggregate, not a catalogue default. Mould design covers the formats the buyer’s market actually sells, including custom drawings when standard sizes do not match. The automation level is selectable, so a buyer starting with manual pallet handling can add automatic pallet feeding later without replacing the press. Installation support includes operator training on the specific line configuration delivered, and wear parts lists are provided so the first replacement order can be placed before stock runs out. [NEED_CITE: machinery supplier integration best practices]
Documentation & Verification
- Line layout drawing with station positions, conveyor routing, and curing area allocation for the QTJ4-24 footprint
- Capacity calculation sheet stating which block format the daily output figure assumes
- Mould drawing and format list covering all four cavity configurations
- Pallet specification including material, thickness, and compatibility with buyer’s forklift
- Voltage and control language confirmation recorded before dispatch
- Factory test record on the buyer’s specified block format before crating
Installation, Commissioning & Support
- Ground slab must support the 3.5 T machine mass plus dynamic vibration loads across the 3600 × 1700 mm footprint
- Dedicated 3×6 mm² circuit for the 11.95 kW main machine with separate breakers for mixer and conveyor
- Machine arrives partially dismantled for container loading; on-site reassembly covers frame, hopper, and vibration table
- First-run commissioning includes cycle timing verification against the 24–26 s target on the buyer’s chosen block format
- Operator training covers manual pallet feed rhythm, mould change procedure, and electrical cabinet interlocks
- Wear parts list identifies high-wear vibration components and hydraulic elements with recommended replacement intervals
Preparing Your Line Inquiry
To size the supporting equipment around the QTJ4-24, share the block formats your market demands and the daily volume you need per format. Provide your local aggregate type and cement source so the mixer and conveyor can be matched to your actual mix. Include your site voltage, frequency, and preferred control language, along with the curing yard dimensions and forklift specs you already have on site.
Frequently Asked Questions
Q: How is daily output calculated and which block format is it based on?
A: Daily output depends on the mould installed. The QTJ4-24 produces 4 hollow blocks per stroke with the 400×200×200 mm mould and 21 standard bricks with the 240×115×53 mm mould, each on a 24–26 second cycle. Any quoted daily figure must state the specific format, because switching moulds changes the count per stroke significantly.
Q: What supporting equipment is included versus quoted separately?
A: The standard line pairs the QTJ4-24 with a J350 mixer and a 6 m belt conveyor. Pallet stock, curing racks, and forklift are typically buyer-supplied unless explicitly added. Confirming the full station list before order avoids gaps that leave the press waiting for material or pallets.
Q: How do the mixer discharge, conveyor speed, and press cycle stay synchronized?
A: The J350 batch volume and drum rotation speed are selected so that one full mix charge arrives at the hopper before the QTJ4-24 completes its current molding stroke. The belt conveyor length and speed are set to bridge the gap without material pile-up or starvation between stations.
Q: What are the installation requirements for the full line?
A: The line needs a level concrete slab rated for 3.5 T static load plus vibration, separate electrical circuits per the wiring specification, and a curing yard sized for 900×450 mm pallets. Clearance around the 3600×1700 mm machine footprint must allow manual pallet feeding and block removal on both sides.



