
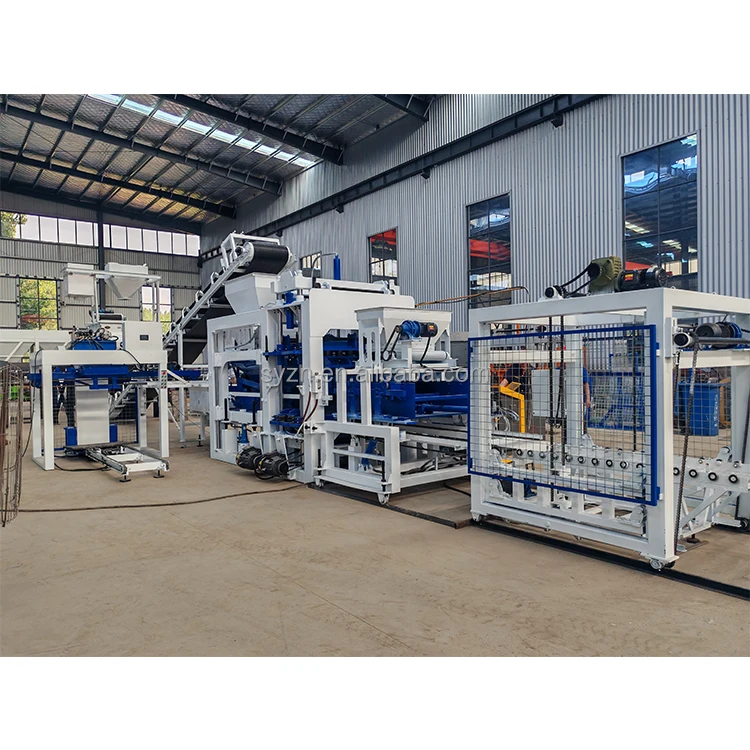
Line-Synced Engineering — Every upstream and downstream station is sized against the QT8-15’s actual cycle rhythm so the press never waits for a pallet or a batch.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT8-15 |
| Product Type | Hydraulic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 8300×1860×3000 mm |
| Rated Pressure | 21 MPa |
| Main Vibration Form | Platform Vibration |
| Vibration Frequency | 2800–4500 r/min |
| Vibration Force | 45 kN |
| Pallet Size | 950×900 mm |
| Molding Cycle | 15–20 s (basis not stated in source — confirm block format / material / thickness) |
| Overall Power | 55.5 kW |
| Total Mass | 8 T |
| Demolding Method | Hydraulic |
| Factory Area | 300 m² |
| Applied Products | Concrete hollow blocks, solid blocks, pavers, interlocking blocks, curbstone, colored pavers |
| Raw Materials | Crushed stone, sand, cement, dust, fly ash, gravel, slag |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for load-bearing walls | Crushed stone, sand, cement, fly ash |
| Solid block manufacturing for foundation courses | Gravel, sand, cement blends |
| Interlocking paver runs for driveways and walkways | Colored aggregates, fine sand, cement |
| Curbstone forming for road and landscaping projects | Coarse aggregate, slag, cement |
Why the Slowest Station Dictates Your Real Output
A 15-second press cycle means nothing if the pallet feeder takes 25 seconds to deliver the next board.
I once watched a block plant in Shandong sit idle for a full third of every shift because the batching mixer could not keep up with the host machine. The supplier had quoted output based on press cycles alone, ignoring that the local aggregate had a high clay content requiring longer mixing times. The whole concrete block making machine production line ran at the speed of its weakest link, and the buyer did not discover this until commissioning day. That mismatch is what line-level engineering is meant to prevent [NEED_CITE: line throughput bottleneck analysis in block plants].
Raw Material Feeding and Mixing Must Match the Press Rhythm
The QT8-15 cycles between 15 and 20 seconds, which means the mixer must deliver a fresh batch within that window every time. A pan mixer may suffice for clean, well-graded sand, but if your local aggregate carries silt or clay, a twin-shaft forced mixer becomes necessary to reach homogeneity within the available window. Undersizing the mixer is the most common cause of press idle time on a concrete block making machine production line, and it is the first station I verify when planning any layout.
Pallet Circulation Sets the Ceiling for Continuous Running
The 950×900 mm pallet size drives the entire return loop — from the feeder conveyor width to the curing rack slot spacing. If the buyer already operates a curing yard with racks built for a different pallet dimension, the return conveyor and rack adapters must be specified before the press ships. A mismatch here means pallets pile up at the press exit, forcing operators to clear them by hand and breaking the automatic cycle that the block pre*TE: pallet return conveyor design standards for block lines].
Reading the Specs That Matter Beyond the Press
Platform vibration at 2800–4500 r/min paired with 45 kN of force determines how densely the concrete is compacted inside the mould. Higher frequency with lower force suits thin pavers; lower frequency with higher force works for tall hollow blocks. The 21 MPa hydraulic demolding pressure must be balanced against mould wear — harder pressure strips blocks faster but accelerates wear on mould liners, which in turn dictates how often the changeover station sees use. At 55.5 kW overall power, the electrical supply must account for the mixer motor, conveyor drives, and stacking station simultaneously, not just the press alone.
When One Undersized Station Cascades Through the Entire Line
A batching hopper that is too small forces the loader operator to feed material more often, creating gaps in supply that starve the mixer. A mixer that cannot finish within the press cycle leaves the host machine vibrating an empty mould box. Downstream, if the stacker cannot lift and place a full rack layer before the next pallet exits, wet blocks queue on the conveyor and risk surface damage. Every one of these failures traces back to a station that was specified in isolation rather than as part of a synchronized concrete block making machine production line [NEED_CITE: consequences of unbalanced station capacity in block production].
Why Sourcing the Line Together Changes the Outcome
Block machinery as a single focus means the press, mould, pallet, and handling equipment are specified as one matched system, not assembled from separate suppliers who each optimize for their own unit. Configuration is set against the buyer’s actual mix design and local aggregate, not a catalogue default — so the mixer type and batching capacity reflect what your yard actually stocks. Mould design covers the formats your market sells, with custom drawings available when standard moulds do not fit. The automation level is selectable, so a buyer can start with semi-automatic pallet handling and add a stacker or cubing station later without replacing the press. Factory testing runs the entire line together before dispatch, catching timing mismatches while corrections are still cheap.
Documentation & Verification
- Line layout drawing with capacity calculation stating the block format assumed
- Pallet specification sheet matched to your existing curing rack dimensions
- Hydraulic and electrical schematics covering every station in the line
- Voltage, frequency, and PLC display language confirmation before production
- Factory test record running your target block format through the full cycle
Installation, Commissioning & Support
- Foundation plan sized to the QT8-15’s 8 T mass and 8300 mm length to prevent vibration transfer
- Dedicated electrical circuit rated for the 55.5 kW total draw including mixer and conveyors
- Machine arrives partially dismantled for container loading; reassembly sequence provided in manual
- On-site commissioning includes cycle timing verification across every station with your actual mix
- Operator training covers mould change procedure and platform vibration adjustment by block format
- Wear parts list with mould liner and hydraulic seal intervals based on your production volume
What We Need to Size Your Line Correctly
To build a concrete block making machine production line that actually runs at its rated rhythm, share your target block formats and daily output goal, the raw materials available in your area including aggregate grading and moisture content, and the dimensions of your existing curing yard and forklift capacity. If you already operate upstream or downstream equipment, provide those specs so we can confirm interface points before quoting.
Frequently Asked Questions
Q: How do I verify real daily output when the supplier quotes cycles per hour?
A: Ask which block format, wall thickness, and mix design the quoted cycle time assumes. A 15–20 second cycle on a thin paver does not apply to a 200 mm hollow block. Request a capacity table that lists output per format, and confirm that upstream stations — batching, mixing, pallet feeding — are timed to sustain that rate without gaps.
Q: Which upstream stations must match the QT8-15’s cycle time to prevent the press from idling?
A: The batching feeder, mixer, and pallet feeder all need to deliver within the press’s 15–20 second window. If any of these takes longer, the press sits empty. Verify each station’s throughput against your actual mix recipe and pallet return speed, not catalogue defaults.
Q: Is the pallet size fixed, or can the pallet feeding and curing rack system be configured to my existing equipment?
A: The QT8-15 uses 950×900 mm pallets. If your curing racks or forklift are built for a different size, the return conveyor and rack adapters can be configured around your existing setup. Confirm your current pallet dimensions and rack spacing early so the line layout accounts for them.
Q: What automation level is the QT8-15 designed for — and which stations can be added or upgraded later?
A: The press supports configurations from manual pallet handling through fully automatic stacking and cubing. Buyers often start semi-automatic to manage initial investment and add a stacker or curing rack handler as volume grows. The control system allows these stations to be integrated without replacing the host machine.
Q: What voltage, frequency, and control language need to be confirmed before the line ships?
A: These must be locked in before production starts. A mismatch in voltage or frequency delays commissioning, and an unfamiliar PLC display language slows operator training. Confirm your site supply specs and preferred language early so the electrical panels and control interface are built accordingly [NEED_CITE: electrical commissioning delays due to unconfirmed voltage and language settings].



