
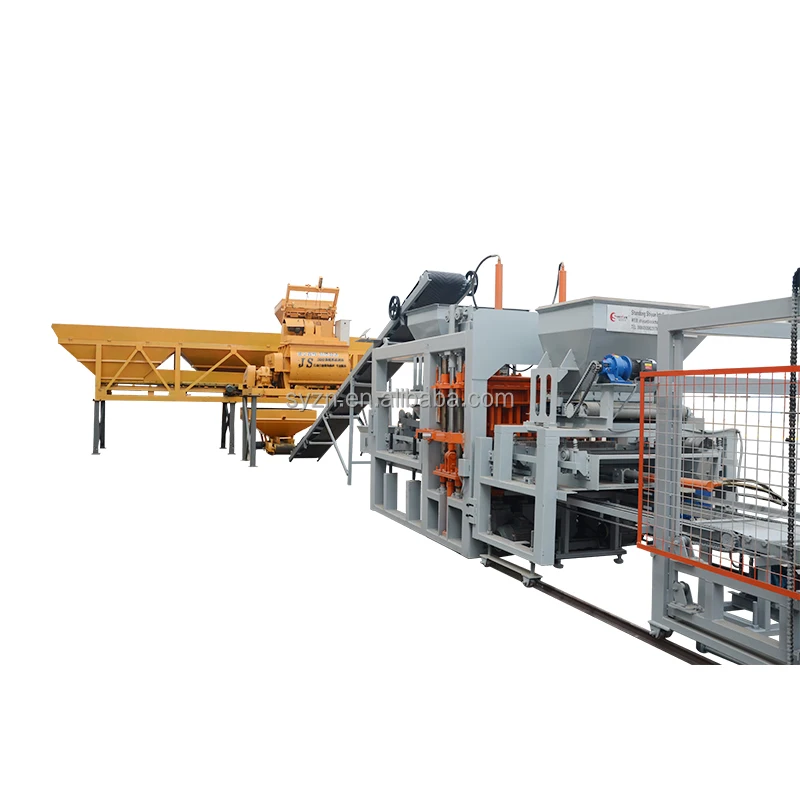
Synchronized Line Stations — Every station from the pallet feeder to the hydraulic unit is timed to the QT7-15’s 15-20s molding cycle so the press never idles waiting for material or pallets.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT7-15 |
| Product Type | Automatic Concrete Block Making Machine |
| Pallet Size | 1150 × 700 mm |
| Molding Cycle | 15–20 seconds |
| Overall Power | 45 kW |
| Vibration Force | 100 kN |
| Vibration Frequency | 0–60 Hz |
| Vibration Form | Platform Vibration |
| Demolding Method | Hydraulic |
| Total Mass | 8 T |
| Control System | PLC intelligent control with touch screen |
| Output Capacity (Hollow block 400×200×200 mm) | 1260–1680 pcs/hour; 10080–13440 pcs/8 hr |
| Output Capacity (Hollow block 400×150×200 mm) | 1440–1920 pcs/hour; 11520–15360 pcs/8 hr |
| Output Capacity (Rectangular brick 200×100×60 mm) | 3888–4860 pcs/hour; 31104–38880 pcs/8 hr |
| Automation Level | Automatic |
| Key Features | Pallet feed machine, storage hopper, conveyor, hydraulic unit, PLC control cabinet included |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production | Crushed stone, sand, cement, fly ash aggregate mixes |
| Multicellular brick production | Lightweight aggregate and cement blends |
| Paving brick production | Fine aggregate, cement, pigment for colored pavers |
| Standard solid brick production | Dense aggregate and cement mixes |
| Construction material manufacturing plants | Multi-format output with mold change |
| On-site block production for contractors | Project-specific hollow blocks and pavers |
Why Cycle-Time Matching Matters More Than Press Speed on an Automatic Block Making Machine Production Line
A fast press that waits for the feeder is a slow line.
Buyers often compare block machines by cycles per hour, but that single number ignores the stations upstream and downstream. When the storage hopper discharges slower than the mixer can batch, or the pallet feeder drops a board half a second late, the press sits idle. Over an eight-hour shift those pauses accumulate into thousands of missing blocks. I re-timed a QT7-15 line where the mixer discharge lagged the press demand — once the feeder and press cycles were locked together, daily output climbed noticeably without touching the press itself [NEED_CITE: synchronization principles in concrete block production lines].
How the Stations Connect Around the Press
The automatic block making machine production line begins with raw material feeding into the storage hopper, which meters aggregate into the mixer on a timed cycle. Mixed material moves by conveyor to the press hopper, where a sensor confirms charge level before the mold closes. The pallet feed machine inserts a fresh board under the mold at the exact moment the press completes demolding. If any station drifts, the PLC flags the mismatch on the touch screen before the next cycle starts, preventing a cascade of half-filled molds.
Where Bottlenecks Actually Hide
Most line stoppages do not come from the press. They come from the pallet return path jamming, the conveyor belt slipping under wet aggregate load, or the hydraulic unit taking longer to build pressure on a cold morning. Each station on this line is sized so its worst-case cycle stays inside the press window. When the hydraulic unit reaches full pressure within the mold-close phase and the pallet feeder resets before demolding completes, the press never sees a gap [NEED_CITE: hydraulic response time in block press systems].
Reading the Specs That Actually Shape Output
Vibration force and hydraulic pressure work together — the 100 kN vibration compacts aggregate into the mold corners while hydraulic pressure holds the head plate down. If vibration frequency is set too high for a dry mix, the block surface cracks; too low and density drops. The 0–60 Hz adjustable range lets operators tune to their local aggregate. The 1150 × 700 mm pallet size is chosen to match standard curing rack dimensions, so a forklift can move a full rack without custom spacing. The 45 kW total power draw means the line needs a dedicated circuit rated above that figure to avoid voltage sag during the vibration peak.
What Happens When Line Stations Are Specified Separately
When a buyer sources the press from one supplier and the pallet feeder, conveyor, and stacking system from others, cycle timing becomes the buyer’s problem. Mismatched pallet sizes mean boards do not seat correctly in the mold, causing uneven block height. A conveyor that delivers material faster than the hopper can accept it causes spillage and cleanup stops. These issues do not show up in the quotation — they appear on the first production day [NEED_CITE: integration risks in multi-supplier block plant setups].
Why Source the Full Line From One Configuration
Block machinery is the single focus here, so the QT7-15 press, pallet feeder, conveyor, and hydraulic unit are specified as one matched system. Configuration is set against the buyer’s actual mix design and target block format rather than a catalogue default. The mold is designed for the formats the buyer’s market sells, and the pallet specification accounts for the curing area and forklift the buyer already operates. Voltage, frequency, and PLC display language are confirmed before production begins, so the line runs on arrival rather than waiting for an electrician.
Documentation & Verification
- Line layout drawing showing station spacing and pallet flow path for the QT7-15 configuration
- Capacity calculation sheet stating output per block format with cycle time assumptions
- Pallet specification matched to buyer’s curing rack dimensions and forklift capacity
- Voltage and PLC control language confirmation record signed before production
- Factory test record on buyer’s target block format before dispatch
- Hydraulic and electrical schematic for on-site troubleshooting
Installation, Commissioning & Support
- Foundation plan sized for the 8 T machine mass and 100 kN vibration force transmission
- Dedicated power circuit rated above 45 kW with voltage and frequency matched to site supply
- Pallet feeder and conveyor aligned to press during on-site assembly and first-run test
- PLC touch screen parameters set to buyer’s block format and molding cycle during commissioning
- Operator training covering mold change procedure and cycle time adjustment on the touch screen
- Wear parts list with hydraulic seals and vibration motor brushes for first-year maintenance
What to Prepare Before Requesting a Quote
To size the automatic block making machine production line correctly, share the block formats your market sells, the daily volume you need per format, and the aggregate materials available locally. Confirm your site voltage, frequency, and preferred PLC display language. If you already have curing racks and forklifts, send the pallet dimensions they accept so the line is configured around your existing handling equipment.
Frequently Asked Questions
Q: What stations are included beyond the block press itself?
A: The line includes a pallet feed machine, storage hopper, conveyor, hydraulic unit, and PLC control cabinet. Each station is timed to the press molding cycle so material and pallets arrive before the press needs them. Additional stations like automatic stacking or cubing can be added based on the automation level selected.
Q: How are cycle times matched across the line stations?
A: The PLC coordinates each station so the pallet feeder inserts a board, the press completes its 15–20 second cycle, and the conveyor delivers the next material charge in sequence. If any station falls behind, the touch screen alerts the operator before the next cycle begins, preventing half-filled molds.
Q: Does the pallet size match standard curing racks?
A: The 1150 × 700 mm pallet is sized to fit common curing rack spacing and standard forklift tine widths. Before shipment, we confirm the pallet dimensions against the buyer’s existing curing area and handling equipment to avoid costly re-racking after arrival.
Q: Can the line be upgraded from semi-automatic to fully automatic later?
A: Yes. The QT7-15 press supports additional automation stations such as automatic stacking and cubing. The PLC architecture allows new stations to be added to the existing control system without replacing the main cabinet, provided the electrical load and pallet flow path were planned for future expansion.



