
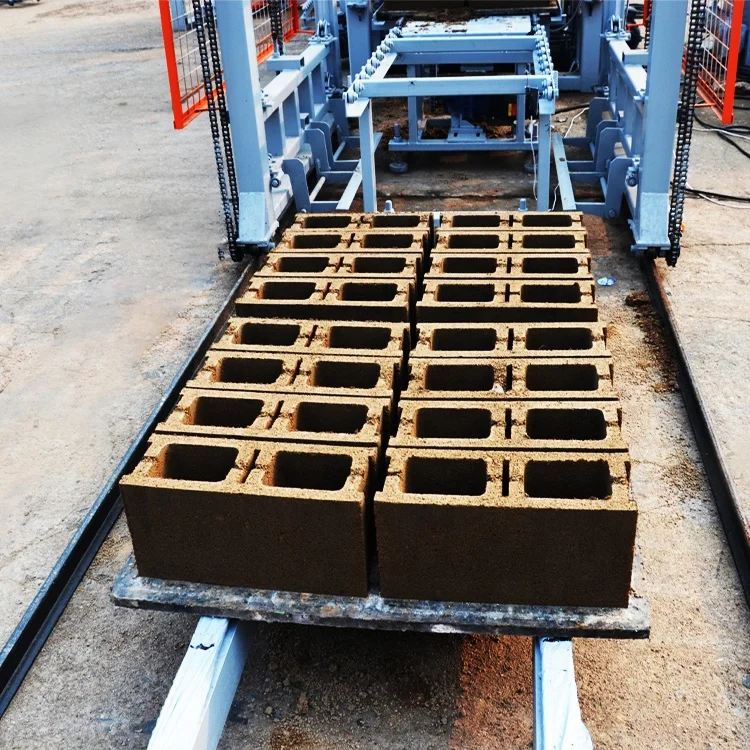
Integrated Line Layout — the QT6-15 block making machine is specified alongside raw material feeding, mixing, pallet circulation and stacking stations so the press is never left waiting for upstream or downstream equipment.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT6-15 |
| Product Type | Concrete Block Making Machine |
| Overall Dimensions | 8200×1700×2950 mm |
| Pallet Size | 880×850 mm |
| Vibration Force | 45 kN |
| Vibration Frequency | 0-60 Hz |
| Vibration Form | Platform Vibration |
| Moulding Mode | Automatic loading, vibration moulding |
| Molding Cycle | 15-20 s (basis not stated in source — confirm block format) |
| Overall Power | 37 kW |
| Total Mass | 7 T |
| Demolding Method | Hydraulic |
| Hydraulic System | Independent integrated hydraulic station |
| Control System | PLC controlled |
| Factory Area Required | 1200 m² |
| Compressive Strength of Blocks | >15 MPa |
| Output Capacity — Hollow Block 400×200×200 mm | 1080-1440 pcs/h (6 pcs/mould, 15-20s cycle) |
| Output Capacity — Hollow Block 400×150×200 mm | 1440-1920 pcs/h (8 pcs/mould, 15-20s cycle) |
| Output Capacity — Solid Brick 240×115×53 mm | 5760-7680 pcs/h (32 pcs/mould, 15-20s cycle) |
| Output Capacity — Rectangular Paver 200×100×60 mm | 2160-2880 pcs/h (21 pcs/mould, 20-25s cycle) |
| Output Capacity — Zigzag Paver 225×112.5×60 mm | 2160-2880 pcs/h (15 pcs/mould, 20-25s cycle) |
| Raw Material Adaptability | Waste ash, slag, cement, various aggregates |
| Warranty | 1 year (excluding spare parts) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production | Cement, crushed stone and waste ash blends for 400×200×200 mm and 400×150×200 mm formats |
| Solid brick production | Fine aggregate and cement mixes for 240×115×53 mm standard bricks |
| Paving brick production | High-density aggregate blends for 200×100×60 mm rectangular and 225×112.5×60 mm zigzag pavers |
| On-site contractor block making | Local slag and waste ash sourced near development and housing project sites |
What "15-20 Second Cycle Time" Leaves Out of the QT6-15 Concrete Block Making Machine Production Line
A cycle time only translates to daily output when every station around the press keeps pace.
I once watched a QT6-15 concrete block making machine production line sit idle for nearly a third of each shift because the mixer could not deliver batches fast enough. The press cycled perfectly, but the hopper above it ran dry every few minutes. The buyer had been quoted a moulding cycle of 15-20 seconds and multiplied it into an eight-hour day without anyone checking whether the raw material feeding, mixing capacity and pallet return loop could sustain that rhythm [NEED_CITE: typical block plant cycle time audit checklist]. When the line is planned station by station instead of as one system, the bottleneck simply moves rather than disappears.
How the Raw Material Feeding and Mixing Loop Must Sync with the Press
The QT6-15 concrete block making machine draws from an independent integrated hydraulic station that isolates hydraulic components from platform vibration and dust, but this protection only matters if material arrives at the hopper on schedule. The mixer batch size and discharge speed must be calculated against the moulding cycle so the press never waits. Belt conveyor width and speed, aggregate bin gate sizing and cement screw feeder throughput all feed into one timing equation. When any station runs slower than the press, the quoted 15-20 second cycle becomes irrelevant because the real cycle stretches to whatever the slowest link allows.
Pallet Circulation and Curing Rack Handling as Part of the Same Timing Chain
Once the press completes a cycle, the wet block on its 880×850 mm pallet must be carried away before the next pallet enters. The pallet return conveyor, the transfer car or finger car, and the curing rack elevator all operate within the same window. If the curing rack is full or the finger car is still returning from the yard, the press stalls. Planning the 1200 m² factory area means positioning raw material storage, press, curing racks and stacking stations so pallet travel distance does not create a hidden delay [NEED_CITE: block plant layout guidelines for pallet circulation]. The pallet size itself must also match the forklift tine spacing and the curing rack shelf width already in use or planned for the site.
Reading the Key Specifications Beyond the Brochure Numbers
The 45 kN vibration force delivered through platform vibration at 0-60 Hz determines how tightly aggregate particles pack inside the mould, but vibration alone does not guarantee block density. Hydraulic pressure during the compression stroke works together with vibration frequency to reach the stated compressive strength above 15 MPa. The 37 kW overall power rating covers the vibration motors, hydraulic pump and conveyor drives, so the electrical supply must provide a dedicated circuit with adequate capacity rather than sharing a feeder with other heavy loads. The PLC-controlled system coordinates automatic loading, vibration moulding and fault diagnosis, yet the display language and voltage frequency must be confirmed before the panel is wired at the factory, because re-flashing a PLC on site is far more disruptive than getting it right before shipment.
The Hidden Cost of Treating the Press as a Standalone Purchase
When a buyer orders only the press and sources the mixer, pallets and stacking equipment separately, cycle mismatches are almost guaranteed. A mixer that discharges too slowly starves the hopper, and a pallet stacker that cannot keep up blocks the press exit. The 880×850 mm pallet size may not fit the curing racks the buyer already owns, forcing an unplanned rack replacement. Electrical voltage confirmed too late means the motor winding or transformer must be swapped after arrival, adding days to commissioning [NEED_CITE: voltage and frequency standards by export market]. These costs never appear in the original quotation, yet they consume the budget the buyer thought was left over for raw materials.
Why a Line-Level Approach Changes the Outcome
Block machinery is our single focus, so the QT6-15 is never quoted without asking what mixer, pallets and handling equipment will sit beside it. Configuration starts from the buyer’s actual mix design and local aggregate, not a catalogue default, which means vibration force and hydraulic pressure are matched to the material that will actually enter the hopper. Mould design covers the block formats the buyer’s market sells, including custom drawings when standard sizes do not apply. The automation level is selectable, so a plant can begin with semi-automatic pallet handling and add automatic stacking later. Factory test records cover the full sequence from raw material feed through to block discharge, not just a dry press cycle.
Documentation & Verification
- Line layout and capacity calculation stating the block format assumed for each output figure
- Machine specification sheet with pallet size, vibration force and overall power confirmed
- Mould drawing and format list covering hollow, solid and paver options selected
- Pallet specification matched to curing rack dimensions and forklift capacity
- Hydraulic and electrical schematic for integration with existing plant infrastructure
- Voltage, frequency and PLC display language confirmation before shipment
Installation, Commissioning & Support
- 1200 m² factory area layout plan positioning press, mixer, curing racks and pallet return loop
- Dedicated 37 kW electrical circuit with voltage and frequency matching confirmed before wiring
- Independent hydraulic station placement away from vibration sources and dust ingress points
- PLC touch screen configured in the buyer’s preferred operating language before dispatch
- Mould change training covering hydraulic demolding and format-specific parameter settings
- Wear parts and mould list provided with first replacement schedule based on production hours
What to Prepare Before Requesting a Line Quotation
To size the QT6-15 concrete block making machine production line correctly, share the block format you sell most, your target daily output and the local aggregate or waste ash available near the site. Confirm the voltage, frequency and PLC display language required in your country, along with the forklift model and curing rack dimensions you plan to use. If you already have a mixer or batching plant, provide its batch size and discharge rate so the feeding loop can be matched from the start.
Frequently Asked Questions
Q: How do I verify that the quoted output capacity is based on my actual block format and not a catalogue default?
A: Ask the supplier to state the output figure alongside the specific block format, mould cavity count and cycle time assumed. The QT6-15 delivers different hourly rates for 400×200×200 mm hollow blocks versus 240×115×53 mm solid bricks, so a single blanket number without a format reference is unreliable for planning your daily production target.
Q: What supporting line stations are included and where can cycle time mismatches occur?
A: A complete line includes raw material feeding, mixing, pallet feeding, stacking and curing rack handling. Mismatches typically appear where the mixer discharge speed or pallet return conveyor cannot match the press cycle, causing the hopper to run dry or the press exit to block.
Q: How does the 880×850 mm pallet size affect my curing area layout and forklift selection?
A: The pallet dimensions determine the curing rack shelf width, the spacing between rack uprights and the forklift tine length required. Ordering pallets, racks and forklifts as one matched set avoids costly replacements after the line is already running.
Q: What voltage, frequency and PLC language options need to be confirmed before the line is shipped?
A: The PLC-controlled system, vibration motors and hydraulic pump all depend on correct voltage and frequency. Confirming these along with the preferred PLC display language before wiring ensures the line can be commissioned immediately on arrival without on-site reprogramming or transformer swaps.
Q: What is the full factory area requirement and how should stations be positioned within it?
A: The 1200 m² requirement covers the press, raw material yard, mixing station, curing racks and pallet return loop. Positioning each station to minimize pallet travel distance and keep the mixer discharge close to the press hopper reduces hidden cycle delays.



