
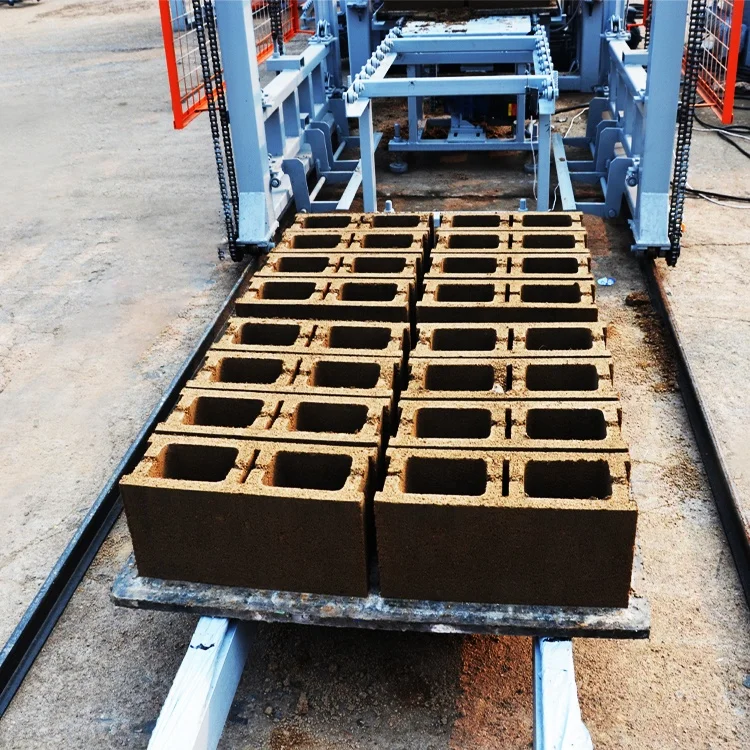
Synchronized Line Design — every station from the JQ350 mixer to the pallet feeder is timed against the QT6-15 press cycle, so the host machine never idles waiting for material or boards.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT6-15 |
| Product Type | Automatic Hydraulic Vibrating Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 7400×1900×2660 mm |
| Molding Cycle | 15–25 s |
| Vibration Frequency | 4600 r/min |
| Exciting Force | 40–50 kN |
| Total Power | 31.25 kW |
| Mixer Model | JQ350 |
| Pallet Size | 850×550×25 mm |
| Total Weight | 7 T |
| Control System | PLC control system |
| Hydraulic Station | High-pressure hydraulic system, included |
| Applied Products | Paver, solid block, hollow block, curbstone |
| Raw Materials | Crushed stone, sand, cement, dust, fly ash |
| Included Equipment | Block making machine, hydraulic station, PLC control system, pallet feeder, brick conveyor, block sweeper |
| Free Accessories | Manual hydraulic trolley, spare parts and tools |
| Output Capacity (Hollow block 400×200×200 mm) | 1200–1680 pcs/hr (basis: 15–20 s cycle, 6 pcs/mould) |
| Output Capacity (Hollow block 400×150×200 mm) | 1800–2400 pcs/hr (basis: 15–20 s cycle) |
| Output Capacity (Solid brick 240×115×53 mm) | 3240 pcs/hr (basis: 15–20 s cycle) |
| 8-Hour Output (Hollow block 400×200×200 mm) | 9600–13440 pcs/8 hr |
| 8-Hour Output (Hollow block 400×150×200 mm) | 14400–19200 pcs/8 hr |
| 8-Hour Output (Solid brick 240×115×53 mm) | 16200–19440 pcs/8 hr |
| Automation Level | Automatic with PLC and pallet feeder |
| Standards | CE |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for wall construction | Crushed stone, sand, cement, fly ash — 400×200×200 mm and 400×150×200 mm formats |
| Solid brick manufacturing for load-bearing structures | Sand, cement, stone dust — 240×115×53 mm format |
| Paver and curbstone production for infrastructure | Cement, crushed stone, sand — various mould-dependent formats |
| Mid-capacity block plant with pallet-based curing | Line output synchronized across mixer, press, feeder, and conveyor |
What "15–25 Seconds per Cycle" Actually Means for Your Daily Output
A cycle time is only real when every upstream and downstream station keeps pace with the press.
I once configured a QT6-15 block machine production line for a buyer in Colombia. The press itself ran fine at its rated cycle, but the JQ350 mixer discharged batches slower than the press consumed them. The host machine sat idle for roughly forty seconds every other cycle. Over an eight-hour shift, that added up to thousands of blocks lost — not because the press was slow, but because nobody checked the mixer discharge rate against the press appetite [NEED_CITE: line synchronization principles in block production]. When we rebuilt the timing chart and adjusted the mixer gate, the line finally matched its nameplate capacity. That experience shaped how I now approach every quotation: pull the full line timing sheet first, then discuss anything else.
Matching Mixer Discharge to Press Demand
The QT6-15 block machine production line pairs the press with a JQ350 mixer. The mixer must deliver a fresh batch to the hopper before the press completes its current mould cycle. If the mixer batch volume is too small or the discharge gate too slow, the press waits. Line capacity is therefore governed not by the fastest station but by the slowest node in the material flow path.
Pallet Feeder Speed and Return Loop
The pallet feeder must place a clean board under the mould within seconds of the previous block leaving the press. Downstream, the brick conveyor carries finished blocks away and the block sweeper clears debris before the pallet re-enters the loop. Any bottleneck in this return path forces the press to pause. The PLC control system coordinates these stations, but the mechanical timing — belt speed, sweeper stroke, feeder push distance — must be set during commissioning to match the actual mould cycle.
Output Verified by Block Format
Quoted capacity figures only hold when the specific block format and its corresponding cycle time are stated [NEED_CITE: block machine capacity calculation standards]. The QT6-15 produces hollow blocks at 400×200×200 mm at 1200–1680 pieces per hour based on a 15–20 second cycle with six pieces per mould. Switch to a 400×150×200 mm format and the hourly count changes because the mould cavity count and fill time differ. Solid bricks at 240×115×53 mm yield 3240 pieces per hour under the same cycle assumption. Every figure ties back to a named format, a known cavity count, and a measured cycle — not a single generic number.
Reading the Specs That Matter on Site
Vibration force of 40–50 kN at 4600 r/min works alongside the high-pressure hydraulic station to compact the mix into a dense block. Higher vibration frequency alone does not guarantee strength; the hydraulic pressure must be set to match the buyer’s aggregate grading and cement content. The 850×550×25 mm pallet size determines how many blocks sit on each board, which in turn dictates curing rack spacing and forklift capacity. Total power of 31.25 kW across the line — press, mixer, feeder, conveyor — must be checked against the site transformer rating before the container arrives [NEED_CITE: industrial voltage and frequency standards by region].
When the Line Is Not Synchronized
A press waiting for material burns electricity, wears hydraulic seals through repeated start-stop cycles, and pays operators who watch an idle machine. Over weeks, the cost shows up as higher energy bills, premature component replacement, and missed delivery commitments to the block buyer’s own customers [NEED_CITE: hidden costs of unsynchronized production lines]. The damage is not dramatic — no broken gearbox or burnt motor — just a steady erosion of margin that is hard to trace back to a timing mismatch.
Why Source This Line Here
Block machinery is our single focus, so the QT6-15 press, mould, pallet, and handling equipment are specified as one matched system rather than assembled from separate suppliers. Configuration starts from your actual mix design and local aggregate, not a catalogue default. Mould design covers the formats your market sells, with custom drawings available. Automation level is selectable — start with the included pallet feeder and add stacking later. Installation support includes operator training on the PLC interface and line timing adjustment.
Documentation & Verification
- Line layout drawing showing QT6-15 press, JQ350 mixer, pallet feeder, and conveyor positions with cycle time notes at each station
- Capacity calculation sheet listing output per block format with the cycle time and cavity count behind each figure
- Voltage, frequency, and PLC display language confirmation document signed before production begins
- Factory test record on the buyer’s specified block format before container loading
- Pallet specification sheet cross-referencing 850×550×25 mm boards with curing rack dimensions
Installation, Commissioning & Support
- Foundation plan sized to the 7400×1900 mm machine footprint and 7 T operating weight
- Dedicated power circuit rated for the 31.25 kW total line draw at confirmed voltage and frequency
- Machine dismantled for container shipment and reassembled on-site with alignment checks
- First-run commissioning covering PLC parameter tuning and mould cycle synchronization
- Operator training on format changeover, pallet feeder adjustment, and daily hydraulic checks
- Wear parts and mould inventory list provided at handover for first replacement planning
Before You Request a Quote
Tell us which block formats your market actually buys, the daily volume you need to hit, and the raw materials you can source locally — including aggregate grading and cement type. Share your site voltage, frequency, and preferred PLC display language so we can confirm electrical specs before production. If you already have curing racks, pallets, or forklifts on site, send their dimensions so the 850×550 mm pallet loop fits your existing layout.
Frequently Asked Questions
Q: How is the QT6-15 cycle time synchronized with the JQ350 mixer and pallet feeder?
A: We build a full line timing chart that maps mixer batch discharge, press mould cycle, pallet feed stroke, and conveyor speed. Each station’s mechanical parameters are adjusted during commissioning so the press never idles waiting for material or a clean board. The PLC coordinates the sequence, but the physical timing must be set on site.
Q: What equipment is included in the complete line, and what must the buyer provide locally?
A: The line ships with the QT6-15 press, hydraulic station, PLC control panel, pallet feeder, brick conveyor, and block sweeper. The buyer typically provides the curing area, raw material storage, water supply, and power connection. We supply a line layout drawing so local civil and electrical work can begin before the machine arrives.
Q: How is output capacity calculated for each block format?
A: Every capacity figure is tied to a specific block dimension, mould cavity count, and measured cycle time. For example, hollow blocks at 400×200×200 mm yield 1200–1680 pieces per hour based on a 15–20 second cycle with six cavities. If you install a different mould, the hourly output changes accordingly and we recalculate before confirming the order.
Q: What electrical details are confirmed before production starts?
A: We confirm site voltage, frequency, and PLC display language in writing before the machine enters production. This avoids commissioning delays caused by mismatched motor ratings or an interface the operator cannot read. The confirmation document is part of the standard order file.



