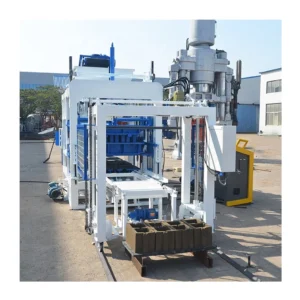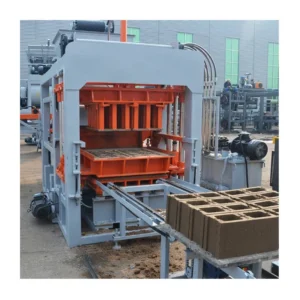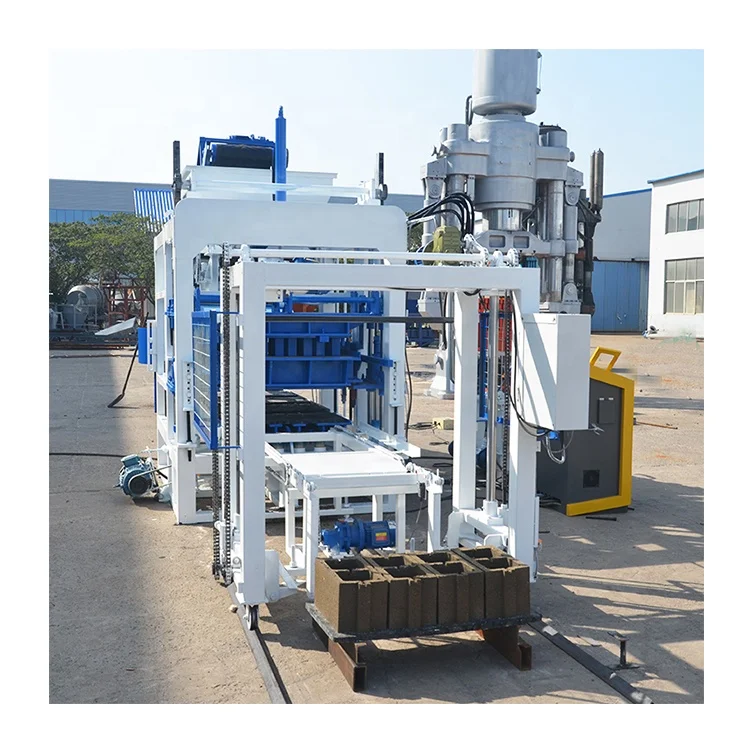
Matched System Integration — The QT4-16 block making machine is configured as the center of a complete line, where mixer batch time, pallet feed rate, and stacking cycle are synchronized to the press so no station becomes the bottleneck.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT4-16 |
| Product Type | Hydraulic Concrete Block Making Machine |
| Overall Dimensions | 7400 × 1950 × 2800 mm |
| Rated Pressure | 21 MPa |
| Main Vibration Form | Platform Vibration |
| Vibration Frequency | 2800–4500 r/min |
| Vibration Force | 40 kN |
| Molding Cycle | 15–20 s (basis not stated in source) |
| Pallet Size | 900 × 550 mm |
| Demolding Method | Hydraulic |
| Total Mass | 5 T |
| Applied Products | Concrete blocks, hollow/solid blocks, pavers, interlocking blocks, curbstone, colored pavers |
| Raw Material Compatibility | Crushed stone, sand, cement, dust, fly ash, gravel, slag |
| Control System | PLC intelligent control with man-machine interface, fault diagnosis, remote monitoring |
| Automation Level | Configurable from semi-automatic to full automatic |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for building walls | Crushed stone, sand, cement, fly ash blends |
| Solid block manufacturing for load-bearing structures | High-density aggregate and cement mixes |
| Paving block and colored paver runs | Fine sand, pigment, and cement combinations |
| Interlocking brick and curbstone forming | Coarse gravel, slag, and cement blends |
| On-site production for housing projects | Locally sourced aggregate with portable mixer setups |
Why the Press Cycle Is Only Half the Story
A press that finishes a cycle in 15–20 seconds is useless if the pallet feeder or stacker takes twice as long.
When buyers evaluate a QT4-16 block making machine production line, the first number they look at is the molding cycle. That figure means very little when the upstream mixer cannot deliver a fresh batch before the hopper runs dry, or when the downstream stacker falls two pallets behind. I have visited plants where the press sat idle for several seconds every cycle simply because the pallet return conveyor was undersized. The line was quoted as a high-capacity setup, but actual daily throughput reflected the weakest station, not the press. [NEED_CITE: bottleneck analysis in multi-station block production lines]
Upstream Feeding and Mixing Synchronization
The raw material feeding and mixing stations must deliver a consistent, homogenous batch to the QT4-16 hopper before each cycle begins. If the mixer batch time exceeds the press cycle, the hopper starves and the press waits. We size the mixer drum capacity and conveyor belt speed against the press consumption rate so the material flow never interrupts the vibration and hydraulic pressing sequence.
Downstream Pallet Handling and Curing Coordination
Once the QT4-16 completes demolding, the wet block on its 900 × 550 mm pallet moves to the stacking station. If the stacker cycle is slower than the press cycle, pallets queue up on the return conveyor, and eventually the press has nowhere to discharge. The curing rack spacing must match the pallet dimensions so that forklift operators can load and retrieve racks without manual repositioning. Every station in this QT4-16 block making machine production line is specified together, not sourced separately. [NEED_CITE: pallet handling integration standards for block plants]
Interpreting Pressure, Vibration, and Cycle Parameters
The rated pressure of 21 MPa and vibration force of 40 kN work together during each molding cycle. Hydraulic pressure compacts the mix from above while platform vibration at 2800–4500 r/min settles the aggregate from below. If the vibration frequency is set too high for a lightweight aggregate like pumice, the mix segregates and block strength drops. If pressure is insufficient for a dense gravel mix, the block crumbles during demolding. The PLC control system allows the operator to store different pressure and vibration profiles for each block format, so switching from hollow blocks to pavers does not require manual recalibration. The 5-tonne total mass of the machine provides the inertial stability needed to absorb vibration without transmitting it to the factory floor, which matters when the curing racks are positioned nearby.
The Cost of Ignoring Line-Wide Timing
When a buyer purchases the press alone and adds supporting equipment later, timing mismatches are almost guaranteed. A mixer that was adequate for a smaller press will choke the QT4-16. A stacker rated for lighter pallets will jam when loaded with dense curbstone blocks on hardwood pallets. These problems do not appear during the factory test because each machine runs in isolation. They surface on the first full production day, when the line must run continuously and every station depends on the next. [NEED_CITE: common causes of throughput shortfall in block production plants]
Why Source the Line from One Supplier
Block machinery is our single focus, so the QT4-16 press, its moulds, pallets, and handling equipment are specified as one matched system rather than assembled from separate vendors. We configure the line against your actual mix design and local aggregate, not a catalogue default. Pallet size and material are chosen with your existing curing area and forklift capacity in mind. Voltage, frequency, and PLC display language are confirmed before production begins. Mould design covers the formats your market actually sells, including custom drawings when standard formats do not apply. Every station in the QT4-16 block making machine production line is documented with its cycle time so you can verify there is no bottleneck before shipment.
Documentation & Verification
- Line layout and capacity calculation stating the block format assumed for each output figure
- Machine specification sheet with hydraulic and electrical schematics for the QT4-16
- Mould drawing and format list covering hollow, solid, paver, and curbstone options
- Pallet specification matched to your curing rack spacing and forklift capacity
- Voltage, frequency, and PLC display language confirmation sheet before production
- Factory test record on your target block format with cycle timing for each station
Installation, Commissioning & Support
- Foundation plan sized to the 7400 × 1950 mm footprint and 5-tonne operating mass of the QT4-16
- Power supply specification confirming voltage, frequency, and dedicated circuit for the rated load
- Dismantling and container loading plan with reassembly sequence for on-site commissioning
- First-run parameter setting covering hydraulic pressure, vibration frequency, and molding cycle per block format
- Operator training on the PLC interface including fault diagnosis and remote monitoring functions
- Wear parts and mould maintenance list with replacement intervals for hydraulic seals and vibration components
What We Need to Configure Your Line
To build an accurate line proposal, send us your target block format and daily output requirement along with a sample of your local aggregate. Include your workshop dimensions, existing curing area layout, and the forklift model you plan to use. Confirm your local voltage and frequency, and let us know whether you need the line in semi-automatic or full automatic configuration.
Frequently Asked Questions
Q: How is daily output calculated for the QT4-16 block making machine production line?
A: Daily output is calculated per block format, not as a single blanket figure. The molding cycle varies between hollow blocks, pavers, and curbstones because each format requires a different vibration duration and hydraulic pressure profile. Our capacity calculation states the exact block format, dimensions, and mix type assumed, so you can compare the quoted output against your actual production target.
Q: How does the 900 × 550 mm pallet size affect my curing area?
A: The pallet dimensions determine the spacing of every curing rack shelf and the fork pocket positions on the rack frame. If your existing racks were built for a different pallet size, new racks must be fabricated or the pallet size must be changed before the line is ordered. We confirm pallet specifications against your curing layout during the proposal stage.
Q: What upstream and downstream equipment must match the press cycle?
A: The mixer must deliver a full batch within the press cycle window, the pallet feeder must insert a fresh pallet before each molding stroke, and the stacker must remove and return the cured pallet before the next wet pallet arrives. Each station cycle time is documented in the line layout so no single point becomes the bottleneck.
Q: Is the quotation for the press only or the full line?
A: The quotation covers every station from raw material feeding through to cubing, including the mixer, conveyor, pallet feeder, press, stacker, and curing rack handling. If you already own supporting equipment, we can quote the QT4-16 press and moulds alone and provide the timing data your existing equipment must meet.