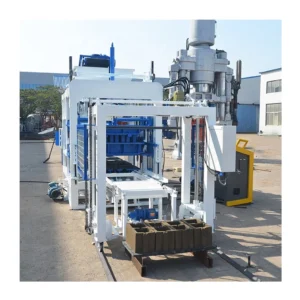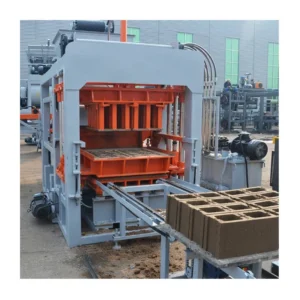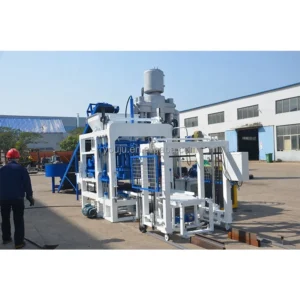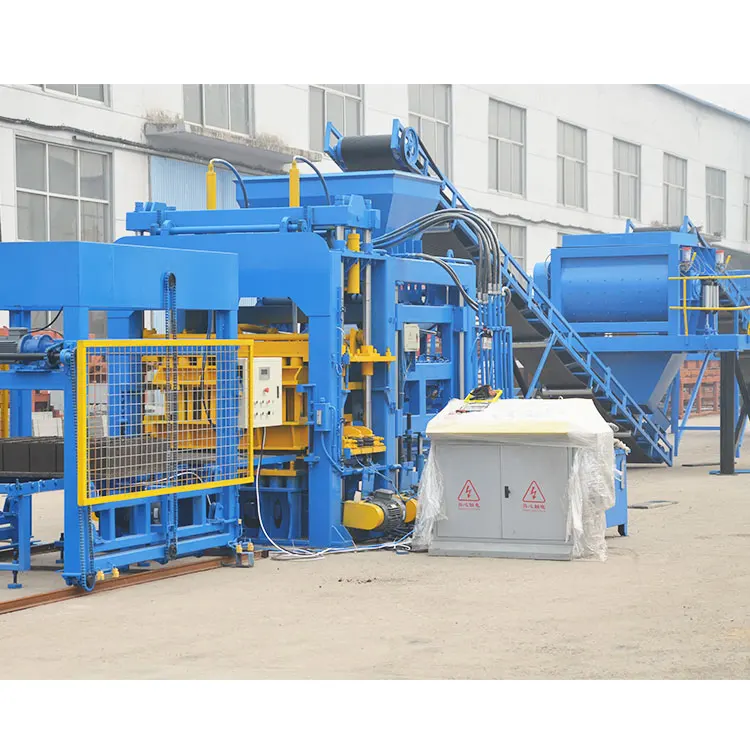
Matched System Integration — Every station around the QT12-15 press is sized to its cycle time so the line never starves the press or lets product pile up unhandled.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT12-15 |
| Product Type | Automatic Hydraulic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 9350 × 2520 × 2950 mm |
| Total Weight | 12000 kgs |
| Total Power | 50.7 kW |
| Rated Hydraulic Pressure | 21 MPa |
| Main Vibration Form | Platform Vibration |
| Vibration Frequency | 2800–4500 r/min |
| Vibration Acceleration | 15–20 g |
| Exciting Force | 120 kN |
| Fixed Brick Height Range | 50–200 mm |
| Pallet Size | 1350 × 850 mm |
| Molding Cycle | 15–25 s |
| Storage Hopper Volume | 0.4 m³ |
| Feeding Device Volume | 0.31 m³ |
| Control System | PLC controlled (mechanical-hydraulic synthesis) |
| Block Compressive Strength | >15 MPa |
| Output Capacity (Hollow block 390×190×190 mm) | 1720–2160 pcs/h, 13700–17200 pcs per 8h day (basis: 20–25 s cycle) |
| Output Capacity (Porous block 240×115×90 mm) | 5040–6300 pcs/h, 40300–50400 pcs per 8h day (basis: 20–25 s cycle) |
| Output Capacity (Standard block 240×115×53 mm) | 13100–14800 pcs/h, 105000–119000 pcs per 8h day (basis: 15–17 s cycle) |
| Suggested Line Configuration | PL1200 batching machine, JS500 or JS750 mixer, 8 m conveyor belt, stacker |
| Mould Type | Cartridge type welding mould, manganese steel, carburized and quenched |
| Voltage & Frequency | Configurable (confirm before shipment) |
| PLC Display Language | Configurable (confirm before commissioning) |
Application Suitability
| Application | Material or Output |
|---|---|
| High-capacity hollow block production | Concrete mixes using local aggregates for 390×190×190 mm structural blocks |
| Porous block manufacturing | Permeable concrete for 240×115×90 mm blocks used in load-bearing walls |
| Standard solid block production | High-density mixes for 240×115×53 mm bricks at shortened cycle times |
| Paving block and interlocking brick lines | Abrasion-resistant surface mixes for heavy-duty pedestrian and vehicular formats |
| Fly ash block production | Blended fly ash, cement, and aggregate mixes for lightweight masonry units |
What "Cycles per Hour" Leaves Out About Your Actual Daily Output
A press speed figure is meaningless unless it names the exact block format and cycle time it assumes.
Buyers regularly receive quotations listing a single impressive hourly number for the QT12-15 concrete block making machine production line, only to discover on site that the number assumed a small solid brick running at the fastest possible cycle. When the plant switches to the hollow block the local market actually buys, the cycle lengthens and daily output drops accordingly. This gap between quoted and real throughput is the single most common reason new block plants miss their revenue targets in the first six months [NEED_CITE: common causes of block plant output shortfall in first year of operation]. The figures in the table above state the format and cycle behind every capacity number so you can plan against the product you will actually sell.
Cycle-Matching Every Station Around the Press
The QT12-15 concrete block making machine production line is anchored by a press that completes a molding cycle in 15 to 25 seconds depending on the block format. For that rhythm to hold, every upstream and downstream station must deliver and remove material within the same window. The PL1200 batching machine and JS500 or JS750 mixer are specified to prepare and discharge a fresh batch before the storage hopper runs low, while the 8-meter conveyor bridges the gap without spillage or delay. If any one of these stations is undersized, the press sits idle between cycles and the quoted output becomes unreachable.
Pallet Flow and Stacking as Part of the Line, Not an Afterthought
Wet blocks leave the press on 1350 × 850 mm pallets that must travel through curing racks and return to the press in a continuous loop. The stacker at the end of the line is selected to handle the pallet weight and cycle speed of the QT12-15 so that finished product is never left sitting on the press table waiting for manual removal. When stacking and curing rack handling are treated as separate purchases rather than integrated stations, the result is a bottleneck that caps daily output well below what the press itself can produce [NEED_CITE: impact of pallet handling bottlenecks on block plant daily output]. Line layout must therefore account for pallet return speed and curing area capacity from the start.
Reading the Numbers Behind Vibration and Hydraulic Pressure
Block compressive strength above 15 MPa depends on how well the mix is compacted inside the mould, which is governed by two forces working together. The platform vibration at 2800–4500 r/min with 15–20 g acceleration shakes the mix into every corner of the mould cavity, while the 21 MPa hydraulic pressure clamps the mould halves and applies a 120 kN exciting force to densify the material. If vibration frequency is too low for a stiff, low-slump mix, voids remain in the block wall. If hydraulic pressure is set without regard to the vibration profile, the block surface may crack under over-pressurization. Both values must be tuned against the buyer’s specific aggregate gradation and cement content during commissioning.
The 0.4 m³ storage hopper and 0.31 m³ feeding device together ensure that each mould fill is metered precisely, reducing material waste and keeping block weight consistent across an eight-hour shift. The cartridge-type welding mould, machined from carburized and quenched manganese steel, holds dimensional tolerance across tens of thousands of cycles, which matters when the buyer is producing interlocking pavers that must fit together on site without cutting. Mould change time is a function of the cartridge design and the tools available on the shop floor, and this should be verified during the factory test before the line is shipped.
The Cost of Skipping the Pallet and Voltage Conversation
Choosing a pallet material and size without checking the curing racks and forklift already on site leads to pallets that do not fit existing racks or exceed the forklift’s safe load capacity. The buyer then faces an unplanned purchase of new racks or a larger forklift before the first block is cured. Equally, failing to confirm voltage, frequency, and PLC display language before the machine enters production results in a control cabinet that cannot be energized on arrival or an interface the operators cannot read. I have watched a line sit idle for weeks while a transformer was sourced locally and a new HMI program was written — all because the electrical specification was left as "standard" on the order form [NEED_CITE: commissioning delays caused by voltage and language mismatches in exported machinery].
Why Sourcing the Full Line from One Supplier Matters
Block machinery is the single focus here, which means the QT12-15 press, moulds, pallets, batching, mixing, and stacking are specified as one matched system rather than assembled from separate vendors who each optimize for their own equipment. Configuration is set against the buyer’s actual mix design, local aggregate, and target block format instead of a catalogue default that may not match regional materials. Mould design covers the formats the buyer’s market actually demands, with custom drawings available when standard moulds do not fit. Automation level is selectable, allowing a buyer to start with semi-automatic pallet handling and add full stacking later without replacing the press. Installation support includes operator training so the crew running the line on day one understands cycle timing, mould changes, and daily maintenance.
Documentation & Verification
- Line layout drawing with capacity calculation stating the block format assumed for each output figure
- Machine specification sheet confirming QT12-15 hydraulic pressure, vibration, and pallet dimensions
- Mould drawing and format list covering hollow, porous, standard, paving, and interlocking options
- Hydraulic and electrical schematic with confirmed voltage, frequency, and PLC language
- Factory test record showing cycle times and block strength results on the buyer’s mix design
- Operation and maintenance manual with wear parts list and mould replacement procedure
Installation, Commissioning & Support
- Foundation plan sized for 12000 kgs total weight and vibration isolation requirements
- Power supply confirmation for 50.7 kW total load at the buyer’s site voltage and frequency
- Machine dismantling for container loading and reassembly supervision on arrival
- PLC commissioning with confirmed display language and parameter tuning to local mix
- Operator training covering mould change, pallet feed, stacking, and daily maintenance routines
- Wear parts and mould supply plan with lead times for first replacement order
What We Need to Size Your Line Accurately
To prepare a layout and quotation that reflect real output rather than catalogue promises, share the block formats your market demands, the daily volume you need per format, and the raw materials available locally including aggregate type and gradation. Provide your site’s voltage, frequency, and preferred PLC display language along with the dimensions of your curing area and the forklift you will use for pallet handling. If you are integrating this line with existing batching or stacking equipment, send the specifications of that equipment so cycle matching can be verified before production begins.
Frequently Asked Questions
Q: How is daily output calculated per block format on the QT12-15 line, and what cycle time does each figure assume?
A: Each output figure is tied to a specific block format and its corresponding molding cycle. For 390×190×190 mm hollow blocks, the calculation assumes a 20–25 second cycle yielding 13700–17200 pieces per eight-hour day. For 240×115×53 mm standard blocks, a faster 15–17 second cycle is used. Every capacity number in the specification table states its format and cycle basis so you can plan against the product you will actually manufacture.
Q: How do I match the press cycle to the batching, mixing, pallet feeding, and stacking stations?
A: The press completes a cycle every 15 to 25 seconds, so the PL1200 batcher and JS500 or JS750 mixer must prepare and discharge a fresh batch within that window. The 8-meter conveyor and stacker are sized to move material and pallets at matching speed. The line layout documents cycle time at each station to confirm no point becomes a bottleneck.
Q: What pallet size does the QT12-15 use, and how should it align with my curing setup?
A: The standard pallet size is 1350 × 850 mm. Before the line is laid out, this must be checked against your existing curing rack dimensions and forklift capacity. If your racks or forklift were sized for a different pallet, the line layout adjusts to accommodate your equipment or new racks are included in the quotation.
Q: How is the line configured for my local aggregate and mix design?
A: Vibration frequency, hydraulic pressure, and mould fill settings are tuned against the buyer’s specific aggregate gradation and cement content during factory testing. The goal is consistent block compressive strength above 15 MPa using materials the buyer can actually source locally, rather than forcing a costly material change after installation.
Q: Which line stations are included in the quotation and which are separate?
A: The quotation specifies which stations — batching, mixing, conveyor, press, stacker, pallet return, and curing rack handling — are included and which are buyer-supplied. This is documented in the line layout so there is no ambiguity about scope before the order is confirmed.