
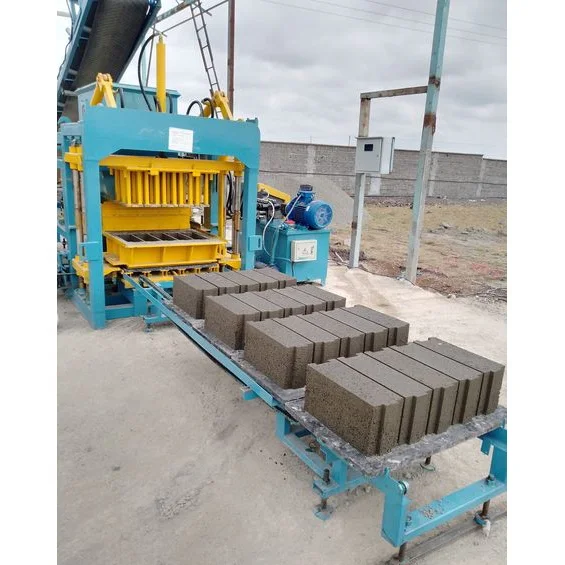
Integrated Line Matching — Every station around the QT4-15A press is timed and specified together so the block machine never waits on upstream feeding or downstream pallet handling.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT4-15A |
| Product Type | Hydraulic Block Making Machine |
| Overall Dimensions (L×W×H) | 7100×1600×2610 mm |
| Molding Cycle | 15-25 s |
| Vibration Frequency | 4600 r/min |
| Vibration Force | 40-50 kN |
| Total Power | 18.45 kW |
| Mixer Model | JQ350 |
| Pallet Size | 850×550×25 mm |
| Total Weight | 3 T |
| Control System | PLC control system |
| Hydraulic Station | High pressure, included |
| Included Equipment | Block making machine, hydraulic station, PLC control system, pallet feeder, brick conveyor, block sweeper |
| Applied Products | Paver, solid block, hollow block, curbstone |
| Raw Materials | Crushed stones, sand, cement, dust, fly ash |
| Output (Hollow 400×200×200 mm) | 408 pcs/hr, 3264 pcs/8hr (basis: stated format) |
| Output (Hollow 400×150×200 mm) | 510 pcs/hr, 4080 pcs/8hr (basis: stated format) |
| Output (Solid 240×115×53 mm) | 2100 pcs/hr, 17000 pcs/8hr (basis: stated format) |
| Voltage & Frequency | Configurable to target market (basis to be confirmed before production) |
| Automation Level | Semi-automatic with PLC control |
| Free Accessories | Manual hydraulic trolley, spare parts and tools |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for wall construction | Crushed stone, sand, cement, fly ash — 400×200×200 mm or 400×150×200 mm formats |
| Solid brick manufacturing | Cement and aggregate mix — 240×115×53 mm format |
| Paver production for pathways and yards | Dense aggregate blend with pigmented face mix |
| Curbstone forming for road edges | High-strength concrete mix with extended vibration |
| On-site block production for housing projects | Locally sourced sand, stone dust and cement |
What "3264 Blocks per Day" Actually Assumes
Quoted output only holds when the block format, mix design and line rhythm all align with the number on the spec sheet.
Many buyers discover after commissioning that the capacity figure they were sold assumed a hollow block format their market never orders. The daily count then drops sharply because the machine runs a different mould with a different cycle. A mismatched pallet size or a mixer that cannot feed fast enough further erodes throughput. [NEED_CITE: block plant output verification standards for concrete masonry] When a hydraulic block making machine production line is specified, every station must be checked against the format the buyer actually sells.
Line Rhythm: Where Stations Meet the Press
The QT4-15A hydraulic block making machine production line includes a JQ350 mixer, a pallet feeder, a brick conveyor and a block sweeper. These are not optional extras; they are timed to the press cycle. If the mixer discharges slower than the press consumes raw material, the press sits idle and cycle time lengthens. If the pallet feeder cannot deliver in time, the same idle gap appears. Each station must match the 15-25 s molding window.
Pallet Flow and Downstream Handling
After pressing, loaded pallets travel via the brick conveyor to the curing area. The pallet size of 850×550×25 mm dictates how many blocks ride on each board and how they stack in the curing yard. A mismatch between this pallet dimension and the buyer’s existing forklift or curing rack means manual re-handling, which negates the output the press itself delivers. [NEED_CITE: concrete block curing rack spacing and pallet dimension standards]
Reading the Specs That Shape Daily Output
Vibration force at 40-50 kN combined with hydraulic pressure determines block density and compressive strength. Higher vibration compacts the aggregate more thoroughly, but only when the mix moisture and aggregate grading suit the force applied. The 4600 r/min vibration frequency is chosen to work with crushed stone and sand blends typical in masonry production. Total power of 18.45 kW covers the press, hydraulic station and feeder motors, meaning the electrical supply must provide a dedicated circuit at the confirmed voltage and frequency. The PLC control system manages cycle timing, allowing semi-automatic operation where the operator triggers each press stroke while the system handles vibration duration and hydraulic sequence.
The Cost of Skipping Line-Level Specification
When a buyer evaluates the press alone without checking the mixer discharge rate or pallet feeder speed, the result is a bottleneck hidden in the middle of the line. Output drops, operators improvise with manual pallet handling, and the extra labour erodes the margin the machine was supposed to deliver. Voltage left unconfirmed until shipment arrival delays commissioning while a transformer or panel swap is arranged locally. [NEED_CITE: consequences of voltage mismatch on industrial PLC systems]
Why Sourcing the Line Together Matters
Block machinery as a single focus means the QT4-15A, its mould, pallets and handling equipment are specified as one matched system. The configuration is set against the buyer’s actual mix design and local aggregate, not a catalogue default. Mould design covers the formats the buyer’s market sells, including custom drawings when standard formats do not fit. Automation level is selectable, so a buyer can start with semi-automatic PLC control and plan an upgrade path. Installation support includes operator training so the crew understands cycle timing from day one.
Documentation & Verification
- Line layout and capacity calculation stating the block format assumed for each output figure
- Machine specification sheet with hydraulic and electrical schematic for the QT4-15A
- Mould drawing and format list confirming paver, hollow block, solid brick and curbstone options
- Pallet specification matching 850×550×25 mm to buyer’s curing area and forklift
- Voltage and PLC display language confirmation before production release
- Factory test record on buyer’s target block format before dispatch
Installation, Commissioning & Support
- Foundation plan sized to the 7100×1600 mm footprint with anchor bolt locations
- Dedicated power circuit confirmed for 18.45 kW total load at local voltage and frequency
- Machine shipped with hydraulic station and pallet feeder pre-assembled for faster site setup
- PLC control parameters loaded and cycle timing verified against the chosen block format on site
- Operator training covers mould change procedure and semi-automatic press stroke sequencing
- Wear parts list and spare tool kit included for early-stage maintenance planning
Preparing Your Line Inquiry
Before requesting a quotation, confirm the block formats your market requires and the daily output you need per format. Share your local raw material sources, typical aggregate grading and cement type so the mix can be matched to the vibration and pressure settings. Provide your site voltage, frequency and preferred PLC display language. Let us know the pallet size your curing area and forklift already use so the line is configured around existing infrastructure.
Frequently Asked Questions
Q: How is output capacity verified per block format and what does each figure assume?
A: Each capacity figure on the spec sheet is tied to a specific block dimension. The 408 pcs/hr rate applies to 400×200×200 mm hollow blocks, 510 pcs/hr to 400×150×200 mm hollow blocks, and 2100 pcs/hr to 240×115×53 mm solid bricks. These assume the mixer, pallet feeder and conveyor keep pace with the press cycle and that the mix design suits the vibration force applied.
Q: What line stations are included and where must cycle times match?
A: The line includes the JQ350 mixer, pallet feeder, brick conveyor and block sweeper alongside the press and hydraulic station. Each station’s cycle must fit within the 15-25 s molding window. If the mixer discharge or pallet delivery lags behind the press, the press idles and actual output drops below the rated figure.
Q: How are voltage, frequency and PLC language confirmed before shipment?
A: These are confirmed during the quotation stage before production begins. The buyer states the local supply voltage, frequency and preferred PLC display language. The control panel is then wired and programmed accordingly, avoiding on-site delays caused by electrical mismatch or an interface the operator cannot read.
Q: What pallet size is used and how does it relate to curing infrastructure?
A: The QT4-15A uses an 850×550×25 mm pallet. This dimension determines how pallets stack in curing racks and which forklift fork spacing works. Confirming pallet compatibility before ordering prevents a situation where loaded pallets cannot be moved to the curing yard with existing equipment.
Q: What is the mould change procedure on the QT4-15A?
A: Format switching requires removing the current mould and bolting in the replacement, then adjusting PLC parameters for the new cycle time and vibration duration. The semi-automatic control system stores settings per format once configured. Mould change time depends on crew familiarity and whether the correct tools from the included kit are on hand.



