
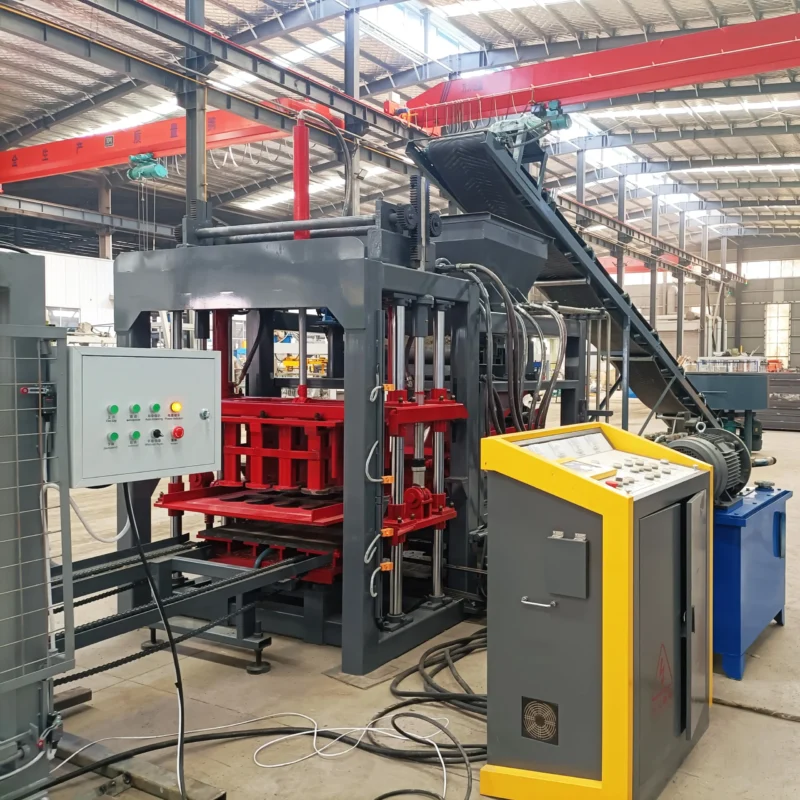
Matched System Integration — The QT4-15A block machine production line is specified as a complete system with synchronized pallet circulation, mixing, and stacking stations, ensuring the press never idles waiting for upstream or downstream equipment.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT4-15A |
| Product Type | Fully Automatic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 4100×1600×2600 mm |
| Rated Pressure | 16–21 MPa |
| Main Vibration Form | Platform Vibration |
| Vibration Frequency | 4200 r/min |
| Vibration Force | 55 kN |
| Pallet Size | 880×550 mm |
| Molding Cycle | 25–30 s (basis not stated in source — confirm block format / material / thickness) |
| Overall Power | 18.45 kW (source states "18.45W" — verify against manufacturer catalog) |
| Total Mass | 4 T |
| Demolding Method | Hydraulic |
| Factory Area Required | 300 m² |
| Automation Level | Fully automatic |
| Control System | PLC (inferred from fully automatic designation) |
| Warranty | 1 year |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow and solid block production | Crushed stone, sand, cement, fly ash |
| Paving and interlocking block manufacturing | Gravel, slag, dust, cement |
| Kerbstone and colored paver production | Aggregate blends with pigment additives |
| On-site contractor block production | Local sand and crushed stone mixes |
Why "25-30 Seconds" Means Nothing Without Line Synchronization
A molding cycle is only meaningful when every station upstream and downstream can sustain it without interruption.
I have stood in block plants where the press was capable of a 25-second cycle, but the pallet return conveyor took 40 seconds to complete its loop. The result was a press that spent half its shift idling. The QT4-15A fully automatic concrete block making machine turnkey solution addresses this by timing the raw material feeder, mixer discharge, pallet feeding mechanism, and stacking station to the same rhythm before the line ever ships. [NEED_CITE: production line cycle synchronization principles in concrete block manufacturing]
The Bottleneck That Hides in the Pallet Return Loop
When a buyer focuses only on press speed, the pallet return conveyor often receives minimal specification attention. Yet this conveyor must travel the full curing rack distance and return an empty pallet to the press within the QT4-15A block machine production line cycle window. If the conveyor motor is undersized or the guide rails introduce friction, the press waits. The complete line quotation must include the return conveyor’s travel speed and motor rating matched to the 25–30 s cycle.
What Happens When the Mixer Discharge Cannot Keep Pace
The raw material mixing station must deliver a fresh batch to the press hopper before the current batch runs out. For a QT4-15A fully automatic concrete block making machine turnkey installation, the mixer capacity and discharge time must align with the press consumption rate across all intended block formats. A mixer sized for hollow blocks may fall behind when the production shifts to denser solid pavers that consume more material per cycle. [NEED_CITE: mixer sizing relative to block press consumption rate]
Matching Vibration, Pressure, and Local Aggregate
The 4200 r/min platform vibration combined with 55 kN vibration force and 16–21 MPa hydraulic pressure defines how densely the QT4-15A compacts concrete into the mould. These three parameters must be evaluated against your local aggregate hardness and gradation. A line configured for river sand in one region may produce under-strength blocks when the same settings are applied to crushed granite dust. The mould cavity fill time, vibration duration, and pressure application sequence are adjusted during commissioning based on trial runs with your actual raw materials. The pallet size of 880×550 mm must also be checked against your curing area dimensions and existing forklift capacity so that pallets move smoothly from press to curing zone without manual intervention.
The Cost of Treating Supporting Equipment as Optional
When pallet feeding, stacking, and curing rack handling are excluded from the initial quotation, the buyer ends up hiring manual labor to move and stack blocks that the press has already produced. This not only slows the overall throughput but introduces handling damage that reduces the saleable output. [NEED_CITE: manual handling damage rates in concrete block plants] A QT4-15A block machine production line that includes automatic stacking and cubing from the outset eliminates this bottleneck and keeps the daily throughput aligned with the press capacity.
Why the Line Is Specified as One System
Every station on the QT4-15A fully automatic concrete block making machine turnkey line is selected to match the press cycle rather than sourced as an independent unit. The raw material feeder delivers aggregate to the mixer at a rate that prevents the press hopper from running dry. The pallet feeding mechanism places a clean pallet under the mould within the return window. The stacking station lifts and cubes cured blocks without requiring a separate forklift operator at that point in the line. Configuration is set against the buyer’s actual mix design and target block format, not a generic catalogue default. Mould design covers the formats the buyer’s market sells, including custom drawings for non-standard dimensions. Automation level is selectable, so a buyer can begin with semi-automatic pallet handling and add full stacking later. Installation includes on-site commissioning with operator training so that every station is tuned before handover. [NEED_CITE: on-site commissioning standards for block production lines]
Documentation & Verification
- Line layout drawing showing every station with cycle time at each point for the QT4-15A
- Capacity calculation stating the exact block format and pallet arrangement assumed
- Mould drawing and format list confirming cavity count per pallet for each block type
- Voltage, frequency, and PLC display language confirmation before production begins
- Factory test record on your specified raw material mix before dispatch
- Wear parts and mould list with hydraulic seal and vibration component part numbers
Installation, Commissioning & Support
- Factory area of 300 m² covers raw material storage, mixing, press, pallet return, stacking, and curing zone
- Overall power of 18.45 kW requires a dedicated circuit with voltage and frequency confirmed for your grid
- Machine ships in 1×40HQ container as a complete unit; supporting equipment packed to match assembly sequence
- On-site commissioning includes vibration duration and pressure tuning against your local aggregate
- Operator training covers PLC navigation, mould change procedure, and daily pallet inspection routine
- Wear parts list supplied at delivery so hydraulic seals and vibration components are available for first replacement
Before You Request a Quotation
To size the QT4-15A block machine production line correctly, share your target block formats with dimensions, the daily output you need per format, and your local raw material source including aggregate type and gradation. Confirm the voltage and frequency at your site, the PLC display language your operators require, and whether your existing curing area and forklift can accommodate 880×550 mm pallets. If you have upstream or downstream equipment already in place, provide its specifications so the line can be matched around it.
Frequently Asked Questions
Q: How do I verify that the mixer and stacker are timed to the QT4-15A molding cycle?
A: Request a line layout drawing that lists the cycle time at each station — feeding, mixing, press, pallet return, stacking. Each upstream and downstream value must fall within the 25–30 s press window. If any station shows a longer time, that station will become a bottleneck and reduce your real daily output below the quoted figure.
Q: What equipment is included beyond the press in a complete line quotation?
A: A full QT4-15A fully automatic concrete block making machine turnkey quotation should list the raw material feeder, mixer, pallet feeding mechanism, return conveyor, automatic stacker, and curing rack handling system. Confirm each item appears with its own specification sheet so nothing is left to manual handling on arrival.
Q: How is daily capacity calculated when multiple block formats share one pallet size?
A: Each format uses a different number of cavities per 880×550 mm pallet and may require a different vibration duration. The quotation must state the daily output separately for each format you intend to produce, with the molding cycle and cavity count that figure is based on clearly written beside it.
Q: Can I start with semi-automatic pallet handling and upgrade the line later?
A: The QT4-15A press can be configured for semi-automatic pallet handling initially, with the mechanical interfaces for a full automatic stacker left in place. When you are ready to upgrade, the stacking and cubing modules are added without replacing the press or modifying the mould system.



