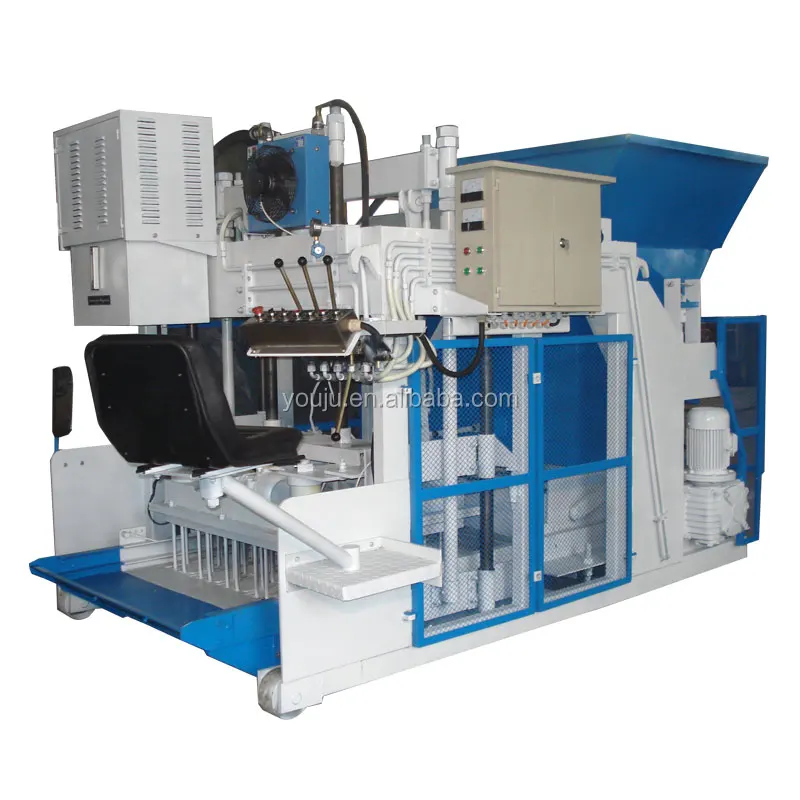
Matched Line Configuration — press, pallet feeding, and stacking specified as one system so cycle times align from raw material infeed to cured output.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QMY12-15 |
| Product Type | Automatic Hollow Block Making Machine |
| Block Format Capability | 9 / 8 / 6 / 4 Inch Hollow Blocks, Cement Brick |
| Automation Level | Automatic production line configuration |
| Hydraulic Pressure | Value to be confirmed |
| Vibration Force | Value to be confirmed |
| Pallet Size | Dimensions and material to be confirmed |
| Cycle Time per Format | Seconds per cycle to be confirmed (basis to be confirmed) |
| Output Capacity | Pieces per hour to be confirmed (basis to be confirmed) |
| Mould Change Time | Minutes to be confirmed |
| Control System | PLC type and brand to be confirmed |
| Power Supply | Voltage and frequency to be confirmed |
| Stacking Method | Manual, automatic stacking, or cubing — options available |
| Assembly State | Production line with optional equipment available |
| PLC Display Language | Language options to be confirmed |
| Certification | CE / ISO availability to be confirmed |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production plant | Crushed stone, sand, cement, fly ash mixes for 9/8/6/4 inch blocks |
| Cement brick manufacturing | Fine aggregate and cement blends for solid brick formats |
| Contractor on-site block supply | Local aggregate and cement for project-specific hollow block formats |
| Multi-format concrete product line | Varying mix designs across hollow block and cement brick moulds |
What "Cycles per Hour" Fails to Tell You About an Automatic Hollow Block Making Machine Production Line
Quoted press speed means nothing if the mixer, pallet feeder, and stacker cannot keep the same pace.
I spent years in QC across Shandong’s manufacturing belt before moving to the commercial side, and the most common failure I have documented on block lines is a mismatch between station cycle times. One plant owner invested in a fast press only to discover the upstream mixer needed an extra thirty seconds per batch, leaving the press idle almost every other cycle. The daily throughput ended up well below the nameplate figure because nobody had calculated the line as a connected system. The automatic hollow block making machine production line must be balanced end to end — not quoted one station at a time [NEED_CITE: industrial line balancing principles for concrete product plants].
How Stations Connect Around the Press
The QMY12-15 sits at the centre of a chain that begins with raw material feeding and mixing, moves through pallet supply, and ends with stacking and curing rack handling. Each station has its own cycle time, and the slowest one sets the real output for the entire automatic hollow block making machine production line. When the mixer delivers a batch every forty-five seconds but the press completes a cycle in twenty, the press waits. Specifying every station against the same target cycle removes that idle window.
Where the Hidden Idle Time Accumulates
Pallet feeding is the station most often underestimated. If the pallet return conveyor cannot deliver a clean pallet before the press is ready, every cycle extends by the difference. Downstream, stacking speed must match or exceed press output; otherwise the operator manually removes blocks while the press pauses. These micro-delays add up across a shift and are rarely captured in a single-station quotation. Documenting each hand-off point during line layout prevents the idle gaps from appearing after installation [NEED_CITE: concrete block plant cycle time audit methodology].
Reading the Specifications That Actually Matter
Hydraulic pressure and vibration force together determine the density and compressive strength of each block. A high vibration value with insufficient hydraulic clamp force produces blocks that crack at the edges during demoulding. The mould format options — 9, 8, 6, and 4 inch hollow blocks plus cement brick — each demand a different pressure and vibration setting, which is why the PLC must store per-format recipes rather than a single default. Pallet size directly dictates how many blocks fit per cycle and must match the curing racks and forklifts already on site. Choosing a pallet dimension without checking the curing area layout forces the plant to restack manually before the blocks can enter the rack system.
The Cost of a Line That Was Never Balanced
When upstream and downstream stations are sourced separately, each supplier quotes their own speed and leaves integration to the buyer. The result is a press that technically meets its cycle time but spends a large share of each shift waiting. Pallet damage rises because return conveyors run out of sync, and block breakage increases when the stacker cannot handle output at full press speed. These problems are not mechanical failures — they are specification failures that only surface weeks after commissioning, when the daily tally consistently falls short [NEED_CITE: common causes of throughput shortfall in block production lines].
Why Sourcing the Full Line From One Supplier Changes the Equation
Block machinery is the single focus here, so the QMY12-15 press, moulds, pallets, and handling equipment are specified as one matched set rather than assembled from separate vendors. The configuration is built around the buyer’s actual mix design and local aggregate, not a catalogue default. Mould design covers the formats the buyer’s market demands, including custom drawings when standard formats do not fit. Automation level is selectable, allowing a plant to start with semi-automatic handling and add stacking or cubing later without replacing the press. Installation support includes operator training so the team understands how each station’s cycle time affects the next.
Documentation & Verification
- Line layout drawing showing station positions and pallet flow path for the QMY12-15
- Capacity calculation stating the block format assumed for each throughput figure
- Mould drawing and format list covering 9/8/6/4 inch hollow block and cement brick
- Hydraulic and electrical schematic for the full production line configuration
- Factory test record on the buyer’s specified block format before dispatch
- Pallet specification sheet matched to curing rack dimensions and forklift capacity
Installation, Commissioning & Support
- Foundation plan indicating load points and anchor positions for the QMY12-15 press and handling stations
- Power supply requirements covering voltage, frequency, and dedicated circuit rating confirmed before production
- Machine dismantling sequence for container loading and on-site reassembly instructions
- First-run commissioning with per-format PLC recipe setup and cycle time verification across all stations
- Operator training on mould change procedure, pallet handling, and daily maintenance checkpoints
- Wear parts and mould list with recommended replacement intervals for hydraulic and vibration components
What to Include in Your Inquiry
Share the block formats you sell most and the daily volume each format must reach. Confirm your local raw materials and typical mix proportions so the line can be configured around what you can actually source. State your site voltage, frequency, and preferred PLC display language early — these details shape the electrical package and prevent delays at commissioning.
Frequently Asked Questions
Q: How is daily output calculated for each block format on the full line?
A: Output is calculated by multiplying cycles per hour by the number of blocks per mould for a specific format, then adjusting for the actual cycle time of the slowest station in the line. The capacity sheet states which format each figure assumes so you can compare against your product mix.
Q: Which supporting stations are included and which are optional?
A: The core line covers raw material feeding, mixing, pallet feeding, the press, and basic stacking. Automatic cubing and curing rack handling are available as optional additions. Each quotation lists included and optional stations separately so you can phase the investment.
Q: How do cycle times at each station match so the press is never starved?
A: Every station is specified against the same target cycle time during line layout. If the mixer batch time or pallet return speed falls outside that window, the station is resized or an additional unit is added before the quotation is finalised.
Q: What voltage, frequency, and PLC language are confirmed before shipment?
A: These are confirmed during the quotation stage and written into the production order. The electrical package and PLC display are built to your specification so the line can be powered up and operated on arrival without rewiring or language changes.
Q: How does the mould change procedure affect line throughput across a shift?
A: Mould change involves stopping the press, swapping the mould, and loading the corresponding PLC recipe. The time required depends on the mould clamping system specified. This changeover window is factored into the daily capacity calculation so the quoted output reflects real shift conditions.