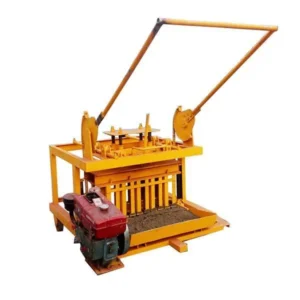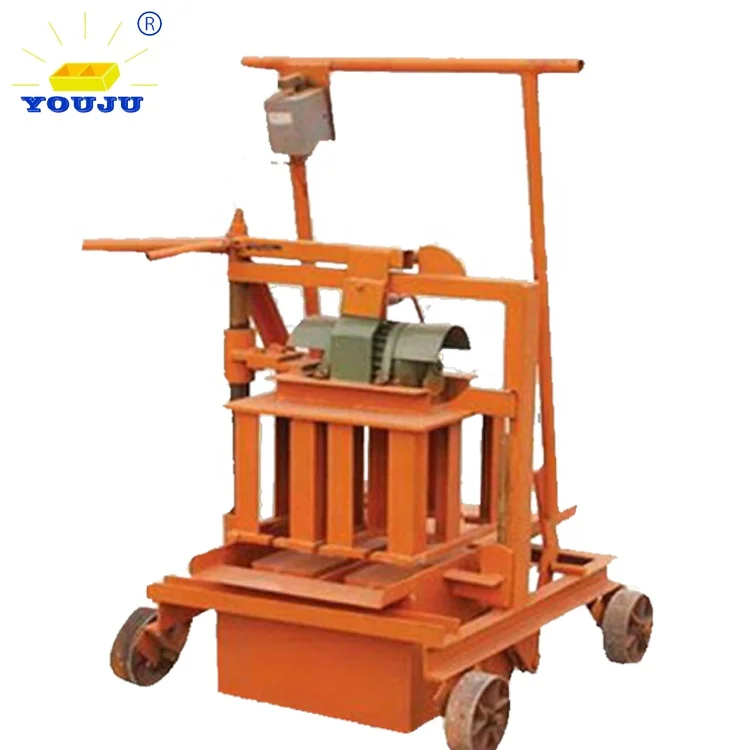
Matching Press to Line — The QMJ2-45 mobile block making machine production line is sized against your actual mixing speed and curing footprint, not a standalone press quotation that ignores upstream and downstream timing.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QMJ2-45 |
| Product Type | Mobile Concrete Block Making Machine |
| Operation Mode | Hand-pushed, palletless egg-laying |
| Molding Cycle | 25–30 seconds per mould |
| Mould Formats Available | 400×200×200 mm, 400×150×200 mm, 400×100×200 mm hollow brick |
| Output — 400×200×200 mm Hollow Brick | 2 pcs/mould, 160 pcs/h, 1280 pcs/8hr (basis: 25–30s molding cycle) |
| Output — 400×150×200 mm Hollow Brick | 3 pcs/mould, 240 pcs/h, 1920 pcs/8hr (basis: 25–30s molding cycle; source listed 4800 pcs/8hr — basis to be confirmed) |
| Output — 400×100×200 mm Hollow Brick | 4 pcs/mould, 320 pcs/h, 2560 pcs/8hr (basis: 25–30s molding cycle) |
| Mould Change | Manual, interchangeable |
| Labour Requirement | 1 to 3 workers |
| Pallet System | Not required |
| Mould Treatment | Heat treatment and carburization |
| Power Source | Electric |
| Standards | ISO9001:2000, CE |
Application Suitability
| Application | Material or Output |
|---|---|
| On-site hollow brick production for building contractors | Crushed stone, sand, and cement mix laid directly on ground |
| Small-scale block plant startups | Multiple hollow brick formats with minimal fixed infrastructure |
| Remote or rural construction sites | Palletless egg-laying operation where pallet return systems are impractical |
| Existing manufacturers adding hollow brick formats | Mobile press running alongside stationary concrete product lines |
What "Cycles per Hour" Means When the Mixer Is Undersized
A block press only runs as fast as the mixer feeds it.
I once watched a QMJ-class mobile press sit idle for half its shift in Kenya because the customer paired it with a small pan mixer that batched slower than the 25–30 second molding cycle demanded. The rated output assumes a continuous supply of mixed material arriving at the press hopper without interruption. When the mobile block making machine production line is quoted without specifying the mixer batch size and discharge interval, the hourly figure on paper never materialises on the ground. Workers end up standing by while the press waits for the next batch, and the daily total falls well short of what the brochure promised [NEED_CITE: mixer-to-press batch timing alignment in small block plants].
Removing Pallet Stations From the Line Layout
The egg-laying design of this press eliminates three stations that a conventional static line requires: pallet feeding, pallet return conveyor, and pallet storage rack. For a contractor setting up production on a job site, this means the mobile block making machine production line occupies only the pressing zone and the adjacent curing area. Blocks are deposited directly onto the ground and left in place until cured, so the line layout centres on how far workers can carry or wheel wet blocks before the next mould cycle completes.
Matching Mixer Batch Frequency to Moulding Rhythm
A 25–30 second moulding cycle means the press consumes one full mould of material roughly every half minute. The supporting mixer must discharge a batch at least this frequently, or the press operator will pause between cycles. We calculate the mixer drum capacity against the volume of concrete each mould draws, then confirm the discharge interval matches the press cadence. If your local aggregate is coarse or the mix is stiff, discharge slows and the gap widens — a detail that only surfaces when the line is mapped as a system rather than sold as individual machines [NEED_CITE: aggregate gradation effect on mixer discharge rate].
Reading the Output Table With the Right Block in Mind
The specification sheet lists three hollow brick formats, each with a different piece count per mould. The 400×200×200 mm format yields two blocks per cycle, while the 400×100×200 mm format yields four — doubling the hourly piece count without changing the press speed. This matters when sizing the curing area: a line producing the smaller format at 320 pieces per hour needs a ground area large enough to hold roughly 2,560 blocks per shift, all laid flat and spaced for air circulation. The heat-treated and carburised mould surfaces hold dimensional accuracy across these format changes, so blocks remain consistent in wall thickness and interlock geometry even after repeated mould swaps. The manual mould change procedure is covered in the operation documentation and requires basic hand tools.
The Cost of Quoting a Press Without the Line Around It
When quotations list only the press, buyers arrive at site and discover they still need a mixer, raw material feeder, water supply arrangement, and a curing zone with adequate space and protection from rain. Sourcing these separately often leads to mismatched capacities — a mixer too slow, a water tank too small, or a curing area that fills up before the shift ends. The press then bottlenecks on logistics rather than mechanics. I have seen projects lose weeks recalculating the layout after the equipment arrived because nobody had mapped the upstream feed rate against the press cycle [NEED_CITE: common line imbalance issues in small-scale block production].
Why Sourcing the Supporting Equipment Together Matters
Block machinery as a single focus means the QMJ2-45 press, its interchangeable moulds, and the supporting mixer and feeding equipment are specified as a matched set rather than assembled from separate vendors. The configuration is set against your actual mix design and local aggregate, not a catalogue default. Line layout and capacity calculations state which block format each output figure assumes, so there is no ambiguity when you compare daily totals against your project schedule. Voltage, frequency, and control language are confirmed before production begins, preventing commissioning delays when the equipment reaches your site. Mould design covers the formats your market actually sells, including custom drawings when standard sizes do not match local building codes.
Documentation & Verification
- Line layout drawing showing mixer placement, press travel path, and curing area dimensions matched to your chosen block format
- Capacity calculation sheet stating the block format and moulding cycle assumed for each output figure
- Mould drawing and format list confirming dimensional compatibility with local hollow brick standards
- Voltage and frequency confirmation record for the press motor and any supporting mixer or feeder
- Factory test record on your specified block format before dispatch
- Operation and maintenance manual covering manual mould change procedure and wear parts list
Installation, Commissioning & Support
- Ground preparation guidance specifying the flatness and compaction required for palletless egg-laying operation
- Electrical connection schedule confirming voltage and dedicated circuit requirements for the press motor and mixer
- On-site assembly covering wheel alignment and mould mounting after transport dismantling
- First-run moulding trial on your local aggregate mix to verify block density and dimensional tolerance
- Operator training on manual mould change across the three standard hollow brick formats
- Wear parts list covering mould liner and vibration components with replacement intervals
What to Include With Your Inquiry
Send us your target hollow brick format and the daily output you need so we can calculate the mixer batch size and curing area required around the QMJ2-45. Include your local voltage and frequency, the type of aggregate available on site, and whether you already have a mixer or need one specified as part of the mobile block making machine production line. If you have an existing curing area or a forklift with a specific turning radius, note those dimensions so the line layout accounts for them from the start.
Frequently Asked Questions
Q: How do I calculate realistic daily output for my block format?
A: The output table ties each figure to a specific block size and a 25–30 second moulding cycle. Identify which format you will produce most, then multiply the hourly rate by your actual working hours, subtracting time for mould changes, mixer refill pauses, and block transfer to the curing area. We provide a capacity calculation sheet that states the format assumed.
Q: What supporting equipment does a palletless mobile press still need?
A: Even without pallets, the press requires a mixer that can discharge batches at the press cadence, a consistent water supply, and a flat, prepared ground area for blocks to cure in place. Raw material feeding can be manual at small scale or upgraded to a belt feeder as output grows.
Q: How should I size the mixer to avoid press idle time?
A: The mixer drum must hold enough concrete for at least one mould cycle and discharge within the 25–30 second window. We match the drum capacity and motor power to the volume each mould draws, then confirm the discharge rate on your specific mix design before finalising the line.
Q: Why must voltage and frequency be confirmed before shipment?
A: The press motor and any supporting mixer are wound for a specific voltage and frequency combination. Running a motor on the wrong supply causes overheating and premature failure. We record your site supply details before production and label all electrical panels accordingly.
Q: How much curing space do I need when blocks are laid on the ground?
A: Curing area depends on your daily output and block footprint. At 320 pieces per hour of 400×100×200 mm blocks, one shift produces roughly 2,560 units. Each block needs spacing for air circulation, so we calculate the total ground area required and factor in worker access paths for watering and inspection.