
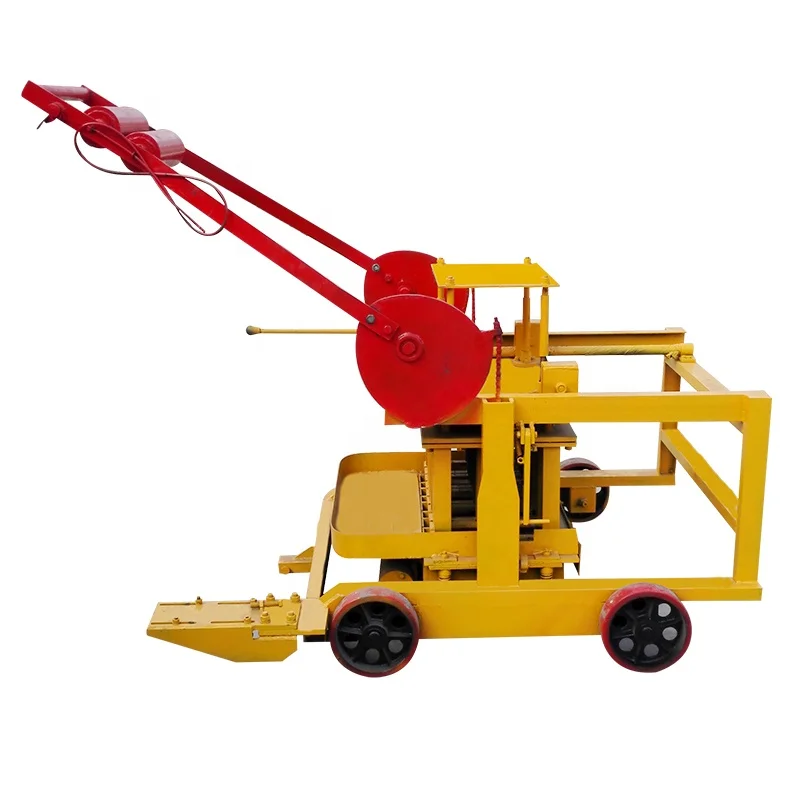
Single-focus block line design — the mixer, trolley and press are specified together so feed rate matches cycle time and the machine never waits for material on site.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QMR4-45 |
| Product Type | Mobile Concrete Block Making Machine |
| Power Source | Diesel / Petrol Engine / Electric (configurable) |
| Overall Dimensions (L×W×H) | 1100 × 950 × 2100 mm |
| Net Weight | 810 kg |
| Molding Cycle | 30–45 s |
| Output Capacity | 2,560 pcs/day (basis not stated in source — confirm block format, material and thickness) |
| Pallet Requirement | None (egg-laying type) |
| Mobility | Movable on-site |
| Block Formats | Hollow block, solid brick, paver brick, fly ash brick, concrete block |
| Basic Equipment Included | JZC350 Diesel Concrete Mixer or JQ350 Diesel Concrete Mixer with Electric Generating Unit; Trolley |
| Automation Level | Manual / Semi-automatic |
| Warranty | 1 Year |
Application Suitability
| Application | Material or Output |
|---|---|
| On-site hollow and solid block production | Crushed stone, sand, cement, fly ash blends |
| Remote construction camp masonry supply | Locally sourced aggregate with cement binder |
| Housing project phased block manufacturing | Paver bricks and interlocking formats per phase |
| First-time small plant operation | Low-footprint setup before scaling to fixed lines |
| Contractor self-supply at building sites | Concrete blocks and solid bricks from site-mixed material |
Why the Mixer Matters More Than the Press Rating
A mobile block machine production line is only as fast as its slowest station.
Quoted output figures for the QMR4-45 often appear without stating which block format or wall thickness they assume. When the mixer delivers material slower than the press cycle demands, the operator stands idle and daily throughput drops well below expectation. This is the single most common mismatch I see in mobile setups sent to remote project sites [NEED_CITE: mixer-to-press cycle matching in mobile block plants]. Specifying the JZC350 diesel mixer or the JQ350 with its generating unit alongside the press keeps the feed rate aligned with the 30–45 second molding cycle, so the mobile block machine production line runs without dead time between batches.
Feeding the Press Without a Fixed Conveyor
The QMR4-45 drops freshly molded blocks directly onto the ground — no pallet, no pallet-return conveyor, no curing rack system. That simplicity is exactly what a remote site needs, but it also means the trolley operator must keep pace with every 30–45 second cycle. The included trolley is sized for this rhythm, and the diesel mixer batch volume is matched so one mix fills roughly one trolley load. When those three elements — mixer, trolley, press — are quoted as separate items from different suppliers, cycle times rarely align.
Power Source and Site Reality
Diesel, petrol and electric options let the mobile block machine production line run where grid power is unreliable or absent. On projects I have supported in West Africa, the diesel mixer variant kept production going during multi-day outages that would have shut down an electric-only setup [NEED_CITE: power reliability challenges in Sub-Saharan construction sites]. The electric generating unit paired with the JQ350 mixer offers a middle path: electric motor precision without grid dependency. Confirming voltage and frequency for the destination market before the machine leaves the factory avoids the three-week transformer delay I once watched stall an entire shipment.
Reading the Specs That Actually Matter
The 1100 × 950 mm footprint tells you the press fits through a standard doorway and can be repositioned by two workers as the build progresses. Net weight of 810 kg means the machine is stable during vibration molding yet light enough to lift onto a flatbed between project phases. The 30–45 second molding cycle range reflects the difference between a thin paver brick and a deeper hollow block — thicker formats push the cycle toward the upper end because the vibration must compact more material volume. Block format directly determines realistic daily output, which is why any capacity discussion must start with the specific product the buyer intends to sell.
When Supporting Equipment Gets Left Off the Quote
A press quoted without its mixer, trolley and power unit looks cheaper on paper but forces the buyer to source compatible equipment locally — often at higher cost and with mismatched cycle times. The egg-laying design eliminates pallets and their associated storage area, but it still demands a flat, level curing surface close to the molding point. When that ground preparation is overlooked, blocks settle unevenly and strength suffers, and the buyer blames the machine instead of the site layout [NEED_CITE: ground preparation requirements for egg-laying block machines].
What Makes This Line Different
Block machinery is the single focus here, so the QMR4-45 press, mixer, trolley and power unit arrive as one matched system rather than separate purchases assembled by the buyer. Configuration is set against the buyer’s actual aggregate source and target block format, not a catalogue default. Mould design covers the formats the buyer’s local market actually demands, including custom drawings when standard options do not fit. The automation level is selectable — a buyer can begin with manual trolley handling and add semi-automatic controls later without replacing the press. Installation support includes operator training so the crew understands cycle timing, mix ratios and basic maintenance from day one.
Documentation & Verification
- Line layout showing mixer, trolley and press positioning with cycle time alignment
- Machine specification sheet confirming power source, voltage and frequency for your market
- Mould drawing and format list with dimensional tolerances per block type
- Factory test record on the block format and mix design you confirm before dispatch
- Operation and maintenance manual with wear parts list for both press and mixer
Installation, Commissioning & Support
- Flat, level curing area prepared to match the 1100 × 950 mm press footprint and trolley path
- Power supply verified — diesel tank capacity or electric circuit rated for the chosen mixer variant
- Mixer discharge height checked against trolley loading point to prevent spillage during transfer
- First-run molding cycle timed at 30–45 seconds with your confirmed block format and aggregate
- Operator training on mould change, vibration adjustment and daily grease-point maintenance
- Wear parts list supplied for both QMR4-45 press and included mixer model
Before You Request a Quote
To size this mobile block machine production line correctly, share the specific block format and dimensions your market requires, the aggregate and cement source available at your project site, and the daily output target in finished pieces. If you are choosing the electric generating unit variant, confirm your local voltage and frequency so the unit is wound to match before it ships.
Frequently Asked Questions
Q: How is the 2,560 pieces per day figure verified, and which block format does it assume?
A: That number depends entirely on the block format, wall thickness and mix design in use. A thin solid brick cycles faster than a large hollow block, so the same press produces different daily totals. We state capacity per confirmed format after reviewing your specific product drawing and material source, not from a generic table.
Q: How do I match the mixer output to the press cycle so the line does not bottleneck?
A: The included JZC350 or JQ350 mixer is batch-sized to deliver enough material for roughly one trolley load per mix. This keeps feed rate aligned with the 30–45 second press cycle. If your mix design uses heavier aggregate, batch time may extend, and we adjust the specification accordingly before quoting.
Q: What voltage and frequency options are available for the electric generating unit variant?
A: The generating unit can be wound to common export voltages including 220V, 380V and 440V at 50 or 60 Hz. You must confirm your destination market standard before production begins. Incorrect voltage is the most frequent cause of commissioning delays on international shipments.
Q: What supporting equipment needs to be in place before the press starts on site?
A: A flat, compacted curing surface adjacent to the molding area is essential since the egg-laying design places blocks directly on the ground. You also need water supply for the mixer and, for diesel variants, a fuel storage point. We provide a site preparation checklist with the quotation.
Q: What is the lead time from order to on-site delivery for a complete mobile line setup?
A: Typical multi-week lead times apply from order confirmation to factory test completion, followed by container loading and ocean transit. The total timeline depends on your destination port and whether custom moulds are included. We quote the arrival estimate before you commit.


