
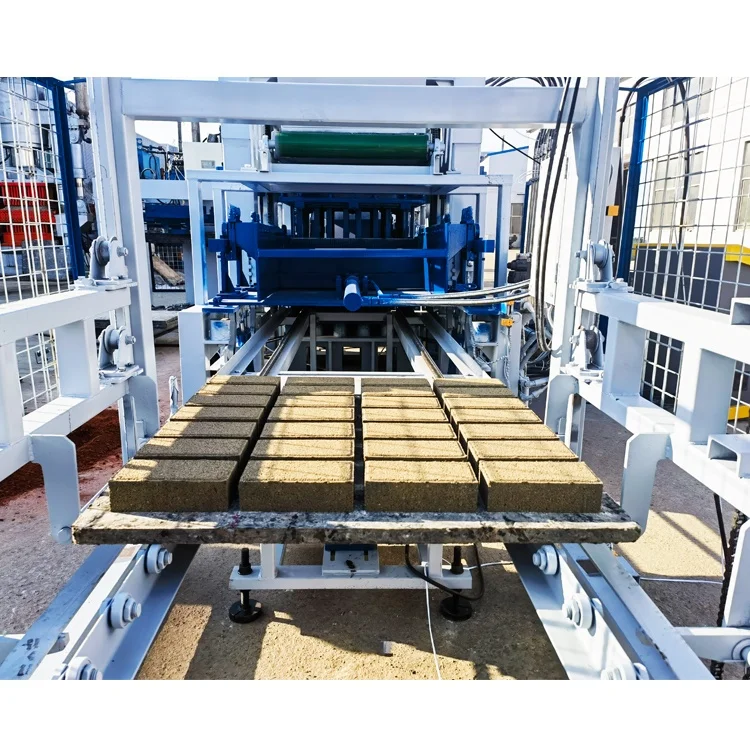
Matched line cycle times — QT612 block production line stations are configured together so the press, mixer and pallet loop never idle waiting for each other.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT612 |
| Product Type | Hydraulic Block Making Machine |
| Overall Dimensions (L×W×H) | 7350×1780×2950 mm |
| Rated Pressure | 16 MPa |
| Main Vibration | Platform vibration |
| Vibration Frequency | 4600 r/min |
| Pallet Size | 880×700 mm |
| Moulding Cycle | 15-20 s |
| Overall Power | 30.5 kW |
| Output Capacity (Hollow Brick 400×200×200 mm) | 6 pcs/mould, 1080 pcs/h, 8640 pcs/day (basis: 12-15 s cycle) |
| Output Capacity (Porous Brick 240×115×90 mm) | 14 pcs/mould, 2800 pcs/h, 22400 pcs/day (basis: 15-18 s cycle) |
| Output Capacity (Standard Brick 240×115×53 mm) | 30 pcs/mould, 6800 pcs/h, 54400 pcs/day (basis: 14-17 s cycle) |
| Applied Products | Hollow blocks, solid blocks, porous bricks, paving stones, interlocking blocks, kerbstones, slope blocks |
| Standards | CE, SGS, ISO 9001 |
| Automation Level | Automatic |
Application Suitability
| Application | Material or Output |
|---|---|
| Building construction | Hollow and solid concrete blocks from cement, sand, crushed stone |
| Road and square paving | Paving stones and interlocking pavers with face mix |
| Garden and landscaping | Kerbstones, edgers, grass blocks from local aggregate |
| Infrastructure slope protection | Slope blocks and interlocking blocks using fly ash and slag |
| Industrial waste recycling | Blocks incorporating cinder, gangue, perlite and coal fly ash |
Why the Mixer Discharge Rate Must Match the Press Cycle
A press rated at 15-20 seconds per cycle will idle if the mixer cannot discharge a full batch within that window.
When I plan a block production line, I calculate the mixer discharge time against the QT612 moulding cycle first. I once saw a plant in West Africa pair a fast-cycling press with an undersized mixer, and the operator stood waiting for material for over forty seconds every cycle. That gap alone cut daily output by a noticeable margin before any other bottleneck appeared [NEED_CITE: block plant mixer sizing guidelines]. The complete turnkey block making plant must account for every station between raw material intake and cured output.
How Each Station Feeds the Next
A block production line is only as fast as its slowest handoff. The raw material feeding system must deliver aggregate to the mixer at a rate that keeps the hopper from running dry mid-batch. The mixer then discharges into a distribution hopper above the press, and that hopper must release material fast enough to fill the mould cavity before the vibration phase starts. If any one of these transfers lags, the QT612 platform vibration at 4600 r/min fires on an underfilled mould and produces a lighter, weaker block.
Pallet Circulation Sets the Real Rhythm
The 880×700 mm pallet leaves the press carrying a wet block and travels through the stacking station, then the curing rack, and finally returns to the pallet feeder. The total loop distance and the speed of each conveyor segment determine how many pallets you need in circulation. On a block production line with limited curing yard space, the return speed drops and pallets queue up, forcing the press to pause. Calculating the full loop time before ordering pallets prevents a situation where the press is capable but the line is not [NEED_CITE: pallet return loop calculations for block plants].
What Vibration and Pressure Together Mean for Block Density
Platform vibration at 4600 r/min fluidises the concrete mix inside the mould cavity, allowing aggregate particles to settle tightly. The 16 MPa rated hydraulic pressure then compresses that settled mix from above. Both forces must be present: vibration without enough pressure leaves air pockets, while pressure without sufficient vibration cannot compact a stiff mix evenly across a large pallet area. For hollow blocks at 400×200×200 mm, this combination produces a consistent wall density across all six cavities per mould. For denser formats like standard bricks at 30 pieces per mould, the same vibration frequency must penetrate a taller stack of material, which is why the cycle extends to 14-17 seconds.
The Hidden Cost of Ignoring Pallet Specification
Pallet size and material are often decided after the press is ordered, and that sequence causes problems downstream. An 880×700 mm pallet must fit the buyer’s existing curing rack slots and forklift tine spacing. If the rack was built for a different pallet dimension, the buyer either rebuilds the rack or runs a mixed pallet inventory. Wooden pallets warp in humid climates and change the block height slightly each cycle, while steel pallets add weight that the return conveyor motor must handle [NEED_CITE: pallet material performance in tropical block production]. These mismatches show up weeks after commissioning, not on the quotation.
Why a Line Layout Drawing Matters Before Commitment
A block production line involves Shiyue Machinery as a single source for press, mould, pallet and handling equipment, so the layout drawing reflects actual station positions rather than assumed clearances. Each capacity figure on that drawing states the block format it was calculated for, avoiding the common situation where a headline hourly number was based on a small brick format the buyer does not sell. The mould list is confirmed before production, so the buyer receives the formats their market demands rather than a catalogue default set. Voltage, frequency and PLC display language are locked in before the control panel is wired, which prevents a commissioning delay that I have seen hold up projects for weeks.
Documentation & Verification
- Line layout drawing with capacity stated per block format for the QT612
- Pallet specification sheet confirming 880×700 mm dimension, material and weight
- Factory test record showing cycle time and block strength on your mix design
- Voltage, frequency and PLC language confirmation document before panel wiring
- Mould drawing and format list matched to your market requirements
- Operation and maintenance manual covering the QT612 hydraulic and vibration systems
Installation, Commissioning & Support
- Foundation plan sized for 7350×1780×2950 mm QT612 footprint and vibration load
- Power supply rated for 30.5 kW overall draw with dedicated circuit breaker
- Machine arrives dismantled; reassembly sequence provided with bolt torque values
- Commissioning includes cycle time verification at 15-20 s on your block format
- Operator training covers mould change procedure and platform vibration adjustment
- Wear parts list with hydraulic seal and vibration mount part numbers for reorder
Before You Request a Quotation
To size a block production line around the QT612, share the block formats your market actually sells and the daily volume you need per format. Confirm the local aggregate type and whether fly ash or slag will be part of the mix, because that determines mixer selection. State your available curing yard area and the forklift model you already operate so the pallet specification and return conveyor can be matched. Finally, provide the site voltage and frequency along with the preferred control display language.
Frequently Asked Questions
Q: How is daily output calculated per block format on this block production line?
A: Each format has its own moulding cycle. Hollow blocks at 400×200×200 mm run on a 12-15 second basis yielding 8640 pieces per day, while standard bricks at 240×115×53 mm use a 14-17 second basis for 54400 per day. The line throughput changes when you switch formats because cycle time, pallet return speed and stacking pattern all differ.
Q: How do I match the mixer discharge rate to the QT612 cycle?
A: The press moulding cycle is 15-20 seconds. The mixer must discharge one full batch into the distribution hopper within that window, including the time for the hopper gate to close. We calculate mixer drum volume and discharge gate size against your target cycle so the press never idles waiting for material.
Q: What pallet material suits a humid tropical curing environment?
A: Wooden pallets absorb moisture and warp, changing block height across the 880×700 mm surface. Steel or composite pallets hold dimension better but weigh more, requiring the pallet return conveyor motor to be sized accordingly. We specify pallet material and thickness based on your climate and existing curing rack load capacity.
Q: Which line stations can be added later as production grows?
A: A buyer can start with manual pallet handling and add automatic stacking and cubing stations later. The QT612 pallet feeder interface remains the same, so the upgrade connects without modifying the press frame. We provide the electrical and mechanical connection points on the initial machine to keep the upgrade path open.



