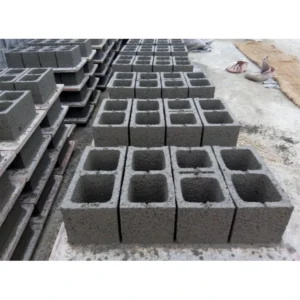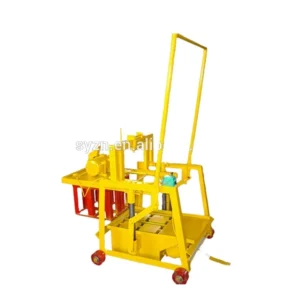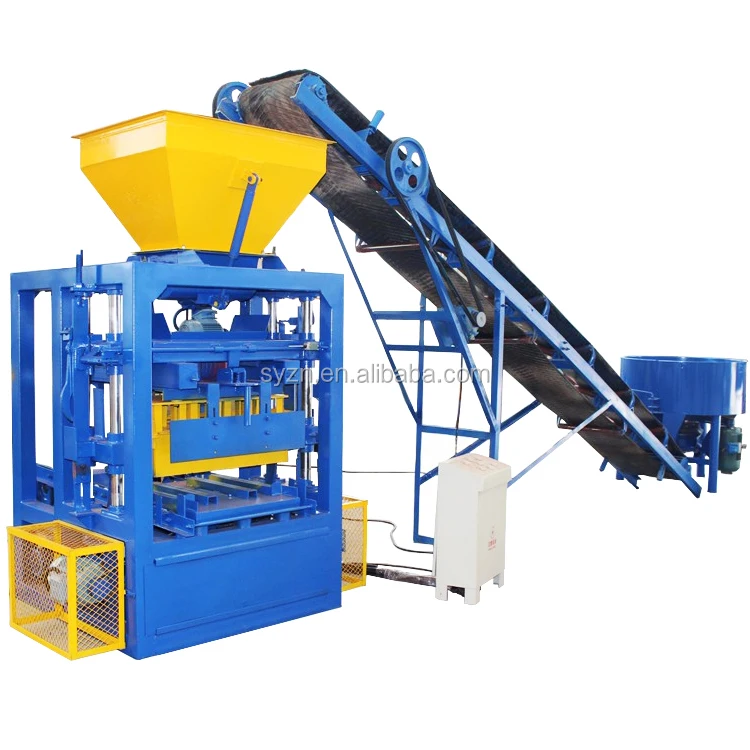
Matched Line Flow — Every station from the JQ350 mixer through to the curing rack is timed to the Qt4-26 press cycle, so the machine runs continuously without waiting for upstream feed or downstream pallet clearance.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | Qt4-26 |
| Product Type | Semi-automatic Concrete Block Making Machine |
| Dimension of Host Machine | 2060×1730×2580 mm |
| Rated Pressure | 26 MPa |
| Main Vibration Form | Platform Vibration |
| Vibration Frequency | 4500 r/min |
| Vibration Force | 40 kN |
| Pallet Size | 880×480×25 mm |
| Molding Cycle | 15–20 s (basis not stated in source — confirm block format) |
| Total Power | 19.75 kW |
| Host Machine Power | 14.25 kW |
| Total Mass | 2 T |
| Demolding Method | Semi-automatic |
| Mixer Model | JQ350 |
| Assembly State | Fully assembled line (press + JQ350 mixer) |
| Applied Products | Hollow blocks, solid blocks, pavers, interlocking blocks, kerbstones, colored pavers |
| Raw Materials | Crushed stone, sand, cement, fly ash, gravel, slag |
| Standards | CE |
Application Suitability
| Application | Material or Output |
|---|---|
| Small to mid-size block plant | Hollow and solid blocks from crushed stone, sand, and cement |
| On-site contractor production | Interlocking blocks and pavers using local aggregate and fly ash |
| Landscaping and municipal supply | Colored pavers and kerbstones from standard concrete mixes |
| First-time entrepreneur plant | Mixed-format output for buildings, roads, squares, and gardens |
What "15–20 Seconds per Cycle" Leaves Out for a Semi-automatic Block Making Machine production line
A cycle time only becomes real daily output when the mixer batch window, pallet feed rate, and manual stacking pace are all matched to it.
I have watched block plants stall within the first week because the upstream mixer could not deliver a fresh batch before the press finished its cycle. The press sat idle while the operator waited. On other sites, the pallet conveyor jammed every third cycle because the curing rack spacing did not match the 880×480 mm pallet, forcing the operator to clear pallets by hand. The Semi-automatic Block Making Machine production line only reaches its stated rhythm when every station around it is specified to the same tempo [NEED_CITE: line balancing principles in concrete block manufacturing].
Mixer-to-Press Timing
The JQ350 mixer included with this line must discharge a full batch into the press hopper within the 15–20 s molding window. If the mixer cycle runs longer, the press idles and the stated cycle time becomes meaningless. We specify the JQ350 because its batch volume and discharge speed align with the Qt4-26 hopper capacity, keeping material flowing without overfilling.
Pallet Flow and Curing Rack Alignment
The 880×480×25 mm pallet governs every station downstream of the press. The pallet feeder must accept this exact dimension, the curing rack slots must be spaced to receive it, and the forklift tines must be wide enough to collect stacked pallets without tipping. When any one of these dimensions is mismatched, the Semi-automatic Block Making Machine production line stops while operators clear the bottleneck by hand [NEED_CITE: pallet dimension standards in concrete block plants].
Reading the Vibration and Pressure Specs Together
Platform vibration at 4500 r/min and 40 kN of vibration force work in combination with the 26 MPa rated hydraulic pressure to compact the mix into a dense block. Vibration alone settles the aggregate; hydraulic pressure alone squeezes water out. The two forces must be balanced against the buyer’s specific mix design and local aggregate gradation to produce consistent block strength across every cycle.
The Cost of Ignoring Line Balance
When a buyer orders only the press and sources the mixer and pallet handling locally, the stations rarely match. The mixer discharges too slowly or too quickly, the pallet feeder jams on undersized pallets, and the curing racks cannot accept the pallet dimensions the press was built around. These mismatches surface after the machine arrives, when changing any single station means re-engineering the layout on the shop floor [NEED_CITE: concrete block line integration challenges].
Why This Line Is Quoted as a System
Block machinery as a single focus means the Qt4-26 press, JQ350 mixer, pallet specification, and handling stations are sized together before quotation, not assembled from separate suppliers after the fact. The configuration is set against the buyer’s actual mix design and local aggregate, not a catalogue default. Pallet size and material are confirmed against the buyer’s existing curing area and forklift. Voltage, frequency, and control language are locked in before production starts. Mould design covers the formats the buyer’s market actually sells. Automation level is selectable, so a plant can begin semi-automatic and add stacking or cubing later without replacing the press.
Documentation & Verification
- Line layout drawing showing station positions and pallet flow path for the 880×480 mm format
- Capacity calculation sheet stating the block format assumed for the 15–20 s cycle
- Hydraulic and electrical schematic covering both the press and the JQ350 mixer
- Pallet specification cross-referenced with curing rack spacing and forklift dimensions
- Factory test record run on the buyer’s target block format before dispatch
- CE declaration documentation for import compliance
Installation, Commissioning & Support
- Foundation plan based on the 2060×1730 mm host machine footprint and 2 T total mass
- Power supply confirmation for 19.75 kW total load with dedicated circuit requirements
- Fully assembled line delivery with station-by-station alignment check on site
- Mixer discharge timing calibrated to the 15–20 s press cycle during commissioning
- Operator training covering mould change procedure and pallet feed sequencing
- Wear parts and mould list supplied for first replacement planning
Before You Request a Quote
To size the supporting stations correctly, we need your target block format and dimensions, your local raw material source and aggregate gradation, and the curing area layout you already have or plan to build. Share your site voltage and frequency, the forklift model you will use for pallet transfer, and whether you need the line configured for a specific daily output target.
Frequently Asked Questions
Q: How does the 15–20 s molding cycle translate to real daily output?
A: The 15–20 s figure is a press cycle time, not a finished-block count. Real daily output depends on which block format is being produced, how fast the JQ350 mixer can deliver batches, and how quickly operators clear pallets from the curing area. We provide a capacity calculation that states the assumed block format so the number is verifiable before purchase.
Q: Which supporting stations are included in the line quotation?
A: The Qt4-26 press and JQ350 mixer ship as a matched set. Pallet feeder, curing racks, and stacking stations are specified based on your site layout and added to the quotation separately. This prevents mismatched dimensions that would otherwise surface during installation.
Q: How must the mixer batch time match the press cycle?
A: The JQ350 must discharge a full batch into the press hopper within the 15–20 s window. If the mixer takes longer, the press idles and output drops. We confirm batch volume and discharge speed during configuration so the two stations stay synchronized.
Q: Is the 880×480 mm pallet compatible with standard curing racks?
A: Compatibility depends on the rack slot width and the forklift tine spacing at your site. We cross-reference the pallet specification against your existing equipment before production so that pallets move from press to rack to dispatch without manual repositioning.
Q: What documentation arrives with the line?
A: You receive a line layout drawing, capacity calculation per block format, hydraulic and electrical schematics for all stations, a pallet specification sheet, and a factory test record run on your target format. These documents support local maintenance planning and import compliance.