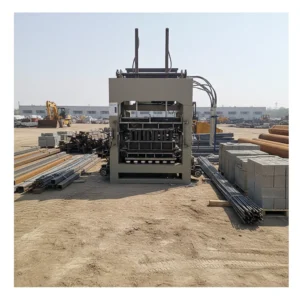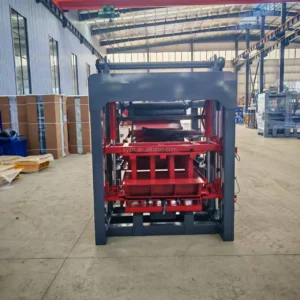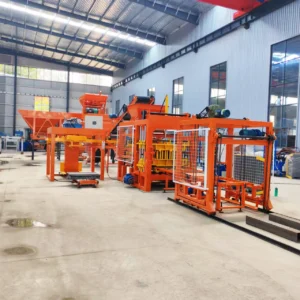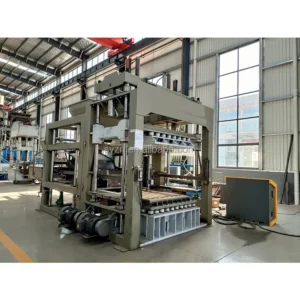
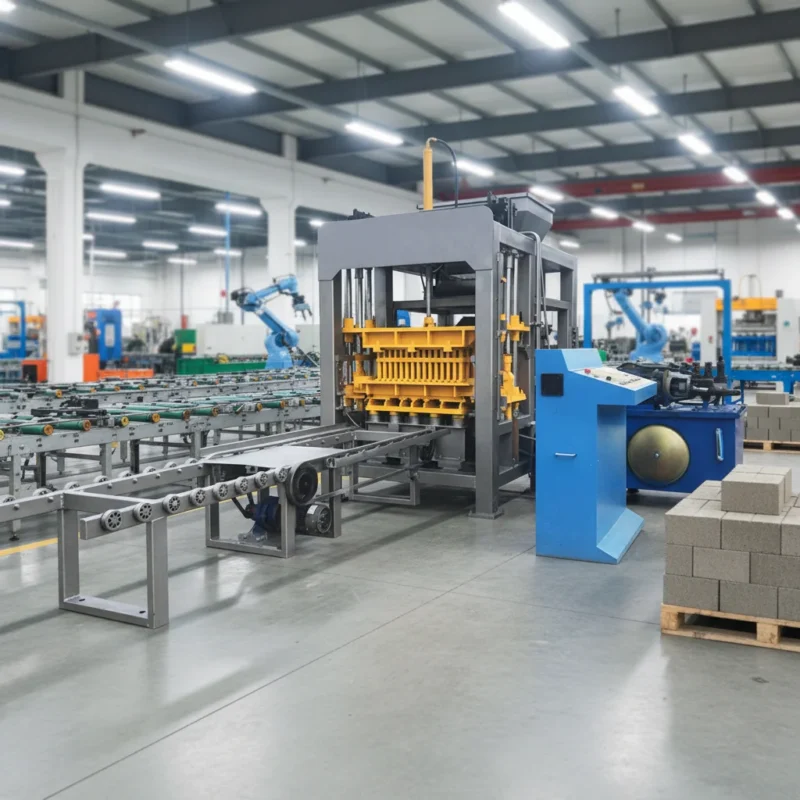
Matched Line Configuration — every station from raw material feed to stacking is sized against the QT10-15 cycle time so the press is never left waiting for upstream or downstream equipment.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT10-15 |
| Product Type | Automatic Cement Block Making Machine |
| Control System | PLC control cabinet |
| Hydraulic System | Independent integrated hydraulic station |
| Vibration Mode | Vertical station mode resonance with automatic FM-AM |
| Cycle Time | 15–25 seconds depending on block format |
| Mould Change | Quick replacement system for multi-format production |
| Line Components | Pallet feed machine, block making machine, storage hopper, conveyor, hydraulic unit, PLC control cabinet |
| Output (Hollow Block 400×200×200mm) | 14,400–19,200 pcs / 8 hr (basis: 15–20s cycle, 10 pcs/mould) |
| Output (Hollow Block 400×150×200mm) | 17,280–23,040 pcs / 8 hr (basis: 15–20s cycle, 12 pcs/mould) |
| Output (Solid Brick 240×115×53mm) | 71,424–89,280 pcs / 8 hr (basis: 15–20s cycle, 62 pcs/mould) |
| Output (Paver 200×100×60mm) | 41,472–51,840 pcs / 8 hr (basis: 20–25s cycle, 27 pcs/mould) |
| Output (Paver 225×112.5×60mm) | 32,256–40,320 pcs / 8 hr (basis: 20–25s cycle, 24 pcs/mould) |
| Assembly State | Complete line with supporting equipment |
| Rated Power | To be confirmed |
| Voltage & Frequency | To be confirmed |
| Overall Dimensions | To be confirmed |
| Net Weight | To be confirmed |
| Pallet Size | To be confirmed |
| Stacking Method | To be confirmed |
| Warranty | 1 year for the whole machine (excluding spare parts) |
| Certification | CE (verify for this specific model) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for commercial and residential walls | Crushed stone, sand, cement, fly ash blends |
| Solid brick manufacturing for load-bearing structures | Local aggregate with cement binder |
| Interlocking paving block for driveways and walkways | Fine aggregate, cement, pigment additives |
| Kerbstone and multi-cellular brick for municipal projects | Coarse aggregate with high cement content |
| Porous permeable brick for stormwater management | Open-graded aggregate with controlled cement ratio |
What "14,400 Blocks per Shift" Leaves Out About Your automatic block making machine production line
Capacity means nothing if the pallet feeder runs out before the press finishes its cycle.
A quoted output figure typically assumes the press running uninterrupted at peak cycle speed. In reality, the storage hopper empties, the pallet feed machine jams, or the conveyor cannot keep pace with the mixer output. I once helped a West African plant owner troubleshoot a line that never reached its stated daily volume — the press was fine, but the pallet return conveyor was undersized for the curing rack distance, so operators spent half the shift moving pallets by hand [NEED_CITE: typical bottleneck sources in block production lines]. When planning an automatic block making machine production line, the question is not what the press can do in isolation but whether every surrounding station can sustain that tempo for eight continuous hours.
How Station Synchronization Keeps the QT10-15 Running
An automatic block making machine production line lives or dies by its slowest station. The QT10-15 completes a cycle every 15 to 25 seconds depending on the block format, which means the pallet feed machine must deliver a fresh pallet within that same window while the block conveyor removes the finished layer. The storage hopper and raw material conveyor are sized so that the mixer never starves the press hopper mid-cycle. This synchronization is where most lines fail — one undersized station turns a theoretical capacity figure into a daily disappointment.
Matching the Line to Your Curing Area and Forklift
The pallet size specification is not a machine parameter alone; it must align with the curing racks and the forklift the plant already operates or plans to buy. A pallet that is too wide for the existing rack system forces a complete rack replacement before the first block is produced. The stacking method and automation level determine how many workers are needed between the press output and the curing zone. Getting this wrong means paying for automation on the press side while still relying on manual labor to move and stack every layer [NEED_CITE: pallet handling and curing area planning for block plants].
Reading the Specs That Actually Matter on Site
The independent integrated hydraulic station is physically isolated from the main press vibration and dust exposure. On a block line running eight-hour shifts with continuous impact loading, hydraulic valves and seals degrade faster when exposed to resonance and airborne cement dust. Separating the station extends service intervals and reduces unplanned downtime during peak production periods.
The vertical station mode resonance with automatic FM-AM vibration tuning adjusts the vibration profile as the mould fills. Different block formats — a thin paver versus a tall hollow block — need different force distribution across the mould cavity. Automatic tuning means the operator does not manually recalibrate between format runs, which keeps density consistent across the batch.
The PLC control cabinet coordinates every station in the automatic block making machine production line from a single interface. When a pallet sensor trips or the hopper level drops below threshold, the PLC pauses the sequence in the correct order rather than letting the press cycle on an empty mould. This prevents damage to the mould face and avoids producing a batch of under-formed blocks that must be scrapped.
The quick mould replacement system allows format changes within a single shift rather than consuming the entire shift. For plants that run hollow block in the morning and switch to pavers after lunch, the changeover time directly determines whether two formats per day is realistic or theoretical.
The Hidden Cost of Specifying the Press Alone
Plant owners who select a block press based on its cycle time and then source conveyors, mixers, and pallet feeders from separate suppliers frequently discover timing mismatches during commissioning. The mixer batch cycle does not align with the press cycle, so the hopper alternates between overflowing and running dry. Pallets accumulate on the return side because the conveyor speed was never calculated against the curing rack distance. These problems do not show up in a catalogue quotation — they surface only when the line is assembled on site and the first full shift reveals where the bottleneck actually sits [NEED_CITE: risks of multi-supplier block line assembly].
Why Sourcing the Full Line from One Configuration Point Matters
The QT10-15 is specified as a matched system: pallet feed machine, storage hopper, conveyor, hydraulic unit, and PLC control cabinet are selected together so that each station’s throughput aligns with the press cycle time for every block format in the mould list. Configuration is set against the buyer’s actual mix design and local aggregate rather than a default catalogue recipe, which matters because aggregate grading and moisture content directly affect vibration tuning and hydraulic pressure requirements. Moulds are designed for the specific formats the buyer’s market demands, including custom drawings when standard formats do not match local construction practice. Automation level is selectable, so a buyer can start with semi-automatic pallet handling and add automatic stacking later without replacing the press. Documentation includes a line layout with capacity calculations that state which block format each output figure assumes, eliminating guesswork during plant planning.
Documentation & Verification
- Line layout drawing with capacity calculations per block format for the QT10-15
- Hydraulic and electrical schematics for local maintenance team reference
- Pallet specification sheet matched to your curing rack dimensions
- Voltage, frequency, and PLC display language confirmation before production
- Factory test record on your target block format before dispatch
- Mould drawing and format list covering all requested block types
Installation, Commissioning & Support
- Foundation plan showing load points for the QT10-15 press and supporting stations
- Power supply requirements confirmed for voltage and frequency at your site
- Line stations dismantled for container loading with reassembly sequence documented
- On-site commissioning with cycle time verification per block format
- Operator training covering PLC controls, mould change, and daily maintenance routines
- Wear parts and mould inventory list with reorder specifications provided at handover
What to Include in Your Inquiry
Provide your target block formats with dimensions, the daily output you need per format, and the raw materials available locally including aggregate type and grading. Confirm the voltage and frequency at your site, the PLC display language your operators require, and the pallet size that fits your existing curing racks and forklift. If you have an existing mixer or conveyor that will remain in the line, share its specifications so the new stations can be matched to it.
Frequently Asked Questions
Q: How is line capacity verified per block format, and which stations can become bottlenecks?
A: Each output figure in the specification table is tied to a specific block dimension, mould cavity count, and cycle time range. The most common bottleneck is the pallet return conveyor when the curing rack distance is longer than calculated. The mixer batch size and cycle time can also fall behind the press demand if not sized against the highest-output format you plan to run.
Q: How do pallet feeding and stacking stations synchronize with the press cycle time?
A: The PLC control cabinet monitors pallet position sensors and press cycle status simultaneously. A fresh pallet is released only when the press completes its current cycle and the finished layer has cleared the output conveyor. If the stacking station detects a full rack, it signals the PLC to pause the sequence rather than allowing blocks to accumulate on the line.
Q: What supporting equipment is included in the line quotation versus supplied separately?
A: The standard QT10-15 line includes the pallet feed machine, block making machine, storage hopper, conveyor, hydraulic unit, and PLC control cabinet. Raw material batching silos, curing racks, and forklifts are typically supplied by the buyer. If you need stacking or cubing automation, that is configured as an add-on based on your plant layout.
Q: How is the hydraulic station protected from vibration and dust in continuous operation?
A: The independent integrated hydraulic station is mounted separately from the main press frame so that vibration from the mould table does not transmit into the valve block and pump assembly. Enclosures limit cement dust ingress. This separation extends seal life and reduces the frequency of hydraulic fluid contamination during extended production runs.
Q: What is the lead time for line delivery, and how are stations packed for container loading?
A: Lead time depends on mould customization and the automation level selected. Stations are dismantled to fit standard shipping containers, with each component labeled against the reassembly drawing. The packing list and container loading plan are shared before dispatch so your site team can prepare the unloading sequence and foundation in advance.