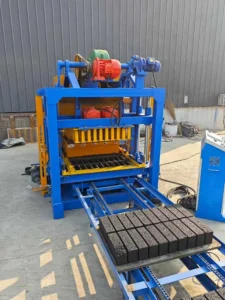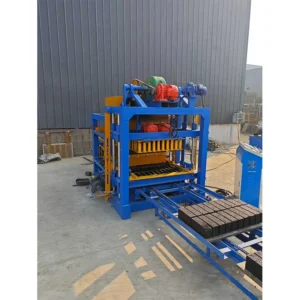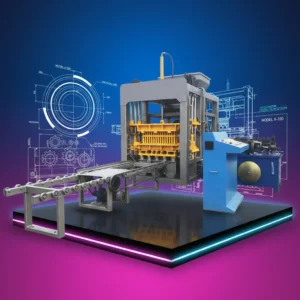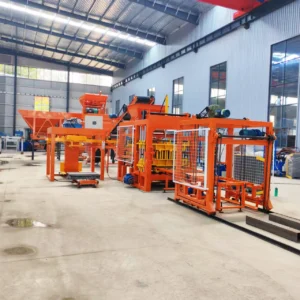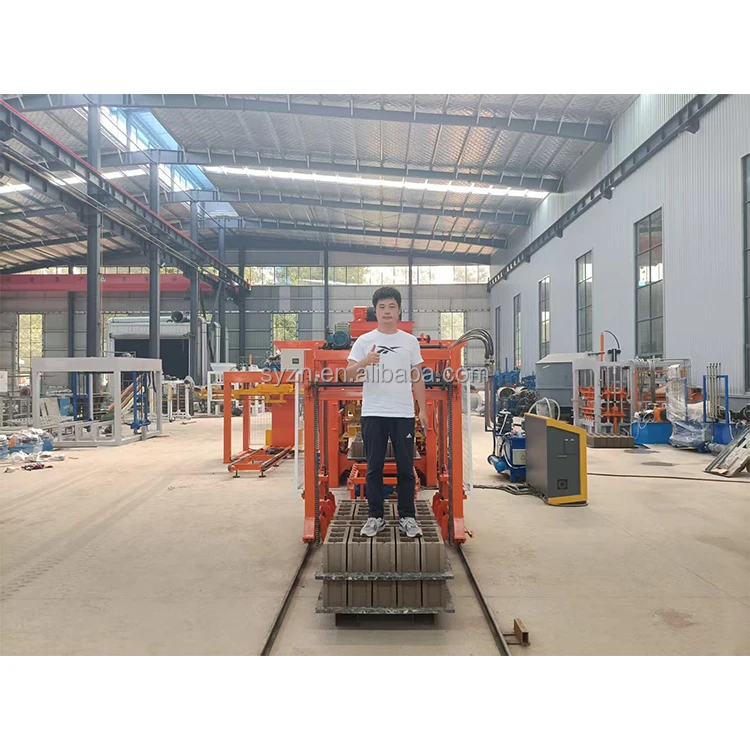
Synchronized Line Cadence — the QT6-15 press cycle, mixer discharge, pallet feed and stacker lift are timed so no station idles while another catches up.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT6-15 |
| Product Type | Automatic Concrete Block Making Machine |
| Rated Power | 31.25 kW |
| Voltage & Frequency | Configured to buyer’s local supply (confirmed before build) |
| Control System | PLC with display language confirmed before production |
| Overall Dimensions (L×W×H) | 7100 × 1500 × 3000 mm |
| Net Weight | 8500 kg |
| Hydraulic Pressure | 16–21 MPa |
| Vibration Form | Platform vibration |
| Moulding Cycle | 15–20 s (basis to be confirmed with target block format and mix) |
| Pallet Size | 850 × 680 mm |
| Output — Hollow Block 400×200×200 mm | 6 pcs/mould, 8640 pcs/day (8-hour shift, basis not stated in source) |
| Output — Porous Block 240×115×90 mm | 14 pcs/mould, 22400 pcs/day (8-hour shift, basis not stated in source) |
| Output — Solid Block 240×115×53 mm | 30 pcs/mould, 54400 pcs/day (8-hour shift, basis not stated in source) |
| Compatible Mould Formats | Hollow, solid, paver, interlocking, curbstone, colored paver |
| Automation Level | Automatic (scope of stacking, pallet feeding and cubing to be confirmed) |
| Raw Materials | Crushed stone, sand, cement, fly ash, gravel, slag, dust |
| Assembly State | Skid-mounted / bolted frame |
| Standards | CE (confirm marking applicability before order) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for masonry walls | Crushed stone and cement with fly ash or slag replacement |
| Solid paver manufacturing for walkways and driveways | Sand, fine aggregate and cement blends |
| Interlocking block production for retaining structures | Coarse aggregate with controlled moisture content |
| Curbstone forming for road and infrastructure projects | Dense aggregate mix requiring higher hydraulic pressure |
| Porous brick runs for permeable paving | Open-graded aggregate with low fines content |
What "Cycles per Hour" Hides About Your Real Daily Tonnage
A press cycle means nothing if the mixer cannot discharge, the pallet feeder runs dry, or the stacker cannot keep pace.
I once watched a block plant owner stare at a press that was theoretically capable of strong output, while upstream the mixer sat idle waiting for aggregate and downstream wet blocks piled on the floor because no one had budgeted for a pallet return conveyor. The automatic block making machine production line had been quoted as a single press figure. The owner paid for a machine but received a bottleneck. Quoted cycle times assume every surrounding station is ready when the press finishes its stroke [NEED_CITE: block plant line balancing principles for concrete products]. When even one supporting station lags, the actual daily volume drops sharply from the number on the quotation.
How the QT6-15 Fits Inside a Coordinated Block Line
The QT6-15 is not sold as an isolated press. It sits at the centre of an automatic block making machine production line where raw material feeding, mixing, pallet circulation, pressing, stacking and curing rack handling are each sized against the same cycle target. When the press completes its 15–20 second moulding window, the pallet must already be in position on the feed table, the mixer must have discharged the next batch into the hopper, and the stacker must have cleared the previous wet block. If any station is undersized, the press waits and real output slips.
Why Pallet Return and Curing Rack Handling Decide Your Actual Shift Output
The press ejects a loaded pallet every cycle. That pallet must travel to a curing rack, be stripped once the block has set, and return to the feed table before the next stroke. On a line where pallet return is manual, two workers spend the entire shift carrying pallets instead of monitoring quality. Specifying the pallet size at 850 × 680 mm against the buyer’s existing curing yard dimensions and forklift capacity means the pallet travels through the full loop without re-handling. Curing rack handling and cubing are therefore not optional extras but the difference between a press that runs and a press that waits [NEED_CITE: curing area sizing for concrete block plants].
Pressure, Vibration and Mix Design — Why All Three Must Agree
Hydraulic pressure between 16 and 21 MPa provides the static compaction force, while platform vibration rearranges particles into a dense packing arrangement. These two forces only produce consistent block strength when they are matched to the actual mix design and local aggregate. A crushed stone blend with high clay content absorbs vibration differently from clean river sand, and the pressure setting that works for one will leave the other under-compacted. Before we confirm a machine build, we ask for the buyer’s aggregate sieve analysis and cement proportion so the vibration amplitude and hydraulic hold time can be set against real material rather than a catalogue default. Pallet size, mould cavity count and cycle length are then locked together so the quoted output reflects the format the buyer actually intends to sell.
The Cost of Skipping the Supporting Equipment Conversation
When a quotation covers only the press, the buyer discovers after delivery that pallet handling, stacking and curing were never included. Workers end up lifting wet blocks by hand, pallets pile up against the machine frame, and the daily tonnage falls far below expectation. Voltage and frequency mismatches compound the problem: the press arrives, the local supply does not match the motor nameplate, and commissioning stalls for weeks while a transformer is sourced [NEED_CITE: electrical supply verification for imported industrial machinery]. These are not minor delays. They are the reason a plant owner loses an entire production season before the first saleable block leaves the yard.
Why Buyers Source This Line Through Shandong Shiyue
Block machinery is our single focus, so the QT6-15 press, its moulds, pallets and handling equipment are specified as one matched system rather than assembled from separate suppliers. Configuration is set against the buyer’s actual mix design, local aggregate and target block format, not a catalogue default. Mould design covers the formats the buyer’s market sells, including custom drawings when a non-standard kerbstone or interlocking profile is required. Automation level is selectable, so a buyer can begin with semi-automatic pallet handling and add stacking and cubing later. Installation and commissioning support includes operator training on the specific PLC language and cycle parameters confirmed before shipment.
Documentation & Verification
- Line layout drawing with capacity calculation stated per block format
- Machine specification sheet with confirmed voltage, frequency and PLC language
- Mould drawing and format list matched to buyer’s product range
- Pallet specification cross-referenced to buyer’s curing yard and forklift
- Hydraulic and electrical schematic for local maintenance teams
- Factory test record showing cycle time achieved with buyer’s target mould installed
Installation, Commissioning & Support
- Foundation plan sized to the QT6-15 footprint of 7100 × 1500 × 3000 mm and 8500 kg static load
- Dedicated power circuit matching the confirmed 31.25 kW draw at buyer’s local voltage and frequency
- Skid-mounted frame with bolted assembly for container loading and on-site re-erection
- First-run parameter setting against buyer’s aggregate and cement proportion
- Operator training on PLC interface in the confirmed display language
- Wear parts and mould list with availability terms documented at order confirmation
Preparing Your Line Enquiry
Tell us the block formats your market demands, the daily volume you need per format, and the local aggregate sieve analysis you can source. Include your site voltage, frequency, available curing yard area, and whether existing forklifts or mixers must integrate with the new line. We use these inputs to return a line layout and capacity calculation tied to your actual product, not a generic cycle figure.
Frequently Asked Questions
Q: How is daily capacity calculated per block format, and what shift length is assumed?
A: The QT6-15 output figures are based on an 8-hour shift, but the moulding cycle varies with block format, mix design and compaction requirement. We calculate daily capacity separately for hollow, porous and solid blocks and state the assumed format in the quotation so the number matches what you actually plan to produce.
Q: Which supporting stations are included in the line quotation?
A: Our line proposal covers raw material feeding, mixing, pallet feeding, the QT6-15 press, automatic stacking and curing rack handling. Each station is sized against the same cycle target so the press is never left waiting for a pallet or a batch of material.
Q: How are pallet size and material matched to my existing curing yard and forklift?
A: We confirm the 850 × 680 mm pallet dimension against your curing rack spacing, yard area and forklift tine width before finalising the order. Using a pallet that matches equipment you already own avoids the cost of replacing racks or buying a different forklift after the line arrives.
Q: What voltage, frequency and PLC language will be set before the line ships?
A: We confirm your local supply voltage, frequency and preferred PLC display language during the quotation stage and lock these into the production build. The factory test then runs the QT6-15 under these exact electrical conditions before the machine is packed for dispatch.
Q: How do we rebalance the line when a new mould format is added later?
A: Each mould format has a different cycle time and pallet load weight. When you add a new format, we recalculate mixer discharge rate, pallet feed interval and stacker cadence against the new cycle so every station stays synchronised and the press maintains its target output.