
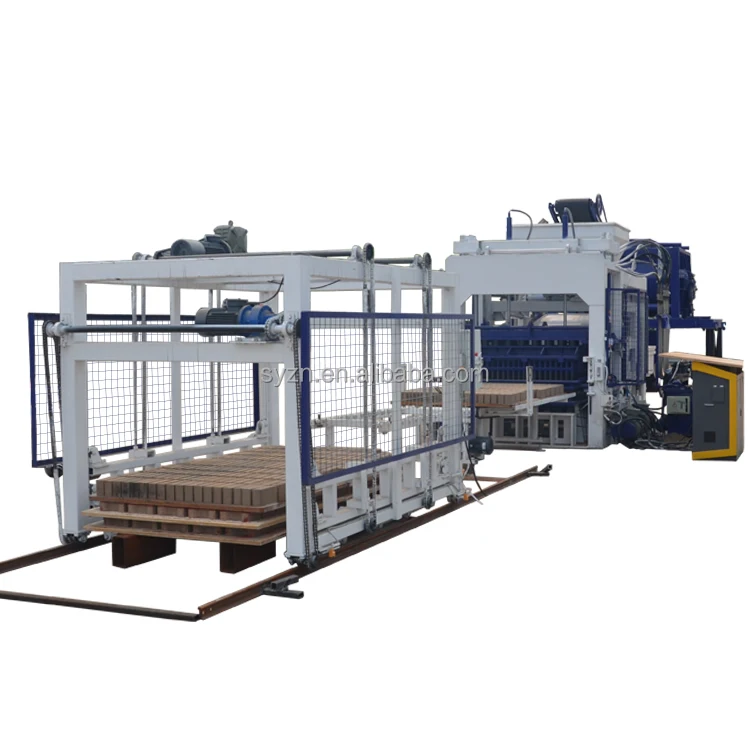
Line-Synchronized Engineering — The QT12-15 block machine production line turnkey configuration treats the press as one node within a coordinated material flow, ensuring mixer discharge, pallet cycling, and stacker lift speeds are timed against the 15–30 second moulding cycle rather than left to chance.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT12-15 |
| Product Type | Hydraulic Block Making Machine |
| Total Power | 62 kW |
| Pallet Size | 1300 × 900 mm |
| Moulding Cycle | 15–30 seconds |
| Vibration Type | Table vibration |
| Vibration Force | 120 kN |
| Voltage | Customized according to local industrial voltage |
| Moulds | All moulds customized according to blocks required |
| Control System | PLC (brand and language options to be confirmed) |
| Hydraulic Pressure | To be confirmed (MPa rating) |
| Automation Level | Configurable from semi-automatic to fully automatic stacking and cubing |
| Overall Dimensions | To be confirmed |
| Net Weight | To be confirmed |
| Mould Change Time | To be confirmed |
| Output Capacity | Dependent on block format (basis to be confirmed) |
| Certification | CE declaration where applicable |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production | Crushed stone, cement, sand, and fly ash blends |
| Solid block production | Dense aggregate mixes for load-bearing walls |
| Paving block production | Fine aggregate face mix with structural backing |
| Kerbstone production | High-density concrete with extended vibration |
| Interlocking brick production | Precision moulds with dry-leaning mix designs |
| Porous brick production | Permeable aggregate gradings for drainage applications |
| Slope protection brick production | Heavy-section moulds with reinforced concrete |
Why "Cycles per Hour" Tells Only Half the Story for Your QT12-15 Block Machine Production Line Turnkey
A press quoted at peak cycle speed means nothing if the mixer cannot refill the hopper before the next mould closes.
When I first started specifying lines, I watched a QT12-15 block machine production line turnkey installation in West Africa sit idle for eight seconds every cycle because the pan mixer discharged too slowly for the press demand. The press itself was rated correctly, but the upstream feed rate had been sized for a smaller machine. The plant owner paid for high-capacity output and received roughly sixty percent of it [NEED_CITE: line synchronization principles for block production]. This is why every station from raw material intake to curing rack handling must be calculated against the same cycle window.
How Upstream and Downstream Stations Match the Press Rhythm
The QT12-15 completes a moulding cycle every 15 to 30 seconds depending on block format and mix stiffness. The batch mixer must discharge a full charge into the press hopper within that window, which means mixer drum capacity, discharge gate size, and conveyor belt speed are all derived from the press cycle — not selected from a catalogue default. The pallet feeder must index a fresh pallet into position and retract before the vibration phase begins, requiring sensor coordination with the PLC sequence.
What Happens When Line Stations Fall Out of Sync
When the stacker lift speed is slower than the press discharge rate, finished blocks accumulate on the roller table and operators begin pulling pallets by hand. This defeats the purpose of the QT12-15 block machine production line turnkey automation investment and introduces pallet damage from rough handling [NEED_CITE: pallet handling damage rates in manual vs automatic stacking]. Downstream curing rack spacing must also match the 1300 × 900 mm pallet footprint — racks designed for a smaller pallet leave overhang that catches forklift tines during retrieval.
Reading the Numbers That Actually Matter
The 62 kW total power rating covers the press hydraulic unit, vibration motor, and control panel but does not include the mixer motor, conveyor drives, or stacker hydraulics. Plant main supply sizing must account for all stations running simultaneously, with a margin for motor starting current. The 120 kN vibration force transmitted through the table determines foundation mass requirements — an undersized concrete pad allows vibration to propagate into adjacent line stations, affecting batching scale accuracy and PLC sensor reliability. The 1300 × 900 mm pallet size drives three decisions at once: curing rack column spacing, forklift tine width, and the total floor area needed for the 28-day curing cycle.
The Cost of Treating the Press as a Standalone Purchase
Buyers who source the press separately from the pallet feeder, stacker, and curing rack handler often discover that the electrical interlocks between stations were never specified. Each supplier assumes the other party wrote the PLC ladder logic for the handoff points. The result is a commissioning delay measured in weeks while a controls engineer rewrites the sequence on site [NEED_CITE: commissioning delays from multi-supplier control integration]. Pallet material choice also causes problems when decided in isolation — bamboo pallets flex differently under vibration than PVC or steel, affecting block dimensional tolerance and requiring different vibration dampening settings.
Why Sourcing the Complete Line from One Specification Point Matters
Shandong Shiyue Intelligent Machinery treats the QT12-15 as part of a matched system rather than a standalone catalogue item. The mixer discharge rate is calculated against the press cycle for the buyer’s specific block format. Pallet material and thickness are selected based on the buyer’s existing curing rack dimensions and forklift capacity, not a default warehouse stock. The PLC display language and voltage frequency are confirmed in writing before the control cabinet is wired, eliminating the on-site rewiring that delays commissioning for many export installations. Factory testing runs the full line — feeder, press, stacker, and pallet return — as one continuous sequence before any station is dismantled for container loading.
Documentation & Verification
- Line layout drawing showing every station from feeder to cubing with cycle time per block format
- Pallet specification sheet confirming 1300 × 900 mm size, material, and load rating matched to site curing racks
- Voltage, frequency, and PLC display language confirmation signed before production begins
- Factory test record covering full line run including pallet return conveyor continuity
- Hydraulic and electrical schematic for every station with interlock logic diagram
- Mould drawing and format list for every block type the buyer intends to produce
Installation, Commissioning & Support
- Foundation design accounts for 120 kN vibration force with isolation pads between press pad and adjacent station footings
- Electrical supply sizing covers the full 62 kW press load plus mixer, conveyor, and stacker motors with starting current margin
- Machine arrives dismantled for container loading with reassembly sequence documented per station
- Commissioning includes PLC sequence verification across all handoff points between feeder, press, and stacker
- Operator training covers mould change procedure, pallet jam clearing, and daily hydraulic fluid level checks
- Wear parts list identifies vibration motor bearings, hydraulic seals, and mould liner plates with replacement intervals
Before You Request a Quotation
To specify a QT12-15 block machine production line turnkey system that actually runs at rated cycle time, we need to know which block formats your market sells, the daily output target per format, and the raw materials available locally including aggregate grading. Share your workshop floor dimensions and ceiling height so the line layout accounts for pallet return conveyor routing and curing rack placement. Confirm your local industrial voltage, frequency, and preferred PLC display language so the control cabinet is wired correctly before dispatch.
Frequently Asked Questions
Q: How are upstream mixer feed rate and downstream stacker speed matched to the QT12-15 moulding cycle?
A: The mixer discharge gate and conveyor belt speed are calculated so a full batch enters the press hopper within the 15–30 second moulding window. The stacker lift cycle is timed so the finished pallet clears the roller table before the next mould opens. Both values are stated on the line layout drawing per block format.
Q: What pallet size and material does the 1300 × 900 mm spec require for my existing facility?
A: The 1300 × 900 mm pallet must fit your curing rack column spacing and forklift tine width. Pallet material — bamboo, PVC, or steel — is selected based on the vibration force transmitted and the block dimensional tolerance required. We confirm rack and forklift compatibility before finalizing the pallet specification.
Q: Which stations are included in the quotation for the complete line?
A: The quotation covers raw material feeding, mixing, pallet feeding, the QT12-15 press, automatic stacking, curing rack handling, and cubing. Each station is listed individually with its cycle time contribution so the buyer can see where capacity is determined. No station is excluded by default.
Q: How is daily output calculated and which block format is it based on?
A: Daily output is stated per block format, not as a single peak figure. A 400 × 200 × 200 mm hollow block has a different cycle time and mould cavity count than a paving block, so the line layout document lists realistic daily production for each format the buyer intends to run.
Q: What electrical load does the full line draw and how should the plant supply be sized?
A: The QT12-15 press draws 62 kW, but total plant load includes the mixer motor, conveyor drives, stacker hydraulics, and lighting. We provide a consolidated electrical load schedule with motor starting current values so the buyer’s electrician can size the main breaker and dedicated circuits before equipment arrives.



