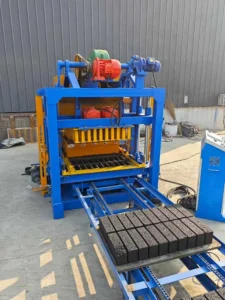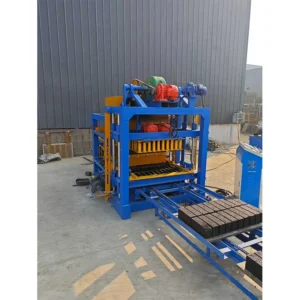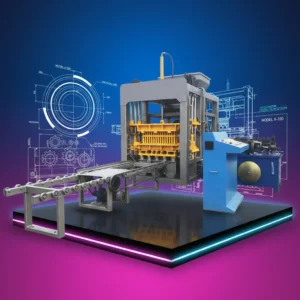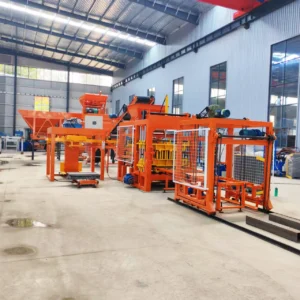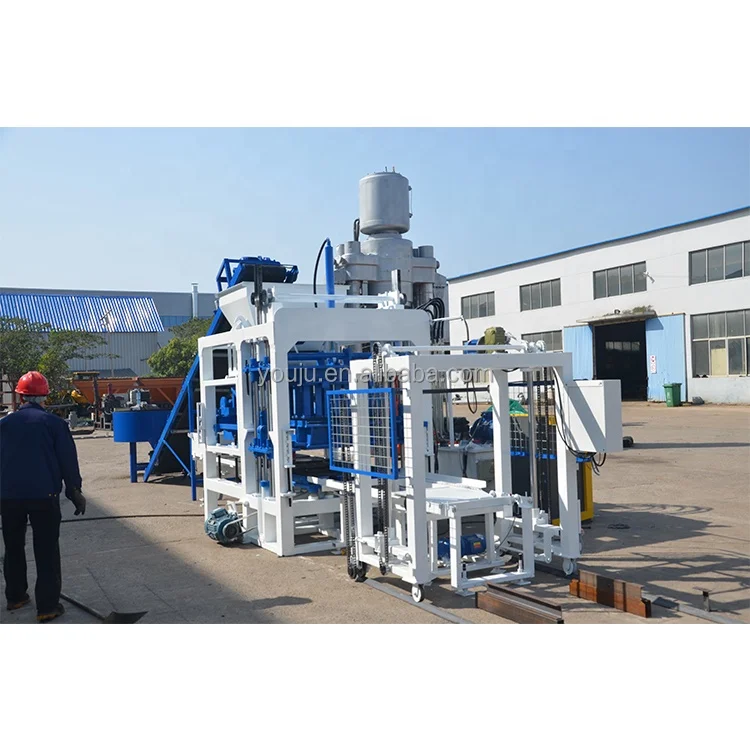
Matched Line Synchronization — Mixer, conveyor and stacker cycle times calculated against the 18–25s press rhythm so upstream and downstream stations never leave the QT4-18 waiting.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT4-18 |
| Product Type | Automatic Concrete Block Making Machine |
| Overall Dimensions | 2500 × 1750 × 2200 mm |
| Rated Pressure | 16 MPa |
| Vibration Form | Platform Vibration |
| Pallet Size | 950 × 550 mm |
| Molding Cycle | 18–25 s (basis to be confirmed per block format) |
| Overall Power | 27.5 kW |
| Control System | PLC control with frequency converter |
| Electrical Components | Schneider brand |
| Mold Lifting Mechanism | Double-sided sync gears |
| Material Feeding System | Hopper, feeding box, feeding platform, conveyor system |
| Block Receiver | Chassis, transport system, idlers with motor, reducer and triangular belt |
| Support Equipment | JQ500 concrete mixer, 8 m belt conveyor (6 m optional), stacker, block gripper, trolley, concrete batching plant |
| Assembly State | Complete line configuration available |
| Standards | CE (where applicable) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production | Crushed stone, sand, cement and fly ash blends |
| Solid block production | Dense aggregate mixes for load-bearing walls |
| Paving block production | High-strength concrete for pedestrian and vehicular surfaces |
| Kerbstone production | Coarse aggregate with cement for roadside profiles |
| Interlocking brick production | Interlocking geometry with locally sourced sand and gravel |
| Porous brick production | Permeable concrete mixes for drainage applications |
| On-site contractor production | Mobile batching with site-available aggregate and cement |
What a "Complete Line" Quotation Often Leaves Out
An automatic block making machine production line is only as fast as its slowest station — and that station is rarely the press itself.
I once configured a fully automatic setup for a client in Jiangsu. The press ran its cycle on time, but the mixer discharged batches slower than the hopper consumed them, and the stacker could not clear cured pallets before the next round arrived. The result was a workshop floor covered in half-cured blocks waiting for manual handling. The rated cycles-per-hour figure assumed every upstream and downstream station kept pace — an assumption that was never stated in the original scope. When stations are sourced separately, the buyer inherits the integration risk [NEED_CITE: common causes of throughput shortfall in block production lines].
Upstream Feeding and Mixing Alignment
The JQ500 mixer and 8 m belt conveyor are specified so that batch discharge volume and transport speed match what the QT4-18 hopper consumes during each 18–25 s molding window. A shorter 6 m conveyor option is available when the raw material storage area sits closer to the press. The concrete batching plant feeds proportioned aggregate and cement into the mixer, keeping the material flow continuous without requiring the operator to stage batches manually.
Downstream Handling and Curing Flow
Once blocks leave the press, the block receiver chassis and transport system carry loaded pallets toward the stacker. The block gripper and trolley move stacked output to the curing area. Each station in this automatic block making machine production line is timed so that the press does not pause while waiting for a cleared pallet or an occupied stacking position. The sequence runs under PLC control with a frequency converter, letting one operator monitor the full loop from the control cabinet.
Reading the Specs That Actually Matter
The 16 MPa rated hydraulic pressure works together with platform vibration to compact the mix into the mould cavity — higher pressure alone does not guarantee block strength if the vibration frequency is mismatched to the aggregate size. The 950 × 550 mm pallet size must align with the curing rack spacing and the forklift tine width the buyer already has on site; choosing a pallet dimension without this check forces a separate equipment purchase. Double-sided sync gears on the mould lifting mechanism keep the mould box level during withdrawal, reducing the risk of corner damage on freshly formed blocks. Schneider electrical components and a PLC with frequency converter give the operator speed control over the feed and vibration stages, which matters when switching between a lightweight porous mix and a dense paving block formula [NEED_CITE: PLC-controlled vibration frequency adjustment in hydraulic block presses].
The Cost of Stations That Do Not Talk to Each Other
When the mixer output exceeds what the conveyor can carry, wet material backs up at the hopper mouth and requires manual clearing — a slowdown that never appears in the press cycle calculation. When the stacker speed is slower than the block receiver discharge, pallets queue on the floor and blocks cure in uncontrolled positions, producing inconsistent strength across the batch. These mismatches are not visible in individual equipment quotations; they only surface once the full line is running under load. Buyers who have experienced this describe it as paying for automatic output and receiving semi-automatic throughput [NEED_CITE: integration failures in multi-station block production setups].
Why Sourcing the Full Line Matters Here
The QT4-18 is specified as one system rather than assembled from separate supplier catalogues — mixer capacity, conveyor length, pallet size, stacker speed and press cycle are all cross-referenced before the quotation is issued. The line layout includes a capacity calculation that names the block format behind the quoted cycle, so the buyer knows exactly which product the throughput figure refers to. Mould options cover hollow, solid, paving, kerbstone, interlocking and porous formats, and custom mould drawings can be built to buyer specifications. Automation level is selectable, allowing a plant to begin with semi-automatic pallet handling and add the stacker and gripper later without replacing the press. Installation includes operator training on the PLC interface and mould changeover sequence, so the line is producing saleable blocks before the commissioning team leaves site.
Documentation & Verification
- Line layout drawing naming the block format assumed for the 18–25 s cycle time
- Machine specification sheet with 27.5 kW power and 16 MPa pressure ratings
- Mould drawing and format list covering hollow, solid, paving, kerbstone, interlocking and porous profiles
- Pallet specification confirming 950 × 550 mm dimensions and material grade
- Hydraulic and electrical schematic with Schneider component references
- Voltage and PLC display language confirmation before production starts
- Factory test record on the buyer’s target block format before dispatch
Installation, Commissioning & Support
- Foundation drawing with cement pour points matching the 2500 × 1750 mm press footprint
- Dedicated power circuit sized for the 27.5 kW total load at confirmed voltage and frequency
- Machine shipped in dismantled modules for container loading and reassembled on site
- PLC control language and frequency converter parameters set during commissioning
- Operator training covering mould change sequence using double-sided sync gears
- Wear parts list for hydraulic seals and mould liners with recommended replacement intervals
What to Share Before Requesting a Quotation
To size the automatic block making machine production line accurately, provide the target block format and dimensions, the daily output you need to hit, and the local aggregate and cement types available. Share your workshop floor area and ceiling height so the conveyor route and stacker reach can be planned around existing structures. Confirm the local voltage and frequency, the PLC display language your operators need, and whether you already have forklifts and curing racks that the pallet size must match.
Frequently Asked Questions
Q: What block format is the 18–25 s molding cycle based on, and how does it change for other formats?
A: The molding cycle range is stated before a specific block format is confirmed. Heavier formats such as large kerbstones typically require longer vibration and pressure hold times, while standard hollow blocks may sit at the shorter end. A capacity calculation naming the exact format will be included with the line proposal so the buyer can see realistic daily output.
Q: How do mixer capacity, conveyor length and stacker speed match the press output?
A: The JQ500 mixer batch volume and discharge rate are calculated against the hopper consumption rate during the press cycle. The 8 m conveyor moves mixed material fast enough to keep the hopper topped up, and the stacker clears cured pallets before the next press cycle deposits new ones. Each station timing is confirmed in the line layout.
Q: What foundation preparation is needed before the line arrives?
A: A reinforced concrete foundation drawing is provided, showing load points for the press, mixer and conveyor supports. The buyer pours the slab and installs anchor bolts before delivery. Power supply must be connected to a dedicated circuit matching the confirmed voltage, and the curing area must be leveled and accessible to the trolley route.
Q: Which voltage and PLC display language options are available?
A: Voltage and frequency are confirmed during the quotation stage to match the buyer’s local grid. The PLC display language is set before the control cabinet leaves the factory, so operators can read prompts and alarms in a familiar language from the first day of commissioning.
Q: What does the mould change procedure involve and how long does it take?
A: The double-sided sync gear mechanism keeps the mould box level during removal and installation, reducing alignment adjustments. A step-by-step sequence is documented for each mould format. The actual changeover time depends on operator familiarity and is covered during on-site training so the team can perform it independently after commissioning.