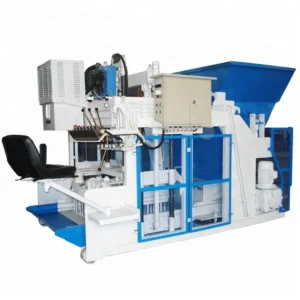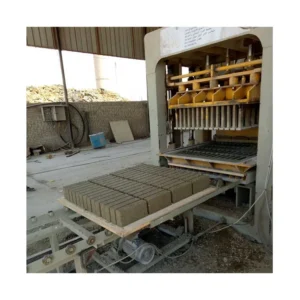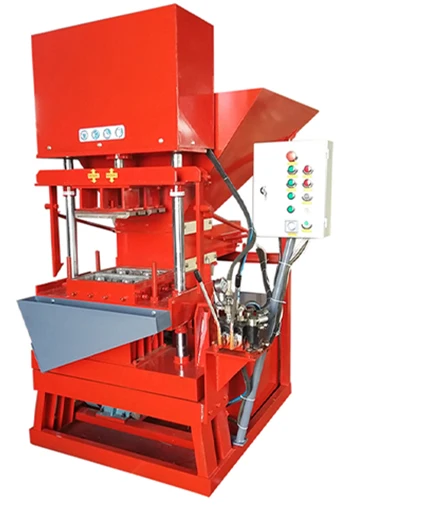
Integrated Line Matching — Every station from the clay feeder through the curing rack is timed against the actual block format you will produce, not a catalogue assumption.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Automatic Compressed Earth Block Making Machine |
| Block Format | Compressed earth / clay ecological brick |
| Power Source | Electric (rated power to be confirmed) |
| Automation Level | Automatic (PLC brand and model to be confirmed) |
| Output Capacity | Basis to be confirmed against block format, mix, and thickness |
| Cycle Time | To be confirmed against specific mould and material test |
| Hydraulic Pressure | To be confirmed against mix design requirement |
| Vibration Force | To be confirmed against target block density |
| Pallet Size | To be confirmed against curing area and handling equipment |
| Mould Format | Earth / clay ecological brick (interchange system to be confirmed) |
| Voltage & Frequency | Configurable to destination grid (to be confirmed before production) |
| Control System | PLC-based (HMI language configurable) |
Application Suitability
| Application | Material or Output |
|---|---|
| Compressed earth block plants | Laterite, clay-soil mixes, and stabilized earth blends |
| Ecological brick production | Low-carbon unfired earth blocks replacing kiln-fired clay bricks |
| On-site housing project factories | Local soil stabilized with cement or lime for walling blocks |
| Existing concrete block lines adding earth formats | Interchangeable mould setups for CEB alongside conventional pavers |
What "Cycles Per Hour" Hides About Your Actual Daily Output
A press rate means nothing if the mixer, feeder, and pallet return cannot keep the same pace.
I have watched automatic compressed earth block making machine production line setups sit idle for seconds between cycles because the pallet feeder was a half-second too slow or the mixer discharged in batches that did not align with the press intake rhythm. The quoted hourly figure assumed a perfect loop that never existed on the shop floor [NEED_CITE: typical cycle loss from station mismatch in block production]. When the soil mix arrives late or the pallets stack up at the return conveyor, the press waits, and your real output drops well below the brochure number. That is why the line layout must be drawn around your specific block dimensions, soil density, and target volume before any station is built.
Synchronizing Every Station Around the Earth-Block Press
The automatic compressed earth block making machine production line only delivers its rated output when every upstream and downstream station matches the press cycle. The raw material feeder must meter stabilized earth into the mixer at a rate that ensures a fresh batch is ready before the press completes its current mould. The pallet feeder must present a clean, cured pallet at the exact moment the press opens, and the stacking system must clear finished blocks before the next cycle begins. Any mismatch creates dead seconds that compound across a shift.
Matching Pallet Circulation to Your Curing Footprint
Pallets are the hidden bottleneck in most earth-block lines. If the curing racks are two hundred meters from the press but the pallet return conveyor only handles a short loop, pallets pile up at the stacking end and the press stalls waiting for an empty board. The pallet size must also match the forks and rack spacing already in your yard, not force you to buy new handling equipment. We specify pallet dimensions and return speed against the distance and layout of your actual curing area so the automatic compressed earth block making machine production line keeps moving without pallets queuing at any point.
Reading the Specs That Actually Shape Your Output
Hydraulic pressure and vibration force together determine whether a compressed earth block reaches the density needed for structural walls or crumbles during curing. High pressure alone compacts the soil but leaves air pockets; vibration alone rearranges particles without bonding them. The two forces must be tuned to your specific laterite or clay-soil blend, which is why we test your material sample before locking in the press settings [NEED_CITE: soil stabilization parameters for compressed earth blocks]. The PLC control manages this tuning by storing recipes for different mixes, so an operator switching from a 6% cement-stabilized blend to a 10% lime-stabilized one only changes a parameter set rather than manually adjusting valves. Voltage and frequency must be confirmed against the local grid before the control cabinet is wired, because a 400V machine arriving at a 415V site risks motor burnout on the first day.
The Cost of Skipping Line-Wide Timing
When a buyer orders the press alone and sources the mixer and pallet system separately, each vendor quotes a machine that works on paper but has never run together. The mixer may discharge too fast for the feeder, flooding the hopper. The pallet return may be rated for lighter concrete blocks and bend under the heavier earth-block pallets [NEED_CITE: pallet load ratings for earth versus concrete blocks]. These mismatches surface during commissioning, when every station is already bolted to the floor and rewiring or replacing a conveyor means weeks of lost production.
Why Sourcing the Line as One System Matters Here
We treat the earth-block press, feeder, mixer, pallet handler, and stacking unit as a single timed system, not a bundle of independent machines. The line layout we provide states the assumed block format and cycle time at every station, so you can see where the bottleneck sits before metal is cut. Pallet specifications are matched to your existing curing racks and forklift capacity, not chosen from a default list. Voltage, frequency, and PLC display language are confirmed in writing before the control cabinet is assembled [NEED_CITE: electrical standards for industrial machinery exports]. If your operation starts semi-automatic, the station layout leaves space and wiring provisions for adding automatic stacking or cubing later without rebuilding the line.
Documentation & Verification
- Line layout drawing showing capacity calculation per block format at each station
- Machine and pallet specification sheets issued together as a matched set
- Voltage, frequency, and PLC language confirmation signed before cabinet wiring
- Factory test record measuring cycle times on your soil sample and block dimensions
- Hydraulic and electrical schematics for on-site troubleshooting
Installation, Commissioning & Support
- Foundation plan aligned to the press footprint and vibration isolation requirements
- Dedicated power circuit sized to the confirmed total kW draw of the full line
- Modular station layout allowing staged assembly if site access is limited
- On-site parameter tuning using local soil to validate cycle times against the layout
- Operator training covering PLC recipe changes for different earth-soil blends
- Wear parts list with mould and hydraulic seal interchange procedures
Starting Your Line Specification
To build a line layout that reflects your real output, we need the block format and dimensions you plan to produce, the daily volume target, and a soil sample or lab report from your site. Share the voltage and frequency available at your plant, the curing area dimensions, and the forklift or pallet jack models already in use so we can match pallet circulation from day one.
Frequently Asked Questions
Q: How is the line capacity calculated for my specific earth-block format?
A: We run your soil sample through the press at the target block dimensions and measure the actual cycle time, then multiply by the number of working hours. The layout states this format-specific capacity at each station so you can verify that feeder, mixer, and stacking speed all match the press rhythm.
Q: How do you match pallet size to my existing curing area?
A: We take the dimensions of your current curing racks, the aisle width, and the forklift fork spacing, then select a pallet that fits all three. The pallet return conveyor length is set against the distance between your press and the curing yard to prevent queuing.
Q: Can I start with semi-automatic operation and add automation later?
A: Yes. The station layout reserves physical space and wiring conduits for automatic stacking and cubing modules. When you are ready to add them, the existing PLC accepts the new I/O without a full control cabinet replacement.
Q: How are voltage and PLC language confirmed before the machine ships?
A: We send a written confirmation form listing your site voltage, frequency, and the required HMI display language. The control cabinet is only wired after you sign off, and the factory test runs at that confirmed voltage.
Q: What happens if my local soil differs from the test sample?
A: The PLC stores multiple mix recipes, so operators can adjust pressure, vibration duration, and cycle timing on-site. We include a parameter adjustment guide tied to common soil variables like moisture content and clay-to-sand ratio.