
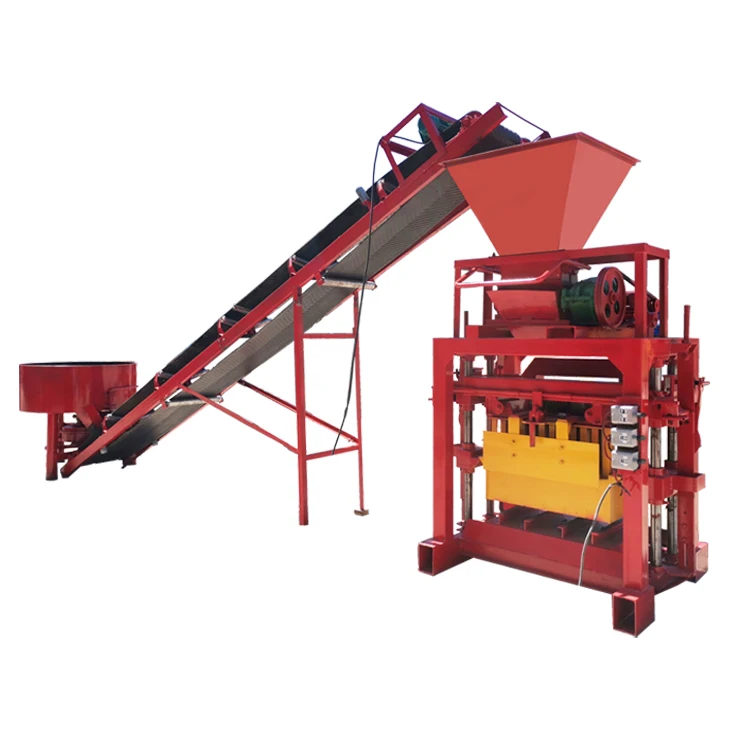
Single-focus block line design — every station from raw material feeding through curing is specified against the QTJ4-35’s actual cycle tempo so the press never waits on upstream or downstream bottlenecks.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QTJ4-35 |
| Product Type | Mechanical Block Making Machine |
| Overall Dimensions | 2050 x 1660 x 1900 mm |
| Main Vibration Form | Motor Vibration |
| Vibration Force | 35 kN |
| Overall Power | 9.8 kW |
| Pallet Size | 850 x 450 x 20 mm |
| Molding Cycle | 35–50 s (varies by block format) |
| Mould Compression | Upper mould and bottom mould compression |
| Automation Level | Semi-automatic / Mechanical manual |
| Hydraulic Pressure | Not applicable (mechanical vibration type) |
| Stacking Method | Manual pallet handling |
| Production Capacity (400x200x200 mm hollow block) | 4 pcs/mould, 360–408 pcs/h, 2880–3264 pcs/8 hr |
| Production Capacity (400x150x200 mm hollow block) | 5 pcs/mould, 360–510 pcs/h, 2880–4080 pcs/8 hr |
| Production Capacity (240x115x53 mm solid brick) | 21 pcs/mould, 1512–1890 pcs/h, 12096–15120 pcs/8 hr |
| Production Capacity (200x100x60 mm paver) | 14 pcs/mould, 1008–1260 pcs/h, 8064–10080 pcs/8 hr |
| Production Capacity (225×112.5×60 mm interlocking brick) | 9 pcs/mould, 648–810 pcs/h, 5184–6480 pcs/8 hr |
| Voltage & Frequency | Configurable to target market electrical standard (basis to be confirmed) |
| Control System | Relay-based or PLC option (basis to be confirmed) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production | Crushed stone, sand, cement and fly ash blends for load-bearing and partition walls |
| Solid brick production | Fine aggregate and cement mixes for masonry and infill |
| Paving block production | High-strength concrete mixes with graded aggregate for pedestrian and light-traffic surfaces |
| Interlocking brick production | Cement-stabilised soil or sand-cement blends for slope protection and retaining walls |
| On-site contractor production | Locally sourced aggregate and cement for project-specific block formats |
| Small to medium plant setup | Multi-format output from a single press station within a compact block machine production line |
Why the Block Machine Production Line Stops at the Press
A press rated at 408 hollow blocks per hour means nothing if the mixer cannot feed it or the pallets run out before the curing rack fills.
I once watched a semi-automatic line in Brazil sit idle for twenty minutes every hour because the batching hopper discharged slower than the QTJ4-35 consumed material. The press itself never faulted; the upstream station simply could not sustain a 35-second cycle. Downstream, the buyer had ordered only fifty pallets, so the line stopped every time those pallets filled the curing area and had to be carried back by hand. Nobody had calculated how many pallets an eight-hour shift actually requires when each block needs twenty-four hours of curing. That gap between press capacity and line throughput is where most block machine production line projects lose their daily output [NEED_CITE: typical block curing duration and pallet circulation requirements].
Upstream Feeding and Mixing Must Match the Press Tempo
The QTJ4-35 completes a moulding cycle every 35 to 50 seconds depending on block format, which means the mixer must deliver a fresh batch of concrete within that same window. A pan mixer with a discharge time longer than the press cycle creates a bottleneck that no amount of automation downstream can fix. Raw material feeding — whether by belt conveyor or skip hoist — must also be sized so that aggregate and cement reach the mixer without queuing. When we lay out a block machine production line, we calculate each station’s throughput against the slowest format the buyer plans to run, not the fastest one in the catalogue.
Downstream Pallet Circulation and Curing Area Sizing
Each pallet leaving the QTJ4-35 carries a freshly pressed block that typically needs twenty-four hours of curing before the pallet can return to the press. At a cycle of 35 seconds and four hollow blocks per pallet, a single shift consumes a large number of pallets in continuous rotation. If the curing area is too small or the forklift cannot stack pallets at the pace the press ejects them, the line stalls. The pallet size of 850 x 450 x 20 mm was chosen to match standard curing rack dimensions and common warehouse forklift tine spacing, but the buyer’s existing equipment must still be verified before the line is finalised [NEED_CITE: pallet circulation calculation methods for concrete block plants].
Reading the Specifications Through a Line-Integration Lens
The 9.8 kW overall power rating covers the vibration motor and mould compression drive on the QTJ4-35 itself. When you add a mixer, conveyor, and any pallet return system, the total connected load rises, and the workshop’s main distribution board must accommodate the combined inrush current. The vibration force of 35 kN with upper and lower mould compression is a mechanical system — no hydraulic station to maintain — which simplifies the utility supply to electrical power alone. The moulding cycle range of 35 to 50 seconds tells you the line’s base tempo: every upstream and downstream station must be capable of sustaining the shorter end of that range, because the buyer will inevitably want to run the fastest format the market demands. Pallet specification at 850 x 450 x 20 mm affects not only the press but also the curing rack slot width, the forklift tine length, and the pallet return conveyor geometry.
The Hidden Cost of Ignoring Line-Level Station Matching
When a buyer prices only the press and sources the mixer, conveyor, and pallets separately, the cycle times rarely align. A mixer that discharges in ninety seconds against a thirty-five-second press cycle cuts actual output roughly in half. Pallets bought at the wrong thickness jam in the press guides, and undersized curing racks force the operator to stop the line and carry blocks by hand. I have seen lines where the block machine production line quotation looked competitive until the buyer added the missing stations after delivery, and the total cost exceeded a properly specified complete line [NEED_CITE: common cost overruns in partial block line procurement].
Why Specifying the Whole Line from One Source Matters
Block machinery is our single focus, so the QTJ4-35 is never quoted as an isolated press. We configure raw material feeding, mixing, pallet supply, and curing rack handling as one matched system, calculating each station’s throughput against the buyer’s chosen block format and local aggregate. Mould design is included for the formats the buyer’s market actually sells, with custom drawings available when standard moulds do not cover a local size. Automation level is selectable — a buyer can start with mechanical manual pallet handling on the QTJ4-35 and add automatic stacking later without replacing the press. Factory testing covers the full cycle sequence, not just the press in isolation, so upstream and downstream timing is verified before the container is loaded.
Documentation & Verification
- Line layout and capacity calculation stating the block format assumed for each station’s throughput
- Pallet specification sheet covering size, material, and quantity required for continuous QTJ4-35 operation
- Voltage and control language confirmation for the entire line before production begins
- Factory test record demonstrating full cycle sequence across all stations
- Hydraulic and electrical schematic showing how the press connects to mixer, feeder, and stacking equipment
- Operation and maintenance manual covering the QTJ4-35 and all supporting stations
Installation, Commissioning & Support
- Workshop floor must accommodate the QTJ4-35 footprint of 2050 x 1660 mm plus clearance for pallet circulation and mixer placement
- Dedicated electrical circuit sized for the 9.8 kW press plus all upstream and downstream station loads
- Machine ships partially dismantled for container loading; reassembly includes press, mixer, and conveyor alignment
- First-run commissioning verifies cycle timing between mixer discharge, press moulding, and pallet return
- Operator training covers mould change procedure, pallet handling, and daily vibration motor inspection
- Wear parts list identifies vibration motor brushes and mould liner plates with replacement intervals
What to Include in Your Inquiry
Send us the block formats you sell today and the ones you plan to add, along with your target daily output per format. We also need your workshop dimensions, existing forklift specifications, and the voltage and frequency at your site. If you already have a mixer or conveyor in place, share the model and capacity so we can verify cycle-time compatibility with the QTJ4-35 before we propose the block machine production line layout.
Frequently Asked Questions
Q: How is line capacity verified per block format across all stations?
A: We calculate each station’s throughput — mixer batch size, conveyor speed, pallet return rate — against the QTJ4-35’s moulding cycle for every format you plan to run. The slowest station determines the line’s real daily output, and we state that number in the capacity document rather than quoting only the press’s theoretical rate.
Q: How do pallet choices affect the curing area and forklift across the line?
A: The QTJ4-35 uses 850 x 450 x 20 mm pallets. Your curing rack slots must accept that width, and your forklift tines must support the loaded pallet length. We verify both before finalising the pallet quantity, which is calculated from your press cycle and the curing duration your local climate requires.
Q: What upstream and downstream speeds must match the 35–50 s cycle?
A: The mixer must discharge a full batch within the shortest cycle time you intend to run. The pallet return system — whether manual or powered — must deliver a clean pallet to the press before the next moulding stroke. Any station slower than the press becomes the line’s actual bottleneck.
Q: How are voltage, frequency, and control language confirmed for the whole line?
A: Before production starts, we confirm the electrical standard and preferred control language for every motor and panel on the line, not just the QTJ4-35. This prevents delays during on-site commissioning when the mixer or conveyor control does not match the local supply or the operator’s language.
Q: What supporting equipment is included in the line quotation?
A: Our quotation covers the QTJ4-35 press, moulds, pallets, raw material feeder, mixer, pallet return system, and curing rack handling as one package. Items the buyer typically supplies — such as the workshop building, foundation, main electrical incoming panel, and forklift — are listed separately so there are no surprises after delivery.



