
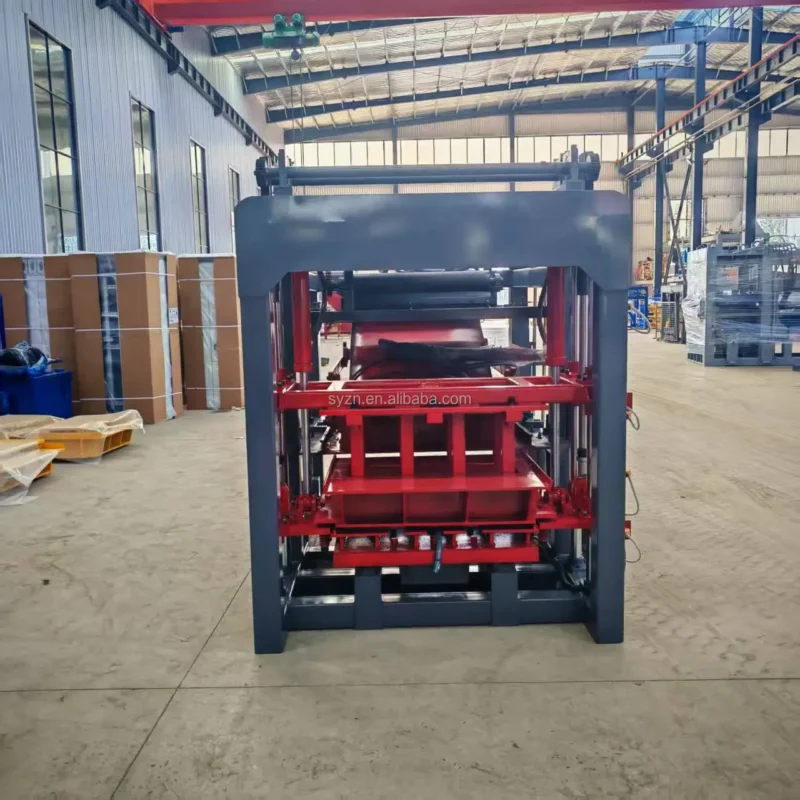
Matched System Configuration — Every station around the QT4-15A block machine production line turnkey is timed to the press cycle, not sourced as standalone units.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT4-15A |
| Product Type | Fully Automatic Concrete Brick Making Machine |
| Overall Dimensions | 4100×1600×2600 mm |
| Rated Pressure | 16–21 MPa |
| Main Vibration Form | Platform Vibration |
| Vibration Frequency | 4200 r/min |
| Vibration Force | 55 kN |
| Pallet Size | 880×550 mm |
| Molding Cycle | 25–30 s (basis not stated in source — confirm block format / material / thickness) |
| Overall Power | 18.45 kW (source value — verify against manufacturer catalog) |
| Total Mass | 4 T |
| Demolding Method | Hydraulic |
| Factory Area Required | 300 m² |
| Automation Level | Fully automatic |
| Applied Products | Concrete blocks, hollow/solid blocks, pavers, interlocking blocks, curbstone, colored pavers |
| Raw Material Compatibility | Crushed stone, sand, cement, dust, fly ash, gravel, slag |
| Loading | 1×40HQ container (basic equipment) |
| Warranty | 1 year (excluding spare parts) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for building walls | Crushed stone, sand, cement, fly ash blends |
| Solid block manufacturing for load-bearing structures | Gravel, sand, cement with local aggregate |
| Paving block and colored paver runs | Fine aggregate, cement, pigment additives |
| Interlocking brick production for landscaping | Sand, dust, cement mix designs |
| Kerbstone and curb production for roadworks | Coarse aggregate, cement, high-pressure成型 |
| On-site block production for housing projects | Locally sourced gravel, slag, cement |
Why the Supporting Line Matters More Than the Press Alone
A QT4-15A block machine production line turnkey only delivers its rated cycle when every upstream and downstream station keeps pace.
I remember a project where a fully automatic press sat idle for seconds each cycle because the mixer batch time was longer than the molding interval. The buyer had invested in a high-output machine but paired it with an undersized mixer. Daily output dropped well below the calculated figure, and the bottleneck was not the press — it was the station feeding it [NEED_CITE: common bottlenecks in block production lines]. This is why the QT4-15A must be specified alongside its raw material feeding, mixing, pallet handling, stacking, and curing stations as one matched system.
Station-to-Station Cycle Matching Across the Full Line
The 25–30 second molding cycle of the QT4-15A sets the tempo for every other station. The mixer must discharge a fresh batch within that window, the pallet feeder must deliver a clean pallet before the press opens, and the stacker must clear cured blocks before the next wet pallet arrives. When any one of these stations runs slower, the press waits — and the entire QT4-15A block machine production line turnkey loses output proportionally. Line layout planning starts with the press cycle and works outward to each supporting station, calculating buffer times and travel distances for pallets and raw materials.
Pallet Handling and Curing Area Integration
The 880×550 mm pallet size on the QT4-15A is not an isolated choice. It determines the spacing of curing rack shelves, the fork dimensions of the handling forklift, and the footprint of the wet-side stacking station. If a buyer already operates curing racks built for a different pallet dimension, the entire downstream layout must be reconfigured. The pallet material — whether bamboo, PVC, or steel — also affects weight per loaded pallet, which in turn dictates the load rating of the stacking mechanism and the curing rack structure [NEED_CITE: pallet material selection for concrete block curing]. A mismatched pallet specification creates friction at every station after the press.
Reading the Core Parameters for Line Design
The 16–21 MPa rated pressure and 55 kN vibration force work together to compact the concrete mix into a dense, consistent block. Higher pressure alone does not guarantee strength; the vibration frequency of 4200 r/min distributes the mix evenly across the 880×550 mm mold cavity before full hydraulic pressure engages. Platform vibration, as opposed to mold vibration, transfers energy through the pallet, which means the pallet must be rigid enough to transmit force without absorbing it. The 300 m² factory area requirement covers the full line footprint — raw material bins, mixer, press, pallet return conveyor, stacking station, and curing racks — not the press in isolation. The 4-ton total mass reflects a machine built with sufficient frame weight to dampen vibration during high-frequency cycles, reducing wear on hydraulic seals and mold mounts over extended production runs.
The Hidden Cost of Underspecifying Downstream Stations
When a quotation covers only the press and omits pallet handling, stacking, and curing equipment, the buyer ends up moving wet blocks by hand. Labor costs rise, breakage increases, and the actual daily output never reaches what the press cycle alone would suggest. I have seen plants where operators carried loaded pallets to curing racks one at a time, turning a fully automatic press into a semi-manual operation [NEED_CITE: labor costs in manual vs automatic block handling]. The QT4-15A block machine production line turnkey avoids this by specifying every station from raw material feeding through to cubed and stacked output, so the automation level the buyer pays for is the automation level the plant actually runs.
Why Source the Full Line From One Configuration Point
Block machinery as a single focus means the QT4-15A press, molds, pallets, and handling equipment are specified as one matched system rather than assembled from separate suppliers. Configuration is set against the buyer’s actual mix design and local aggregate, not a catalog default. Mold design covers the formats the buyer’s market actually sells, including custom drawings when standard formats do not match local demand. The automation level is selectable, allowing a buyer to start with semi-automatic pallet handling and upgrade to full stacking and cubing as volume grows. Installation support includes operator training on the specific line configuration delivered, and wear parts lists are matched to the exact hydraulic and mold components installed.
Documentation & Verification
- Line layout drawing with capacity calculation stating the block format assumed for cycle time
- Machine specification sheet covering pressure, vibration, and pallet dimensions
- Mold drawing and format list for each block type included in the order
- Pallet specification with material grade and load rating per pallet
- Hydraulic and electrical schematic matching the as-built configuration
- Factory test record on the buyer’s target block format before dispatch
Installation, Commissioning & Support
- 300 m² factory area prepared with level concrete floor matching the full line footprint
- Power supply confirmed for overall plant load including mixer and stacking stations
- Machine arrives dismantled for 40HQ container loading with reassembly on site
- PLC display language and voltage frequency confirmed before production begins
- Operator training covers mold change procedure and pallet feeder adjustment
- Wear parts list provided with hydraulic seal and mold liner replacement intervals
What We Need to Size Your Line Correctly
To configure the QT4-15A block machine production line turnkey for your plant, share your target block formats and the daily volume you need for each. Tell us about your local raw materials — aggregate type, cement grade, and any industrial byproducts like fly ash you plan to use. Confirm your available factory floor area, ceiling height, and existing curing rack dimensions. Let us know your local voltage, frequency, and preferred PLC display language so the control system arrives ready to run.
Frequently Asked Questions
Q: How is the daily output of the QT4-15A calculated, and which block format is assumed?
A: The 25–30 second molding cycle applies to a specific block format, thickness, and mix design. Daily output must be recalculated for each format the buyer intends to produce, because larger or thicker blocks require longer vibration and pressing times. The line layout document states the assumed format so the buyer can verify realistic daily volumes against their production targets before committing.
Q: What supporting equipment stations are included, and where could a bottleneck occur?
A: The full line covers raw material feeding, mixing, pallet feeding, the QT4-15A press, wet-side stacking, and curing rack handling. A bottleneck typically appears where cycle times do not match — most often at the mixer if batch discharge is slower than the press cycle, or at the stacker if pallet clearing takes longer than the interval between press openings.
Q: How should pallet size and material be chosen to match my existing curing racks and forklift?
A: The 880×550 mm pallet size must align with the shelf spacing on your curing racks and the fork width of your handling forklift. Pallet material affects weight and rigidity — steel pallets transmit vibration better but add weight, while bamboo pallets are lighter but may flex under high-pressure cycles. The specification is confirmed against your existing equipment before production.
Q: Can the automation level be upgraded from the QT4-15A base configuration as production volume grows?
A: The line supports a staged upgrade path. A buyer can start with manual pallet handling at the stacking station and add automatic stacking and cubing later as daily volume increases. The PLC control system accommodates additional sensors and actuators, and the pallet return conveyor can be extended to connect new curing rack rows without replacing the press.
Q: What raw material feeding and mixing configuration is recommended for my local aggregate and target block format?
A: The feeder and mixer are sized to match the QT4-15A press cycle and the buyer’s specific mix design. Coarse aggregate requires a different bin gate and mixer blade configuration than fine sand or fly ash blends. The configuration proposal includes batch weights and mixer discharge timing calculated for the buyer’s target block format and local material availability.



