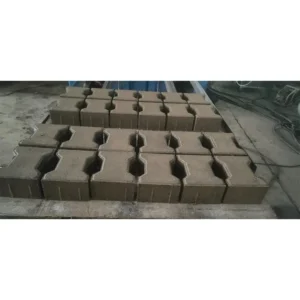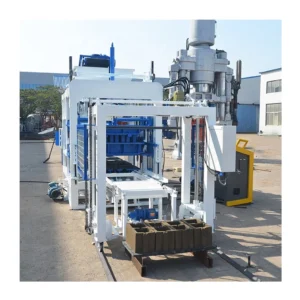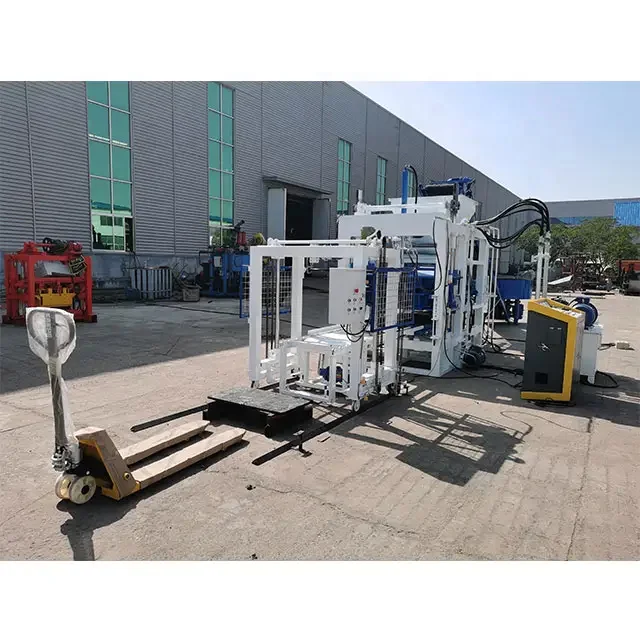
Synchronized Line Design — the QT4-18 press, JQ500 mixer, belt conveyor, stacker and pallet recycle are sized together so the 18–25 s moulding cycle is never starved of material or blocked by downstream pallet handling.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Automatic Concrete Block Making Machine with Supporting Line Equipment |
| Model | QT4-18 |
| Overall Dimensions (L×W×H) | 2500×1750×2200 mm |
| Rated Pressure | 16 MPa |
| Vibration Form | Platform Vibration |
| Pallet Size | 950×550 mm |
| Molding Cycle | 18–25 s |
| Overall Power | 27.5 kW |
| Control System | PLC with frequency converter, Schneider electrical components |
| Mould Lifting Mechanism | Double-sided synchronous gears |
| Material Feeder | Distribution belt hopper |
| Pallet Feeder | Hydro-cylinder driven, automatic |
| Block Receiver | Automatic with conveyor |
| Supporting Mixer | JQ500 concrete pan mixer |
| Belt Conveyor | 8 m (6 m optional) |
| Additional Line Stations | Automatic stacker, block clamper, trolley |
| Optional Equipment | Cement silo, batching plant |
| Mould | One free hollow mould included; extra moulds available and customizable |
| Output Capacity | (basis to be confirmed per block format, material and thickness) |
| CE Declaration | Applicable where required |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production | Crushed stone, sand, cement and fly ash aggregates |
| Solid block production | Dense concrete mix for load-bearing masonry |
| Paving block production | Fine aggregate and cement with colour oxide additive |
| Block plant scaling | Semi-automatic to fully automatic operation with matched upstream and downstream stations |
| On-site construction | Housing or infrastructure projects requiring integrated mixer, conveyor, stacking and curing handling |
Why "Cycles per Hour" Is the Wrong Starting Point
A press quoted at cycles per hour without stating the block format it assumes is the most common reason an automatic block making machine production line falls short of its headline output on the day it starts running.
The only honest capacity figure is the one tied to a specific mould, pallet size and moulding cycle.
I have watched buyers sign off on a number that looked right in the brochure, then discover on commissioning day that their target hollow block takes 25 s per cycle while the quoted rate was based on a thinner paver at 18 s. The difference compounds across a ten-hour shift into hundreds of pallets of lost output. Worse, when the downstream stacker or pallet recycle was not included in the quotation, the press spends a third of its day waiting for a worker to clear the curing rack. [NEED_CITE: mismatch between quoted cycle rate and actual format-based output in block production]
How the Upstream and Downstream Stations Keep Pace
The JQ500 pan mixer and 8 m belt conveyor are selected to deliver fresh concrete to the distribution belt hopper at a rate that matches the 18–25 s press cycle. If the mixer batch arrives late, the press sits idle; if it arrives too early, the mix begins to stiffen in the hopper and block surface quality degrades. Sizing the mixer volume and conveyor speed against the moulding cycle removes both failure modes and keeps the automatic block making machine production line running without operator intervention between the batching station and the press.
Pallet Recycle as the Real Bottleneck
The hydro-cylinder-driven pallet feeder pushes a fresh pallet in and the moulded block out in one stroke. This synchronisation matters because any delay on the demould side cascades back through the press, the conveyor and the stacker. On a line where the pallet recycle is undersized, the press waits for an empty pallet to return from the curing yard, and the daily output drops even though the press itself is capable of the quoted cycle time. [NEED_CITE: pallet recycle speed as limiting factor in automated block lines]
Reading the Specs That Actually Shape Your Line
The 16 MPa rated pressure and platform vibration work together: pressure compacts the mix while vibration settles fine aggregate into the mould cavity. If the local aggregate is coarse or the mix is dry, higher vibration amplitude is needed to achieve the same block density, and the PLC frequency converter allows the operator to adjust vibration force per format rather than running a fixed setting. The 950×550 mm pallet size dictates how many blocks fit per cycle and how the pallets stack on the curing racks the buyer already owns — choosing a pallet dimension that does not match the existing forklift fork width or rack spacing creates handling problems no amount of press speed can fix. Double-sided synchronous gears keep upper and lower mould halves aligned across every cycle, which is what maintains wall-thickness consistency from the first block of the shift to the last.
The Hidden Cost of an Underspecified Line
When pallet handling, stacking and curing are left out of the quotation, the buyer fills the gap with manual labour. Two or three workers assigned to pallet recycle and stacking add a recurring wage cost that compounds over the life of the machine, and human-paced handling cannot keep up with the press during peak cycles. The result is a line that runs below its mechanical capacity every hour of every shift. [NEED_CITE: manual pallet handling reducing effective line throughput in block plants]
Why the Line Is Specified Here, Not Assembled Elsewhere
Every station — mixer, conveyor, press, stacker, clamper and trolley — is selected as one matched set rather than sourced from separate suppliers and bolted together on site. The pallet size, mould format and automation level are confirmed against the buyer’s actual curing area, forklift and target block before the quotation is issued. Mould design covers the formats the buyer’s market sells, including custom drawings when a standard mould does not fit. The automation level is selectable: a buyer can start with the hydro-cylinder pallet feeder and add the automatic stacker later without replacing the press. Installation support includes operator training on the PLC interface, and wear parts and mould replacements remain available after the first production run.
Documentation & Verification
- Line layout drawing showing mixer, press, conveyor, stacker and pallet recycle positions with foundation plan
- Capacity calculation stated per block format with the moulding cycle and pallet size the figure assumes
- Voltage, frequency and PLC display language confirmed in writing before production begins
- Mould drawing and format list included so the buyer knows exactly which blocks can be produced
- Factory test record on the buyer’s target block format before dispatch
- Hydraulic and electrical schematics with Schneider component references for on-site troubleshooting
Installation, Commissioning & Support
- Foundation plan sized to the 2500×1750 mm footprint and 27.5 kW total load of the QT4-18 line
- Dedicated circuit with confirmed voltage and frequency matching the PLC and frequency converter
- Machine shipped in dismantled sections with reassembly supervised during on-site commissioning
- PLC parameters and vibration settings tuned to the buyer’s local mix design on first production run
- Operator training covers mould change, pallet feeder timing and stacker sequence
- Wear parts list and mould replacement schedule provided with spare hydraulic seal kit
What to Prepare Before Requesting a Quotation
Send the target block format with dimensions, the daily output required and the local aggregate available so the mix design can be matched to the press. Confirm the voltage and frequency at the site, the language needed for the PLC display, and the dimensions of the curing yard so the pallet recycle layout fits the space. If there is an existing mixer or conveyor, note its model and throughput so the line can be planned around it rather than duplicating equipment.
Frequently Asked Questions
Q: How is daily output calculated for my target block format?
A: We calculate output per block format using the moulding cycle, pallet size and number of cavities in the mould for that format. The capacity sheet states the exact cycle time and pallet dimension assumed, so you can verify the figure against your shift length before placing the order.
Q: Which supporting stations are included and which are optional?
A: The quotation includes the JQ500 pan mixer, belt conveyor, hydro-cylinder pallet feeder, automatic block receiver, stacker, clamper and trolley. The cement silo and batching plant are optional and can be added to the line layout if your site does not already have them.
Q: How do upstream and downstream cycle times match the press?
A: The mixer batch volume and conveyor speed are set so fresh concrete reaches the hopper within the 18–25 s moulding window. The pallet feeder and stacker are timed to the demould stroke so the press is never left waiting for an empty pallet or a clear conveyor path.
Q: What voltage, frequency and PLC language will my machine use?
A: These are confirmed in writing before production. The PLC display language is set to your operator’s preference, and the electrical components are matched to your site’s supply so commissioning is not delayed on arrival.
Q: How is the line layout adapted to my available floor area?
A: The line layout drawing arranges the mixer, conveyor, press, stacker and pallet recycle to fit your building footprint and curing yard. The foundation plan is included so civil work can begin before the machine arrives.