
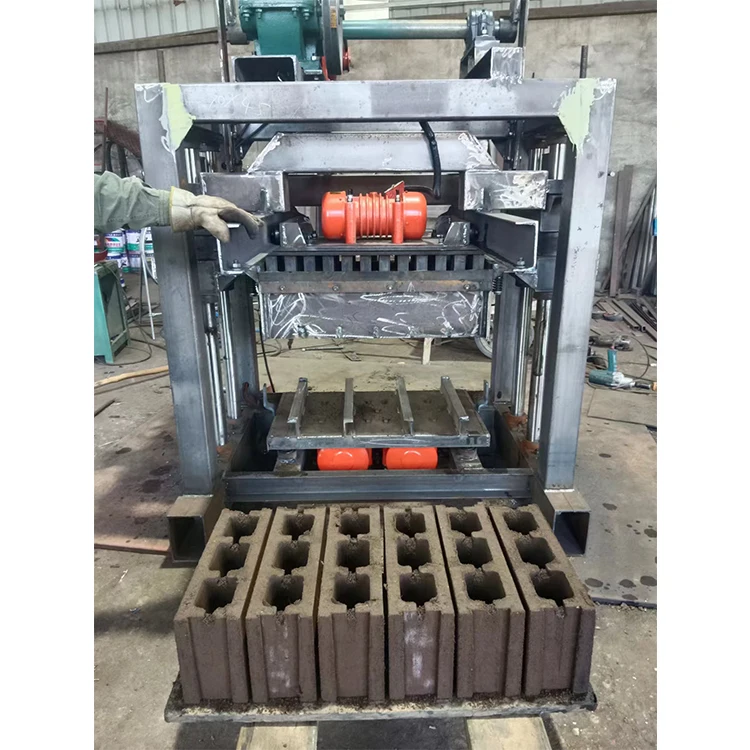
QTJ4-40 Semi-Automatic Block Machine | Production Line
Pallet and Press Integration — The QTJ4-40 block production line QTJ4-40 is engineered so the press, pallet feed, and curing stations share one cycle rhythm, eliminating the idle gaps that typically strand a small plant’s output.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QTJ4-40 |
| Product Type | Semi-Automatic Concrete Block Making Machine |
| Machine Power | 10.4 kW |
| Molding Cycle | 40 s |
| Output Capacity | 2000–2500 pcs/8h (basis not stated in source) |
| Theoretical Productivity (400×200×200mm hollow, 4 pcs/mould) | 360 pcs/h, 2800 pcs/day |
| Theoretical Productivity (400×150×200mm block, 5 pcs/mould) | 450 pcs/h, 3600 pcs/day |
| Theoretical Productivity (225×112.5×60mm interlocking, 9 pcs/mould) | 800 pcs/h, 6400 pcs/day |
| Vibration System | Bed mould vertical + upper mould compression |
| Mould Operation | Top die push-pull with automatic scraper |
| Pallet Size | 850 × 450 mm |
| Overall Dimensions (L×W×H) | 1350 × 1460 × 1800 mm |
| Machine Weight | 1 T |
| Automation Level | Semi-automatic |
| Voltage | Configurable to local supply |
| CE Declaration | Available where applicable |
Application Suitability
| Application | Material or Output |
|---|---|
| Small-to-medium hollow block production | Concrete with crushed stone and cement |
| Solid block manufacturing for load-bearing walls | Sand-cement mixes with fly ash addition |
| Interlocking paver and kerbstone runs | Fine aggregate blends with gypsum or lime |
| On-site block pressing for housing projects | Locally sourced sand and cement with variable grading |
| First-line plant for entrepreneurs | Concrete, sand, cement, fly ash, lime, gypsum combinations |
What "2000 Pieces per Day" Leaves Out About Line Planning
Daily throughput only matters when every station around the press is timed to the same cycle.
I have watched small block plants in South Asia and East Africa stall because the mixer batch size was calculated for one mould format while the press was running another. The QTJ4-40 semi-automatic block machine completes a cycle every 40 seconds, so upstream mixing, pallet feeding, and downstream stacking must all synchronize to that rhythm. When one station lags, the press sits idle and the quoted capacity becomes a ceiling nobody reaches [NEED_CITE: block plant line synchronization principles]. A production line that treats the press as an island will always underperform its own datasheet.
Matching Mixer Batch Size to the 40-Second Press Cycle
Every block production line QTJ4-40 installation starts with the mixer. A 40-second moulding cycle means roughly 90 cycles per hour on a single format. If the mixer discharges less material than one cycle consumes, the press waits. If it discharges more, wet concrete hardens in the hopper. The mixer capacity, discharge rate, and conveyor length must be calculated against the exact block format the buyer intends to run first, then rechecked when moulds change.
Pallet Feed Rate and Downstream Curing Alignment
The 850 × 450 mm pallet size on this machine is not arbitrary. It dictates curing rack spacing, forklift tine width, and the number of pallets needed to keep a full shift running without cycling back to the press too early. When pallet dimensions are chosen without checking the buyer’s existing racks and handling equipment, freshly pressed blocks end up stacked on the ground, losing moisture and strength before they ever reach the curing area [NEED_CITE: concrete block curing rack dimension standards].
Where the Semi-Automatic Boundary Sits
Semi-automatic means the press cycles on its own — vibration, compression, scraper — while an operator places and removes pallets by hand. This keeps the labour count low without the capital outlay of a full automatic stacker. For a first block plant or a second line added beside an existing one, it is the boundary where manual effort stops and mechanical repeatability begins.
Vibration Force, Hydraulic Pressure, and Real Block Density
The QTJ4-40 pairs bed mould vertical vibration with upper mould compression. These two forces must match the buyer’s actual mix design — the aggregate size, cement ratio, and moisture content available locally. A machine tuned for graded river sand will produce crumbly blocks when fed the weathered laterite common in parts of West Africa, and no amount of vibration adjustment compensates for a mix the press was never configured to handle [NEED_CITE: concrete block density and vibration force correlation]. The 10.4 kW motor delivers enough force for standard hollow and solid formats, but the mould cavity depth and vibration duration need to be set against the specific block the buyer’s market actually buys.
The Hidden Cost of Skipping Line Integration
When supporting equipment is sourced from separate suppliers without cycle-time matching, the result is predictable: the mixer floods the hopper, the pallet feeder jams because the spacing is off by millimetres, and the operator spends half the shift clearing blockages instead of pressing blocks. A semi-automatic block machine supporting equipment package that was never tested as one system will always leak time at every junction between stations [NEED_CITE: production line integration failure modes in block plants].
Why Procurement Through a Single Line Supplier Matters
- Machine, mould, pallet, and handling equipment specified as one matched system, not assembled from separate quotations.
- Configuration set against the buyer’s local aggregate and target block format before production begins.
- Pallet size confirmed against the buyer’s existing curing racks and forklifts, not pulled from a default catalogue.
- Voltage, frequency, and PLC language confirmed before dispatch to prevent commissioning delays on arrival.
- Mould and wear parts listed at order stage so the first replacement does not become a sourcing crisis.
Documentation & Verification
- Line layout drawing with cycle-time matching at each station connection point
- Capacity calculation sheet stating output per block format, not a single aggregate figure
- Pallet specification matched to buyer’s curing rack dimensions and forklift type
- Voltage, frequency, and control language written confirmation before production
- Factory test record on the buyer’s target block format before container loading
Installation, Commissioning & Support
- Foundation pad sized to the 1350 × 1460 mm footprint with vibration isolation allowance
- Dedicated electrical circuit rated for the 10.4 kW motor plus mixer and conveyor draw
- Machine shipped as a single unit with pallet feeder and supporting equipment dismantled for container loading
- On-site commissioning includes cycle-time verification between press, mixer discharge, and pallet feed
- Operator training covers mould change procedure using the top die push-pull and automatic scraper system
- Wear parts list provided at shipment covering vibration pads, scraper blades, and hydraulic seals
Before You Request a Quotation
Tell us the block format your market buys most — hollow, solid, paver, or interlocking — along with the daily volume you need to sustain. Share your local aggregate type and the voltage and frequency at your site so we can match the motor and controls before production starts. If you already have curing racks and forklifts on site, send the pallet dimensions they accept so the 850 × 450 mm pallet can be confirmed or adjusted to fit your downstream handling.
Frequently Asked Questions
Q: How is daily output calculated, and which block format does each figure assume?
A: Each output figure on this page is tied to a specific block size and mould cavity count. For example, 2800 pieces per day assumes 400×200×200mm hollow blocks at four per mould, while 6400 assumes 225×112.5×60mm interlocking blocks at nine per mould. Always confirm which format the quoted capacity references before comparing machines.
Q: What supporting equipment is needed to keep the QTJ4-40 running without idle time?
A: A mixer with discharge rate matched to the 40-second cycle, a pallet feeder sized for 850 × 450 mm pallets, and enough pallets in rotation to cover pressing, curing, and return travel. Missing any of these stations leaves the press waiting between cycles.
Q: How does pallet size selection affect curing rack layout and forklift compatibility?
A: The 850 × 450 mm pallet dictates rack shelf width and spacing. If your existing racks were built for a different pallet, blocks will not fit or will overhang. Forklift tine width must also clear the pallet length to move full racks without manual repositioning.
Q: Can the line be upgraded from semi-automatic pallet handling to automatic stacking later?
A: Yes. The semi-automatic configuration leaves space in the line layout for an automatic stacker to be added downstream. The upgrade replaces manual pallet removal and stacking while the press, mould, and vibration system remain unchanged.
Q: What voltage, frequency, and control language options are confirmed before shipment?
A: Voltage and frequency are configured to match the buyer’s local grid before production begins. Control panel language is confirmed at the same stage. All three are documented in writing so commissioning is not delayed by electrical or interface mismatches on arrival.



