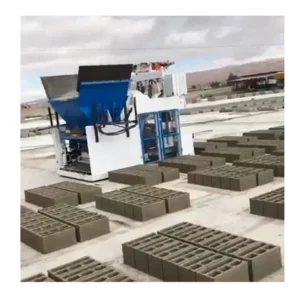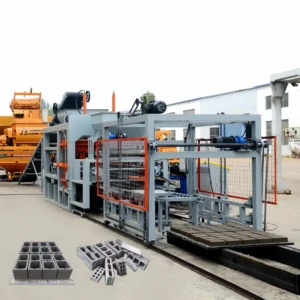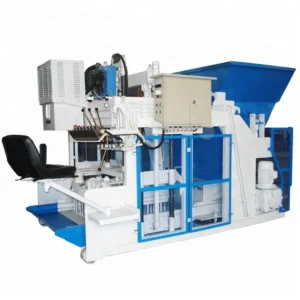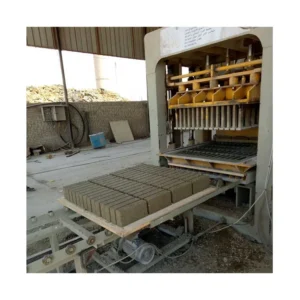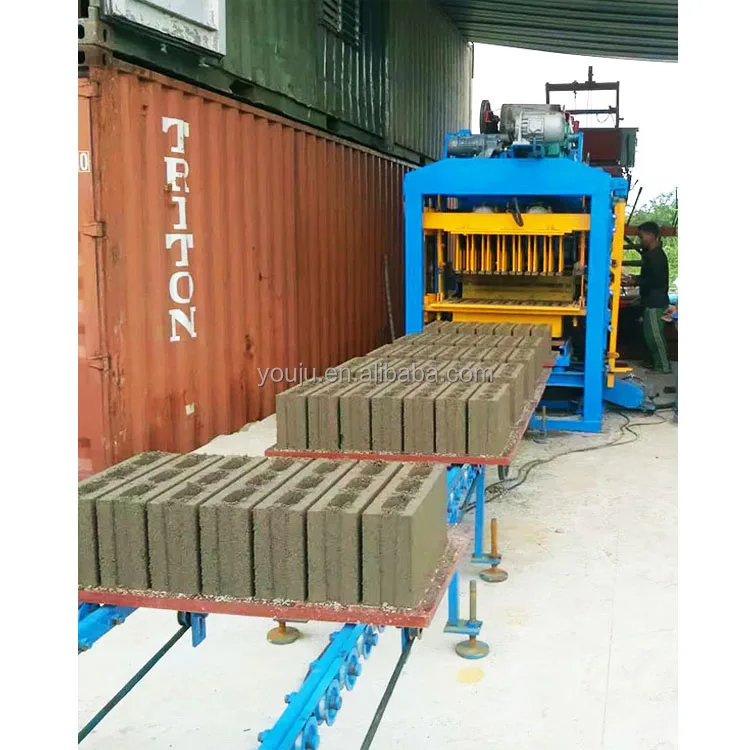
Pallet Handling & Line Flow — Every station around the QTJ4-25 is sized against its 25-second cycle so the press never waits for the next pallet or mix batch.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Semi-Automatic Concrete Block Making Machine |
| Model | QTJ4-25 |
| Overall Dimensions (L×W×H) | 3000 × 1800 × 2680 mm |
| Total Mass | 3.5 T |
| Overall Power | 16.58 kW |
| Vibration Force | 60 kN |
| Main Vibration Form | Platform Vibration |
| Vibration Frequency | 2800–4500 r/min |
| Pallet Size | 850 × 480 mm |
| Molding Cycle | 25 s |
| Demolding Method | Mechanical |
| Guide Column | Four guide columns, overlong guide design |
| Frame Material | National standard manganese steel |
| Surface Treatment | Chrome-plated guide columns |
| Welding | Anti-wear, anti-seismic, anti-moisture technology |
| Output (400×200×200 mm hollow block) | 4 pcs/mould, 580 pcs/h, 4640 pcs/day (8 h) |
| Output (240×115×90 mm porous brick) | 9 pcs/mould, 1400 pcs/h, 11200 pcs/day (8 h) |
| Output (240×115×53 mm standard brick) | 21 pcs/mould, 3300 pcs/h, 26400 pcs/day (8 h) |
| Factory Area Required | 300 m² |
| Control System | Basis to be confirmed (PLC or manual relay) |
| Voltage & Frequency | Basis to be confirmed before order |
| Automation Level | Semi-automatic (mechanical demolding, manual pallet handling implied) |
| Warranty | 1 year (excluding spare parts) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for housing projects | Crushed stone, sand, cement, fly ash |
| Solid brick runs for load-bearing walls | Gravel, slag, cement blends |
| Interlocking paver and colored paver batches | Fine aggregate with pigment additives |
| Porous brick manufacturing | Lightweight aggregate and fly ash mixes |
| Kerbstone and curb production | Coarse aggregate with high cement content |
| On-site block production for contractors | Locally sourced sand, dust, and gravel |
Why Voltage Must Be Settled Before the QTJ4-25 Block Making Machine Production Line Ships
Mismatched voltage is the single most preventable cause of commissioning delays on a block plant site.
I once stood on a job site in Nigeria watching a brand-new machine sit idle for three weeks because the local grid ran at a frequency the control cabinet was never built to handle. The entire panel had to be rewound and re-shipped while the contractor burned through crew wages with nothing to show for it. That same scenario repeats across West Africa and South Asia far more often than manufacturers like to admit [NEED_CITE: voltage and frequency standards by export market]. Confirming the exact voltage, phase, and frequency at your site — and locking in the PLC display language — before the QTJ4-25 block making machine production line enters production removes that risk entirely.
How Each Station Around the Press Connects
A block press is only as productive as the slowest station feeding it. The QTJ4-25 block making machine production line pairs the press with a mixer sized to deliver a fresh batch within the 25-second molding window, a pallet feeder that stages the next board before the press opens, and a curing rack layout planned around the 850 × 480 mm pallet footprint. When any one of those stations falls behind, the press idles and the quoted cycle time becomes meaningless.
Where Line Bottlenecks Typically Appear
Bottlenecks rarely show up in the press itself — they hide in the gaps between stations. If the mixer discharge height does not match the hopper inlet, an operator manually shovels material and the cycle stretches. If pallets are hand-carried from the curing yard instead of fed by a return conveyor, the press waits every third or fourth cycle. On a recent site visit I watched a crew lose nearly half a shift because the pallet stack height did not clear the forklift mast, forcing a re-stack before any boards could reach the feeder [NEED_CITE: pallet handling logistics in small block plants]. Mapping every hand-off point before the line is ordered is the only way to catch these delays on paper rather than on the floor.
Reading the Numbers Behind the Cycle
The 60 kN platform vibration force, delivered through dual motors under the table and an upper mould vibration motor, determines how tightly aggregate particles are packed during each 25-second cycle. Higher compaction density directly translates to block strength, but only when the hydraulic or mechanical pressure and the vibration frequency are tuned to the buyer’s specific mix design. The 850 × 480 mm pallet size sets the curing area footprint — every rack, shelf, and forklift aisle must be planned around that board dimension. Mechanical demolding, driven by the four chrome-plated guide columns, keeps the system running in areas where electrical infrastructure cannot support full servo automation, though it does mean pallets leave the press by hand rather than on a conveyor.
The Hidden Cost of Ignoring Line Integration
Ordering a press on its own and bolting on supporting equipment later almost always costs more than specifying the full line up front. Mismatched mixer output leaves the hopper half-empty, forcing operators to extend the fill portion of each cycle. Pallets ordered without checking the curing yard dimensions arrive in a size that will not stack in the existing racks, pushing the buyer into a second purchase before the first block is cured. And when voltage and control language are left as afterthoughts, the machine may physically arrive but sit powerless until a new panel ships overseas — burning through project timelines that had no slack to begin with [NEED_CITE: CE machinery directive requirements for industrial equipment].
Why This Is Where the Line Gets Specified
Every machine, mould, pallet, and handling station is quoted as one matched system rather than assembled from separate suppliers, so cycle times align across the line. The raw material feed configuration is set against the buyer’s actual local aggregate and mix design, not a catalogue default. Mould formats are chosen for what the buyer’s market actually sells, with custom drawings available for non-standard shapes. Automation level is selectable — a buyer can start with semi-automatic pallet handling and upgrade the stacking end later without replacing the press. Installation support includes operator training on the specific configuration that ships, and spare parts lists cover hydraulic and mould wear items from day one.
Documentation & Verification
- Line layout drawing showing every station and pallet flow path for the QTJ4-25
- Capacity calculation sheet stating the exact block format behind each output figure
- Pallet specification with size, material, and quantity matched to curing area
- Voltage and PLC language confirmation signed off before production begins
- Factory test record on the buyer’s target mould format before dispatch
- Packing photographs and customs documentation support for smooth clearance
Installation, Commissioning & Support
- Foundation pad sized to the 3000 × 1800 mm footprint with vibration isolation
- Dedicated power circuit rated for the 16.58 kW total load at confirmed voltage
- Press arrives partially assembled; guide columns and vibration table bolt on site
- First-run commissioning includes cycle timing and mould alignment verification
- Operator training covers mechanical demolding sequence and pallet return flow
- Wear parts list for guide bushings and mould liners shipped with the machine
- Maintenance schedule tied to vibration motor bearing intervals
What to Share With Your Inquiry
Send the exact block format your market buys most — hollow, solid, paver, or a mix — along with the daily volume target and available factory space. Include your local aggregate types so the feed system can be configured before the quote is finalised. Confirm your site voltage, phase, and frequency to avoid any panel rework after production starts.
Frequently Asked Questions
Q: How is daily output calculated for each block format on this line?
A: Each output figure is based on the 25-second molding cycle applied to the number of cavities per mould for a specific block size. For example, the 4640-piece daily figure assumes 400×200×200 mm hollow blocks at 4 pieces per mould over an 8-hour shift. Different formats change the cavity count and therefore the per-hour total.
Q: Which supporting equipment is included versus sold separately?
A: The line quotation covers the press, mixer, pallet feeder, and handling stations as a matched set. Stacking and curing rack systems can be added or left out depending on whether the buyer already has compatible infrastructure on site. Each item is listed individually so nothing arrives unannounced.
Q: How does pallet size affect my curing area and forklift layout?
A: The 850 × 480 mm pallet sets the spacing for every curing rack shelf and aisle width. If your existing forklift mast cannot clear that board height when stacked, you will need either a different pallet specification or a modified racking plan. Confirming these dimensions before shipment avoids costly yard rework.
Q: What voltage and control options are available for my market?
A: Voltage, frequency, and PLC display language are confirmed with each buyer before production. This ensures the control cabinet matches the local grid and operators can read the interface without translation delays. The confirmation step is built into the order process, not left to commissioning day.