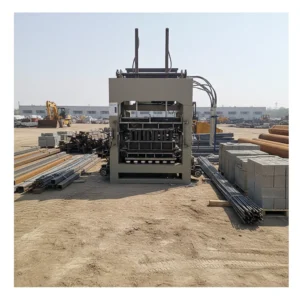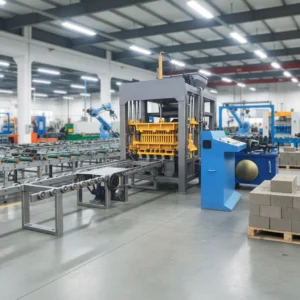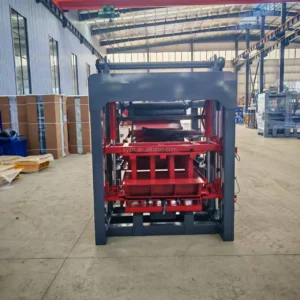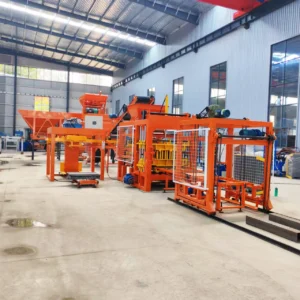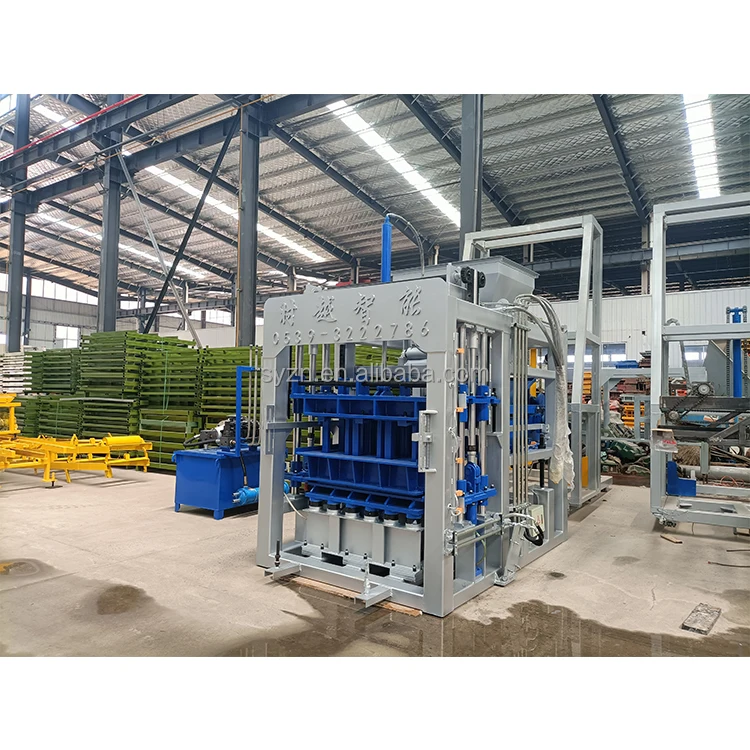
Matched System Configuration — every upstream and downstream station timed to the press cycle so the QT10-15 block making machine production line is never left waiting for pallets or raw material.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT10-15 |
| Product Type | Automatic Concrete Block Making Machine |
| Control System | PLC control cabinet |
| Hydraulic System | Independent integrated hydraulic station |
| Vibration Mode | Vertical station mode resonance with automatic FM-AM |
| Mould Format: 400×200×200 mm | 10 pcs/mould, 15-20s cycle, 1800-2400 pcs/hour, 14400-19200 pcs/8hr |
| Mould Format: 400×150×200 mm | 12 pcs/mould, 15-20s cycle, 2160-2880 pcs/hour, 17280-23040 pcs/8hr |
| Mould Format: 240×115×53 mm (solid brick) | 62 pcs/mould, 15-20s cycle, 8928-11160 pcs/hour, 71424-89280 pcs/8hr |
| Mould Format: 200×100×60 mm (paver) | 27 pcs/mould, 20-25s cycle, 5184-6480 pcs/hour, 41472-51840 pcs/8hr |
| Mould Format: 225×112.5×60 mm (interlocking) | 24 pcs/mould, 20-25s cycle, 4032-5040 pcs/hour, 32256-40320 pcs/8hr |
| Line Components | Pallet feed machine, block making machine, storage hopper, conveyor, hydraulic unit, PLC control cabinet |
| Automation Level | Automatic (basis to be confirmed) |
| Voltage & Frequency | Configurable per target market (basis to be confirmed) |
| Pallet Size & Material | Matched to buyer’s curing area and forklift (basis to be confirmed) |
| Warranty | 1 year for whole machine (excluding spare parts) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for building construction | Crushed stone, cement, sand aggregate mix |
| Solid brick production (240×115×53 mm) | Cement and fine aggregate blend |
| Paving block production (200×100×60 mm) | High-density concrete with coarse aggregate |
| Interlocking block production (225×112.5×60 mm) | Stabilized soil-cement or concrete mix |
| Multi-cellular brick production | Lightweight aggregate or foamed concrete |
| Block plant capacity upgrade | Replacement of existing press while retaining pallet circuit |
Why the Pallet Question Determines Your Real Output
A press cycling at full speed means nothing if pallets are not returning fast enough.
I spent years on assembly floors watching block machines idle while operators dragged pallets back by hand. The QT10-15 block making machine production line addresses this by specifying the pallet feed machine, conveyor, and hydraulic unit together with the press, so cycle times align across stations. When the pallet return loop is not quoted, buyers discover after commissioning that their actual daily output is a fraction of the press rating [NEED_CITE: pallet return circuit impact on block line throughput]. The quotation should show every station from raw material feeding through finished block removal, not just the press.
How the Line Stations Connect Around the Press
The storage hopper feeds raw material to the press on a timed sequence controlled by the PLC cabinet, so the mould fills at the exact moment the previous cycle ends. The pallet feed machine inserts a fresh pallet under the mould before vibration begins, and the conveyor removes the loaded pallet immediately after compaction. This coordination means the QT10-15 block making machine production line maintains its cycle rate without manual intervention at any single station. Each station’s timing is tuned during commissioning against the buyer’s specific mix design and block format.
Where Mismatched Cycle Times Stall the Entire Circuit
When a buyer adds an automatic stacker later without recalibrating the PLC logic, the stacker may not clear pallets quickly enough for the next cycle. I once configured a line where the downstream stacker could not keep pace with the press during solid brick runs, and the whole line backed up at the pallet exit. The PLC cabinet supplied with this line coordinates every station as one sequence, but the sequence must be verified against the buyer’s target format before dispatch [NEED_CITE: PLC logic synchronization across block line stations]. A mismatch at any single point — mixer output, pallet return, or stacker speed — forces the press to wait.
Reading the Specifications Against Your Actual Product Mix
The vibration force and hydraulic pressure must be matched to the buyer’s local aggregate and target block density. Vertical station mode resonance with automatic FM-AM adapts the compaction profile to different block formats, but the starting parameters must reflect the actual mix. The independent integrated hydraulic station sits apart from the host vibration and dust, which protects valve response over long shifts. Cycle times listed above are tied to specific mould formats — 15-20 seconds for hollow blocks and solid bricks, 20-25 seconds for pavers and interlocking bricks. Mould replacement is designed for simple format switching, but change time depends on the format and material being produced (basis to be confirmed). Pallet size must match both the curing rack spacing and the forklift the buyer already operates on site.
What Happens When Supporting Equipment Is Left Off the Quotation
A buyer who receives only the press and mould will soon realize that pallet handling, stacking, and curing are still manual operations. Real daily output then depends on how many workers are moving blocks by hand, not on the press cycle rate. I have seen lines where the quotation excluded the pallet feed machine and conveyor, and the buyer spent the first month reorganizing the entire floor layout to compensate [NEED_CITE: hidden costs of incomplete block line quotations]. The result is a press that runs at half capacity because pallets are not circulating fast enough.
Why This Line Is Configured as One Matched System
Block machinery is our single focus, which means the press, mould, pallet, and handling equipment are specified together rather than assembled from separate suppliers. Configuration is set against the buyer’s actual mix design, local aggregate, and target block format, not a catalogue default. Mould design covers the formats the buyer’s market sells, including custom drawings when standard formats do not match. The automation level is selectable so a buyer can begin with semi-automatic pallet handling and add stacking later. Installation includes operator training so the team understands how each station’s timing affects the next.
Documentation & Verification
- Line layout and capacity calculation stating the block format assumed for each output figure
- Machine specification sheet with hydraulic and electrical schematic
- Mould drawing and format list for every block type in the quotation
- Pallet specification showing size and material matched to buyer’s curing area
- Voltage, frequency, and PLC display language confirmation before production
- Factory test record on buyer’s target block format before dispatch
Installation, Commissioning & Support
- Foundation plan provided showing load points for the QT10-15 press and pallet feed machine
- Power circuit specification for the independent hydraulic station and PLC cabinet
- Machine arrives dismantled for container loading with reassembly guide included
- On-site commissioning with PLC sequence tuning against the buyer’s block format
- Operator training covering mould change procedure and daily maintenance checks
- Wear parts and mould list supplied with first replacement items identified
What to Share With Your Inquiry
Tell us the block formats your market sells and the daily output you need per format. Share your local aggregate type and whether you have an existing mixer and curing area. Confirm your site voltage, frequency, and preferred PLC display language so we can set the control cabinet before production begins.
Frequently Asked Questions
Q: How is line capacity verified per block format, and what if upstream or downstream stations cannot match?
A: Every capacity figure is stated against a specific mould format and cycle time. During line design, each station’s throughput — mixer output, pallet feed speed, conveyor removal rate — is calculated to match or exceed the press cycle. If any station falls short, the PLC sequence is adjusted or the station is upgraded before dispatch.
Q: Which supporting equipment stations are included, and which are optional?
A: The standard line includes the pallet feed machine, storage hopper, conveyor, hydraulic unit, and PLC control cabinet alongside the press. Automatic stacking and curing rack handling are available as additions and must be specified during quotation so the PLC logic accounts for them from the start.
Q: How is pallet size and material chosen for the buyer’s site?
A: Pallet dimensions are matched to the curing rack spacing the buyer already uses, and the material is selected based on the block weight and forklift capacity on site. We confirm these details during inquiry so pallets arrive compatible with existing handling equipment.
Q: What voltage, frequency, and PLC language are confirmed before production?
A: These are confirmed during the quotation stage. The PLC cabinet is configured for the buyer’s local power supply and display language before the factory test, so commissioning on site is not delayed by electrical mismatches or unreadable menus.
Q: How are mould change times coordinated across the full line?
A: Mould replacement on the press is one part of format switching. The pallet feed timing, vibration profile, and conveyor speed must also adjust to the new format. The PLC cabinet stores parameters for each confirmed mould, and operators are trained to switch formats across all stations during commissioning.