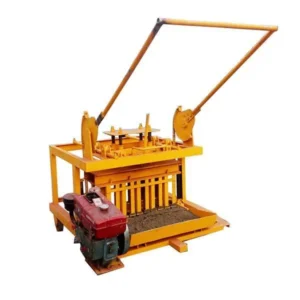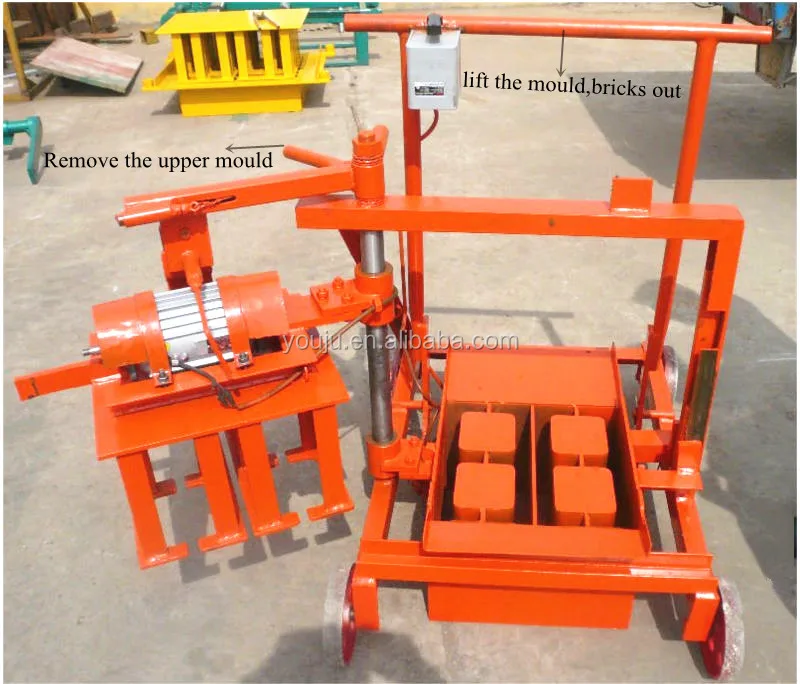
Matched System Configuration — every QMJ2-45 mobile block making machine production line proposal includes the upstream mixer, material feed arrangement, and curing layout calculated against the buyer’s target block format, so the press never waits for the next batch.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QMJ2-45 |
| Product Type | Mobile Concrete Block Making Machine |
| Automation Level | Manual mobile operation |
| Mould Format | Hollow brick (multiple sizes via mould change) |
| Mould Change System | Manual mould change for different hollow brick formats |
| Cycle Time per Format | 25–30s (basis not stated in source — confirm block format / material / thickness) |
| Output Capacity | 160 pcs/h based on 400×200×200mm hollow block, 2 pcs/mould; 320 pcs/h based on 400×100×200mm hollow block, 4 pcs/mould |
| Daily Output (8h) | 1280 pcs based on 400×200×200mm hollow block; 2560 pcs based on 400×100×200mm hollow block |
| Pallet Size | Not required (pallet-less egg-laying operation) |
| Labour Requirement | 1–3 workers |
| Operating Space | Small footprint, mobile and free-moving |
| Hydraulic Pressure | Not applicable (manual mobile type) |
| Control System | None (manual operation) |
| Certification | ISO9001:2000, CE |
Application Suitability
| Application | Material or Output |
|---|---|
| Small-scale on-site hollow block production | Crushed stone, sand, cement, and water mixed for structural hollow bricks |
| Entrepreneur-level first block plant | Low-investment hollow brick production using locally sourced aggregate |
| Remote or space-constrained job sites | Pallet-less egg-laying operation on flat compacted ground |
| Multi-format hollow brick production | 400×200×200mm, 400×150×200mm, and 400×100×200mm formats via manual mould change |
Why "Pieces per Hour" Means Nothing Without the Rest of the Line
The mobile block making machine production line only produces blocks as fast as the slowest station around it.
Buyers regularly compare mobile machines on cycle time alone, assuming a 25–30 second press stroke translates directly into hourly output. In practice, I have watched a mobile press sit idle for most of a shift because the pan mixer upstream could not deliver a fresh batch in time. The operator stands there, the machine waits, and the daily count falls well short of the catalogue figure. [NEED_CITE: material feed rate impact on manual press uptime]
A mobile block making machine production line must be sized around the bottleneck, and for a manual mobile press that bottleneck is almost always mixing and material delivery, not the press stroke itself.
How the QMJ2-45 Connects to Upstream Mixing
The QMJ2-45 is a pallet-less egg-laying press, which means every cycle deposits wet blocks directly on the ground and the machine moves forward. The press operator needs a steady supply of mixed concrete delivered to the hopper within each 25–30 second window. If a small pan mixer is feeding the QMJ2-45, its batch volume and mixing time must be calculated so that a fresh batch arrives before the current one runs out. On a mobile block making machine production line, undersizing the mixer is the most common reason daily output disappoints.
How Pallet-less Operation Reshapes the Curing Area
Unlike pallet-based lines where blocks ride on boards through a curing rack system, the QMJ2-45 leaves blocks on the ground where they are laid. This removes the entire pallet return loop — no pallet feeding station, no pallet cleaning, no pallet storage racks. The trade-off is that the curing area must be a large, flat, compacted surface that can accommodate the daily output footprint. Planning the curing zone length and the path the machine travels each shift is a core part of laying out this mobile block making machine production line correctly. [NEED_CITE: ground curing area requirements for egg-laying block machines]
Reading the Capacity Table Without Being Misled
The QMJ2-45 can produce hollow bricks in three thickness formats: 400×200×200mm at 2 pieces per mould, 400×150×200mm at 3 pieces per mould, and 400×100×200mm at 4 pieces per mould. The cycle time of 25–30 seconds applies across formats, but the piece count per stroke changes the hourly rate significantly — from 160 pieces per hour on the 200mm format up to 320 pieces per hour on the 100mm format. A realistic mobile block making machine production line proposal must state which block format the capacity calculation assumes, because sizing the mixer and curing area against the wrong number leads to idle time or wasted space. The vibration force and hydraulic pressure figures are not applicable here since this is a manual mobile unit; block density depends on the mix design and local aggregate rather than machine pressure settings.
The Cost of Skipping the Line Balance Check
When a mobile press arrives on site without the supporting equipment specified alongside it, the buyer is forced to improvise. A mixer that is too small means the press waits. A curing area that is too short means blocks are stacked before they have set, cracking under their own weight. Workers assigned to block handling without a clear workflow end up bottling-necking at the press exit. [NEED_CITE: common commissioning delays in small-scale block plants] These problems do not show up in the machine quotation — they surface on the first production day, and the buyer blames the press for what is actually a line design failure.
Why Buyers Plan the Line Here
Every mobile block making machine production line we configure starts from the buyer’s target block format and local aggregate, not from a catalogue default. The QMJ2-45 is specified together with its mould set, mixer sizing, and curing layout as one matched system. Mould design covers the hollow brick formats the buyer’s market actually sells, including custom drawings when needed. The automation level is selectable — a buyer can begin with this manual mobile unit and move to a semi-automatic pallet-based line later without changing the block format. Installation support includes line layout planning and operator training so the crew understands how mixing cadence, press stroke, and block handling fit together. [NEED_CITE: mobile block machine installation and operator training scope]
Documentation & Verification
- Line layout and capacity calculation stating the block format assumed for the QMJ2-45
- Machine specification sheet with per-format cycle time and output figures
- Mould drawing and format list for all hollow brick sizes included in the order
- Voltage and power confirmation for the mixer and any ancillary motors before dispatch
- Factory test record on the buyer’s specified block format before shipment
- Operation and maintenance manual covering daily checks and mould change procedure
Installation, Commissioning & Support
- Flat compacted ground assessment for pallet-less egg-laying operation and curing area sizing
- Power supply and voltage confirmation for mixer motor before the QMJ2-45 ships
- Mixer placement relative to the press to keep manual material feed within the 25–30 second cycle window
- First-run block density and dimension check across all three hollow brick formats
- Operator training on manual mould change, mix consistency, and block handling workflow
- Wear parts list covering mould edges and vibration components with reorder reference numbers
Before You Request a Quote
Tell us which hollow brick format drives your daily volume and what local aggregate you plan to use — sand type, stone grading, and cement availability shape both the mixer sizing and the cycle time we calculate. Share your available site area so we can map the curing zone and material delivery path around the QMJ2-45. If you already have a mixer or other equipment on site, send the specifications so we can confirm whether they fit the line or need replacing.
Frequently Asked Questions
Q: How do I verify realistic daily output when the capacity table shows different figures for each block format?
A: Identify the format your market buys most and use that figure for line sizing. The QMJ2-45 produces 160 pieces per hour on 400×200×200mm blocks and 320 pieces per hour on 400×100×200mm blocks, so the gap is significant. We calculate daily output based on your target format and confirm mixer capacity against that number, not the highest figure in the table.
Q: What upstream mixing equipment is needed to keep the QMJ2-45 running without idle time?
A: The mixer must deliver a fresh batch within each 25–30 second press cycle. For the QMJ2-45, a small pan mixer with a batch volume matched to the mould cavity fill is typically sufficient. We calculate the mixer drum size and motor power against your chosen block format so material feed never becomes the bottleneck on the line.
Q: How does pallet-less egg-laying operation change the curing area layout compared to a pallet-based line?
A: Pallet-based lines stack blocks on boards inside curing racks, using vertical space. The QMJ2-45 deposits blocks directly on flat ground, so the curing area must be wide enough to hold a full shift of output spread across the machine’s travel path. We include curing zone dimensions in the line layout before the machine ships.
Q: Can the QMJ2-45 be upgraded later into a semi-automatic line with pallet feeding and stacking?
A: The QMJ2-45 itself is designed for manual mobile operation and cannot be retrofitted with automatic pallet systems. However, buyers who outgrow it can move to a semi-automatic pallet-based press in the same product range while keeping the same block formats and mould design principles. We plan that transition path during the initial consultation.
Q: What installation and training support is available for first-time buyers setting up a complete small-scale line?
A: We provide a line layout showing mixer placement, press travel path, and curing area dimensions for the QMJ2-45. On-site commissioning covers first-run testing across all ordered hollow brick formats, and operator training addresses mix consistency, manual mould change, and block handling workflow so the crew can run independently from day one.