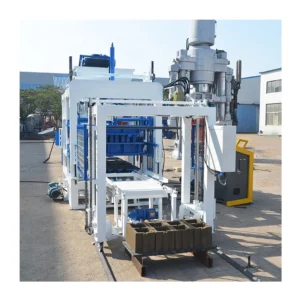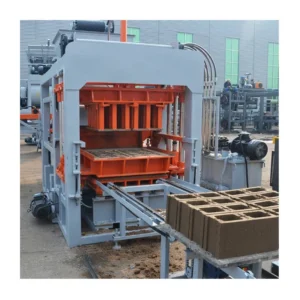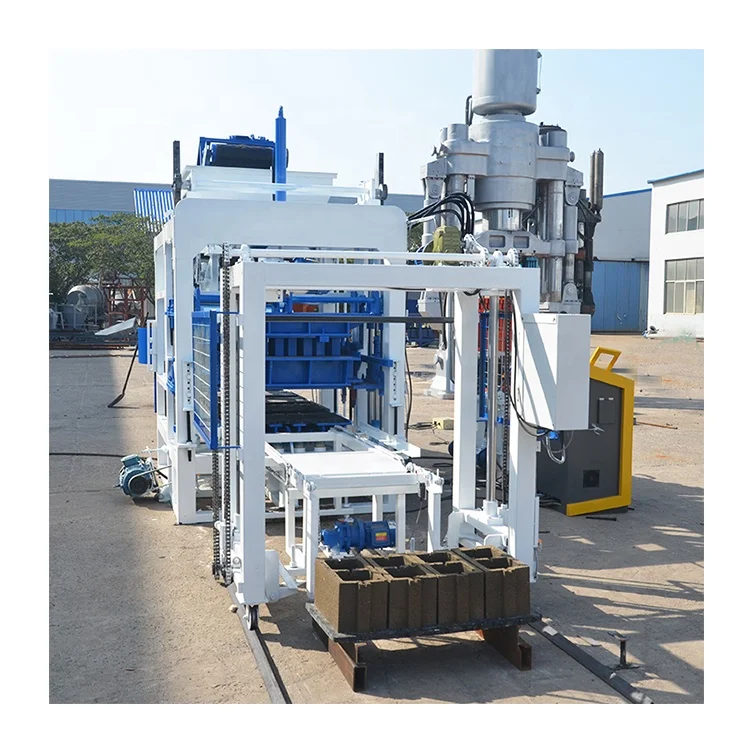
Matched System Supply — every station from mixer to stacker specified against the QT4-18 cycle, not sourced piecemeal and left to mismatch on your floor.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Semi-Automatic Concrete Block Making Machine |
| Model | QT4-18 |
| Overall Dimension | 2500×1750×2200 mm |
| Rated Pressure | 16 MPa |
| Vibration Form | Platform Vibration |
| Pallet Size | 950×550 mm |
| Molding Cycle | 18–25 s (basis to be confirmed by block format) |
| Overall Power | 27.5 kW |
| Control System | PLC with frequency converter, Schneider electrical components |
| Mould Lifting Mechanism | Double-sided synchronous gears |
| Material Feeder System | Hopper, feeding box, feeding platform and conveyor |
| Block Receiver | Frame, conveyor system, idler wheels with motor, reducer and triangle belt |
| Automation Level | Semi-automatic (manual or mechanical pallet handling to curing yard) |
| Mould Included | One free hollow mould; extra moulds available at additional cost |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production | Crushed stone, sand, cement, water |
| Solid block manufacturing | Local aggregate blended with Portland cement |
| Paving and interlocking formats | Fine aggregate mixes subject to mould selection |
| Contractor on-site plants | Raw materials sourced within project radius |
Why "Blocks per Hour" Means Nothing Without the Rest of the Line
The press cycle only matters when the mixer, conveyor and pallet feeder keep the same tempo.
I once watched a semi-automatic block machine production line lose most of a shift because the pan mixer discharged slower than the press cycled. The operator stood idle while the hopper ran dry, and the daily tally fell well short of what the brochure promised. When the QT4-18 is quoted as a complete line, the JQ500 pan mixer, 8 m belt conveyor and hydro-cylinder pallet feeder are matched to the 18–25 s molding window so no station waits on another [NEED_CITE: line balancing principles for concrete block plants].
Stations That Share a Clock
The hydro-cylinder pallet feeder pushes a fresh pallet onto the vibrating platform and, in the same stroke, transfers the cured green block onto the receiver conveyor. This mechanical link means the pallet recycle time is bound to the press cycle, removing one variable from the operator’s day. The semi-automatic block machine production line only holds its rhythm when every station respects that shared clock.
Feeding the Hopper Without Gaps
An 8 m belt conveyor — with a 6 m option for tighter plant footprints — carries mixed material from the JQ500 pan mixer to the QT4-18 hopper. The conveyor speed is set so the hopper never empties mid-cycle, yet never overfills and spills onto the platform. If the belt runs too fast, aggregate segregates; too slow, and the press stalls [NEED_CITE: conveyor speed versus material segregation in concrete handling].
Reading the Pressure and Vibration Together
The 16 MPa rated pressure works with platform vibration to consolidate the mix inside the mould cavity. Higher pressure alone will not produce a denser block if the vibration frequency fails to settle fine particles into voids. The PLC with frequency converter lets the operator tune vibration duration per format, so a hollow block with thin walls receives a different profile than a solid paver. Double-sided synchronous gears lift the mould evenly, preventing the half-formed block from dragging against one side of the cavity.
What Happens When Upstream Stations Are Sized Wrong
A mixer with too small a batch volume forces the press operator to wait between batches, cutting real daily output without any fault in the press itself. A conveyor that is too short or too long shifts the material drop point, causing the feeding box to scrape or spill. Stackers and trolleys that arrive as an afterthought leave green blocks sitting on the pallets longer than necessary, risking surface damage before they reach the curing yard [NEED_CITE: green block handling damage in semi-automatic plants].
Why Procure the Line as One Package
Specifying the QT4-18 alongside its JQ500 mixer, belt conveyor and block receiver from a single source means the foundation drawing shows every station in relation to the next. Voltage, frequency and PLC display language are confirmed once for the entire line, so commissioning is not delayed by a mismatched control panel on the conveyor motor. Moulds, pallets and wear parts are listed together, so the first replacement order does not reveal that a critical hydraulic seal was never included in the original quotation.
Documentation & Verification
- Line layout drawing showing QT4-18, mixer and conveyor positions with overall footprint
- Capacity calculation sheet stating the block format and molding cycle assumed
- Hydraulic and electrical schematics matching the shipped PLC and valve configuration
- Factory test record run on the buyer’s specified pallet size and mould format
- Packing photographs and container loading plan before dispatch
Installation, Commissioning & Support
- Cement-poured foundation leveled to tolerance before the 2500×1750 mm press footprint is set
- Dedicated circuit rated for the 27.5 kW total load with voltage confirmed to local grid
- Machine arrives dismantled; reassembly includes aligning synchronous gears and conveyor idlers
- PLC display language and frequency converter parameters set during first-power commissioning
- Operator training covers mould change procedure and pallet feeder timing adjustment
- Wear parts list covers hydraulic seals, gear teeth and conveyor belts for the first year
Before You Send an Inquiry
Tell us which block format your market buys most, the local aggregate you plan to use and the daily volume you need to sustain. Share your workshop dimensions, existing curing yard layout and the voltage and frequency at your site. If you already run a mixer or conveyor from another supplier, send the model plate details so we can confirm whether the QT4-18 semi-automatic block machine production line can integrate with what you have.
Frequently Asked Questions
Q: How is daily capacity calculated and which block format does the molding cycle assume?
A: The 18–25 s cycle varies with block height and wall thickness. We calculate daily capacity against your target format — for example, a 400×200×200 mm hollow block — and state the assumed pallet count per shift in the quotation, so you see a number tied to your product, not a catalogue maximum.
Q: How do station cycle times need to match so the press is not left waiting?
A: The JQ500 mixer batch volume, belt conveyor travel speed and hydro-cylinder pallet stroke are all set against the QT4-18 press cycle. If any station runs slower, the press idles; if faster, material piles up. We specify every station together and verify timing during factory testing.
Q: What supporting equipment is included in the quotation and what must I source separately?
A: The standard package covers the press, one hollow mould, pallet feeder, block receiver, JQ500 mixer and belt conveyor. Cement silo, batching plant, curing-yard trolleys and stacker are listed as options. We confirm each item as included or excluded before you sign.
Q: Can the line start semi-automatic and later upgrade individual stations?
A: Yes. The PLC and frequency converter architecture allows individual stations — such as automatic stacking or pallet recycle — to be added later without replacing the press control cabinet. We leave conduit and signal points during initial installation to simplify future upgrades.