
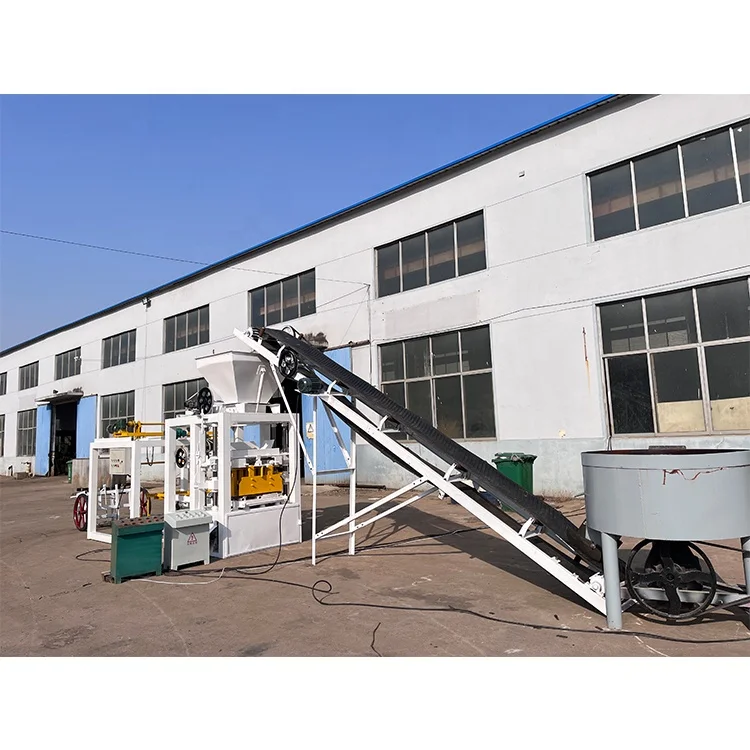
Matched system integration — Every station from the JQ350 mixer to the pallet trolley is specified together with the QTJ4-24 press so cycle times align and the machine is never left waiting for upstream or downstream equipment.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QTJ4-24 |
| Product Type | Semi-Automatic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 2060×1730×2580 mm |
| Total Weight | 1800 kg |
| Rated Power | 14.25 kW |
| Molding Cycle | 24 s |
| Vibration Frequency | 4200 r/min |
| Vibration Force | 35.5 kN |
| Mixer Model | JQ350 |
| Pallet Size | 850×450×20 mm |
| Output Capacity (Hollow Block 390×190×190 mm) | 480 pcs/hr, 3800 pcs/8hr |
| Output Capacity (Hollow Block 400×150×200 mm) | 600 pcs/hr, 4800 pcs/8hr |
| Output Capacity (Solid Brick 240×115×53 mm) | 2100 pcs/hr, 17000 pcs/8hr |
| Mould Format Options | Hollow block (8/6/5/4 inch), solid brick, paver |
| Raw Materials | Crushed stones, sand, cement, fly ash, dust |
| Automation Level | Semi-automatic |
| Certification | CE |
Application Suitability
| Application | Material or Output |
|---|---|
| Small to medium-scale block plants | Hollow blocks from crushed stone, sand, and cement |
| On-site contractor production | Solid bricks and pavers using locally available aggregate |
| Building material distributor lines | Multiple block formats via interchangeable moulds |
| First-time block plant entrepreneurs | Semi-automatic setup with manual pallet handling |
Why Pallet Size Matters More Than Press Capacity in a Semi-Automatic Block Making Machine Production Line
A mismatched pallet spec can halt an entire block line regardless of how fast the press cycles.
I have watched lines sit idle for weeks because the buyer ordered pallets that did not fit the curing racks already on site, or that were too heavy for the forklift in the yard. The QTJ4-24 runs on 850×450×20 mm pallets, and that dimension must align with your curing area spacing and material handling equipment before the first pallet is fed. When it does not, freshly pressed blocks sit on the press table and the next cycle cannot start [NEED_CITE: pallet sizing and curing rack coordination in block plants].
How Stations Connect Around the Press
A Semi-Automatic Block Making Machine production line is only as fast as its slowest station. The JQ350 mixer must deliver a consistent batch to the press hopper within the 24-second molding cycle, otherwise the press idles between cycles. Belt conveyors and feed systems need to be sized so that raw material arrives at the mixer at a rate matching the press throughput.
Where Bottlenecks Hide in Semi-Automatic Layouts
In semi-automatic configurations, pallet feeding and block removal are handled manually or by trolley. If the operator cannot return a cured pallet and remove a fresh one within the cycle window, the press waits. I always map the operator walk path and pallet travel distance during line layout to spot these delays before equipment ships [NEED_CITE: manual pallet handling cycle time in semi-automatic block plants].
Reading the Specs That Actually Matter
Vibration force of 35.5 kN combined with vertical bed mould vibration determines the density and compressive strength of each block. The 4200 r/min vibration frequency works in tandem with the upper mould compression to compact the mix evenly. Pallet material — whether fiberglass or treated wood at 850×450×20 mm — affects vibration transmission and therefore block consistency across the pallet surface.
What Happens When Stations Are Sourced Separately
When a buyer purchases the press from one supplier, the mixer from another, and pallets from a third, there is no single party responsible for cycle time coordination. The mixer may batch too slowly, the pallets may arrive the wrong thickness, and the conveyor may not match the feed height. These gaps surface during commissioning, not during quoting, and they cost time and rework to fix [NEED_CITE: equipment integration risks in multi-supplier block lines].
Why Buying the Line as a System Changes the Outcome
Block machinery is our single focus, which means the QTJ4-24 press, JQ350 mixer, pallet specification, and trolley are configured as one package rather than assembled from separate sources. The line layout we provide states output per block format, not a single headline number. We confirm pallet size against your curing area and forklift capacity before production begins. Mould options are matched to the formats your market actually sells. Voltage, frequency, and control language are verified against your local standard so commissioning does not stall at first power-on.
Documentation & Verification
- Line layout with capacity stated per block format and molding cycle assumption
- Pallet specification sheet including dimensions, material, and recommended quantity
- Factory test record covering press cycle time and vibration force before dispatch
- Mould drawing and format list showing all available block profiles
- Voltage and control language confirmation document signed before production
Installation, Commissioning & Support
- Foundation plan based on 2060×1730 mm footprint and 1800 kg operating weight
- Power connection requirements for 14.25 kW total rated load with dedicated circuit
- Pallet quantity recommendation of 300 to 500 pieces for continuous curing rotation
- Operator training on 24-second cycle workflow including manual pallet exchange
- Wear parts list covering vibration components and hydraulic seals for first replacement order
- Mould change procedure with estimated time per format swap
What to Prepare Before Requesting a Quote
Tell us which block formats your market moves — hollow block dimensions, solid brick sizes, or paver profiles — and what your target daily output is per format. Share your site voltage and frequency, the pallet material you prefer, and the curing space dimensions you have available so we can confirm pallet sizing fits.
Frequently Asked Questions
Q: How is daily output calculated and which block format does each figure assume?
A: Output is stated per specific block format based on a 24-second molding cycle. For the QTJ4-24, that means 3800 hollow blocks of 390×190×190 mm per 8-hour shift, 4800 pieces of 400×150×200 mm hollow blocks, or 17000 solid bricks of 240×115×53 mm. Figures assume continuous operation with matched pallet handling.
Q: What supporting equipment stations are needed around the QTJ4-24 press to form a complete line?
A: A typical semi-automatic line includes the JQ350 mixer, belt conveyor for raw material feed, pallet feeding system, and a trolley for moving pressed blocks to the curing area. Each station is selected to match the press cycle so no single point creates a bottleneck.
Q: How do I match pallet size and material to my existing curing area and forklift?
A: The QTJ4-24 uses 850×450×20 mm pallets. We confirm that your curing rack spacing accommodates this dimension and that your forklift can handle the loaded pallet weight. Fiberglass and treated wood options are available depending on your curing environment and rotation frequency.
Q: What voltage, frequency, and control language options are available for my target market?
A: Voltage and frequency are confirmed against your local supply standard before production begins. Control panel display language is specified at the same stage. This avoids commissioning delays that occur when these details are left to default settings.
Q: How does the semi-automatic configuration allow for future automation upgrades?
A: The QTJ4-24 line can start with manual pallet handling and later add automatic pallet feeding, stacking, and cubing systems. The press table and cycle timing are designed to accept these upgrades without requiring a full machine replacement.



