
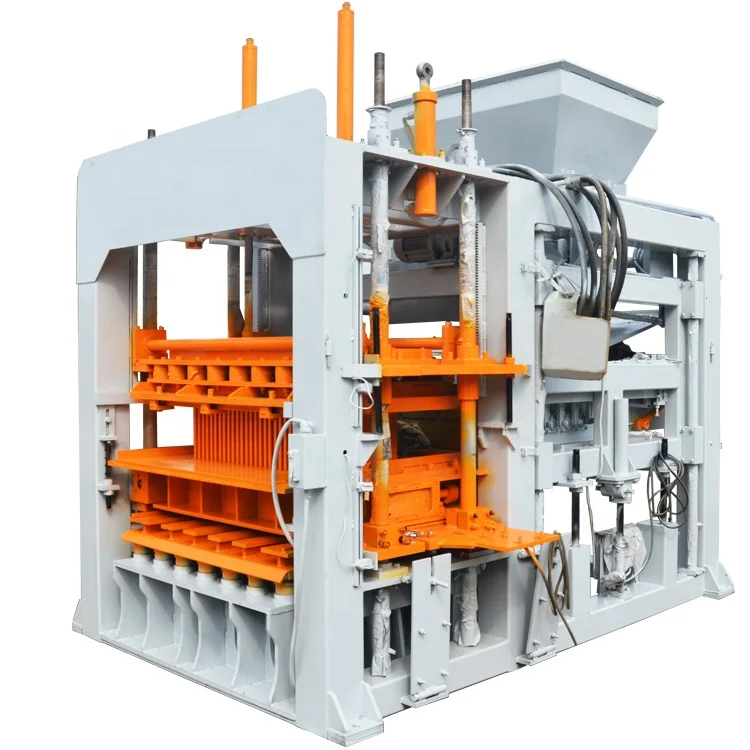
System Matched — Raw material feeding, mixing, pallet circulation, stacking and curing rack handling are specified around the QT8-15 press so cycle times align and the press is never left waiting for upstream or downstream stations.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT8-15 |
| Product Type | Automatic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 8300×1860×3000 mm |
| Total Mass | 8 T |
| Rated Pressure | 21 MPa |
| Main Vibration Form | Platform Vibration |
| Vibration Frequency | 2800-4500 r/min |
| Vibration Force | 45 kN |
| Pallet Size | 950×900 mm |
| Molding Cycle | 15-20 s |
| Overall Power | 55.5 kW |
| Demolding Method | Hydraulic |
| Factory Area | 300 m² |
| Automation Level | Automatic |
| Applied Products | Concrete blocks, hollow/solid blocks, pavers, interlocking blocks, curbstone, colored pavers |
| Raw Material | Crushed stone, sand, cement, dust, fly ash, gravel, slag |
| Output Capacity | (basis not stated in source — confirm block format / material / thickness) |
| Voltage & Frequency | (not stated in source — confirm target market requirement) |
| Control System | (not stated in source — confirm PLC brand / language) |
Application Suitability
| Application | Material or Output |
|---|---|
| Block and paver production plants | Hollow and solid blocks from crushed stone, sand, cement |
| Construction contractors producing blocks on-site | Interlocking blocks and curbstones from local aggregate |
| Concrete product manufacturers expanding format range | Colored pavers and porous bricks with fly ash or slag |
| Housing and infrastructure project contractors | High-volume standard blocks for masonry and paving |
| Building material distributors and machinery importers | Diverse formats from a single platform and pallet size |
What "Complete Line" Actually Means for Daily Output
A block press is only as fast as the slowest station feeding or clearing it.
Buyers often receive quotations for the press alone, with pallet handling, stacking and curing excluded. The result is an automatic block making machine production line on paper, but manual labour bottlenecks in reality. I have seen setups where the mixer discharge and belt conveyor timing were misaligned with the host machine cycle, leaving the press idle for seconds every mould, quietly cutting daily throughput [NEED_CITE: impact of upstream station timing on press utilization]. When raw material feeding, mixing, pallet circulation, stacking and curing rack handling are specified together, the 15-20 s molding cycle of the QT8-15 is supported by matched upstream and downstream stations rather than compromised by them.
Stations Upstream of the Press
The raw material feeding and mixing stations must deliver a consistent batch to the press hopper within the 15-20 s molding cycle. If the mixer discharges too slowly or the belt conveyor runs at a fixed speed that does not sync with the press demand, the host machine waits. Configuring the batching accuracy and conveyor timing around the actual block format and mix design ensures the automatic block making machine production line runs without starvation pauses.
Stations Downstream of the Press
Fresh blocks leave the press on 950×900 mm pallets that must be transferred to the curing rack without delay. If the pallet return loop is too slow, the press cannot accept the next mould. The stacking and cubing station must clear finished pallets at a rate that matches the press output, and the curing rack capacity must hold at least one full day of production so that pallets circulate freely [NEED_CITE: pallet circulation and curing rack sizing for block plants].
Matching Vibration to Mix Design
The platform vibration system operates at an adjustable 2800-4500 r/min with 45 kN force. This range must be set against the buyer’s specific mix design and local aggregate — a sand-rich mix requires a different frequency and amplitude than a crushed-stone-heavy mix. When the vibration profile is tuned to the actual material, block density remains consistent across formats from hollow blocks to pavers.
Specifications That Shape the Line Layout
The 21 MPa rated hydraulic pressure and hydraulic demolding method determine how quickly and cleanly blocks release from the mould, directly affecting the cycle time that upstream and downstream stations must match. The 55.5 kW overall power draws on a dedicated circuit; the voltage and frequency must be confirmed before production so that motors and PLC controls arrive compatible with the site supply. The 300 m² factory area footprint sets the minimum building envelope, and the 8 T total mass requires a reinforced concrete foundation to absorb vibration without transmitting it to adjacent equipment or structures.
The Cost of a Line Designed Around the Press Alone
When supporting equipment is sourced separately or excluded from the quotation, each station operates on its own timing rather than the press cycle. Pallets pile up between the press and the curing rack, operators handle output by hand, and the quoted capacity never materialises on the factory floor [NEED_CITE: consequences of unmatched line station cycle times]. Voltage incompatibility discovered after arrival delays commissioning. A pallet size chosen without reference to the buyer’s existing forklift and curing area forces unplanned equipment purchases.
Why Procure the Full Line From One Source
Block machinery is a single focus here, so the QT8-15 press, mould, pallet and handling equipment are specified as one matched system. The line layout and capacity calculation state the block format assumed for each output figure, removing guesswork. Mould design covers the formats the buyer’s market actually sells, with custom drawings available. Automation level is selectable — a buyer can start with semi-automatic pallet handling and upgrade to full stacking and cubing later. Installation and commissioning support includes operator training so that the timing between stations is verified on site, not just on paper.
Documentation & Verification
- Line layout and capacity calculation stating the block format assumed for each output tier
- Machine specification sheet covering the 55.5 kW power, 21 MPa pressure and 950×900 mm pallet
- Hydraulic and electrical schematics for the complete line from mixer to curing rack
- Voltage, frequency and PLC display language confirmation signed off before production
- Factory test record on the buyer’s target block format and mix design before dispatch
- Operation and maintenance manual with wear parts and mould list
Installation, Commissioning & Support
- Reinforced concrete foundation sized to the 8 T mass and 8300×1860×3000 mm footprint of the QT8-15
- Dedicated power circuit matched to confirmed voltage and frequency for the 55.5 kW total load
- Machine dismantled for container shipment and reassembled on site with alignment verification
- First-run commissioning with molding cycle timing checked across all line stations
- Operator training on mould change procedure, vibration frequency adjustment and PLC controls
- Wear parts and mould supply list with hydraulic seal and vibration motor replacement intervals
Information Needed for a Line Proposal
To configure the QT8-15 within a complete automatic block making machine production line, share the target block format, daily output requirement and local raw material source. Confirm the available workshop area, ceiling height and existing curing rack or forklift capacity. Specify the site voltage, frequency and preferred PLC display language so that electrical and control systems are built to match before shipment.
Frequently Asked Questions
Q: How is the cycle time of each line station matched so the press is not left waiting?
A: Each upstream and downstream station — mixer discharge, belt conveyor, pallet feeder, stacker and curing rack handler — is timed against the 15-20 s molding cycle of the QT8-15. The line layout document shows the cycle time at every station so that no single point creates a bottleneck.
Q: What supporting equipment is included in the quotation?
A: The quotation covers raw material feeding, mixing, pallet circulation, stacking and curing rack handling alongside the QT8-15 press. Each item is listed separately so the buyer sees exactly which stations are included and which remain the buyer’s scope.
Q: How is pallet size and material chosen for the buyer’s site?
A: The 950×900 mm pallet is checked against the buyer’s curing area dimensions and forklift rating. If the existing curing rack or handling equipment requires a different size, the pallet specification is adjusted before the line layout is finalised.
Q: What electrical and control details are confirmed before shipment?
A: Voltage, frequency and PLC display language are confirmed in writing before production begins. This ensures that motors, heaters and control panels arrive compatible with the site supply and readable by local operators, avoiding commissioning delays.
Q: How does the line layout change when adding a new block format?
A: Adding a format may change the molding cycle time, which in turn affects upstream batching and downstream stacking rates. The revised layout recalculates station timing for the new format and confirms whether existing pallet, curing and stacking capacity remains sufficient.



