
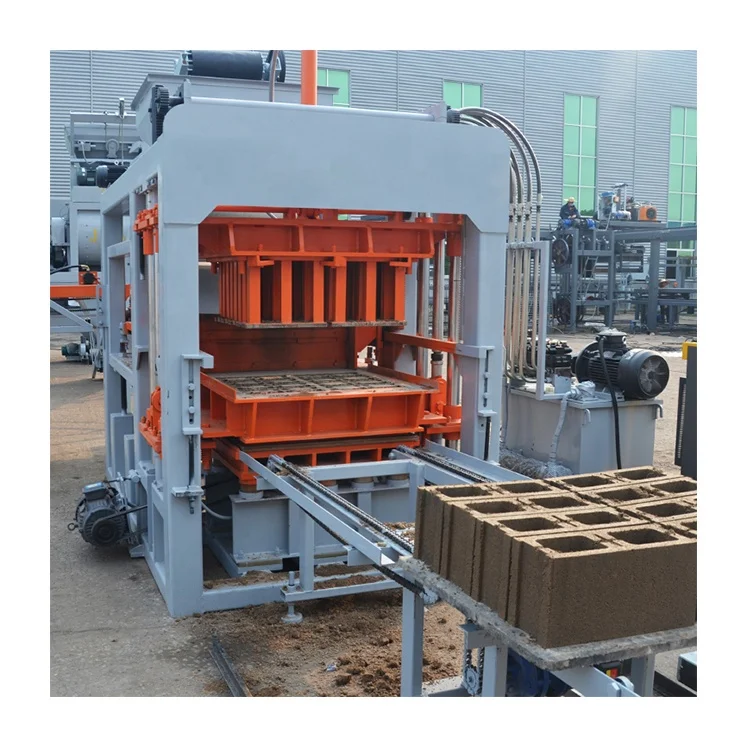
Matched Line Stations — The QT6-15 block making machine production line pairs the press with a JQ350 mixer, pallet feeder, brick conveyor, and block sweeper so cycle times stay balanced across every station.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Fully Automatic Hydraulic Block Making Machine |
| Model | QT6-15 |
| Overall Dimensions (L×W×H) | 7400×1900×2660 mm |
| Molding Cycle | 15–25 s |
| Vibration Frequency | 4600 r/min |
| Vibration Force (Exciting Power) | 40–50 kN |
| Total Power | 31.25 kW |
| Mixer Model | JQ350 |
| Pallet Size | 850×550×25 mm |
| Net Weight | 7 T |
| Control System | PLC control system |
| Hydraulic Station | Included |
| Included Line Equipment | Pallet feeder, brick conveyor, block sweeper, manual hydraulic trolley |
| Applied Products | Paver, solid block, hollow block, curbstone |
| Raw Materials | Crushed stones, sand, cement, dust, fly ash |
| Automation Level | Fully automatic |
| Output – Hollow Block 400×200×200 mm | 1200–1680 pcs/h (basis: 400×200×200 mm, 15–20 s cycle) |
| Output – Hollow Block 400×150×200 mm | 1800–2400 pcs/h (basis: 400×150×200 mm, 15–20 s cycle) |
| Output – Solid Brick 240×115×53 mm | 3240 pcs/h (basis: 240×115×53 mm, 15–20 s cycle) |
| Daily Output – Hollow 400×200×200 mm | 9600–13440 pcs per 8 hr shift |
| Daily Output – Hollow 400×150×200 mm | 14400–19200 pcs per 8 hr shift |
| Daily Output – Solid 240×115×53 mm | 16200–19440 pcs per 8 hr shift |
| Voltage & Frequency | To be confirmed per target market |
| Hydraulic Pressure | To be confirmed with manufacturer |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for masonry walls | Crushed stone, sand, cement, fly ash – 400×200×200 mm or 400×150×200 mm formats |
| Solid brick manufacturing | Cement and fine aggregate – 240×115×53 mm standard brick |
| Paver and curbstone production for infrastructure | Crushed stone and sand mixes in interlocking and kerb formats |
| On-site block production for housing projects | Locally sourced aggregate blended with cement on the project site |
| Fly ash brick production for sustainable construction | Fly ash, dust, and cement blends in solid or hollow formats |
What "Cycles per Hour" Leaves Out of the block making machine production line Quotation
Capacity means nothing unless every station upstream and downstream can keep pace with the press.
I once watched a QT6-15 hollow block press sit idle for two weeks because the mixer feeding it could not deliver a fresh batch every 15–25 seconds. The pallet feeder downstream jammed on every fourth cycle, and the whole block making machine production line bottlenecked at the press while workers stacked wet blocks by hand. Quoted throughput assumed perfect flow; real output fell far short. That kind of mismatch is invisible on a spec sheet but painfully obvious once containers are opened and power is connected [NEED_CITE: common causes of block plant commissioning delays].
Where the Stations Meet — and Where They Don’t
The JQ350 mixer sits upstream of the QT6-15 press and must discharge a full batch before the next molding cycle begins. When the cycle runs at the shorter end of the 15–25 s window, mixing time becomes the governing constraint. Sizing the mixer to the press cycle is part of the block making machine production line design, not an afterthought left to the buyer’s local contractor.
Pallet Flow and the Hidden Gap After the Press
The pallet feeder loads raw boards into the press, and the brick conveyor carries cured blocks away — but the gap between conveyor discharge and the curing rack is where many turnkey block plant plans break down. If pallet size does not match the buyer’s existing curing racks or forklift tines, every board must be rehandled manually. The 850×550×25 mm pallet specified here must be validated against the curing area layout before production begins [NEED_CITE: pallet and curing rack compatibility in block plants].
Reading the Vibration and Hydraulic Numbers Together
The 40–50 kN vibration force and 4600 r/min frequency compact the mix inside the mould, while the hydraulic station holds the head pressure steady across each cycle. These two parameters must be matched to the buyer’s local aggregate grading and cement content. A mix designed for river sand behaves differently under vibration than one built on crushed stone dust, and the PLC control system allows operators to adjust cycle timing to suit the material actually arriving at the hopper.
The Cost of Skipping Line-Level Detail
When a quotation lists only the press, the buyer absorbs the cost of sourcing a separate mixer, designing pallet handling, and wiring a control panel that talks to none of them. Commissioning stretches from days into weeks. Mould changes take longer because no standard tooling interface was specified. Wear parts for the hydraulic station arrive late because the schematic was never shared with the local maintenance team. These are not rare failures — they are the default outcome when a block making machine production line is assembled from separate purchase orders [NEED_CITE: consequences of uncoordinated block plant procurement].
Why Source the Full Line Here
Block machinery is our single focus, so the press, mould, pallet, and handling equipment are specified as one matched system rather than assembled from unrelated suppliers. Configuration is set against the buyer’s actual mix design and target block format, not a catalogue default. The pallet feeder, brick conveyor, and block sweeper ship with the QT6-15 so the turnkey block plant arrives as a coordinated set of stations. Voltage, frequency, and PLC display language are confirmed before production, not discovered on commissioning day. Mould design covers the formats the buyer’s market actually sells, including custom drawings. Installation support extends through operator training and first-replacement wear parts supply.
Documentation & Verification
- Line layout showing station positions and capacity calculation per block format
- Machine specification sheet covering QT6-15 dimensions, power, and cycle range
- Hydraulic and electrical schematics for local maintenance and spare parts sourcing
- Pallet specification matched to curing area dimensions and forklift capacity
- Factory test record on the buyer’s target block format before dispatch
- Voltage, frequency, and PLC language confirmation documented before production
Installation, Commissioning & Support
- Foundation plan accounting for 7 T net weight and 7400×1900 mm footprint of the QT6-15
- Dedicated power circuit sized for 31.25 kW total draw with confirmed voltage and frequency
- Pallet feeder and brick conveyor alignment checked against 850×550×25 mm pallet tolerance
- PLC control system configured to buyer’s language before the first molding cycle
- Operator training on mould change procedure and cycle time adjustment per format
- Wear parts list covering hydraulic seals, vibration motor bearings, and mould liners
Before You Request a Quote
To size this block making machine production line accurately, share your target block formats, daily output target, and the raw materials available locally. Confirm your workshop dimensions, curing area layout, and the forklift you plan to use with 850×550×25 mm pallets. State your site voltage, frequency, and preferred PLC display language so the electrical package matches your grid from day one.
Frequently Asked Questions
Q: How is daily output calculated per block format, and which format does the quoted capacity assume?
A: Each output figure in the spec table is tied to a specific block size and a 15–20 second molding cycle. For example, 9600–13440 pieces per eight-hour shift applies only to the 400×200×200 mm hollow block. Switching to a smaller format changes both pieces per cycle and daily totals, so always ask which format a capacity quote assumes.
Q: Which line stations are included, and which remain optional?
A: The standard package includes the JQ350 mixer, pallet feeder, brick conveyor, block sweeper, and manual hydraulic trolley. Automatic stacking and curing rack handling are available as upgrades. Confirm which downstream stations you need before the quotation is finalized to avoid manual handling gaps.
Q: How must mixer throughput be balanced against press cycle time?
A: The JQ350 must discharge a full batch within the QT6-15 cycle window of 15–25 seconds. If mixing takes longer, the press sits idle. We calculate batch volume against cycle time during the layout stage so the mixer and press stay synchronized without over-specifying motor power.
Q: What voltage and PLC language confirmation is needed before production?
A: Voltage, frequency, and PLC display language must be confirmed in writing before the machine enters the build stage. Mismatched electrical specs delay commissioning and may require a transformer or rewiring on site, adding cost and time after the container arrives.
Q: How is pallet size validated against existing curing racks and forklifts?
A: The 850×550×25 mm pallet must fit the curing rack spacing and the forklift tine width already on site. We ask for rack dimensions and forklift model during the inquiry stage so pallet size is matched deliberately, not chosen by default from a catalogue list.



