
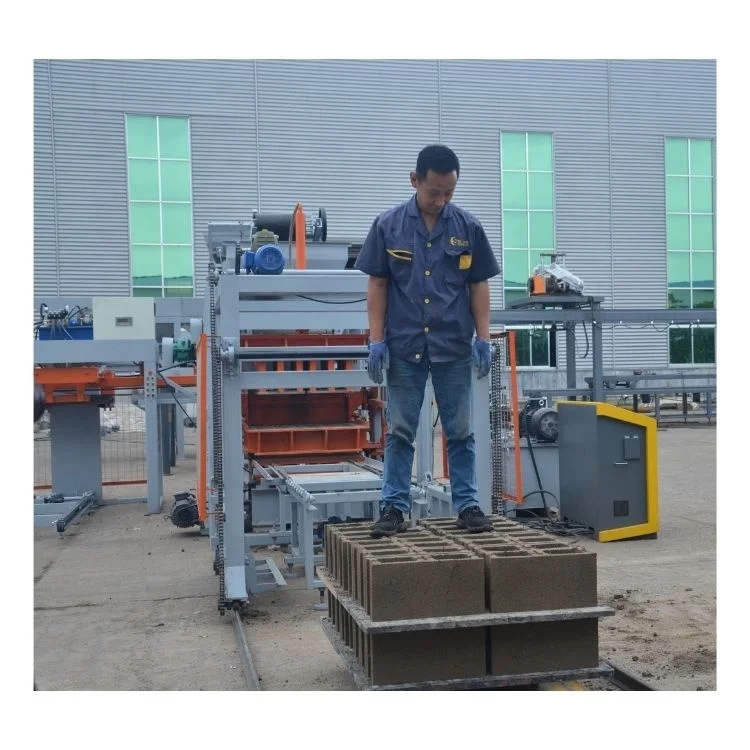
Matched line configuration — the QT6-15 press is specified alongside its mixer, pallet feeder, and stacker so that upstream and downstream stations never bottleneck the 15–20 s molding cycle.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT6-15 |
| Product Type | Automatic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 7350×1780×2950 mm |
| Rated Pressure | 16 MPa |
| Main Vibration | Platform vibration |
| Vibration Frequency | 4600 r/min |
| Pallet Size | 880×700 mm |
| Molding Cycle | 15–20 s |
| Overall Power | 30.5 kW |
| Voltage & Frequency | Configurable to buyer site supply (basis to be confirmed) |
| Control System | PLC-based, language configurable before dispatch |
| Raw Materials | Crushed stone, sand, cement, fly ash, cinder, slag, gangue, gravel, perlite |
| Applied Products | Hollow blocks, solid blocks, paving stones, kerbstones, interlocking blocks, grass blocks, slope blocks |
| Output Capacity | 1080 pcs/h based on 400×200×200 mm hollow block, 6 pcs/mould, 16–20 s cycle |
| Output Capacity | 2800 pcs/h based on 240×115×90 mm porous brick, 14 pcs/mould, 15–18 s cycle |
| Output Capacity | 6800 pcs/h based on 240×115×53 mm standard brick, 30 pcs/mould, 14–17 s cycle |
| Automation Level | Automatic (pallet handling, stacking, and cubing level to be confirmed per line layout) |
| Standards | CE, SGS, ISO 9001 |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for masonry walls | Crushed stone, sand, cement, and fly ash blends |
| Paving stone manufacturing for roads and squares | Hard aggregate with face mix layer option |
| Interlocking block production for landscaping | Cement-stabilized gravel and slag mixes |
| Porous brick runs for building infill | Lightweight aggregate and cinder blends |
| Kerbstone and edger production for municipal works | High-strength concrete with coarse aggregate |
Why Quoted Cycle Times Rarely Match Real Daily Output on a QT6-15 Block Making Machine Production Line
A press is only as fast as the slowest station feeding it or taking pallets away.
I once watched a QT6-15 block making machine production line sit idle for four seconds every cycle because the mixer discharged slower than the press demanded. The pallet feeder had no buffer, and cured blocks piled up at the line end with no stacker to clear them. The brochure said 1080 hollow blocks per hour, but the plant never crossed 700 [NEED_CITE: throughput loss from mismatched station cycle times]. The press was not the problem — everything around it was.
How Station Sequencing Determines Actual Throughput
The QT6-15 block making machine completes a molding cycle in 15–20 seconds. That means the mixer must deliver a fresh batch to the hopper within that same window, the pallet feeder must index a clean pallet into position, and the wet-block conveyor must carry the loaded pallet away before the next press stroke. If any one of these stations runs even a few seconds slow, the press idles and daily output drops. Line layout must calculate each station’s duty cycle against the press rhythm, not against a standalone catalogue figure.
Pallet Flow and Curing Area Coordination
The 880×700 mm pallet size on this press dictates curing rack spacing, forklift fork width, and the stacker magazine dimensions. I have seen plants where pallets came off the line faster than the forklift could shuttle them to the curing yard, causing a jam at the conveyor exit [NEED_CITE: pallet bottleneck in block curing logistics]. Before the line is finalized, the buyer’s existing curing area layout and material-handling equipment must be surveyed so that pallet specification and stacker capacity align with what the site can actually absorb.
Reading the Specs That Actually Matter for Line Balance
Platform vibration at 4600 r/min paired with 16 MPa hydraulic pressure demands a consistent mix from the batching station — any variation in moisture or aggregate grading shows up immediately as density variation across the pallet. The 30.5 kW overall power draw means the electrical supply must sustain continuous motor starts across the press, mixer, and conveyor drives without voltage sag. Pallet size at 880×700 mm is non-negotiable once curing racks are built, so confirming this dimension against site infrastructure prevents costly rack modifications after installation. Molding cycle ranges from 14 to 20 seconds depending on block format, and every upstream station must be sized for the shortest cycle in the buyer’s product mix, not the longest.
The Hidden Cost of Specifying the Press Alone
Quoting the QT6-15 without its supporting stations leads to predictable failures. A mixer that is too small forces the press to wait for mix, cutting daily output well below the stated capacity. A pallet feeder without a buffer magazine causes the press to miss beats every time a pallet jams or arrives late. No stacker means workers manually haul wet pallets, increasing breakage and limiting how fast the line can safely run [NEED_CITE: manual pallet handling breakage rates]. These gaps do not appear on the machine spec sheet — they appear on the plant floor during the first week of production.
Why Sourcing the Full Line from One Supplier Matters
Block machinery as a single focus means the press, moulds, pallets, and handling equipment are specified as one matched system rather than assembled from separate vendors. Configuration is set against the buyer’s actual mix design and local aggregate, not a catalogue default. Mould design covers the formats the buyer’s market actually sells, including custom drawings to buyer specifications. Automation level is selectable, so a plant can start with semi-automatic pallet handling and add a stacker later. Installation support includes operator training so the crew understands station sequencing from day one.
Documentation & Verification
- Line layout drawing with capacity calculation stated per block format
- Machine specification sheet with confirmed pallet size and power rating
- Mould drawing and format list matching buyer target products
- Hydraulic and electrical schematic for on-site maintenance reference
- Voltage, frequency, and PLC display language confirmation before production
- Factory test record on buyer’s specified block format before dispatch
Installation, Commissioning & Support
- Foundation pad sized for 7350×1780 mm footprint with vibration isolation
- Dedicated electrical circuit rated for 30.5 kW continuous draw plus mixer and conveyor loads
- Press arrives partially assembled; on-site alignment of platform and mould frame required
- PLC language and voltage confirmed before first power-on during commissioning
- Operator training covers mould change procedure, pallet feeder adjustment, and daily greasing points
- Wear parts list includes hydraulic seals, vibration springs, and mould liner plates
What to Include in Your Inquiry
Share the block formats your market sells, the daily volume you need per format, and the raw materials available locally. Confirm the voltage and frequency at your site, the PLC display language your operators read, and whether your curing area and forklift are already in place. If you have an existing mixer or conveyor, tell us the model so we can verify it matches the press cycle.
Frequently Asked Questions
Q: How is daily output calculated when the QT6-15 is part of a full line with mixer, pallet feeder, and stacker?
A: Output is stated per block format with its specific mould cavity count and cycle time — for example, 1080 hollow blocks per hour based on a 400×200×200 mm block with 6 cavities and a 16–20 second cycle. Daily figures assume an eight-hour shift and a line where every supporting station keeps pace with the press.
Q: Which supporting stations are included in the quotation and which are optional?
A: The quotation spells out every station from raw material feeding through stacking and cubing. Items such as automatic stackers, curing rack systems, and cubing machines are listed separately so buyers can see which are included and which are optional add-ons for future expansion.
Q: How do we match pallet size to our existing curing racks and forklift?
A: The QT6-15 uses 880×700 mm pallets. Before the order is finalized, we confirm that this dimension fits your curing rack spacing and that your forklift fork width can handle loaded pallets safely. If your racks are already built, pallet specification is locked to match.
Q: What voltage, frequency, and control language will be confirmed before shipment?
A: Voltage and frequency are confirmed against your site electrical supply before production starts. PLC display language is agreed at the same stage so operators can read alarms and menus on day one. Both items appear on the final specification sheet signed off before dispatch.
Q: How do we plan the factory footprint so every station connects without the press waiting?
A: We provide a line layout drawing showing the position of the mixer, pallet feeder, press, wet-block conveyor, and stacker relative to each other. The layout accounts for pallet return path, operator walkways, and curing yard access so station cycle times stay synchronized.



