
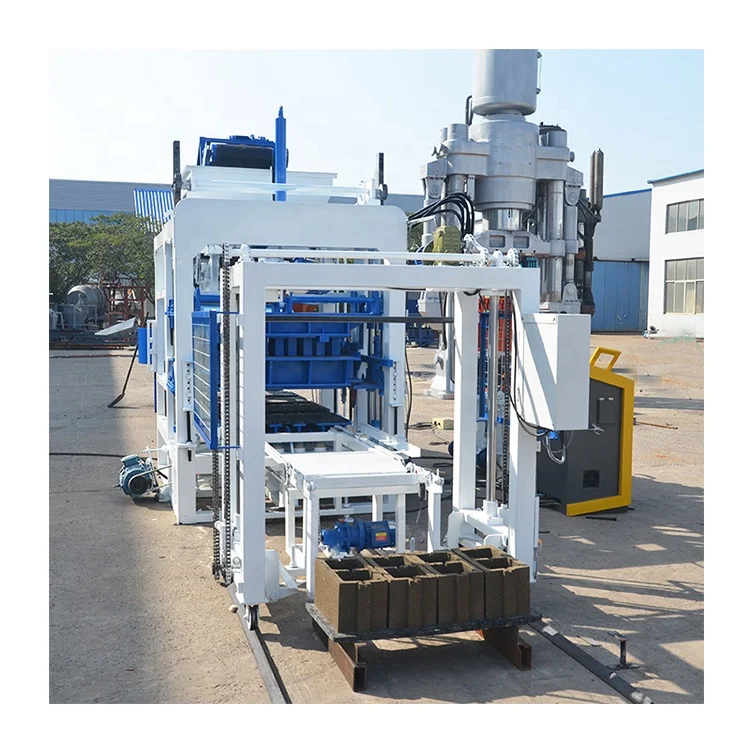
Line-matched configuration — The QT4-18 concrete block making machine production line arrives with JQ350 mixer, pallet feeder, brick conveyor and block sweeper already specified as one system, so the press is not left waiting for upstream feeding or downstream handling to catch up.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Automatic Hydraulic Concrete Block Making Machine |
| Model | QT4-18 |
| Overall Dimensions (L×W×H) | 3900×1600×2300 mm |
| Molding Cycle | 15–25 s |
| Vibration Force | 40–50 kN |
| Rated Power | 24 kW |
| Mixer Model | JQ350 |
| Pallet Size | 850×550×25 mm |
| Net Weight | 3 T |
| Control System | PLC control system |
| Hydraulic Station | Included (high pressure, stable operation) |
| Included Equipment | Block making machine, hydraulic station, PLC control system, pallet feeder, brick conveyor, block sweeper |
| Free Accessories | Manual hydraulic trolley, spare parts and tools |
| Output Capacity (400×200×200 mm hollow block) | 1200–1680 pcs/h |
| Output Capacity (400×150×200 mm hollow block) | 1800–2400 pcs/h |
| Output Capacity (240×115×53 mm solid brick) | 3240 pcs/h (basis not stated in source) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for building walls | Crushed stone, sand, cement, fly ash |
| Solid brick production for masonry | Sand, cement, dust |
| Paver production for walkways and yards | Crushed stone, sand, cement |
| Curbstone production for road edges | Crushed stone, sand, cement |
| On-site or small-to-medium block plant production | Locally available aggregates |
What "15–25 Second Cycle" Means When the Mixer Cannot Keep Up
The press cycle is only the heartbeat; the rest of the concrete block making machine production line must breathe at the same rate.
I have stood on shop floors watching a block press sit idle for eight seconds per cycle simply because the JQ350 mixer discharge gate was too small, or the pallet feeder jammed on warped boards. The QT4-18 molding cycle of 15–25 s sets the rhythm, and every station upstream and downstream must match it or the quoted capacity becomes fiction. Buyers who focus only on press speed often discover the bottleneck was never the press at all [NEED_CITE: line synchronization principles in block manufacturing].
Matching Every Station to the 15–25 s Rhythm
The JQ350 mixer must discharge a full batch within the press cycle window. If mixing takes 45 s but the press finishes every 20 s, the press waits. This concrete block making machine production line pairs the QT4-18 with a mixer sized to the same throughput, and the pallet feeder is timed to deliver a fresh board the moment the press opens.
Where Bottlenecks Hide in a Block Line
Downstream, the brick conveyor must clear finished blocks before the next cycle ejects onto the same pallet slot. The block sweeper cleans the pallet return path so warped or debris-covered boards do not stall the feeder. Each of these stations is included in the QT4-18 package, which removes the integration guesswork when assembling the line from separate suppliers [NEED_CITE: common integration failures in multi-supplier block lines].
Reading the Specs That Actually Matter
The vibration force of 40–50 kN works with the hydraulic station to compact the mix into the mould cavity. Higher vibration alone does not guarantee block strength; the pressure and vibration must suit the buyer’s specific aggregate gradation and cement content. The 850×550×25 mm pallet size dictates curing rack spacing and forklift tine width, so confirming these dimensions against existing site equipment avoids costly pallet replacement after arrival. The PLC control system governs cycle timing, and the display language must be confirmed before production begins so operators can read fault codes without guesswork.
The Cost of Ignoring Line Synchronization
When a buyer sources the press alone and adds a mixer later, the mismatch often surfaces during commissioning. The press idles, hourly output drops, and the blame shifts between suppliers. Pallet feeders from a different vendor may use a different sensor protocol, causing intermittent stops that operators attribute to the press itself. These problems are not mechanical failures; they are integration gaps that a matched-line approach eliminates before the equipment leaves the factory [NEED_CITE: multi-vendor integration issues in block plants].
Why Procure the Line as One Package
Block machinery is the single focus here, so the QT4-18 press, JQ350 mixer, pallet feeder, conveyor and sweeper are specified as one system rather than assembled from separate catalogues. The configuration is set against the buyer’s actual mix design and local aggregate, not a default setting. Mould design covers the formats the buyer’s market sells, including custom drawings when standard moulds do not match. Automation level is selectable, so a buyer can begin with the included pallet feeder and add automatic stacking later as volume grows. Installation support includes operator training on the PLC interface and hydraulic station maintenance.
Documentation & Verification
- Line layout drawing showing station positions and material flow for the QT4-18 footprint
- Capacity calculation sheet stating output per block format with cycle time assumptions
- Pallet specification matched to buyer’s curing rack spacing and forklift dimensions
- Hydraulic and electrical schematic for the 24 kW rated power circuit
- Voltage, frequency and PLC display language confirmation before production
- Factory test record on buyer’s target block format before dispatch
Installation, Commissioning & Support
- Floor space planning around the 3900×1600 mm press footprint plus mixer and conveyor run
- Dedicated power circuit for the 24 kW rated load with voltage and frequency confirmed pre-shipment
- Pallet feeder alignment checked against 850×550×25 mm pallet tolerance on arrival
- PLC control system parameters set to buyer’s block format and molding cycle during commissioning
- Operator training on mould change procedure and hydraulic station pressure adjustment
- Spare parts kit and manual hydraulic trolley included for first-year maintenance
Preparing Your Inquiry
To size this concrete block making machine production line correctly, share your target block format with dimensions, daily output requirement, and the aggregate materials available at your site. Confirm your workshop floor area, ceiling height, and existing curing rack dimensions so pallet size can be matched. State your local voltage and frequency along with the preferred PLC display language so the control system is configured before the line ships.
Frequently Asked Questions
Q: How is daily output calculated when the line includes mixer, feeder and conveyor?
A: Daily output is calculated from the slowest station in the line, not the press alone. The QT4-18 molding cycle of 15–25 s sets the theoretical maximum, but the JQ350 mixer batch time and pallet feeder speed must be verified against that cycle. The capacity calculation sheet provided with each quotation states the assumed block format and the limiting station.
Q: What happens if the mixer output does not match the 15–25 s molding cycle?
A: The press will idle while waiting for the next batch, reducing actual hourly output below the quoted figure. This is why the concrete block making machine production line includes the JQ350 mixer as a matched component rather than leaving mixer selection to the buyer. If a different mixer is used, its discharge rate must be confirmed during line design.
Q: How should the curing area be sized based on pallet dimensions?
A: The 850×550×25 mm pallet determines rack shelf spacing and aisle width for forklift access. Daily pallet volume is calculated from the target output divided by blocks per pallet. The curing area must hold at least one full day’s production plus buffer space for the curing duration required by the block format and local climate conditions.
Q: Which stations are included and which must be sourced separately?
A: The QT4-18 package includes the block making machine, hydraulic station, PLC control system, pallet feeder, brick conveyor, block sweeper, JQ350 mixer, manual hydraulic trolley and spare parts. Curing racks, forklifts, raw material silos and water supply systems are site-provided. Automatic stacking and cubing systems are available as optional additions.



