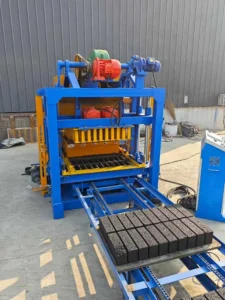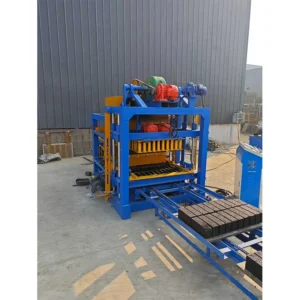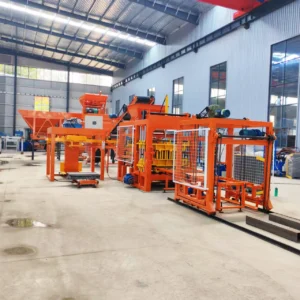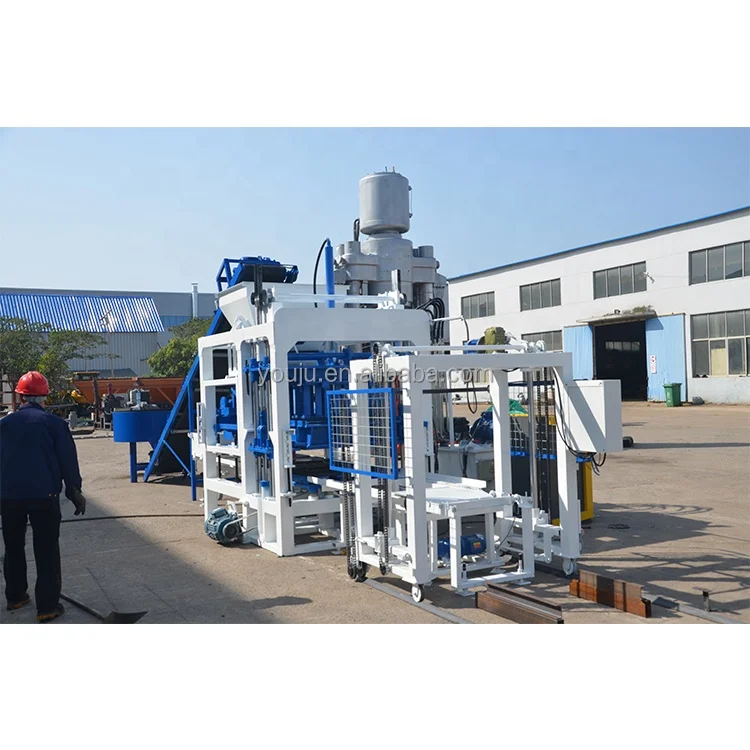
Synchronized Line Flow — The QT4-18 automatic block machine production line connects the mixer, pallet feeder, and stacker so the press cycle never waits on upstream or downstream stations.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | Qt4-18 |
| Product Type | Automatic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 2500×1750×2200mm |
| Rated Pressure | 16 MPa |
| Vibration Form | Platform Vibration |
| Pallet Size | 950×550mm |
| Molding Cycle | 18–25s (basis depends on block format and mix) |
| Overall Power | 27.5 kW |
| Control System | PLC control with frequency converter |
| Electrical Components | Schneider brand components (source value — verify against final bill of materials) |
| Mould Lifting Mechanism | Double-sided synchronous gears |
| Pallet Feeder Power | Hydro-cylinder driven |
| Net Weight | (basis not stated in source — confirm by configuration) |
| Certification | (basis not stated in source — confirm export market requirements) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for commercial and residential walls | Crushed stone, sand, cement, and fly ash aggregates |
| Solid load-bearing block manufacturing | Dense concrete mixes with local gravel |
| Paving block and interlocking brick runs for landscaping | High-strength face-mix or colored concrete blends |
| Kerbstone and porous brick production | Permeable aggregate blends with controlled moisture |
Why the Mixer Becomes the Real Bottleneck on a Turnkey Block Making Line
If the pan mixer cannot discharge a batch within the press cycle window, every downstream station stands idle.
I once configured a Qt4-18 for a client who assumed the mixer was simply an accessory to the press. The JQ500 pan mixer ran fine on paper, but the belt conveyor speed and batching intervals were never timed against the 18–25s molding cycle. Within the first shift, the press sat empty between every third cycle while the crew waited for the next batch. That is not a machine problem — it is a line synchronization failure, and it happens more often than buyers expect when the turnkey block making line is quoted as individual pieces rather than a timed sequence. [NEED_CITE: common causes of idle time in concrete block production lines]
How the Stations Connect Around the Press
The automatic block machine production line flows through a defined sequence: raw material batching into the JQ500 pan mixer, discharge onto the 8-metre belt conveyor, delivery into the hopper above the press, molding on the vibrating platform, and transfer of finished products onto the block receiver conveyor. Each station has its own timing envelope. The PLC with frequency converter coordinates these intervals so the operator sees a single dialogue with the entire line rather than switching between isolated controls.
Where Pallet Handling Defines True Daily Output
The pallet feeder uses a hydro-cylinder to push fresh pallet*ting the pressed block onto the receiver conveyor. This dual-action design collapses what would otherwise be two separate motions into one. When the stacker and block clamper are included in the scope, the cured blocks move off the pallet and onto the trolley without manual lifting — which matters because a crew stacking by hand will set the pace of the whole turnkey block making line regardless of how fast the press can cycle.
Reading the Specifications That Actually Matter
The 16 MPa rated pressure and platform vibration work together: hydraulic pressure compacts the mix while vibration settles fine aggregate into voids, and both must be matched to the buyer’s local stone grading and cement ratio. A mix that is too dry will not consolidate under vibration alone, while one that is too wet will slump before the pallet leaves the platform. The 950×550mm pallet size sets the curing yard grid spacing and the forklift tine width the buyer will need on site. The double-sided synchronous gear lift ensures the mould box rises evenly, preventing drag marks on freshly pressed block faces — a detail that becomes visible the moment surface finish matters to the buyer’s market. [NEED_CITE: relationship between hydraulic pressure and vibration force in block compaction]
What a Missing Conveyor Quotation Costs on Site
When the block receiver, stacker, and trolley are left off the initial quotation, the buyer discovers mid-installation that pressed blocks are accumulating at the end of the press with nowhere to go. Crews end up hand-stacking green blocks that are not yet cured, causing edge damage and inconsistent quality. The cost is not just the conveyor added later at a higher price — it is the first two weeks of production lost to broken and chipped output that never reaches the customer. [NEED_CITE: on-site losses from incomplete block handling scope]
Why This Line Is Specified as One Matched System
The mixer capacity, conveyor speed, and stacker cycle are selected against the Qt4-18 press timing, not pulled from a generic catalogue. The configuration accounts for the buyer’s actual aggregate and target block format so that the 18–25s molding cycle produces blocks that meet local strength standards. Moulds are designed for the formats the buyer’s market sells, and pallet specifications are confirmed against the curing area dimensions before production begins. Voltage, frequency, and PLC display language are locked in before the factory test, preventing commissioning standoffs on arrival. The line can start at a semi-automatic conveying level and accept stacking or batching upgrades later without replacing the press.
Documentation & Verification
- Line layout showing station-to-station timing for your block format
- Capacity calculation stating which block size the 18–25s cycle assumes
- Pallet specification matched to your curing yard and forklift dimensions
- Hydraulic and electrical schematics with confirmed voltage and frequency
- Factory test record on your target mix and block format before dispatch
- Wear parts and mould list with part numbers for first replacement orders
Installation, Commissioning & Support
- Foundation plan accounts for the 2500×1750mm press footprint and vibration isolation requirements
- Dedicated power circuit sized for the 27.5 kW overall load with correct voltage and phase confirmed
- Belt conveyor length adjustable between 6m and 8m to match existing site layout
- PLC language and frequency converter parameters set before dispatch to match operator proficiency
- Mould change training covers double-sided gear synchronization to prevent uneven block surfaces
- Hydraulic station and pan mixer maintenance schedule provided with interval-based part ordering
Before You Request a Quotation
To size this automatic block machine production line accurately, share the block formats your market currently sells, the daily volume you plan to run, and the local aggregate and cement types available on site. Confirm the voltage and frequency at your facility, the PLC display language your operators need, and the dimensions of your curing yard so the pallet and conveyor scope can be set before production.
Frequently Asked Questions
Q: How is the daily output of the QT4-18 line calculated, and which block format is that figure based on?
A: The molding cycle ranges from 18 to 25 seconds, but the actual daily output depends entirely on which block format is being produced — a hollow block takes a different cycle and pallet coverage than a paving stone. We calculate capacity per format and state it in the line layout, so the number you plan against reflects the product you actually sell.
Q: How do the mixer and conveyor match the press cycle to avoid bottlenecks?
A: The JQ500 pan mixer batch volume and the belt conveyor speed are timed so that a fresh mix reaches the hopper before the current charge is exhausted. If the buyer’s aggregate requires a longer mixing time, we adjust conveyor length or add a holding hopper rather than letting the press wait between cycles.
Q: Which stations can be upgraded after the base line is installed?
A: The base configuration includes mixer, pallet conveyor, press, block conveyor, and hydraulic station. Stations such as automatic stacking, curing rack handling, and cement silo batching can be added later without replacing the press or altering the PLC core program, allowing the line to grow with production demand.
Q: How are pallet size and curing yard layout coordinated before shipment?
A: The 950×550mm pallet dictates the spacing of curing racks and the forklift specifications needed on site. We confirm the buyer’s existing yard dimensions and forklift tine width before finalizing pallet material and quantity, so the curing side does not become a constraint once blocks start arriving.
Q: When must voltage, frequency, and PLC language be confirmed?
A: These parameters must be locked in before production begins, not at shipment. The frequency converter, motor windings, and PLC display are all configured during assembly, and changing them after the factory test adds lead time and cost — so we confirm them at the quotation stage.