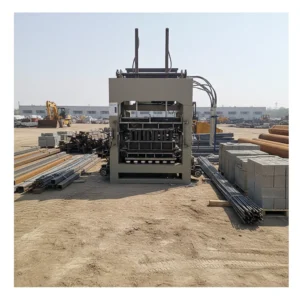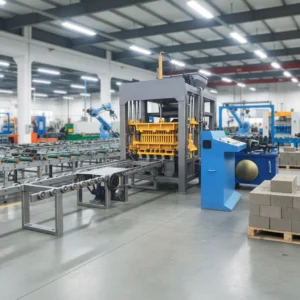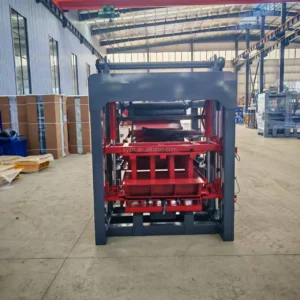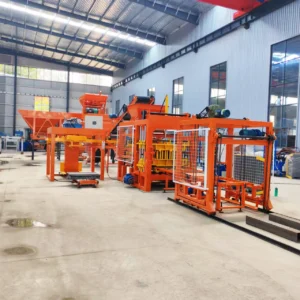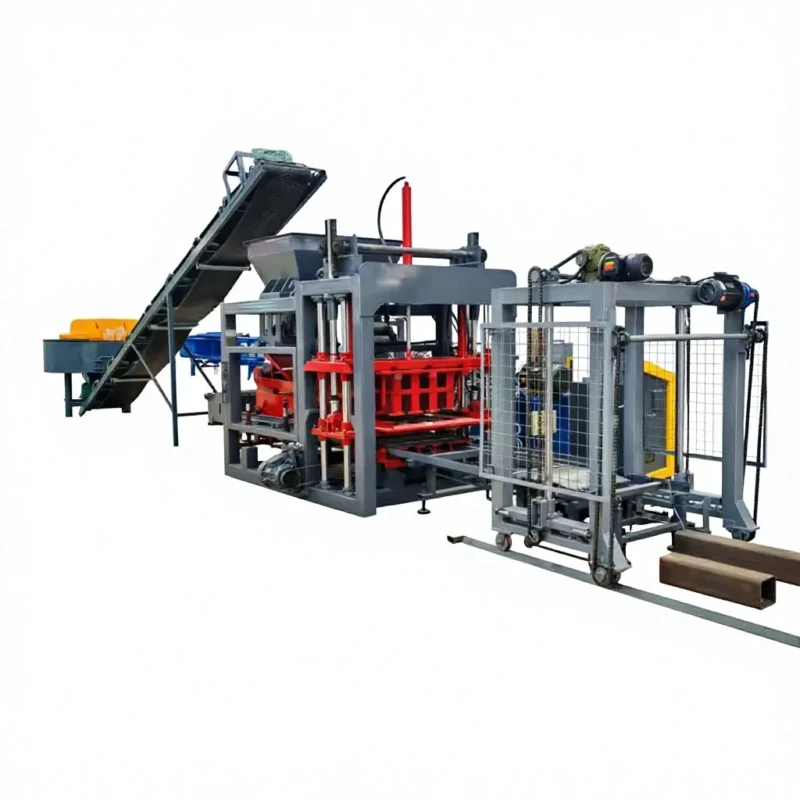
Balanced Line Synchronization — Every station from raw material feeding to stacking is specified as one matched system, ensuring the QT4-15A press never waits for pallets or mix.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT4-15A |
| Product Type | Fully Automatic Hydraulic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 4100×1600×2600 mm |
| Total Mass | 4 T |
| Rated Pressure | 16–21 MPa |
| Vibration Form | Platform Vibration |
| Vibration Frequency | 4200 r/min |
| Vibration Force | 55 kN |
| Pallet Size | 880×550 mm |
| Molding Cycle | 25–30 s (basis not stated in source — confirm block format / material / thickness) |
| Overall Power | 18.45 kW |
| Demolding Method | Hydraulic |
| Recommended Factory Area | 300 m² |
| Automation Level | Fully automatic |
| Warranty | 1 year (excluding spare parts) |
| Loading | 1×40HQ container (for basic equipment) |
Application Suitability
| Application | Material or Output |
|---|---|
| Fixed Block Production Plants | Concrete hollow blocks, solid blocks, and pavers using locally sourced aggregates |
| On-Site Construction Projects | Interlocking blocks, curbstone, and colored pavers for housing developments |
| Concrete Product Manufacturers | Fly ash, gravel, slag, and dust mixtures for various masonry formats |
Why Cycle Times Are Only Half the Story in Block Line Equipment
A quoted molding cycle is useless if the upstream mixer and downstream pallet feeder operate on a different timeline.
I once visited a plant in Peru where the owner was frustrated by his daily output. He had purchased a standalone hydraulic press based on a promising cycles-per-hour figure, but no one had calculated the throughput of the rest of the supporting block making line. The press was sitting idle for fifteen seconds every cycle waiting for the pallet feeder to return a board. By the end of the shift, the loss added up to thousands of unproduced blocks. When planning a block production line equipment setup, the synchronization between the mixer discharge, the press vibration, and the stacking station is more critical than the press specifications in isolation [NEED_CITE: industrial line synchronization principles].
Integrating the Press with Upstream Feeding Stations
The QT4-15A operates with a platform vibration frequency of 4200 r/min and a force of 55 kN. These figures dictate how quickly the mold can be filled and compacted, but they also demand that the raw material feeding station delivers the exact volume of mix within that window. If the mixer capacity is too small or the conveyor belt speed is too slow, the press hopper starves, and the vibration cycle begins with an incomplete mold. A matched supporting block making line ensures that the material flow rate is calculated against the 25–30 s molding cycle, keeping the press continuously fed without overflow.
Synchronizing Pallet Circulation and Downward Stacking
Once the block is formed, the hydraulic demolding system releases it onto the 880×550 mm pallet. The speed at which this pallet is transported to the curing area and a fresh pallet is returned to the press determines the actual daily volume. In many block production line equipment installations, the bottleneck is not the press but the manual handling or undersized stacking robots that cannot keep pace with the 4 T machine’s output. We configure the pallet return loop and automatic stacker to match the press’s maximum rhythm, preventing the wet blocks from sitting on the press table and blocking the next cycle.
How Vibration and Pressure Match Your Local Aggregate
The relationship between the 16–21 MPa hydraulic pressure and the 55 kN vibration force must be tuned to the specific density of your raw materials. Whether you are using heavy crushed stone or lighter fly ash and slag, the energy required to compact the mix into a consistent hollow block varies. If the vibration force is too high for a delicate mix, the block may crack; if the pressure is too low for coarse gravel, the density will be insufficient for structural standards. Our line configuration starts with your local material profile to set these parameters correctly [NEED_CITE: concrete block density standards].
The Cost of Ignoring Line-Wide Throughput
When a buyer focuses only on the press and treats the rest of the line as an afterthought, the result is often a workshop full of bottlenecks. I have seen plants where the curing racks were designed for a different pallet size, forcing operators to manually transfer every single block off the machine pallets and onto the racks. This extra handling not only slows down the entire block production line equipment flow but also damages the green blocks before they have cured. In other cases, the voltage or PLC language was never confirmed for the local grid, leaving the automatic stacker in manual mode for months while waiting for a technician [NEED_CITE: common block plant commissioning delays].
Why We Specify the Entire System Together
Our approach to block machinery is to treat the press, the molds, the pallets, and the handling equipment as a single engineering problem. We do not quote a QT4-15A without first reviewing the layout of your curing area and the capacity of your existing forklifts. This ensures that the 880×550 mm pallets we supply will fit your racks and that the line layout fits within your available 300 m² footprint. From the raw material silo to the final cubing station, every component is selected to support the specific block formats you intend to sell.
Documentation & Verification
- Line layout and capacity calculation stating the assumed block format.
- Hydraulic and electrical schematics for the full supporting line.
- Pallet specification matched to curing rack dimensions.
- Factory test record on your specific mix design.
- Voltage, frequency, and PLC language confirmation sheet.
Installation, Commissioning & Support
- Foundation plan for the 4100×1600 mm press footprint and pallet loop.
- Electrical load check for the 18.45 kW total power requirement.
- On-site calibration of the 16–21 MPa hydraulic system.
- Training on mold change procedures and safety interlocks.
- Wear parts list for hydraulic seals and vibration mounts.
- Commissioning of the PLC in the local operator language.
What We Need to Size Your Line
To provide a quotation that reflects the real-world output of your block production line equipment, we need to know the specific block formats you plan to produce and the daily volume target. Please share details about your local raw materials, such as the type of aggregate and cement available, and the dimensions of your proposed factory floor. It is also helpful to know your local voltage and frequency standards so we can specify the correct motors and control gear from the start.
Frequently Asked Questions
Q: How is the capacity of the QT4-15A line calculated?
A: Capacity is calculated by taking the molding cycle—typically 25–30 seconds—and multiplying it by the number of blocks per mold for a specific format. However, this figure is only valid if the entire supporting block making line, including the mixer and pallet feeder, can sustain that rhythm without interruption. We provide a detailed layout showing the throughput of every station.
Q: How do feeding stations match the press cycle?
A: The raw material batcher is sized to deliver a fresh mix to the press hopper before the current cycle finishes. If the press cycles every 25 seconds, the mixer and conveyor must be capable of discharging the required volume within that same window to prevent the press from idling while waiting for material.
Q: What determines the right pallet size and material?
A: The 880×550 mm pallet size is chosen based on the mold configuration, but the material and thickness depend on your curing environment and handling equipment. We check the dimensions of your existing curing racks and the fork spacing of your forklifts to ensure the pallets move smoothly from the press to the yard.
Q: How are stacking and curing integrated into the line?
A: We design the pallet return system and stacking station to handle the maximum output of the QT4-15A. Wet blocks are transferred automatically to the curing racks or a stacking area, minimizing manual handling that can damage the product and ensuring the press table is cleared instantly for the next cycle.
Q: What technical details must be confirmed before shipping?
A: We must confirm the local voltage and frequency, as well as the language for the PLC display. We also need to verify the specific mix design and block formats to ensure the hydraulic pressure and vibration settings are calibrated correctly for your materials upon arrival.