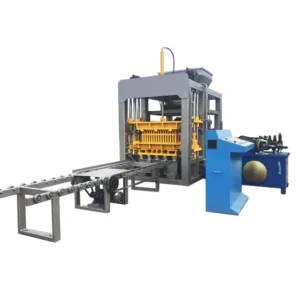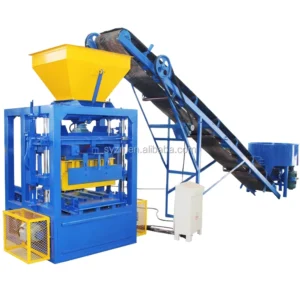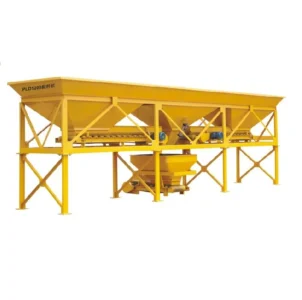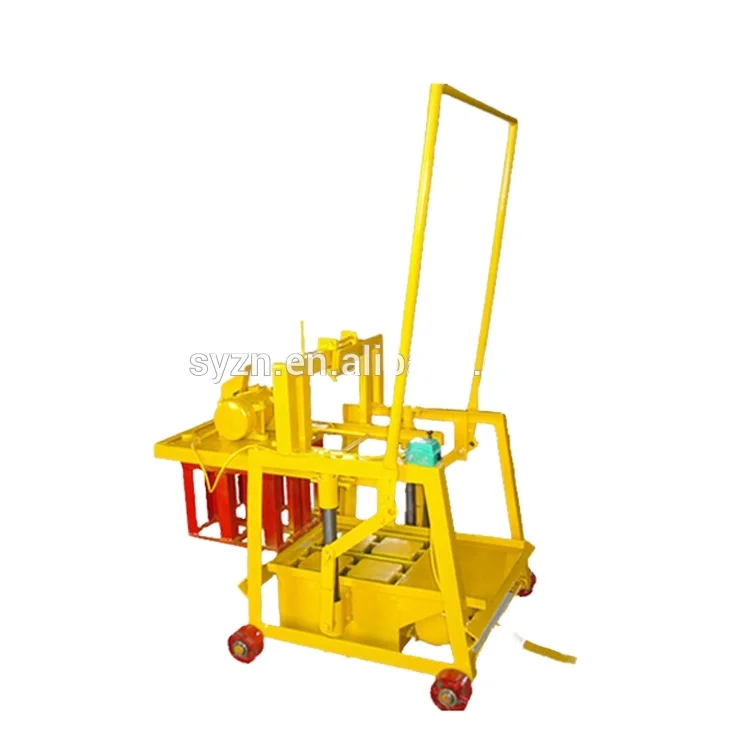
Complete Line Synchronization — every station from mixer to curing is specified as one matched system, so a mobile egg-laying press never sits idle waiting for concrete.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QMJ2-45 |
| Product Type | Mobile Egg-Laying Block Making Machine |
| Overall Dimensions (L×W×H) | 1000 × 800 × 1300 mm |
| Net Weight | 215 kg |
| Rated Power | 1.5 kW |
| Voltage & Frequency | Configurable to buyer’s local supply |
| Control System | Manual operation |
| Vibration Type | Mold box vibration |
| Hydraulic Pressure | Not applicable (manual egg-laying type) |
| Mould Format | 400 × 200 × 200 mm, 2 pcs per mold |
| Cycle Time | 45 s per mold cycle |
| Output Capacity | 1000 pcs/day (basis not stated in source — confirm block format and shift length) |
| Pallet System | Not applicable (egg-laying / no pallet required) |
| Basic Equipment Included | JQ350 Mixer |
| Automation Level | Manual / mobile |
| Warranty | 1 year (wearing parts excluded) |
Application Suitability
| Application | Material or Output |
|---|---|
| On-site hollow block production at housing projects | Cement-based concrete with locally sourced aggregate |
| Small-scale home-business block manufacturing | Standard concrete mix, 400 × 200 × 200 mm hollow blocks |
| Remote or temporary construction sites | Fresh concrete transported from JQ350 mixer to laying position |
| First block operation for entrepreneurs | Low-volume output without fixed plant infrastructure |
What "1000 Blocks per Day" Actually Requires from the Rest of Your Line
A mobile egg-laying machine only meets its output claim when mixer discharge, concrete transport, and curing space all keep pace with a 45-second mold cycle.
The QMJ2-45 completes one mold cycle — producing two 400 × 200 × 200 mm hollow blocks — every 45 seconds. That rhythm sounds manageable until you map it against upstream and downstream stations. A JQ350 mixer must discharge a fresh batch before the press finishes its current cycle; otherwise the operator stands idle and the daily count drops well short of any headline figure. On the downstream side, freshly laid blocks need level ground, adequate spacing, and a curing routine that does not bottleneck the next laying pass. I have visited sites where the mobile block making machine production line supporting equipment around the press was an afterthought, and the entire operation ran at a fraction of expected throughput [NEED_CITE: common causes of output shortfall in mobile block production].
Matching Mixer Batch Size to a 45-Second Press Cycle
The JQ350 mixer included with the QMJ2-45 must deliver a workable batch fast enough to prevent the press from waiting. A 45-second mold cycle means the operator is ready for the next charge of concrete in under a minute. If the mixer is still blending or if the transport method — wheelbarrow, bucket, or small conveyor — introduces delay, cycle time stretches and daily output falls. The entire mobile block making machine production line supporting equipment setup must be walked as a loop: mixer loading time, blending duration, discharge speed, and travel distance to the laying position all feed back into press utilization.
Curing Area Layout and What Happens After Laying
An egg-laying machine deposits blocks directly on the ground, which eliminates pallet cost but creates a different planning requirement. Each block occupies floor space until it reaches handling strength, so the curing footprint grows with every shift. If the site cannot provide enough level, covered area, the operator must stop laying and wait for earlier blocks to cure before reclaiming space. This downstream constraint is where many small operations lose time — the press is ready, but there is nowhere to put the output.
Reading the Specs That Decide Real Output
Mold-box vibration at the QMJ2-45 is the sole compaction mechanism; there is no hydraulic ram supplementing density. That means block strength depends heavily on the mix design — cement content, water-to-cement ratio, and aggregate grading must be tuned to produce adequate green strength the moment the mold lifts off. The 1.5 kW rated power is low enough to run on single-phase supply in many markets, but voltage and frequency must be confirmed before the motor is wound at the factory. A mismatch here leads to overheating or failure to start, delaying commissioning [NEED_CITE: voltage and frequency standards by export market]. The 215 kg net weight keeps the machine portable for on-site movement, but it also means the machine relies on operator technique — steady travel speed and consistent concrete feed — to maintain uniform block quality across a production run.
The Hidden Cost of Treating the Press as an Island
When buyers evaluate a mobile egg-laying machine only by its press specs, the surrounding workflow gaps surface after arrival. No one plans the concrete transport route from mixer to laying line, so workers carry heavy buckets over uneven ground and the 45-second cycle slips to 90 seconds or more. Curing area is improvised on soft soil, causing block breakage during the first days. Spare mold edges and vibration springs are not ordered until the first wear failure halts production entirely. These are not machine defects — they are line-design omissions that turn a capable press into a bottleneck [NEED_CITE: mobile block production workflow audit checklist].
Why Procuring the Full Line Context Matters Here
Block machinery is a single focus at Shandong Shiyue Intelligent Machinery, which means the QMJ2-45 is not quoted as a standalone press but as part of a production loop. Mixer capacity, transport method, and curing layout are discussed before the order is finalized. Configuration is set against the buyer’s actual mix design and local aggregate rather than a catalogue default. Mould formats are matched to what the buyer’s market actually purchases, and custom mould drawings are available for non-standard sizes. Documentation — including a line layout with capacity calculation that names the assumed block format — ships with the machine so the 1000 pcs/day figure can be verified against the buyer’s own shift pattern and target format.
Documentation & Verification
- Line layout and capacity calculation stating the 400 × 200 × 200 mm format assumed
- Machine specification sheet with confirmed voltage and frequency
- JQ350 mixer specification and batch cycle record
- Mold drawing and format list for ordered cavities
- Operation and maintenance manual covering press and mixer
- Wear parts and mold list for first replacement planning
Installation, Commissioning & Support
- Level compacted ground required across the full egg-laying travel path for consistent block height
- Single-phase or three-phase power at confirmed voltage and frequency for the 1.5 kW press motor and mixer
- Machine arrives assembled; verify wheel and handle alignment before first production run
- Mixer-to-press transport route walked and timed during commissioning to confirm cycle match
- Operator training on mold fill technique, vibration timing, and travel speed for uniform block density
- Wear parts list supplied with recommended first-order quantities for springs and mold edges
Before You Send an Inquiry
Share your target block format, the daily output you need per shift, and the raw materials available locally — cement type, aggregate size, and sand source. Include your site voltage and frequency so the motor and mixer can be wound correctly at the factory. If you already own mixing or transport equipment, list those models so the line can be configured around them rather than duplicated.
Frequently Asked Questions
Q: How is the 1000 pcs/day output figure calculated?
A: That figure is based on continuous operation, but the source does not state the assumed block format, shift length, or working rhythm. Confirm with the supplier whether 1000 pcs refers to 400 × 200 × 200 mm hollow blocks produced across an eight-hour shift with uninterrupted mixer supply, then compare against your own production schedule.
Q: Can the JQ350 mixer keep up with the 45-second press cycle?
A: It can, provided the batching routine and concrete transport method are planned as one loop. Mixer loading, blending, discharge, and travel to the laying position must together consume less than 45 seconds. If your site layout introduces long transport distances, consider an additional mixer or a small belt conveyor to close the gap.
Q: What voltage options are available and when must I confirm?
A: Voltage and frequency are configurable to your local supply, but the motor winding is set during manufacturing. Confirm your exact voltage and frequency — single-phase or three-phase — before the order enters production to avoid rewinding delays or commissioning failures on arrival.
Q: What supporting equipment do I need around this mobile machine?
A: Plan for a level curing area large enough to hold each shift’s output until blocks gain handling strength, a method to transport fresh concrete from the mixer to the laying path, and basic manual stacking tools. The press itself requires no pallets, but the surrounding workflow must be designed before production starts.
Q: Can I order custom molds for formats my market sells?
A: Custom mold design to buyer drawings is available. Provide the target block dimensions, wall thickness, and any interlock or face-texture requirements so the mold can be engineered for proper draft angle and vibration transfer within the QMJ2-45 mold box.