
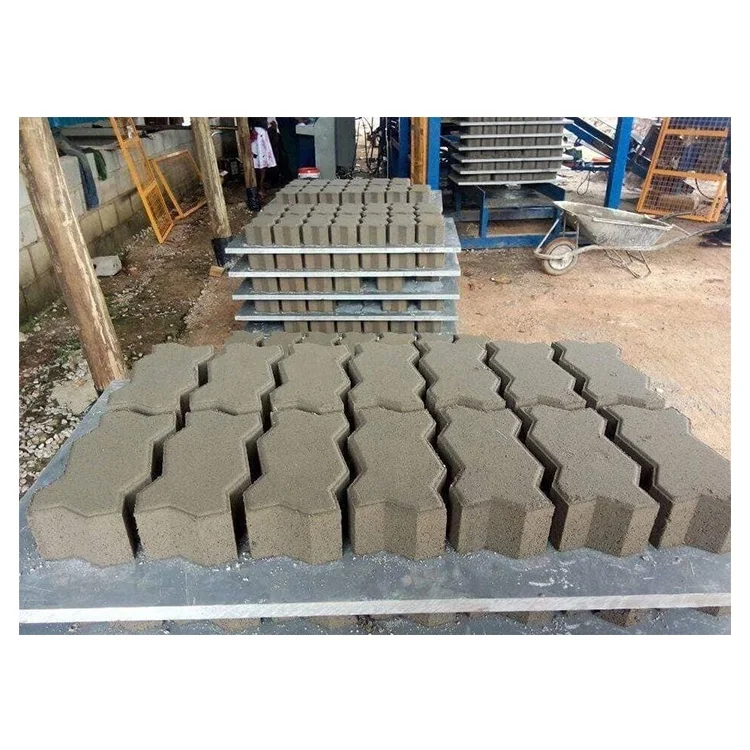
Station-by-station line matching — the QT4-15 block making machine production line is specified so every station from raw material feeding through to stacking keeps pace with the press cycle, preventing the idle time that silently cuts daily output.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT4-15 |
| Product Type | Automatic Hydraulic Concrete Block Making Machine |
| Control System | PLC computer control, fully automatic |
| Vibration Mode | Multiaxis synchronizer vibration (vertically downward) |
| Hydraulic System | High thermal efficiency, low heat productivity |
| Mixer System | Multiaxis forced mixer (adaptable to different raw materials) |
| Guide Bearing | Long-period over-length guide bearing for upper mould and mould box alignment |
| Frame Construction | High-strength steel with special welding technique (vibration shock resistant) |
| Automation Level | Fully automatic |
| Output Capacity (400×200×200mm hollow block) | 900–1,200 pcs/h, 7,200–9,600 pcs/8hr |
| Output Capacity (400×150×200mm block) | 1,080–1,440 pcs/h, 8,640–11,520 pcs/8hr |
| Output Capacity (400×100×200mm block) | 1,440–1,920 pcs/h, 11,520–15,360 pcs/8hr |
| Output Capacity (200×100×60mm paver) | 2,880–3,840 pcs/h, 23,040–30,720 pcs/8hr |
| Output Capacity (240×115×53mm solid brick) | 5,930–6,720 pcs/h, 47,400–53,700 pcs/8hr |
| Molding Cycle | 15–20s |
| Mould Format | 400×200×200 / 400×150×200 / 400×100×200 / 200×100×60 / 240×115×53 |
| Warranty | 1 year (whole machine, excluding spare parts) |
| Voltage & Frequency | (basis to be confirmed before order) |
| PLC Language | (basis to be confirmed before order) |
| Pallet Size | (basis to be confirmed based on mould format) |
| Hydraulic Pressure | (basis to be confirmed against manufacturer catalog) |
| Vibration Force | (basis to be confirmed against manufacturer catalog) |
| Overall Dimensions | (basis to be confirmed against manufacturer catalog) |
| Net Weight | (basis to be confirmed against manufacturer catalog) |
| Rated Power | (basis to be confirmed against manufacturer catalog) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for building construction | 400×200×200mm, 400×150×200mm, 400×100×200mm formats using crushed stone, sand, cement and fly ash |
| Solid brick production | 240×115×53mm standard format from local aggregate and cement blends |
| Paving block and interlocking paver production | 200×100×60mm format with high-density compaction for vehicular and pedestrian surfaces |
| Multi-cellular brick production | Lightweight aggregate or aerated concrete mixes adapted through forced mixer configuration |
| On-site block production for housing projects | Integrated line with mixer, pallet system and handling equipment deployed at project locations |
Why the Mixer Capacity Must Match the Press Cycle
A QT4-15 block making machine production line only reaches its rated output when every upstream station feeds the press without delay.
I once stood on a plant floor in Colombia watching a block machine sit idle for forty seconds every cycle. The press was ready, the mould was clean, the operator was waiting — but the mixer had not finished its batch. The line had been sold as a single unit, yet the mixer capacity had been picked from a catalogue default rather than calculated against the actual cycle time and mould volume. Over an eight-hour shift, that idle gap cost the plant thousands of blocks. [NEED_CITE: cycle time matching across block line stations] When the supporting equipment around a QT4-15 block making machine production line is not scoped station-by-station, the bottleneck simply moves rather than disappears. The quotation may list a mixer, a feeder and a stacker, but if their individual cycle times do not align with the 15–20 second molding cycle, the press spends more time waiting than pressing.
Station Synchronization Across the Full Line
The QT4-15 block making machine production line is built around the principle that every station must complete its task within the press cycle. The multiaxis forced mixer is selected to deliver a fresh batch within the molding window, so the press never waits for material. Raw material feeding, pallet feeding and block stacking are each timed against the same cycle, creating a continuous flow from aggregate infeed to cured product handling.
How the Forced Mixer Adapts to Local Aggregate
Block strength depends on the mix, and the mix depends on what is available locally. The multiaxis forced mixer in this line handles varying aggregate sizes, moisture levels and cement ratios without requiring the buyer to source a specific material grade. This matters because a mixer configured for one type of sand may not properly blend a coarser crushed stone, leading to inconsistent density across the batch. The line is specified around the buyer’s actual raw material profile, not a standard recipe. [NEED_CITE: aggregate variability in concrete block production]
Reading the Capacity Table Without Being Misled
Output figures for the QT4-15 change significantly depending on the block format being produced. A 400×200×200mm hollow block yields 900–1,200 pieces per hour, while a 240×115×53mm solid brick reaches 5,930–6,720 pieces per hour on the same press. The difference comes from mould cavity count and the volume of concrete per cycle, not from any change in the machine itself. When comparing lines, the format behind each capacity figure is the first thing to verify, because a daily output claim based on solid bricks will not hold if your market buys hollow blocks.
What Happens When Line Stations Are Underspecified
A buyer who receives a quotation listing only the press and a generic mixer description may not realize that pallet feeding, stacking and curing rack handling have been left out until the machine arrives. At that point, blocks come off the press and sit on the floor because there is no automated system to move them. [NEED_CITE: block plant commissioning delays from incomplete line scope] The result is a crew of workers handling wet blocks by hand, which damages edges, slows curing and cuts the usable output well below what the press alone could produce.
Why the Supporting Equipment Scope Matters Here
Shiyue approaches the QT4-15 as a complete production line rather than a standalone press. Every supporting station — raw material feeder, mixer, pallet feeder, stacker, curing rack handling — is included in the line layout with its cycle time stated. The mould selection is matched to the buyer’s market formats, and custom mould designs are available when standard sizes do not fit local demand. Automation level is selectable, so a buyer can begin with semi-automatic pallet handling and move to fully automatic stacking later without replacing the press. Voltage, frequency and PLC display language are confirmed in writing before production starts, avoiding the delay of rewiring or reprogramming after the line arrives on site.
Documentation & Verification
- Line layout drawing showing each station and its cycle time matched to the QT4-15 press
- Capacity calculation sheet stating the block format behind every output figure
- Factory test record covering the complete line run, not the press alone
- Voltage, frequency and PLC language confirmation document signed before production
- Mould drawing and format list for every block type included in the quotation
Installation, Commissioning & Support
- Foundation plan and floor space layout provided for the full QT4-15 line including mixer and handling stations
- Electrical schematic with dedicated circuit requirements for the PLC-controlled press and mixer motors
- Machine dismantled for container loading with reassembly sequence documented for on-site crew
- On-site commissioning with parameter setting for the buyer’s specific mix design and block format
- Operator training covering mould change procedure, PLC interface navigation and daily maintenance checks
- Wear parts and mould replacement list provided with the line for first-year procurement planning
What to Prepare Before Requesting a Line Quote
A complete QT4-15 block making machine production line proposal requires information about the production environment and target output. Share the block formats your market demands, the daily volume you need for each format, and the local aggregate and cement types you plan to use. Include your site’s voltage and frequency, the available floor space and ceiling height, and whether you already have forklifts or curing racks that the pallet system must accommodate.
Frequently Asked Questions
Q: How do I verify the real daily output of the complete line for my target block format?
A: Request a capacity calculation that states the output per hour and per eight-hour shift for your specific block format. The figures differ significantly between hollow blocks, pavers and solid bricks on the same press. A line quotation should show which format each number assumes, along with the cycle time and mould cavity count used in the calculation.
Q: Which supporting equipment stations are included, and where must cycle times match so the press does not idle?
A: A complete line includes raw material feeding, mixing, pallet feeding, the press itself, stacking and curing rack handling. Each station must complete its task within the 15–20 second molding cycle. The mixer batch size and discharge speed are the most common mismatch, causing the press to wait for fresh concrete.
Q: Can the line be configured for my local aggregate and mix design?
A: The multiaxis forced mixer is adaptable to different raw material properties, including varying aggregate sizes and moisture levels. The line configuration is set against your actual mix design rather than a default recipe, so block strength and surface finish remain consistent with locally available materials.
Q: What pallet size and material does this line require, and how does that affect my existing curing area?
A: Pallet size is determined by the mould format selected for your production. The pallet material and dimensions must match both the press feeding system and the curing racks or floor space you have available. Confirm your forklift capacity and curing area layout before the pallet specification is finalized.
Q: What is the lead time for the full line including mixer, handling and stacking equipment?
A: Lead time depends on the supporting equipment scope and whether custom moulds are included. A standard line with stock moulds dispatches faster than one with custom format tooling. Request a written arrival estimate that covers every station in the line, not just the press, before placing the order.



