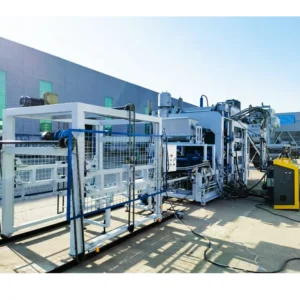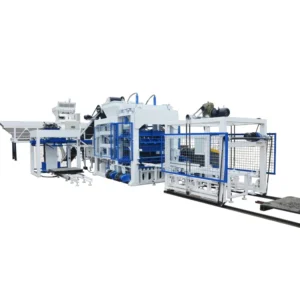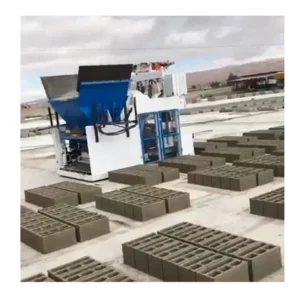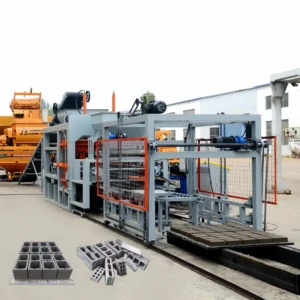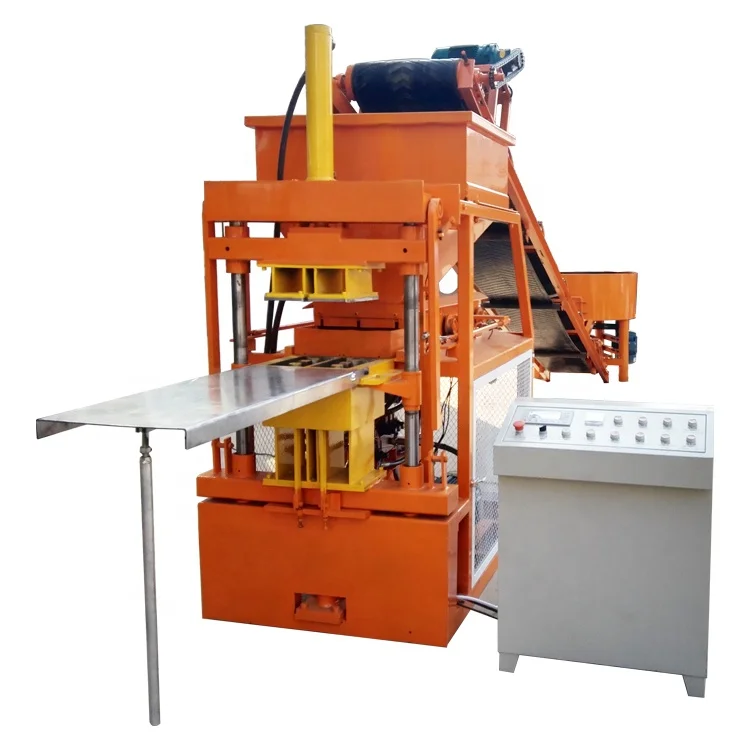
Matched Line Configuration — every station from clay hopper to curing rack is sized against the 10-second press cycle so no equipment sits idle waiting on another.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | LY2-10 |
| Product Type | Hydraulic Interlocking Clay Brick Making Machine |
| Overall Dimensions (L×W×H) | 1300 × 1800 × 2400 mm |
| Net Weight | 1200 kg |
| Power Source | Electric motor or Diesel engine (configurable) |
| Rated Power | 7.5 kW (electric) / 12 HP (diesel) |
| Hydraulic Pressure | 16 MPa |
| Cycle Time | 10 s |
| Output Capacity | 5,760 pcs/day (8 h) (basis not stated in source — confirm block format) |
| Mould Format | 300 × 150 × 100 mm (2 pcs/mould) / 250 × 125 × 60 mm (2 pcs/mould) |
| Pallet Requirement | No pallets required |
| Automation Level | Semi-automatic or Automatic (configurable) |
| Voltage & Frequency | 380 V, 3-phase, 50 Hz (customizable) |
| Raw Material Compatibility | Clay (80–97 %), Cement (6–8 %), Water (~3 %) |
Application Suitability
| Application | Material or Output |
|---|---|
| Interlocking wall brick production | Clay and cement blend, 300 × 150 × 100 mm format |
| Paving and interlock brick for walkways | Clay-cement mix, 250 × 125 × 60 mm format |
| On-site construction block production | Local clay with 6–8 % cement, diesel-powered option |
| Small to mid-scale brick plant startup | Semi-automatic line with manual stacking and curing |
Why "720 Bricks per Hour" Means Nothing Without the Rest of the Line
A press that cycles every 10 seconds only hits its rated throughput when the mixer, feeder, and curing area keep the same pace.
I once stood in a Brazilian plant watching an automatic brick press sit idle for four seconds every cycle because the mixer discharged too slowly. The owner had paid for a high-speed press but never checked whether the upstream stations could match it. Over an eight-hour shift, those lost seconds added up to a noticeable gap in daily output. When you evaluate a hydraulic interlocking clay brick making machine production line, the press cycle time is only the starting point — every station upstream and downstream must be calculated against that same rhythm [NEED_CITE: line balancing principles in block production].
Stations That Must Keep Pace with a 10-Second Cycle
The LY2-10 completes one pressing cycle every 10 seconds, producing two interlocking bricks per mould. That rhythm sets the ceiling for the entire hydraulic interlocking clay brick making machine production line. The raw material feeder must deliver a consistent batch to the mixer within that same window, and the mixer must discharge a fully blended clay-cement charge before the press calls for the next load. If any station lags, the press waits — and the daily output drops below the theoretical figure on the quotation.
Removing Pallets from the Material Flow
Because this press forms interlocking bricks without pallets, three stations disappear from the line entirely: pallet feeding, pallet return, and pallet storage. That simplification shrinks the line footprint and cuts the handling equipment budget. What replaces them is a direct wet-brick transfer path from the press to the curing area — typically a short conveyor or manual cart run. Sizing that transfer path correctly is critical; if the curing rack is too far or too small, finished bricks pile up at the press outlet and the operator has to stop the machine to clear space [NEED_CITE: curing area sizing for no-pallet block lines].
Reading the Numbers That Actually Matter
The 16 MPa hydraulic pressure combined with a 10-second cycle determines the density and compressive strength of every brick that leaves the mould. Clay-cement mixes in the 80–97 % clay range need enough pressure to compact the fines into a tight interlock profile, but excessive pressure on a lean cement mix can cause edge cracking during demoulding. The dual mould formats — 300 × 150 × 100 mm and 250 × 125 × 60 mm — each demand a different charge volume from the mixer, so batch weight must be recalculated when you switch formats rather than running the same feed setting across both.
The Hidden Cost of Skipping Line Calculations
A buyer who specs the press alone and sources the mixer locally often discovers that the mixer’s discharge gate is too small or its drum speed too slow to match a 10-second cycle. The result is a press that idles through several seconds of every cycle, losing output that was already paid for. I have seen plants where the curing rack filled up by mid-morning because nobody calculated how many square metres of flat surface an eight-hour run actually requires, forcing the line to shut down until cured bricks were moved out [NEED_CITE: common bottlenecks in small block production lines].
Why Buyers Source the Full Line Here
Block machinery is our single focus, which means the LY2-10 press, its moulds, feeder, mixer, and curing layout are specified as one matched system rather than assembled from separate suppliers. We set the configuration against your actual clay source and cement availability, not a catalogue default. The dual power option — electric motor or diesel engine — lets us adapt the supporting equipment to grid-connected plants or remote sites where diesel is the only realistic choice. Automation level is selectable, so a first-time buyer can start with semi-automatic operation and add automatic stacking later as volume justifies the investment. Mould design covers the interlocking formats your local market sells, and custom drawings are available when standard formats do not match.
Documentation & Verification
- Line layout drawing with every station from clay hopper to curing rack mapped to the 10-second cycle
- Capacity calculation sheet stating the brick format and mix proportion assumed for each output figure
- Voltage, frequency, and PLC display language confirmation signed off before production begins
- Factory test record showing the press running at cycle time with the specified clay-cement mix
- Hydraulic and electrical schematic matching the as-built configuration for on-site troubleshooting
Installation, Commissioning & Support
- Foundation plan sized for the 1200 kg press weight and 16 MPa hydraulic load, no deep piling required
- Power connection confirmed for 380 V 3-phase 50 Hz or buyer-specified voltage before wiring begins
- Machine ships fully assembled in wooden crate, reducing on-site reassembly to utility hookups
- Commissioning includes mixer batch timing adjusted to match the press 10-second cycle
- Operator training covers mould change procedure for both 300 × 150 and 250 × 125 formats
- Wear parts list with hydraulic seal and mould liner part numbers for first reorder
Before You Request a Quote
Tell us the brick format your market sells most, the daily volume you need to hit, and whether your site has reliable grid power or requires diesel operation. Share the clay source and any local aggregate you plan to blend, along with available floor space for the curing area. With those details we can calculate the supporting equipment that keeps the LY2-10 running at its rated cycle without upstream or downstream bottlenecks.
Frequently Asked Questions
Q: How is the output capacity of 5,760 pieces per day calculated, and which brick format does it assume?
A: The figure assumes continuous operation over an eight-hour shift with no downtime for mould changes or maintenance. However, the source does not specify which of the two mould formats — 300 × 150 × 100 mm or 250 × 125 × 60 mm — was used for that calculation. We confirm the exact output per format when we prepare your line layout.
Q: What upstream equipment is needed to keep the LY2-10 running at its rated cycle time?
A: A raw material feeder sized to deliver clay-cement batches and a mixer with a discharge rate that matches the 10-second press cycle are essential. The mixer drum volume and gate opening must be calculated so a full charge reaches the press hopper before the next cycle begins, eliminating idle time.
Q: How do I size the curing area to match daily output without bottlenecks?
A: Since the LY2-10 forms bricks without pallets, cured bricks rest directly on the floor or on simple racks. You need enough flat surface to hold at least one full day’s output while earlier batches cure. We include a curing area layout in the line drawing based on your target daily volume and available space.
Q: Can the line be configured for diesel power, and how does that change the layout?
A: Yes, the press is available with a 12 HP diesel engine instead of the 7.5 kW electric motor. Diesel operation removes the need for a dedicated electrical supply but requires fuel storage and exhaust ventilation near the press station. Supporting equipment like the mixer can also be diesel-driven to keep the entire line off-grid.
Q: What voltage and control language will the line arrive with, and how is it confirmed?
A: Standard configuration is 380 V, 3-phase, 50 Hz, but we customise voltage and frequency to your local supply. The PLC display language is confirmed in writing before production starts, so the operator interface is readable from the first day of commissioning — no firmware swaps or panel rewiring needed on arrival.