
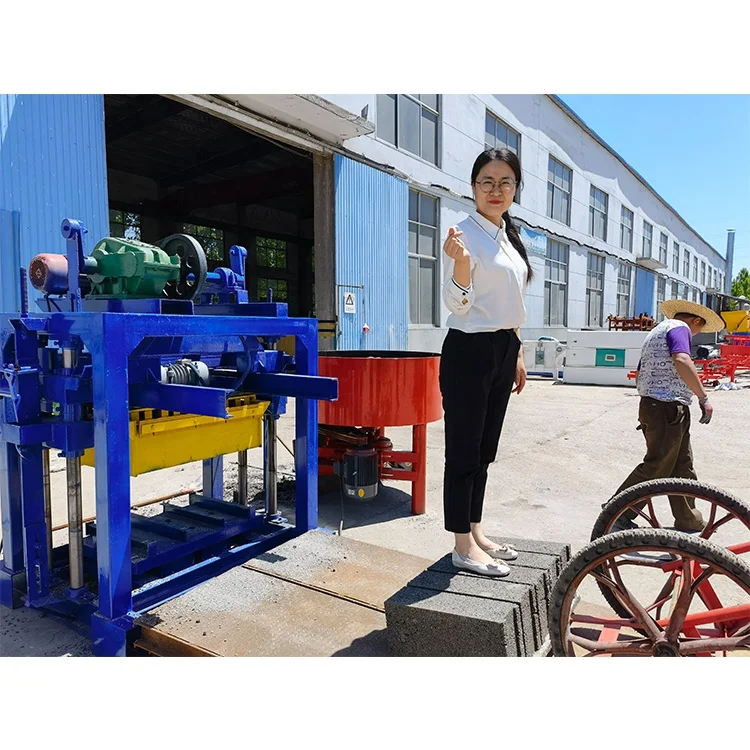
Matched Line Configuration — Every station from raw material feeding to stacking is timed against the QTJ4-40’s 40-second molding cycle so the press never waits on upstream or downstream equipment.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Semi-Automatic Concrete Block Making Machine |
| Model | QTJ4-40 |
| Rated Power | 10.4 kW |
| Molding Cycle | 40 s |
| Vibration System | Bed mould vertical vibration + upper mould compression vibration |
| Control System | Semi-automatic with top die push-pull and automatic scraper |
| Pallet Size | 850 × 450 mm |
| Overall Dimensions | 1350 × 1460 × 1800 mm |
| Machine Weight | 1 T |
| Raw Materials | Concrete, sand, cement, fly ash, lime, gypsum |
| Theoretical Output (400×200×200 mm hollow block, 4 pcs/mould) | 360 pcs/h, 2800 pcs/day |
| Theoretical Output (400×150×200 mm hollow block, 5 pcs/mould) | 450 pcs/h, 3600 pcs/day |
| Theoretical Output (225×112.5×60 mm solid brick, 9 pcs/mould) | 800 pcs/h, 6400 pcs/day |
| Output Capacity | 2000–2500 pcs / 8 hours (basis not stated in source — confirm block format) |
| Voltage | Configured to buyer’s local standard (source value — verify against manufacturer catalog) |
| Automation Level | Semi-automatic |
Application Suitability
| Application | Material or Output |
|---|---|
| Small to medium-scale concrete block production plants | Hollow blocks, solid bricks, and pavers from concrete and fly ash mixes |
| On-site block production for construction contractors | Hollow blocks from crushed stone, sand, and cement at the building site |
| Entrepreneurs establishing a first block production workshop | Solid bricks and interlocking pavers from locally sourced aggregate |
| Existing plants adding a smaller format line | Pavers and kerbstones alongside a high-capacity automatic press |
Why the Mixer Question Must Come Before the Block Machine Price
A 40-second press cycle means nothing if your mixer takes 70 seconds per batch.
I have watched plant owners celebrate fast cycle times on a concrete block making machine production line, only to find the press sitting idle while the mixer finishes its batch. The bottleneck is rarely the press itself. It is the station you forgot to time. When the pallet feeder, mixer, and stacking area are not synchronized to the same rhythm, your actual daily output can fall well below the catalogue number you planned your business around [NEED_CITE: line synchronization standards for concrete block production].
How the Stations Connect Around the Press
The QTJ4-40 sits at the center of a small-to-medium concrete block making machine production line where raw material feeding, mixing, pallet feeding, and stacking must each complete their task within the same 40-second window. If the mixer discharges one batch every 70 seconds but the press needs a fresh batch every 40 seconds, the press waits through nearly half of every cycle. Line layout planning starts with a stopwatch at every station, not a single figure from the press brochure.
Where Semi-Automatic Fits in the Line Flow
Semi-automatic operation means the top die push-pull and scraper run on their own, but pallet handling and stacking still rely on an operator. That is a deliberate choice for plants where labor cost is low and the buyer wants to keep initial investment contained. The pallet circuit — loading empty pallets, receiving filled pallets from the press, and moving cured pallets to the stacking area — must still be designed so the operator is never the bottleneck [NEED_CITE: manual pallet handling workflow in semi-automatic block plants].
Reading the Capacity Table Honestly
The QTJ4-40 produces 360 hollow blocks per hour when running 400×200×200 mm blocks at four per mould, and 800 solid bricks per hour at 225×112.5×60 mm with nine per mould. These figures assume uninterrupted material supply, consistent mix quality, and no pallet delays. The dual vibration system — vertical vibration under the bed mould combined with compression vibration from the upper mould — is what keeps block density consistent across every pallet, but only when the mix arriving at the hopper matches the design the machine was set up for.
The Cost of Ignoring Line Timing
When the pallet size is chosen without checking the curing racks and forklift already on site, pallets pile up on the floor because they do not fit the racks. When voltage and frequency are assumed rather than confirmed, the motor burns out on first startup or the PLC refuses to boot. These are not machine defects. They are configuration gaps that turn a smooth commissioning into a multi-week delay, and the buyer pays for it in lost production time and emergency parts shipments [NEED_CITE: common commissioning failures in exported block machinery].
Why Buyers Come Back for the Second Line
Block machinery is the single focus here, which means the press, mould, pallet, and handling equipment are specified as one matched system rather than assembled from separate suppliers. The configuration is set against your actual mix design and local aggregate, not a catalogue default. Mould design covers the formats your market actually sells, and the automation level is selectable — a plant can start with manual pallet handling and add automatic stacking and cubing later without replacing the press.
Documentation & Verification
- Line layout drawing showing station cycle times matched to the 40-second press cycle
- Capacity calculation sheet stating output per block format, not a single headline figure
- Pallet specification covering size, material, and quantity matched to your curing area
- Voltage, frequency, and PLC display language confirmation before production begins
- Factory test record on your specified block format before dispatch
- Operation and maintenance manual with wear parts and mould replacement list
Installation, Commissioning & Support
- Foundation plan sized to the 1350 × 1460 mm footprint and 1 T operating weight
- Electrical connection confirmed for your local voltage before the 10.4 kW motor is wired
- Pallet circuit layout aligned with your existing curing racks and forklift capacity
- First-run parameter setting with your local aggregate and mix design on site
- Operator training covering mould change, vibration adjustment, and daily maintenance
- Wear parts list with hydraulic seal and scraper blade reorder intervals specified
What to Share When You Request a Line Quote
To size the supporting equipment around the QTJ4-40, share the block formats you plan to produce, the daily output you need per format, and the raw materials available locally. Include your workshop dimensions, existing curing rack and forklift specifications, and the local voltage and frequency. If you already run a mixer or conveyor, note its cycle time so the line layout can be built around real numbers rather than assumptions.
Frequently Asked Questions
Q: How is daily output calculated for each block format on the QTJ4-40?
A: Output is calculated per block format based on mould cavity count and the 40-second cycle. For example, a 400×200×200 mm hollow block at four per mould yields 360 pieces per hour. These figures assume uninterrupted material supply and matched upstream equipment. A capacity sheet stating output per format is provided with every line proposal so you can plan against real numbers.
Q: What supporting equipment must match the 40-second cycle?
A: The mixer, pallet feeder, and stacking station must each complete their task within or faster than 40 seconds. If any station takes longer, the press sits idle and daily output drops. A line layout drawing is provided showing cycle time at every station so bottlenecks are identified before equipment is ordered, not after installation.
Q: Can the pallet size be configured beyond 850 × 450 mm?
A: The standard pallet size is 850 × 450 mm, but it can be adjusted to match your existing curing racks and forklift. Pallet material and quantity are included in the quotation so the curing area is planned as part of the line, not left as an afterthought once the press arrives on site.
Q: How is voltage confirmed before shipment?
A: Voltage, frequency, and PLC display language are confirmed in writing before production begins. This prevents motor burnout or control system failure during commissioning. The electrical schematic is provided with the quotation so your local electrician can verify the supply before the machine arrives.
Q: What is the upgrade path from semi-automatic to full automation?
A: The QTJ4-40 can start with manual pallet handling and later add automatic pallet feeding, stacking, and cubing without replacing the press. The semi-automatic control system is designed to accept these additions, so a plant can grow its automation level as production volume increases and labor costs change.



