
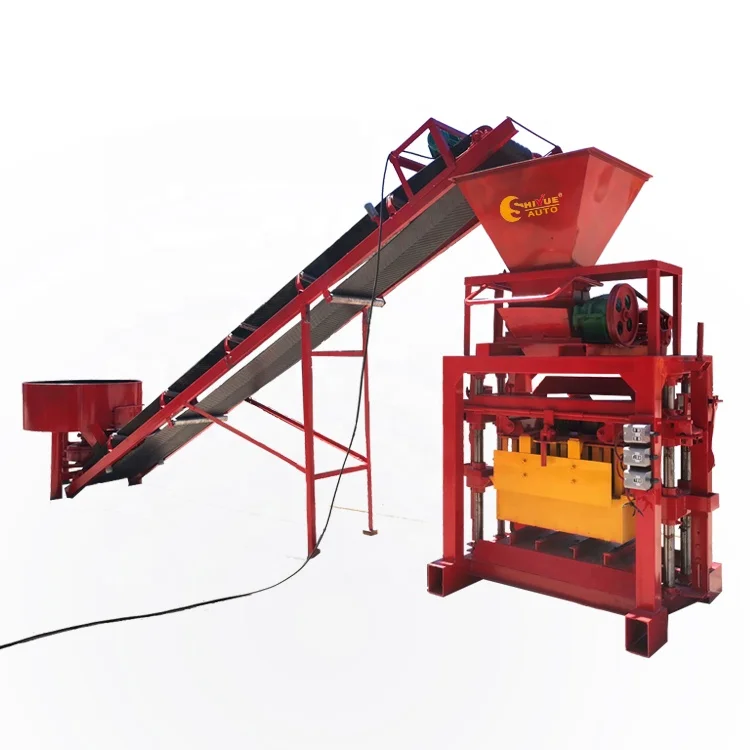
Line-Matched Throughput — The QTJ4-35 press is specified with its JQ350 mixer, pallet size and handling stations as one timed system rather than quoted as an isolated cycle.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QTJ4-35 |
| Product Type | Semi-Automatic Concrete Block Making Machine |
| Overall Dimensions | 1350 × 1460 × 1800 mm |
| Molding Cycle | 35 s (basis not stated in source — confirm block format and material) |
| Vibration Frequency | 2800 r/min |
| Vibration Force | 30 KN |
| Total Power | 11.15 kW |
| Mixer Model | JQ350 |
| Pallet Size | 850 × 450 × 20 mm |
| Net Weight | 1500 KG |
| Applied Products | Concrete hollow blocks (8 inch, 6 inch), solid bricks |
| Raw Materials | Crushed stones, sand, cement, dust, fly ash |
| Automation Level | Semi-automatic with manual pallet handling |
| Production Capacity — 400×200×200 mm Hollow Block | 4 pcs/mould, 408 pcs/hr, 3264 pcs/8hr |
| Production Capacity — 400×150×200 mm Hollow Block | 5 pcs/mould, 510 pcs/hr, 4080 pcs/8hr |
| Production Capacity — 240×115×53 mm Solid Brick | 18 pcs/mould, 2100 pcs/hr, 17000 pcs/8hr |
Application Suitability
| Application | Material or Output |
|---|---|
| Small-scale hollow block plant | Crushed stone, sand, cement and fly ash mixes for 8-inch and 6-inch blocks |
| On-site contractor block production | Solid brick and hollow block formats for housing project walls |
| First block plant with limited investment | Semi-automatic line from manual pallet feeding through to open-air curing |
| Existing concrete product manufacturer adding formats | Hollow block and solid brick alongside current paver or kerbstone output |
Why the Block Production Line Equipment Quotation Must Include Every Station
A press cycle means nothing when the mixer cannot keep up or pallets pile up on the floor.
Many buyers receive a quotation that lists cycles per hour for the press alone. The upstream mixer, pallet feed arrangement and downstream stacking are left out, so the real daily tonnage falls well below the headline figure. On a semi-automatic setup like the QTJ4-35, the operator is moving pallets by hand every 35 seconds; if the curing rack layout does not match the 850 × 450 mm pallet, that operator spends half the shift walking instead of pressing. [NEED_CITE: typical block plant bottleneck causes in semi-automatic lines]
How the 35-Second Cycle Governs Every Other Station
The QTJ4-35 completes one moulding stroke every 35 seconds, which sets the tempo the rest of the block production line equipment must follow. The JQ350 mixer has to discharge a full batch into the press hopper before that window closes; any delay means the press sits idle and the quoted hourly output slips. Downstream, the operator must pull the finished pallet and slide a fresh one into position within the same window, so pallet staging distance and curing rack height become part of the cycle equation, not afterthoughts.
Pallet Size, Curing Area and the Forklift You Already Own
The 850 × 450 × 20 mm pallet is the physical link between the press and your curing yard. If your existing racks are spaced for a different pallet width, the freshly pressed blocks either will not fit or will sit unstable during transport. Matching pallet material to your climate matters too — wooden pallets absorb moisture in humid regions and add weight to every forklift trip, while bamboo or PVC alternatives change the friction surface the press vibrates against. [NEED_CITE: pallet material selection criteria for concrete block curing]
Reading the Specs That Actually Shape Daily Output
Vibration force and frequency together determine how tightly the aggregate packs inside the mould cavity. The QTJ4-35 delivers 30 KN at 2800 r/min, which is adequate for standard crushed-stone and sand mixes but may need adjustment when fly ash replaces a large share of the fine aggregate. Total connected load of 11.15 kW includes the press motor and the JQ350 mixer, so your site transformer and cable sizing must cover both units plus any conveyor you add later. The 1350 × 1460 mm footprint keeps the press compact, yet the manual pallet handling corridor on each side still needs clear floor space that is not reflected in the machine dimensions alone.
What Happens When Line Stations Are Chosen Separately
Specifying the press without the rest of the block production line equipment leads to mismatches that surface only after installation. A mixer that is too small starves the hopper and forces the operator to wait between cycles, cutting real output in half. Pallets ordered from a local supplier without checking the press guide rail width jam during feeding and damage block edges. Voltage and control language left unconfirmed until the crate arrives can delay commissioning by weeks while the correct contactors and PLC display are sourced locally. [NEED_CITE: common commissioning delays from unconfirmed electrical specifications]
Why Sourcing the Press and Line Together Matters
Block machinery is our single focus, so the QTJ4-35 is never shipped as a standalone press — the mixer, pallet specification and handling stations are selected as one matched set. We configure the vibration force and hydraulic settings against your actual mix design and local aggregate, not a default catalogue recipe. Moulds are designed for the hollow block and solid brick formats your market moves, and custom drawings are available when standard moulds do not cover your product range. Pallet size and material are confirmed against your curing area layout and forklift capacity before production begins. Voltage, frequency and control display language are locked in during the order stage so the line is ready to run the day it lands on your floor.
Documentation & Verification
- Line layout drawing showing QTJ4-35 press position, JQ350 mixer placement and pallet flow path
- Capacity calculation sheet stating the block format assumed for each output figure
- Pallet specification matched to your curing rack spacing and forklift rating
- Hydraulic and electrical schematic for your site electrician before dispatch
- Factory test record run on your confirmed mix design and block format
- Voltage, frequency and control language confirmation signed off before crating
Installation, Commissioning & Support
- Foundation pad leveled for 1350 × 1460 mm footprint with anchor bolt template supplied
- Dedicated circuit rated for 11.15 kW total draw covering press and JQ350 mixer
- Vibration force and pressure tuned on-site to your local aggregate and mix ratio
- Pallet guide rails adjusted to match the 850 × 450 mm pallets delivered with the line
- Operator training on mould change procedure and daily greasing schedule before handover
- Wear parts list and first replacement set included for vibration springs and mould liners
Before You Request a Quote
To size the QTJ4-35 and its supporting block production line equipment correctly, we need your target block format, required daily output and the raw materials you can source locally. Share your site voltage and frequency, the curing area dimensions you have available and the pallet size your existing forklift and racks are built around. If you are replacing a current press, tell us the bottleneck you want to eliminate so the surrounding stations are specified to close that gap.
Frequently Asked Questions
Q: How is the daily output of the QTJ4-35 line calculated, and which block format is assumed?
A: Each output figure in the specification is tied to a specific block size. The 408-piece hourly rate assumes the 400×200×200 mm hollow block at four pieces per mould, while the 510-piece rate assumes the 400×150×200 mm hollow block at five per mould. Real daily tonnage also depends on pallet handling speed and curing rack availability, so we state capacity per format rather than a single headline number.
Q: Does the quotation cover pallet feeding, stacking and curing rack handling, or only the press?
A: The quotation covers the QTJ4-35 press, the JQ350 mixer and the pallet specification as a matched set. Stacking and curing rack handling are semi-automatic at this tier, meaning the operator moves pallets manually. If you need automatic stacking or rack handling, we can scope those stations separately and confirm the cycle alignment with the 35-second press stroke.
Q: How must the JQ350 mixer capacity match the press cycle so the press never waits?
A: The JQ350 discharges one batch per mixing cycle, and that cycle must finish before the QTJ4-35 completes its 35-second moulding stroke. We confirm batch weight, mixing time and discharge height against your mix design so the press hopper stays full. If your recipe uses a high fly-ash share that extends mixing time, we adjust the mixer specification or add a storage hopper between the two units.
Q: What pallet size and material are specified, and how do they relate to my curing area?
A: The standard pallet for the QTJ4-35 is 850 × 450 × 20 mm. We confirm the material — wood, bamboo or PVC — against your local humidity and the load rating of your forklift. Your curing rack spacing must accept this pallet width, and the rack height must clear the pressed block plus pallet thickness so blocks are not disturbed during transport.
Q: What voltage, frequency and control language are confirmed before the line ships?
A: We lock in your site voltage and frequency during the order stage and size the motor, contactors and heater elements accordingly. The control panel labels and any display text are produced in the language your operators read. This confirmation is documented in the electrical schematic so your electrician can prepare the incoming supply before the line arrives.



