
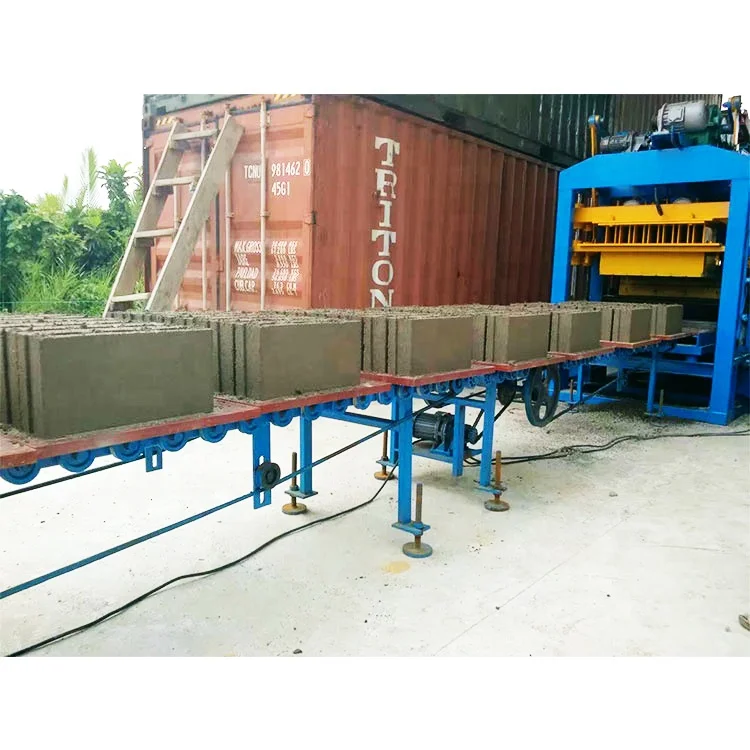
Matched Line Integration — The QTJ4-25 semi-automatic block making machine is specified as a complete production line where the mixer, host press, and pallet handling are timed to the same cycle, so the press never waits on upstream stations.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QTJ4-25 |
| Product Type | Semi-Automatic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 6400×1500×2700 mm |
| Molding Cycle | 25 s |
| Vibration Frequency | 2800–5100 r/min |
| Exciting Force | 60 kN |
| Total Power | 17.9 kW |
| Mixer Model | JQ350 |
| Pallet Size | 850×550×20 mm |
| Net Weight | 2500 kg |
| Applied Products | Concrete hollow blocks (8 inch, 6 inch), solid bricks |
| Raw Materials | Crushed stones, sand, cement, dust, fly ash |
| Output — Hollow Block 390×190×190 mm | 480 pcs/h, 3800 pcs/8hr (4 pcs/mould) |
| Output — Hollow Block 400×150×200 mm | 600 pcs/h, 4800 pcs/8hr (5 pcs/mould) |
| Output — Solid Brick 240×115×53 mm | 2100 pcs/h, 17000 pcs/8hr (18 pcs/mould) |
| Automation Level | Semi-automatic |
| Hydraulic Station | Equipped (high pressure) |
| Vibration System | Bed mould vertical vibration + upper mould compression vibration |
| Key Features | Hydraulic high-pressure forming, dual vibration system, matched JQ350 mixer, CE declaration where applicable |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for masonry walls | Crushed stone, sand, cement, fly ash — 390×190×190 mm or 400×150×200 mm formats |
| Solid brick production for load-bearing and partition work | Sand, cement, stone dust — 240×115×53 mm standard brick |
| On-site block production for housing and commercial projects | Local aggregate blended with cement, semi-automatic operation with manual pallet transfer |
| First plant setup by entrepreneurs entering the block market | Complete line from raw material mixing through to manual stacking on curing racks |
Why Your Daily Output Rarely Matches the Brochure Number
Every capacity figure for the QTJ4-25 semi-automatic block machine production line is tied to a specific block format and mould — no generic "pieces per hour" without context.
I once watched a block plant in Lusaka run a semi-automatic press where the catalogue claimed a certain hourly output, but the sales quote never specified which block size that number assumed. The buyer ordered the machine expecting to produce 8-inch hollow blocks all day, only to discover the quoted figure was based on a smaller solid brick format. Real daily throughput dropped well below the projection. The mismatch was not the machine’s fault — it was a specification failure at the quotation stage [NEED_CITE: common causes of output shortfall in semi-automatic block plants]. With this semi-automatic block machine production line, the output for 390×190×190 mm hollow blocks is rated at 480 pcs/h with 4 pieces per mould on a 25-second cycle, while the 400×150×200 mm format delivers 600 pcs/h with 5 pieces per mould. Solid bricks at 240×115×53 mm reach 2100 pcs/h with 18 pieces per mould. Each number comes with its format, mould cavity count, and cycle time attached.
Mixer-to-Press Feed Synchronization
A semi-automatic block machine production line lives or dies by the rhythm between its stations. The JQ350 mixer included in this line is sized so that its batch discharge rate keeps pace with the 25-second moulding cycle of the QTJ4-25. When the mixer output lags, the press sits idle — burning through the shift without producing. I learned this the hard way on a Zambian site where an undersized mixer turned a rated semi-automatic line into a bottleneck demonstration. The JQ350 was selected to prevent exactly that failure mode, ensuring the hopper above the press stays charged across continuous runs of both hollow block and solid brick formats.
Pallet Flow and Curing Area Alignment
The 850×550×20 mm pallet specified for this line is not an arbitrary choice. It matches the mould footprint for every format listed in the capacity table and aligns with standard curing rack spacing and forklift tine widths common in small-to-medium block yards. When a line is built with pallets that do not match the curing area or the buyer’s existing handling equipment, pallets pile up on the floor, blocks cure unevenly, and semi-automatic operation degenerates into manual shuffling [NEED_CITE: pallet sizing guidelines for concrete block curing areas]. This semi-automatic block machine production line accounts for that chain from the start.
Vibration and Hydraulic Pressure Interaction
The QTJ4-25 uses a dual vibration approach: bed mould vertical vibration combined with upper mould compression vibration, operating across a frequency range of 2800–5100 r/min with an exciting force of 60 kN. The hydraulic station adds high-pressure compaction on top of the vibration. Together, these forces determine the green density of each block before it leaves the mould. Vibration alone produces loosely consolidated concrete; hydraulic pressure alone can trap air pockets. The combination, properly tuned to the buyer’s mix design and local aggregate gradation, produces consistent block strength across the shift.
What Happens When Line Stations Are Mismatched
When supporting equipment is sourced separately from the host press, the gaps show up on day one of production. A conveyor that feeds too slowly leaves the press waiting between cycles. Pallets that are too thin warp under vibration and jam the feed mechanism. A mixer that discharges in surges floods the hopper and then starves it. The result is a semi-automatic block machine production line that technically runs but never reaches the output the buyer budgeted for [NEED_CITE: impact of station mismatch on block line throughput]. These are the failures that no single supplier takes responsibility for, because each component was ordered independently.
Why Source the Full Line from One Configuration
The QTJ4-25 is not sold as a standalone press dropped into an existing setup without review. The line configuration covers the host machine, JQ350 mixer, pallet specification, and manual stacking stations as one matched package. Configuration is set against the buyer’s actual mix design, local aggregate, and target block format rather than a default catalogue entry. Moulds are designed and supplied for the formats the buyer’s market actually sells, with custom drawings available when standard formats do not cover local demand. The automation level is selectable — a buyer can start with semi-automatic operation and add automatic stacking or pallet feeding later without replacing the host press. Installation and commissioning support includes operator training on the complete line, not just the press.
Documentation & Verification
- Line layout drawing showing station spacing and capacity calculation per block format
- Machine specification sheet with vibration frequency, hydraulic pressure, and power ratings
- Mould drawing and format list covering hollow block, solid brick, and custom options
- Pallet specification confirming size, material grade, and quantity matched to curing area
- Voltage, frequency, and control language confirmation signed off before production
- Factory test record demonstrating cycle time and output under actual mould conditions
Installation, Commissioning & Support
- Foundation plan based on the 6400×1500 mm footprint and 2500 kg operating weight
- Electrical supply confirmed at buyer’s voltage and frequency before the 17.9 kW system ships
- Machine arrives dismantled for container loading with reassembly guidance on site
- First-run commissioning covers mould installation, vibration tuning, and hydraulic pressure setting
- Operator training addresses cycle timing, mould change procedure, and daily maintenance checks
- Wear parts list and mould inventory provided for first replacement planning
What We Need to Configure Your Line
To size this semi-automatic block machine production line accurately, share the block formats your market demands, the daily output target per format, and the raw materials available locally — particularly aggregate type and gradation. Confirm your site voltage and frequency, the control panel language your operators need, and the dimensions of your curing area so pallet quantity and rack layout can be calculated. If you have existing conveyors, mixers, or handling equipment that the new line must integrate with, provide their specifications so station timing can be verified before production begins.
Frequently Asked Questions
Q: How is daily output calculated per block format, and what does the 25-second cycle assume?
A: Each output figure for the QTJ4-25 is tied to a specific block size, mould cavity count, and the 25-second moulding cycle. For example, the 390×190×190 mm hollow block uses a 4-cavity mould, yielding 480 pcs/h and 3800 pcs over an 8-hour shift. The calculation assumes continuous material feed and pallet availability with no unplanned stops.
Q: How does the mixer keep pace with the press so the machine is never left waiting?
A: The JQ350 mixer is included in the semi-automatic block machine production line specifically because its batch discharge rate matches the 25-second press cycle. The mixer volume and discharge gate sizing are calculated so the host press hopper remains charged during continuous production, eliminating the idle time that occurs when mixer output falls behind press demand.
Q: What pallet size and quantity are recommended for my curing area?
A: The standard pallet for this line is 850×550×20 mm, matched to the mould footprint and standard forklift handling. The total pallet quantity depends on your curing area footprint, rack configuration, and curing duration. We calculate the recommended count during line configuration so pallets rotate through the curing cycle without creating a bottleneck at the press.
Q: Which supporting stations are included and which remain manual at this automation level?
A: The semi-automatic configuration includes the JQ350 mixer, raw material feed to the press, and hydraulic-vibration forming. Pallet transfer from the press to the curing area and block stacking remain manual operations. Automatic pallet feeding and stacking can be added as an upgrade path without replacing the QTJ4-25 host machine.
Q: What electrical and control details are confirmed before shipment?
A: Voltage, frequency, and PLC or control panel display language are confirmed with the buyer before production begins. This prevents commissioning delays caused by incompatible power supply or an interface the operators cannot read. The confirmation is documented and included in the factory test record shipped with the semi-automatic block machine production line.



