
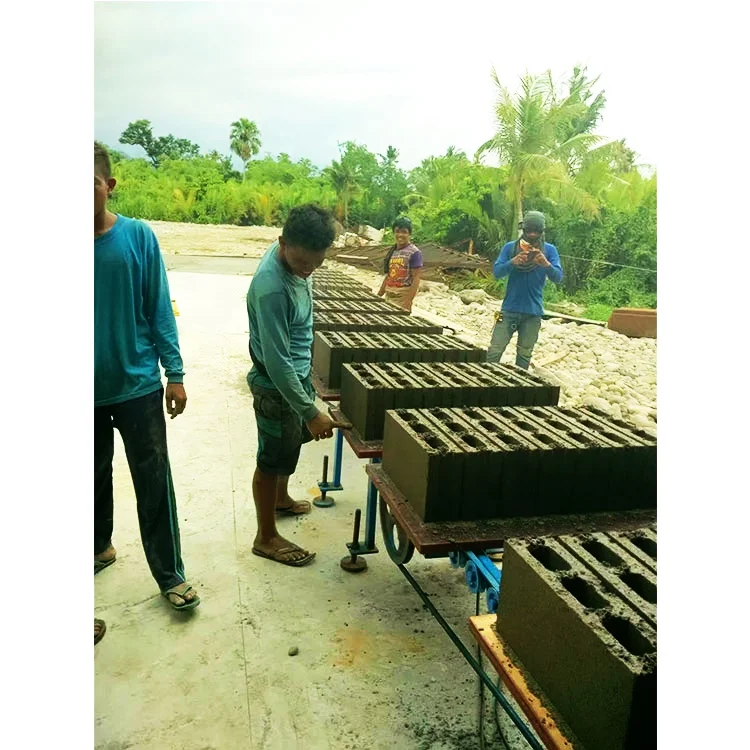
Matched Line Integration — The QTJ4-25 press is never quoted alone; the JQ350 mixer, pallet feeder, and discharge conveyor are sized against the 25-second molding cycle so material and pallets arrive before the press finishes each stroke.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QTJ4-25 |
| Product Type | Automatic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 6400×1500×2700 mm |
| Molding Cycle | 25 s |
| Vibration Frequency | 2800–5100 r/min |
| Exciting Power | 60 KN |
| Total Power | 17.9 KW |
| Mixer Model | JQ350 |
| Pallet Size | 850×550×20 mm |
| Total Weight | 2500 KG |
| Applied Products | Concrete hollow blocks (8 inch, 6 inch), solid bricks |
| Raw Materials | Crushed stones, sand, cement, dust, fly ash |
| Control System | PLC control with automatic plate-supplying, material-disturbing, and brick-discharging |
| Vibration Type | Flat vibration with squeeze compression vibration |
| Output Capacity | 480 pcs/h (basis: 390×190×190 mm hollow block, 4 pcs/mould) |
| Output Capacity | 600 pcs/h (basis: 400×150×200 mm hollow block, 5 pcs/mould) |
| Output Capacity | 2100 pcs/h (basis: 240×115×53 mm solid brick, 18 pcs/mould) |
| Daily Output (8 hr) | 3800 pcs (basis: 390×190×190 mm hollow block) |
| Daily Output (8 hr) | 4800 pcs (basis: 400×150×200 mm hollow block) |
| Daily Output (8 hr) | 17000 pcs (basis: 240×115×53 mm solid brick) |
| Automation Level | Semi-automatic (automatic plate-supplying, material-disturbing, brick-discharging) |
| Voltage & Frequency | To be confirmed per buyer’s local supply |
| Hydraulic Pressure | To be confirmed with manufacturer |
| Stacking Method | To be confirmed (manual or automatic) |
Application Suitability
| Application | Material or Output |
|---|---|
| Small to medium block production plant | Hollow blocks from crushed stone, sand, cement |
| On-site construction block production | 8 inch and 6 inch hollow blocks from local aggregate |
| First block plant for entrepreneurs | Solid bricks and hollow blocks at moderate investment |
| Distributor adding block formats | 240×115×53 mm solid bricks from cement and fly ash |
| Housing project contractor | Multiple formats on a single line using site-available materials |
What the Press Cycle Reveals About the Rest of the Line
A 25-second press cycle means every upstream and downstream station must deliver within that same window or the entire block production line supporting equipment becomes a bottleneck.
I once configured a QTJ4-25 for a West African contractor who already owned a small pan mixer from a different supplier. On paper the press was rated for steady output. In practice, the mixer took 40 seconds to prepare each batch while the press sat idle for 15 seconds every cycle. The daily tally dropped to roughly half the expected volume. That mismatch did not show up in any single machine’s spec sheet — it only appeared when both machines ran together on the same floor. [NEED_CITE: importance of cycle time synchronization in block production lines]
How Raw Material Flow Must Match the 25-Second Rhythm
The JQ350 mixer is paired with the QTJ4-25 because its batch volume and discharge rate align with what the press hopper consumes every 25 seconds. When the mixer discharges, the material must travel through the feeding conveyor and reach the hopper before the next molding stroke begins. If the belt angle is too shallow or the hopper gate too narrow, material piles up or starves the mould cavity. This is where block production line supporting equipment selection either protects or destroys the press’s rated cycle time.
Pallet Circulation: The Station Most Buyers Overlook
Each molding cycle consumes one 850×550×20 mm pallet. Over an eight-hour shift producing solid bricks, that means thousands of pallet movements from the feeder through the press, then to the curing area, and back to the magazine. The pallet feeder, discharge conveyor, and return system must handle this flow without manual intervention if the quoted line claims semi-automatic operation. When pallet return is left out of the scope, workers end up carrying wet blocks by hand — exactly the scenario that erodes the daily output figures the buyer relied on during planning. [NEED_CITE: pallet circulation requirements in semi-automatic block plants]
Reading the Specs Through a Line-Planning Lens
The 60 KN exciting force combined with flat vibration and squeeze compression vibration determines block density and demolding strength. But vibration alone does not guarantee consistent blocks — the raw material must arrive at the mould with uniform moisture and gradation, which is why the JQ350 mixer’s blending consistency matters as much as the press’s vibration frequency range of 2800–5100 r/min. The PLC coordinates plate-supplying, material-disturbing, and brick-discharging in sequence, reducing the chance that one station finishes early while another lags behind. The 6400×1500×2700 mm press footprint must be read alongside mixer placement, conveyor runs, and pallet rack aisles to understand the real floor space the complete line demands.
The Cost of Treating the Press as a Standalone Purchase
When a buyer sources the mixer locally and the pallets from a third party, the press manufacturer has no responsibility for the gaps between stations. A mixer that discharges too slowly forces the press to idle. Pallets cut to the wrong thickness jam the feeder or crack under vibration. A discharge conveyor set at the wrong height drops wet blocks before the cement has gained any green strength. These problems appear one by one over the first weeks of production, and each one is blamed on a different supplier. [NEED_CITE: common integration failures in multi-supplier block plant setups]
Why Sourcing the Full Line From One Supplier Matters Here
The QTJ4-25 is specified alongside its JQ350 mixer, pallet feeder, and discharge stations so cycle times are calculated across the entire flow, not just the press. Line layout drawings state the block format assumed for every capacity figure, preventing misunderstandings about daily output. Pallet size, material, and quantity are confirmed against the buyer’s existing curing racks and forklift before production begins. Voltage, frequency, and PLC display language are locked in at the quotation stage so commissioning is not delayed after the container arrives. Mould options are selected for the formats the buyer’s local market actually purchases, rather than defaulting to a catalogue standard. The block production line supporting equipment is matched so the press never waits on an upstream or downstream station that was never part of the original quote.
Documentation & Verification
- Line layout drawing with capacity stated per block format (390×190×190, 400×150×200, 240×115×53)
- Pallet specification sheet covering size, material, and quantity matched to curing area
- Voltage and PLC language confirmation record signed before production release
- Hydraulic and electrical schematics for the full line including mixer and conveyors
- Factory test record showing press cycle time with matched JQ350 mixer running
Installation, Commissioning & Support
- Foundation plan accounts for the 2500 KG press weight and 6400 mm length plus mixer and conveyor positions
- Dedicated electrical circuit sized for 17.9 KW total draw with voltage and frequency matched to local grid
- Machine shipped in dismantled state for container loading with reassembly and alignment on site
- PLC language set and molding parameters tuned during first commissioning run with operator present
- Mould change procedure trained on site so format switches do not consume a full shift
- Wear parts list supplied for hydraulic seals, vibration springs, and pallet guide rollers
What We Need to Configure Your Line
Before quoting, share your target block format, daily output goal, and the raw materials available at your site. Confirm your local voltage and frequency, the PLC language your operators read, and whether you already have curing racks, forklifts, or mixers that the new line must connect to. If you are working to a project deadline, tell us your required commissioning date so we can work backward through production and shipping timelines.
Frequently Asked Questions
Q: Which stations must be matched to the QTJ4-25 cycle so the press never idles?
A: The JQ350 mixer discharge rate, feeding conveyor speed, pallet feeder timing, and brick discharge conveyor must all complete their tasks within the 25-second molding cycle. If any station is slower, the press waits and daily output drops below the rated capacity for each block format.
Q: How do I check whether the 850×550×20 mm pallet fits my existing curing area?
A: Measure your curing rack spacing and forklift fork width before ordering. The pallet specification sheet provided with the quotation confirms dimensions, material, and load rating so you can verify compatibility with the racks and handling equipment already on your site.
Q: Does the quoted line include stacking and curing rack handling?
A: Stacking method is confirmed during the quotation stage. The scope may cover automatic plate-supplying and brick-discharging through the press, but manual or automatic stacking after discharge is a separate selection that must be agreed before the line is finalized.
Q: What mixer capacity is needed to sustain rated output for each block format?
A: The JQ350 is matched to the QTJ4-25 press throughput. Its batch volume and mixing time are calculated so material reaches the hopper within each 25-second cycle, whether you are producing hollow blocks at 480 pcs/h or solid bricks at 2100 pcs/h.



