
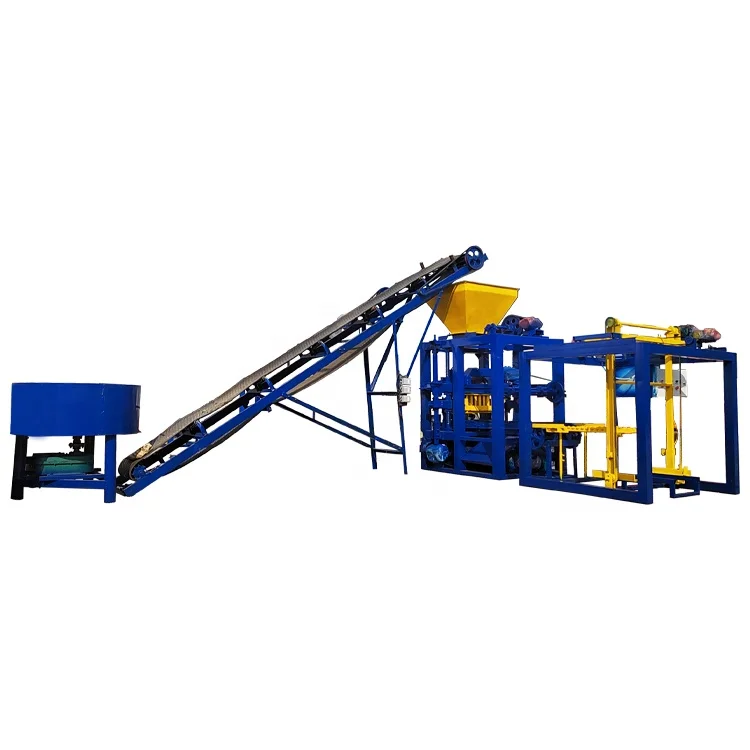
Matched Line Flow — the host press, mixer and conveyor are timed as one loop so the QTJ4-24 never sits idle waiting for feed.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QTJ4-24 (also referenced as QT4-24) |
| Product Type | Semi-Automatic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 3600mm × 1700mm × 2560mm |
| Total Mass | 3.5T |
| Main Machine Power | 11.95kW |
| Pallet Size | 900mm × 450mm |
| Molding Cycle | 24-26s |
| Mould Formats | 400×200×200mm (4 pcs/mould); 390×240×190mm (3 pcs/mould); 390×120×190mm (6 pcs/mould); 240×115×53mm (21 pcs/mould) |
| Automation Level | Semi-automatic (mechanical and manual combined operation) |
| Vibration Type | Table vibration feeding, fluctuation vibration molding |
| Feeding Method | Manual feeding, two feed way options |
| Supporting Line Equipment | J350 or JQ350/JQ500 vertical mixer, 6m or 8m belt conveyor |
| Control System | Electrical control cabinet with mechanical interworking |
| Wire Specification | Main machine 3×6mm; Mixer 3×4mm; Conveyor 3×2.5mm; General power 3×16mm |
| Warranty | 1 year for whole machine (excluding spare parts) |
| Assembly State | Stationary machine on precast concrete ground |
| Standards | CE (basis to be confirmed) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for small plants | Crushed stone, sand, cement and fly ash blends |
| Solid standard brick production (240×115×53mm) | River sand and cement with fine aggregate |
| Multi-cellular brick production | Lightweight aggregate or aerated concrete mixes |
| Paving brick production | Dense aggregate with high cement content |
| On-site block production for contractors | Local stone dust, quarry sand and Portland cement |
What "Daily Output" Leaves Out When the Line Is Not Matched
The semi-automatic block machine production line only reaches its rated cycle when every upstream station feeds the press on time.
I once watched a small block plant in West Africa run the host press at the correct 24-26s molding cycle, yet the operator spent a third of each shift waiting for the mixer to finish its batch and the belt to deliver it. The mixer capacity, conveyor length and hopper gate had been chosen independently, so the daily output ended well below what the press alone could have achieved. This is the most common gap I see on semi-automatic setups. [NEED_CITE: line balancing principles in small concrete product plants]
How the Press, Mixer and Conveyor Form One Loop
The QTJ4-24 completes one molding cycle every 24-26 seconds, which means the mixer must deliver a fresh batch to the hopper within that window. A J350 vertical mixer paired with a 6m belt conveyor keeps the material flow tight for standard hollow block runs, while a JQ500 and 8m conveyor gives more buffer when the mix design is stiff or the site layout forces a longer path. Either way, the semi-automatic block machine production line is planned so the press is never the fastest station in the loop.
Where Pallet Flow and Curing Area Dictate Real Throughput
Each cycle consumes one 900×450mm pallet, and the operator must place it by hand, then carry the loaded pallet to the curing rack. If the rack spacing was built for a different pallet size, or the site forklift cannot lift a full stack of 900×450mm pallets, cured blocks pile up on the floor and the press stops while the crew clears space. Confirming rack dimensions and forklift capacity before shipment removes this bottleneck. [NEED_CITE: pallet and curing yard sizing for small block plants]
Reading the Specs That Actually Shape Your Line
The 11.95kW main power rating covers the vibration motor and hydraulic pump together; running the mixer and conveyor from a separate circuit prevents voltage dip during the high-draw vibration phase. The table vibration feeding stage fills the mould cavity evenly before the fluctuation vibration compacts the mix, which is why stiff, low-slump blends produce denser blocks here than on machines that only vibrate during molding. The electrical control cabinet uses mechanical interworking to stop the press from firing out of sequence, protecting both the mould and the operator. Wire gauges are specified per station — 3×6mm for the main machine, 3×4mm for the mixer — so the site electrician can size conduit and breakers before the containers arrive. Choosing between the two manual feeding options depends on whether the operator stands at the hopper or at the mould station, which in turn depends on the conveyor layout you select. [NEED_CITE: vibration sequencing and block density in table-vibration machines]
The Hidden Cost of Treating Each Station as a Separate Purchase
When the mixer, conveyor and press arrive from different suppliers, nobody is responsible for the gaps between them. I have seen belt conveyors that discharge too high for the hopper, forcing a rebuild of the support frame on site. Mixers sized for a larger press leave the QTJ4-24 waiting for half its cycle. Pallets ordered locally often arrive in a size that does not match the mould or the curing rack, wasting the first week of production. [NEED_CITE: integration risks in multi-supplier block line projects]
Why Spec the Whole Line from One Source
Block machinery is the single focus at Shiyue, so the QTJ4-24 press, mixer, conveyor and pallets are specified as one matched system rather than assembled from separate catalogues. The line layout is drawn against your target block format, local aggregate and available curing area, not a generic template. Mould design covers the formats your market actually sells, and custom drawings are available when standard sizes do not fit. Voltage, frequency and control language are confirmed before production starts, so the electrical cabinet arrives ready for your grid. Operation and maintenance manuals cover every lubrication point and wiring detail specific to this configuration.
Documentation & Verification
- Line layout drawing showing press, mixer and conveyor positions with pallet flow direction
- Capacity calculation sheet stating daily output per mould format, not a single headline figure
- Pallet specification matched to your curing rack spacing and forklift lift capacity
- Electrical schematic with station-by-station wire gauge and breaker ratings
- Factory test record on your selected block format before container loading
- Operation manual covering reducer oil grade, vibration box grease and cabinet settings
Installation, Commissioning & Support
- Precast concrete ground required; no deep foundation for the 3.5T machine mass
- General power circuit needs a leakage protection breaker on the 3×16mm supply
- Two conveyor layout options — inline or perpendicular — avoid ground digging
- First-day commissioning checks vibration sequence against your mix consistency
- Operator training covers mould change procedure and mechanical interlock resets
- Wear parts list includes vibration box bearings and mould liner dimensions
What to Include in Your Inquiry
Send the block formats your market sells, the daily volume you need to hit, and the dimensions of your existing curing area. Include the local voltage and frequency, plus any mixer or forklift you already have on site, so the line layout accounts for them from the first drawing.
Frequently Asked Questions
Q: What daily output can I expect and which block format does that number assume?
A: The QTJ4-24 runs a 24-26s molding cycle, but daily output depends on which of the four mould formats is installed and how quickly the mixer-conveyor loop feeds the press. We calculate capacity per format — 4 pcs hollow block, 21 pcs standard brick — and show the figure on the line layout sheet before you commit.
Q: How do I match the 900×450mm pallet to my existing curing area?
A: Send us the rack spacing and the forklift model you already use. We confirm whether 900×450mm pallets fit your racks and whether your forklift can handle a full stack, adjusting pallet material or suggesting a rack modification before the line ships.
Q: What voltage and wire specifications are required?
A: The main machine draws 11.95kW through a 3×6mm cable, the mixer uses 3×4mm and the conveyor 3×2.5mm, all fed from a 3×16mm general power line with a leakage protection breaker. Confirm your local voltage and frequency so we configure the control cabinet before dispatch.
Q: What is included in the line quotation and what remains manual?
A: The quotation covers the host press, selected mixer, belt conveyor, one set of moulds and the control cabinet. Pallet handling, stacking and curing are manual operations on this semi-automatic configuration, so labour planning and curing yard layout are part of the line drawing we provide.



