
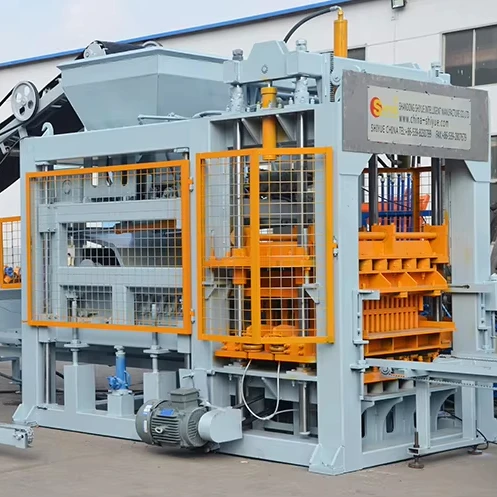
Matched Line Rhythm — The QT8-15 block making machine production line synchronizes mixer discharge, conveyor feed and stacker cycle so the press never waits between stations.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT8-15 |
| Product Type | Automatic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 8300 x 1860 x 3000 mm |
| Rated Pressure | 21 MPa |
| Vibration Form | Platform Vibration |
| Vibration Frequency | 2800-4500 RPM |
| Pallet Size | 950 x 900 mm |
| Moulding Cycle | 15-25 s (basis not stated in source — confirm block format / material / thickness) |
| Overall Power | 46 kW |
| Control System | PLC (Programmable Controller) with touch screen human-computer interface |
| Block Comprehensive Strength | up to 15 MPa |
| Automation Level | High degree of automation, manual/automatic mode transition |
| Hydraulic System | Independent integrated type hydraulic station |
| Support Equipment (Basic Line) | JS750 mixer, 8 m belt conveyor, automatic stacker |
| Included Mould | One free hollow mould with the machine |
| Stacking Method | Automatic stacker (two pallets per cycle, 3-6 layers) |
| Certification | CE declaration where applicable |
Application Suitability
| Application | Material or Output |
|---|---|
| Block and paver production plants | Hollow block, solid block, paving block from crushed stone, sand and cement |
| Construction contractors producing blocks on-site | Standard masonry units cast directly at the development site |
| Concrete product manufacturers adding formats | Interlocking brick, kerbstone and porous brick using interchangeable moulds |
| Housing project contractors | Local production of walling blocks tailored to project specifications |
The Hidden Gap in Block Line Quotations
When a quotation lists a press and nothing else, the real daily output is stacked by hand and the mixer is bought separately — the QT8-15 block making machine production line specifies the JS750 mixer, 8 m belt conveyor and automatic stacker together so cycle times align across every station.
Many buyers discover after installation that their press spends half the shift waiting for the mixer to discharge or the operator to fetch pallets. That idle time is rarely reflected in the capacity figure on the original quotation, yet it determines how many blocks actually reach the curing yard before sunset [NEED_CITE: impact of line synchronization on daily block output].
Synchronizing the Mixer Discharge with the Press Cycle
The JS750 mixer must release a batch into the conveyor hopper before the QT8-15 block making machine finishes its current moulding cycle. If the mixer is undersized, the press completes its vibration phase and sits idle while the next batch mixes. Specifying the mixer, conveyor and press as one matched system removes that dead time from the start.
How the Automatic Stacker Keeps Pace
The automatic stacker handles two pallets per cycle and stacks three to six layers depending on block height. When the press releases a cured pallet, the stacker must index and lower the previous layer before the next pallet arrives. Any mismatch here creates a bottleneck that propagates back to the press, forcing the operator to pull pallets by hand and defeating the purpose of automation.
Reading the Specs That Matter for Line Balance
The QT8-15 block making machine production line draws 46 kW overall, so the site transformer and cable sizing must account for the mixer motor starting current alongside the press. The platform vibration operates between 2800 and 4500 RPM, and the rated hydraulic pressure of 21 MPa works together with that vibration to compact the mix into the mould. The pallet size of 950 × 900 mm must match the curing rack spacing the buyer already has on site, otherwise new racks must be built or existing forklifts cannot load them. The PLC touch-screen control allows the operator to adjust feeding time and vibration duration manually, which is essential when switching between a dense hollow block mix and a lighter paver mix.
What Happens When the Conveyor Feed Lags
If the 8 m belt conveyor is replaced with a shorter or slower unit to save cost, the press hopper runs dry partway through a cycle. The resulting blocks have uneven fill and inconsistent weight, which the buyer only notices once the first batch reaches the compression test [NEED_CITE: consequences of uneven material feed on block density]. Replacing the conveyor later means re-aligning the entire line layout and extending the building footprint.
Why the Full Line Matters Beyond the Press
Every station in this block line must deliver its output within the window the next station expects. Block machinery specified as one matched system means the mixer, conveyor, press and stacker are quoted with compatible cycle times, not assembled from separate suppliers who each guarantee only their own machine. Configuration is set against the buyer’s actual mix design and local aggregate, so the vibration force and hydraulic pressure match what the material needs to reach target strength. Mould design covers the formats the buyer’s market actually sells, with custom drawings available for non-standard profiles. The automation level can start semi-automatic and add stacker or cuber modules later as the plant grows. Installation and commissioning include operator training so the team can adjust cycle parameters from day one.
Documentation & Verification
- Line layout drawing with capacity calculation stating the block format assumed for the 15-25 s cycle
- Machine specification sheet confirming 46 kW overall power and 950 × 900 mm pallet size
- Mould drawing and format list showing included hollow mould and optional profiles
- Voltage and PLC display language confirmation sheet signed before production
- Factory test record on buyer’s target block format before dispatch
- CE declaration where applicable for import clearance
Installation, Commissioning & Support
- Concrete foundation plan provided to match the 8300 x 1860 mm press footprint and 46 kW load
- Power supply confirmed for local voltage and frequency before the JS750 mixer motor is wired
- Press, mixer, conveyor and stacker dismantled into container-load modules for shipment
- PLC parameters for feeding time, vibration duration and stacker layers set during first-run commissioning
- Operator training covers manual/automatic mode transition and mould change procedure
- Wear parts list for hydraulic seals, vibration springs and mould liners supplied with delivery
Preparing Your Inquiry
To size the QT8-15 block making machine production line correctly, share the block format you sell most, the daily output you need for that specific format, and a sample of your local sand or aggregate. Confirm the voltage and frequency available at your site so the motors and PLC are wound accordingly. Let us know whether you already have curing racks and forklifts, so the 950 × 900 mm pallet specification can be verified against your existing equipment before the line ships.
Frequently Asked Questions
Q: How is the 15-25 s moulding cycle verified against a specific block format?
A: The cycle range depends on block height, wall thickness and mix design. We run a factory test using your target format and local aggregate sample, then document the actual cycle time on the test record. That figure becomes the basis for the line capacity calculation, not a generic catalogue number.
Q: How do the JS750 mixer and conveyor match the press cycle?
A: The JS750 discharge volume and the 8 m belt conveyor speed are calculated so a fresh batch reaches the press hopper before the current moulding cycle ends. If your mix includes slow-draining materials, we adjust conveyor speed or mixer timing to prevent the press from starving.
Q: What pallet size and material should I choose?
A: The standard pallet is 950 × 900 mm, but the material — hardwood, bamboo or composite — affects weight, moisture resistance and curing rack compatibility. We confirm your existing rack spacing and forklift tine width before finalizing pallet specification so no retrofit is needed on arrival.
Q: Which voltage and PLC language must be confirmed before shipment?
A: The 46 kW total load and JS750 mixer motor require the correct voltage and frequency winding. The PLC touch-screen display language must be set before the control panel is built. Both are confirmed in writing during the quotation stage to avoid commissioning delays.
Q: What moulds are available beyond the included hollow mould?
A: Solid block, paving block, kerbstone, interlocking brick and porous brick moulds are available, each with a format drawing for approval. The automatic stacker adjusts layer count from three to six depending on block height, so switching formats only requires a mould change and a PLC parameter update.



