
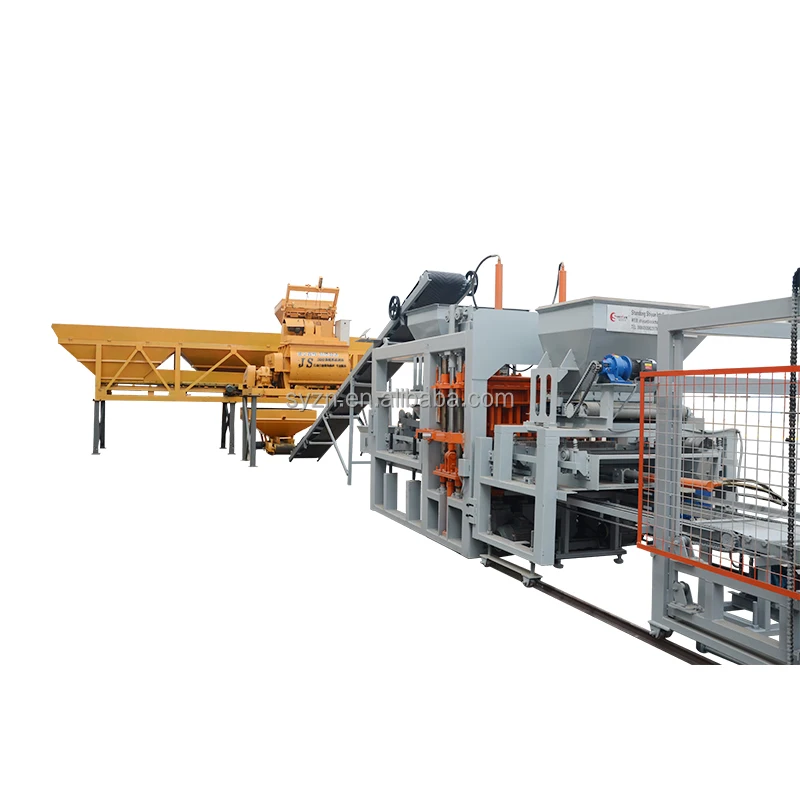
Line-Matched Cycle Timing — Every station from pallet feed to stacking is specified against the 15–20 s QT7-15 press cycle so no upstream or downstream gap throttles real throughput.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Hydraulic Block Making Machine |
| Model | QT7-15 |
| Pallet Size | 1150×700 mm |
| Molding Cycle | 15–20 s |
| Overall Power | 45 kW |
| Vibration Force | 100 kN |
| Vibration Frequency | 0–60 Hz |
| Vibration Form | Platform Vibration |
| Demolding Method | Hydraulic |
| Total Mass | 8 T |
| Control System | PLC with touch screen interface |
| Output (Hollow Block 400×200×200 mm) | 1,260–1,680 pcs/h; 10,080–13,440 pcs/8 hr |
| Output (Hollow Block 400×150×200 mm) | 1,440–1,920 pcs/h; 11,520–15,360 pcs/8 hr |
| Output (Rectangular Paver 200×100×60 mm) | 3,888–4,860 pcs/h; 31,104–38,880 pcs/8 hr at 20–25 s cycle |
| Component Configuration | Pallet feed machine, block making machine, storage hopper, conveyor, hydraulic unit, PLC cabinet |
| Automation Level | Automatic with PLC control |
| Remote Diagnostics | Supported via PLC |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production (400×200×200 mm) | Crushed stone, cement, sand, water — standard concrete mix |
| Hollow block production (400×150×200 mm) | Same mix, thinner wall profile for partition use |
| Rectangular paving brick (200×100×60 mm) | Fine aggregate surface layer over standard base concrete |
| Multi-format manufacturing | Mould change on same line without separate equipment |
| Medium-to-high output block plants | Connected line from raw feed through to cured product handling |
Why "Cycles per Hour" Means Nothing Without the Rest of the Line
The press is only as fast as the slowest station feeding or clearing it.
I once walked into a plant where the owner proudly showed me a block machine rated for impressive hourly numbers. The problem was the pallet return loop and manual stacking station downstream could not keep pace. Blocks piled up on the discharge side, the operator hit the pause button every few cycles, and the real daily output sat well below what the brochure promised. That mismatch is the single biggest reason a block machine production line disappoints after commissioning [NEED_CITE: common causes of block line throughput shortfall].
Pallet Feed and Return: The Hidden Bottleneck
The QT7-15 ships with a dedicated pallet feed machine matched to the 1150×700 mm pallet size. This is not an optional extra — it is the component that sets the rhythm for the entire block machine production line. When the feed mechanism delivers a fresh pallet in time with the press cycle, the machine never idles. When pallet return relies on a worker dragging boards back by hand, the press waits, and every lost second compounds across an eight-hour shift.
Connecting Hopper, Conveyor and Press Timing
The storage hopper and conveyor feed raw material into the mould cavity on a schedule governed by the PLC. If the conveyor delivers a partial charge because its speed was never calibrated against the 15–20 s molding cycle, the vibration phase starts with an uneven fill. Block density varies from one end of the pallet to the other, and the buyer blames the press when the fault lies upstream [NEED_CITE: material feed consistency and block strength correlation].
Reading the Numbers Without Getting Misled
A vibration force of 100 kN applied across a platform at 0–60 Hz is what compacts the concrete into a dense, structurally sound block. The hydraulic demolding system then pushes the finished product off without cracking green edges. Both forces must work in concert: high vibration without sufficient hydraulic hold produces a block that crumbles on the pallet; high pressure without adequate vibration leaves voids inside the wall. The PLC coordinates these phases so the operator sets the recipe once and the line repeats it across every cycle.
Pallet size is the second specification that reaches beyond the press itself. A 1150×700 mm board must fit the curing racks already in the buyer’s yard and match the fork spacing of the forklift on site. Specifying a different pallet dimension means rebuilding the curing area or buying new handling equipment — costs that never appear on the machine quotation.
What Happens When Line Stations Are Sized Separately
When a buyer sources the press from one supplier and the pallet handling from another, nobody owns the cycle-time gap between them. The press completes a moulding cycle in 15–20 s, but the stacking station takes 25 s to clear a finished pallet. Over an hour that gap swallows a significant portion of potential output, and over a month it represents a measurable volume of unsold inventory [NEED_CITE: impact of station mismatch on monthly block output].
Why Sourcing the Line as One Package Changes the Conversation
Shandong Shiyue Intelligent Machinery specifies the QT7-15 together with its pallet feed machine, conveyor, storage hopper, hydraulic unit and PLC cabinet as a single matched system. Every component is selected so the slowest station still falls within the press cycle window. Configuration starts from the buyer’s actual mix design and local aggregate, not a catalogue default, which means the vibration frequency and hydraulic pressure are set for materials the buyer can actually source.
Documentation & Verification
- Line layout drawing with cycle time stated at each station per block format
- Machine specification sheet covering pallet size, power and vibration ratings
- Mould drawing and format list for every block type in the quotation
- Voltage, frequency and PLC display language confirmation before shipment
- Factory test record on the buyer’s target block format before dispatch
- Hydraulic and electrical schematic for on-site maintenance reference
Installation, Commissioning & Support
- Foundation plan dimensioned for the 8 T machine mass and vibration load
- Power supply sized for 45 kW total draw with dedicated circuit breaker
- PLC cabinet wired and labeled in the buyer’s confirmed operating language
- First-run parameter tuning on the buyer’s local aggregate and mix ratio
- Operator training covering mould change, pallet feed adjustment and daily checks
- Wear parts list with hydraulic seal and vibration motor replacement intervals
What to Prepare Before Requesting a Quotation
Send the target block formats and the daily volume you need to hit on each one. Include the raw materials available locally — cement type, aggregate grading, sand source — and the dimensions of your curing yard. Confirm the voltage and frequency at the site and the language your operators will need on the PLC touch screen.
Frequently Asked Questions
Q: How are upstream feeding and downstream pallet handling matched to the QT7-15 press cycle?
A: Each station — storage hopper, conveyor, pallet feed machine — is specified so its cycle time falls within the 15–20 s press window. The line layout drawing states the timing at every station for each block format, ensuring the press never waits for material or pallet clearance.
Q: Is stacking and curing rack handling included in the block machine production line quotation?
A: The standard component list covers the press, pallet feed, conveyor, hopper, hydraulic unit and PLC cabinet. Stacking method depends on automation level selected; buyers should confirm whether automatic stacking or manual handling is quoted to avoid surprise labour costs on the floor.
Q: How is pallet size and material chosen to fit my existing curing area?
A: The 1150×700 mm pallet is the baseline. Before order confirmation, we verify rack spacing, yard dimensions and forklift fork width at your site so the boards in the quotation match what you already handle. Changing pallet size later affects the entire feed and return loop.
Q: What documentation comes with the line to confirm station-by-station capacity?
A: You receive a line layout drawing showing how pallet feed, press, conveyor and stacking stations connect, with cycle time at each station stated per block format. A factory test record on your chosen format is completed before dispatch.
Q: How do I add new block formats later without replacing connected stations?
A: The quick mould replacement system lets the same press produce hollow blocks and pavers. Upstream and downstream stations handle any format that fits the 1150×700 mm pallet, so adding a new mould is a press-side change, not a full line rebuild.



