
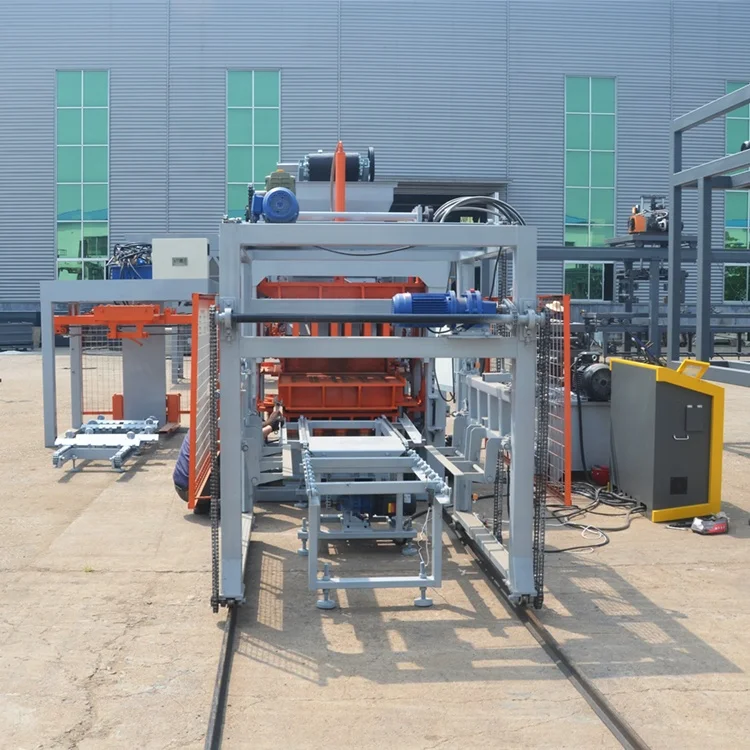
Matched Line Configuration — the QT6-15 press is specified together with raw material feeding, mixing, pallet handling, stacking and curing stations so that every station’s cycle time aligns and the press never waits for material or pallets.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT6-15 |
| Product Type | Cement Block Making Machine |
| Overall Dimensions (L×W×H) | 8200×1700×2950 mm |
| Pallet Size | 880×850 mm |
| Vibration Form | Platform Vibration |
| Vibration Frequency | 0-60 Hz |
| Vibration Force | 45 kN |
| Moulding Mode | Load automatically, vibration moulding |
| Molding Cycle | 15-20 s |
| Demolding Method | Hydraulic |
| Hydraulic System | Independent integrated type hydraulic station |
| Overall Power | 37 kW |
| Total Mass | 7 T |
| Factory Area Required | 1200 m² |
| Control System | PLC (Programmable Controller) with touch screen interface |
| Raw Material Adaptability | Waste ash, slag, various aggregates |
| Block Compressive Strength | More than 15 MPa |
| Output Capacity (Hollow block 400×200×200 mm) | 8640-11520 pcs/8hr |
| Output Capacity (Hollow block 400×150×200 mm) | 11520-15360 pcs/8hr |
| Output Capacity (Solid brick 240×115×53 mm) | 46080-61440 pcs/8hr |
| Output Capacity (Rectangular brick 200×100×60 mm) | 17280-23040 pcs/8hr (basis: 20-25s cycle) |
| Output Capacity (Zigzag brick 225×112.5×60 mm) | 17280-23040 pcs/8hr (basis: 20-25s cycle) |
| Warranty | 1 year for whole machine (excluding spare parts) |
| Standards | CE declaration where applicable |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production plants | Crushed stone, cement, sand, and waste ash blends |
| Solid brick manufacturing | Slag, fly ash, and fine aggregate mixes |
| Paving brick production (rectangular and zigzag) | Coarse aggregate with cement binder for high-strength pavers |
| On-site block production for housing projects | Locally sourced aggregates matched to regional compressive strength standards |
| Concrete product manufacturers expanding format range | Multiple mould formats on a single press with pallet line integration |
Why Quoted Cycles per Hour Miss the Real Daily Output
The press cycle is only as fast as the slowest station upstream or downstream of it.
A cement block making machine production line often quotes capacity based on the press cycle alone — say, 15-20 seconds per mould. But if the mixer discharges too slowly, the host waits ten or more seconds every cycle. If the pallet return conveyor cannot keep pace, the press sits idle again. I once visited a site where a mid-tier press lost roughly three thousand blocks a day simply because the batching and mixing station had never been timed against the press cycle [NEED_CITE: line synchronization losses in block production]. The turnkey block plant only delivers its quoted output when every station — feeding, mixing, pallet circulation, stacking — is calculated against the same rhythm.
Station Synchronization Across the Block Line
The QT6-15 operates on a 15-20 second molding cycle, which sets the tempo every other station must meet. Raw material feeding must deliver a consistent batch to the mixer within that window, and the mixer must discharge fully before the next cycle begins. A cement block making machine production line configured around this press accounts for mixing time, conveyor speed, and pallet return rate so the press is never starved.
Pallet Circulation and Curing Area Alignment
The 880×850 mm pallet size is not chosen arbitrarily — it must match the curing racks the buyer already uses or plans to build, as well as the forklift fork spacing on site. When pallets are sized correctly, wet blocks move from the press to the curing area without manual rehandling. The turnkey block plant layout specifies pallet quantity, rack configuration, and return conveyor length so that the curing loop does not become a bottleneck during an eight-hour shift [NEED_CITE: pallet circulation planning for block plants].
Hydraulic Isolation for Consistent Line Operation
The independent integrated hydraulic station sits apart from the main vibration and dust zone of the press. In a block line running continuously, hydraulic fluid temperature and contamination are primary causes of pressure drift. Isolating the station means the vibration force and demolding pressure stay stable throughout the shift, which keeps block compressive strength above 15 MPa from the first cycle to the last. This matters especially when the line is producing multiple formats in a single day and the hydraulic system must respond to different mould pressures without recalibration delays.
Reading the Specs That Determine Line Rhythm
Platform vibration at 0-60 Hz with 45 kN force is the core forming mechanism here. The frequency range allows the operator to tune vibration to the specific mix — finer aggregates like fly ash need higher frequency and lower amplitude, while coarse crushed stone needs lower frequency and higher force to consolidate properly. The PLC touch screen interface lets the operator store these settings per mould format, so switching from hollow blocks to paving bricks does not require manual trial and error. The overall power of 37 kW covers the press itself; the full cement block making machine production line will draw additional power for the mixer, conveyors, and stacker, so the site electrical plan must account for total connected load. The 1200 m² factory area requirement includes space for the press, raw material storage, mixer station, pallet circulation loop, and curing racks — a tighter footprint forces compromises on curing capacity that reduce real output.
What Happens When Line Stations Are Specified Separately
I have seen buyers source the press from one supplier and the mixer, pallet feeder, and stacker from three others. The result is a line where the mixer output does not match the press demand, the pallet feeder jams because the pallet dimensions are slightly off tolerance, and the stacker cannot handle the cycle speed. Each station works on its own, but together they create stoppages that cut real daily output well below the sum of their individual ratings [NEED_CITE: integration issues in multi-supplier block lines]. The hidden cost is not the equipment — it is the lost production hours and the manual labor required to compensate for mismatched station speeds.
What We Configure Before We Quote
The QT6-15 is never quoted as a standalone press. The block machinery focus means the machine, mould, pallet, and handling equipment are specified as one matched system. Configuration starts with the buyer’s actual mix design and local aggregate, not a catalogue default, so the vibration force and hydraulic pressure are set to produce blocks meeting the required strength. Mould design covers the formats the buyer’s market actually sells, including custom drawings when standard formats do not match local building standards. Automation level is selectable — a buyer can start with semi-automatic pallet handling and add automatic stacking and cubing later without replacing the press. Installation support includes operator training on the PLC interface and line synchronization procedures [NEED_CITE: block machine installation and commissioning practices].
Documentation & Verification
- Line layout drawing with capacity calculation stated per block format and assumed cycle time
- Machine specification sheet covering QT6-15 press, hydraulic station, and PLC control parameters
- Mould drawing and format list matching the buyer’s target block dimensions
- Pallet specification confirming 880×850 mm dimensions and material grade
- Hydraulic and electrical schematic for site connection and maintenance reference
- Factory test record run on the buyer’s specified block format before dispatch
Installation, Commissioning & Support
- Foundation plan sized to the 8200×1700 mm footprint and 7 T mass with vibration isolation pads
- Dedicated electrical circuit planned for the 37 kW press plus upstream mixer and downstream stacker loads
- Machine arrives dismantled for container loading with reassembly supervised on site
- First-run commissioning includes PLC touch screen parameter setting for each mould format
- Operator training covers molding cycle adjustment, mould change procedure, and daily hydraulic checks
- Wear parts list and mould maintenance schedule provided with recommended replacement intervals
What We Need to Start Your Line Configuration
Send us the block formats your market requires — hollow, solid, paving, or a combination — along with your target daily output and the raw materials available locally. Include your site dimensions, existing curing area layout, and forklift specifications so we can confirm pallet sizing. Let us know your local voltage and frequency, preferred PLC display language, and whether you need the full line from raw material feeding through to cubing or only specific stations.
Frequently Asked Questions
Q: How is line capacity calculated per block format, and what cycle time does each format assume?
A: Capacity is calculated per format based on the molding cycle the QT6-15 achieves with that specific mould. Hollow blocks at 400×200×200 mm run on a 15-20 second cycle, while pavers may require 20-25 seconds. The line capacity calculation states the exact format and cycle time assumed, so you can verify the daily output against your production target before placing an order.
Q: Which supporting stations are included and where do cycle times need to match?
A: A complete cement block making machine production line covers raw material feeding, mixing, pallet feeding, stacking, and curing rack handling. Each station’s cycle must align with the press molding cycle so the QT6-15 is never left waiting. The line layout specifies the timing relationship between stations and identifies where buffer capacity is needed.
Q: How is pallet size chosen against my existing curing area and forklift?
A: The 880×850 mm pallet is confirmed against your curing rack spacing and forklift fork dimensions. If your existing racks use a different size, the pallet specification is adjusted accordingly so wet blocks transfer directly from the press to curing without manual rehandling or rack modification.
Q: What voltage, frequency and PLC language will be confirmed before shipment?
A: Voltage, frequency, and PLC display language are confirmed during the quotation stage, before production begins. This ensures the electrical system matches your site supply and the touch screen interface is readable by your operators on the first day of commissioning.
Q: What is the factory area requirement and how should the line layout fit my site?
A: The QT6-15 line requires approximately 1200 m² to accommodate the press, raw material storage, mixer station, pallet circulation loop, and curing racks. The line layout is drawn to your actual site dimensions, positioning each station so material flow follows a logical path from batching to cured product dispatch.



