
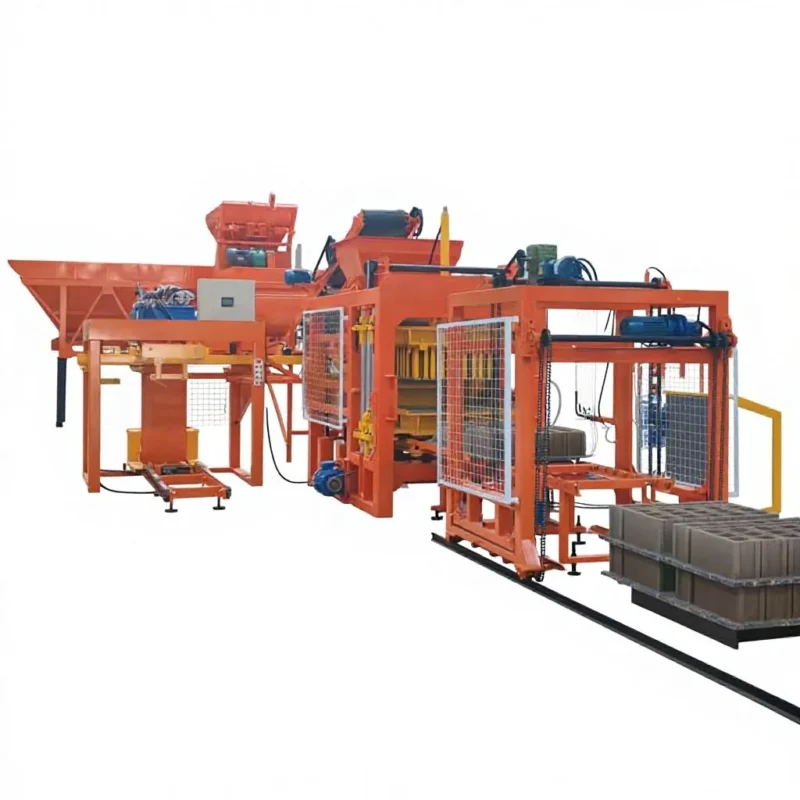
Integrated Line Configuration — The QT6-15 block machine production line is specified as a matched system where feeding, mixing, pallet circulation, and stacking stations are balanced to the press cycle so the host machine never idles waiting for upstream or downstream equipment.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT6-15 |
| Product Type | Hydraulic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 8200×1700×2950 mm |
| Total Mass | 7 T |
| Overall Power | 37 kW |
| Vibration Force | 45 kN |
| Vibration Frequency | 0-60 Hz |
| Vibration Form | Platform Vibration |
| Pallet Size | 880×850 mm |
| Moulding Mode | Automatic load, vibration moulding |
| Demolding Method | Hydraulic |
| Control System | PLC with touch screen interface |
| Hydraulic System | Independent integrated hydraulic station |
| Molding Cycle | 15-20 s (basis not stated in source — confirm block format / material / thickness) |
| Output: Hollow Block 400×200×200 mm | 1080-1440 pcs/hour, 8640-11520 pcs/8hr |
| Output: Hollow Block 400×150×200 mm | 1440-1920 pcs/hour, 11520-15360 pcs/8hr |
| Output: Solid Brick 240×115×53 mm | 5760-7680 pcs/hour, 46080-61440 pcs/8hr |
| Output: Rectangular Paver 200×100×60 mm | 2160-2880 pcs/hour (cycle 20-25 s), 17280-23040 pcs/8hr |
| Block Compressive Strength | >15 MPa |
| Recommended Factory Area | 1200 m² |
| Automation Level | High (automatic loading, PLC process control, fault diagnosis) |
| Warranty | 1 year for whole machine (excluding spare parts) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for wall construction | Crushed stone, sand, cement, and fly ash aggregates |
| Interlocking and rectangular paving brick manufacturing | Fine aggregates, pigment, and cement for high-density pavers |
| Solid standard brick production | River sand, slag, waste ash, and cement mixtures |
| On-site block production for housing projects | Locally sourced aggregate with reduced cement dosage |
| Multi-format building material supply | Various moulds for hollow, solid, and paving formats on a single line |
Why Line Balance Matters More Than Press Speed
The host press capacity is only as real as the slowest station feeding it or clearing it.
A quotation might state a high cycle rate for the QT6-15 block machine production line, but if the mixer discharges slower than the press consumes, or if pallets are not returned fast enough, the press sits idle. I once saw a plant where the press was capable of running continuously, yet the actual daily throughput was barely half the quoted figure because the pallet return conveyor and stacking station could not keep pace [NEED_CITE: common causes of throughput loss in block production lines]. When evaluating any block line, the capacity calculation must trace every station from raw material intake through to cured and stacked output.
Matching Every Station to the Press Cycle
The QT6-15 block machine production line operates on a platform vibration system with a moulding cycle of 15-20 seconds depending on block format. For the line to deliver its rated output, the raw material batching and mixing station must discharge a full batch within that same window. If the mixer takes longer, the press waits. We specify the mixer capacity, discharge gate type, and conveyor speed so that material arrives at the hopper before the press calls for it, not after.
Pallet Circulation and Downstream Handling
The 880×850 mm pallet size determines how many blocks are pressed per cycle, but it also dictates the pallet return conveyor length, the stacking mechanism reach, and the curing rack dimensions. If the buyer already owns forklifts or curing racks sized for a different pallet, the entire downstream flow breaks down. The QT6-15 block machine production line specification includes pallet material selection and curing rack layout so that freshly pressed blocks move from the press to the curing area without manual intervention or bottleneck [NEED_CITE: pallet handling best practices in concrete block plants].
Reading the Specs That Actually Affect Output
The 45 kN vibration force and adjustable 0-60 Hz frequency work together to compact the concrete mix into the mould. Higher frequency with lower force suits fine aggregates and thinner pavers, while lower frequency with sustained force is needed for larger hollow blocks with coarse aggregate. The independent integrated hydraulic station sits apart from the main frame, reducing dust ingress and vibration transmission to hydraulic valves, which extends seal life. The PLC with touch screen interface coordinates the automatic loading sequence, vibration duration, and hydraulic demoulding in a single cycle, and includes fault diagnosis to identify which station has stopped the line.
The Cost of Ignoring Line Integration
When supporting equipment is excluded from the quotation, the buyer often discovers after delivery that pallets must be moved by hand, stacking is done manually, and curing racks do not match the pallet dimensions. The result is a press that runs well in isolation but produces far less than promised because the surrounding workflow cannot keep up [NEED_CITE: hidden costs of incomplete block line quotations]. Voltage, frequency, and PLC display language, if not confirmed before production, delay commissioning further when the machine arrives on site with incompatible electrical connections or an interface the operators cannot read.
Why Source the Complete Line Here
Block machinery is the sole focus, so the QT6-15 block machine production line is configured as one matched system rather than assembled from separate suppliers who do not communicate. The configuration is set against the buyer’s actual mix design and local aggregate, not a catalogue default, ensuring vibration force and hydraulic pressure are appropriate for the material available. Mould design covers the formats the buyer’s market actually sells, including custom drawings when standard moulds do not match local block dimensions. Automation level is selectable, allowing a buyer to start with semi-automatic pallet handling and upgrade to full automatic stacking and cubing later. Installation support includes operator training so the team understands not just the press but the entire line sequence.
Documentation & Verification
- Line layout drawing with capacity calculation stated per block format
- Pallet specification matched to your curing area and forklift dimensions
- Voltage, frequency, and PLC display language confirmation sheet before production
- Hydraulic and electrical schematic for local maintenance teams
- Factory test record on your target block format before dispatch
- Wear parts and mould list with part numbers for reordering
Installation, Commissioning & Support
- Foundation plan based on 8200×1700 mm footprint and 7 T mass for stable mounting
- 37 kW power requirement confirmed with dedicated circuit and correct voltage
- Machine dismantled for container loading and reassembled on site with alignment checks
- PLC touch screen commissioning with cycle time tuning for your specific block format
- Operator training covering mould change, fault diagnosis, and daily maintenance routines
- Hydraulic seal and vibration motor spare parts list provided at delivery
What We Need to Quote Your Line Accurately
To configure the QT6-15 block machine production line for your plant, please share your target block formats with dimensions, the daily output you need per format, and the raw materials available locally including aggregate type and cement supply. Your workshop area and ceiling height, along with the voltage and frequency at your site, determine the supporting equipment layout. Let us also know if you have existing forklifts, curing racks, or pallets so the line can be matched to your current infrastructure.
Frequently Asked Questions
Q: How is line throughput verified when each station must match the press cycle time?
A: We calculate throughput per block format, then check that the mixer discharge rate, pallet return speed, and stacking cycle all complete within the press moulding cycle. If any station is slower, we resize it before the quotation is finalised so the press never waits.
Q: Which supporting equipment is included in the line quotation and which is buyer-supplied?
A: Raw material feeding, mixing, pallet feeding, automatic stacking, and curing rack handling are specified in the line proposal. Items such as the curing yard surface, external water supply, and main power transformer are typically buyer-supplied and noted clearly in the scope document.
Q: How are pallet size and material selected to match the curing area and forklift on site?
A: We start with the 880×850 mm pallet required by the press, then confirm your curing rack spacing and forklift tine width. If your existing infrastructure uses a different pallet dimension, we discuss whether to adapt the line or adjust the curing setup before production begins.
Q: How is the QT6-15 integrated with upstream batching and downstream stacking systems?
A: The PLC coordinates the batching plant discharge, press cycle, and stacker operation through a shared control sequence. Each station receives a signal from the press when a cycle completes, triggering the next material batch and pallet movement so the entire line runs as one continuous flow.
Q: What factory area and utility requirements does the complete line demand?
A: The recommended factory area is 1200 m², which covers the press, mixer, pallet circulation, stacking zone, and curing rack storage. The 37 kW total power must be supplied at the correct voltage and frequency, with a dedicated circuit and adequate earthing for the PLC and hydraulic station.



