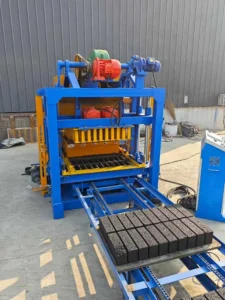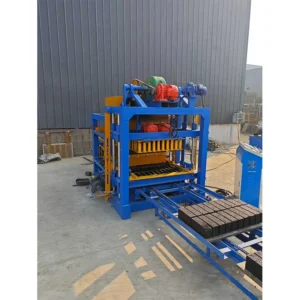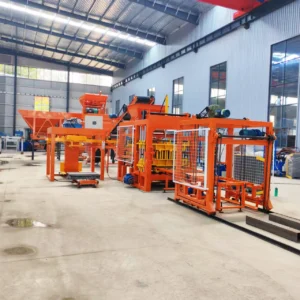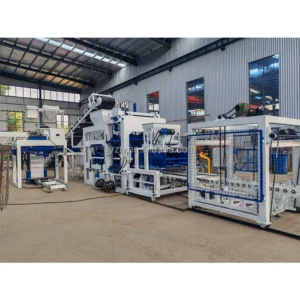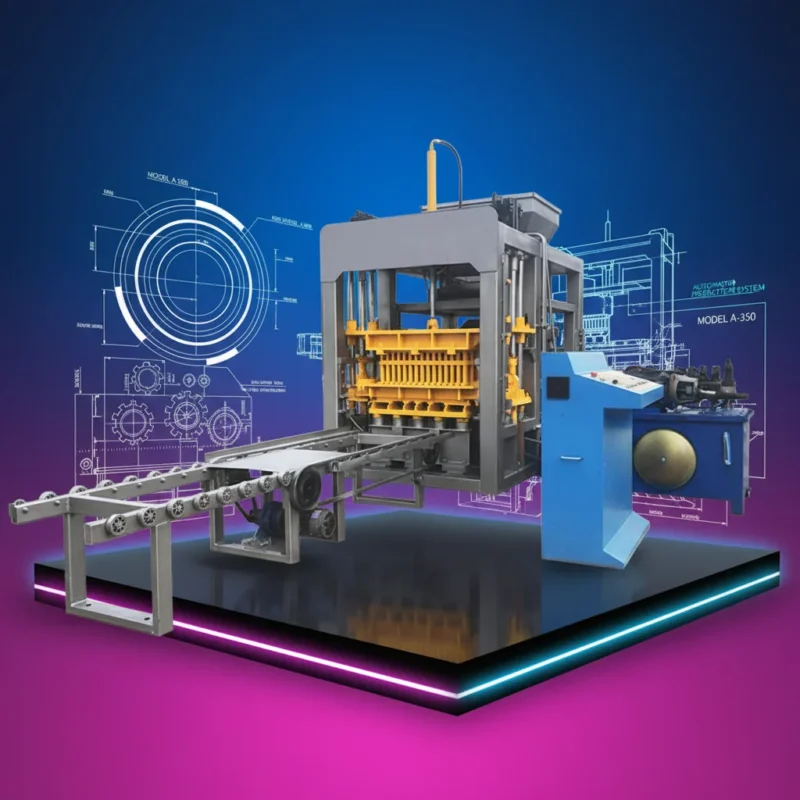
Station Timing Mastery — Every QT5-15 line we configure maps mixer discharge, pallet feed and stacker index to the press cycle so the host machine never idles waiting upstream or downstream.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT5-15 |
| Product Type | Automatic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 7400 × 1950 × 2800 mm |
| Total Mass | 5000 kg |
| Vibration Form | Platform vibration |
| Vibration Frequency Range | 0–60 Hz |
| Vibration Force | 80 kN |
| Moulding Mode | Automatic loading, vibration moulding |
| Demolding Method | Hydraulic |
| Pallet Size | 1100 × 550 mm |
| Molding Cycle | 15–20 s (basis not stated in source — confirm block format / material / thickness) |
| Overall Power | 32 kW |
| Control System | PLC with touch screen interface |
| Hydraulic System | Independent integrated hydraulic station |
| Block Compressive Strength | >15 MPa |
| Factory Area Required | 1000 m² |
| Raw Material Compatibility | Fly ash (up to 70%), slag, gangue, sand, crushed stone, cement, water |
| Output — Hollow Block 400×200×200 mm | 5 pcs/mould, 900–1200 pcs/h, 7200–9600 pcs/8hr (cycle 15–20 s) |
| Output — Hollow Block 400×150×200 mm | 6 pcs/mould, 1080–1440 pcs/h, 8640–11520 pcs/8hr (cycle 15–20 s) |
| Output — Solid Brick 240×115×53 mm | 32 pcs/mould, 5760–7680 pcs/h, 46080–61440 pcs/8hr (cycle 15–20 s) |
| Output — Rectangular Paver 200×100×60 mm | 25 pcs/mould, 3600–4500 pcs/h, 28800–36000 pcs/8hr (cycle 20–25 s) |
| Output — Zigzag Paver 225×112.5×60 mm | 16 pcs/mould, 2304–2880 pcs/h, 18432–23040 pcs/8hr (cycle 20–25 s) |
| Automation Level | Automatic (pallet feeding, material feeding, vibrating, demoulding) |
| Electrical & Hydraulic Components | Original imported or Chinese well-known brand |
| Warranty | 1 year for the whole machine (excluding spare parts) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for building walls and partitions | Fly ash, sand, crushed stone, cement blends |
| Solid brick production for structural and infill masonry | Sand-cement or slag-cement mixes |
| Rectangular and interlocking paver production | Crushed stone and cement for roads, walkways and yards |
| Industrial residue utilization in block manufacturing | Fly ash (up to 70%), slag, gangue as aggregate replacement |
| Fixed block plant production | Lines sized to approximately 1000 m² factory area |
| On-site contractor block production | Project-volume runs with local aggregate sourcing |
What "900 Pieces per Hour" Leaves Out About Line Capacity
Cycle time only matters when every station around the press can keep up.
An automatic block machine production line rated at a certain output figure means nothing if the mixer takes longer to discharge than the press takes to cycle, or if the stacker cannot index pallets fast enough to clear the press table. I have watched sites in Latin America where a fast-pressing host machine sat idle because the batching station was still weighing the next charge, burning through cement and labour while the operator waited. The QT5-15 completes a mould cycle in 15–20 seconds, but that speed is only reachable when raw material feeding, pallet feeding, and downstream stacking are all timed to the same beat. [NEED_CITE: block plant line synchronization principles for continuous production]
Mapping Every Station to the Press Cycle
The automatic block machine production line built around the QT5-15 connects raw material feeding, mixing, pallet feeding, pressing, and stacking into a single timed sequence. The PLC touch screen interface coordinates each station so the press receives a charged pallet and fresh material within the molding cycle window. When one station drifts — a mixer discharge gate that sticks, a pallet feeder that misaligns — the PLC flags the fault before the press attempts a cycle with incomplete input, preventing wasted material and damaged moulds.
Where the Independent Hydraulic Station Fits
The QT5-15 uses an independent integrated hydraulic station physically separated from the press vibration zone and dust fallout. On a busy block line, hydraulic oil contamination from cement dust is a common cause of valve sticking and seal wear. Keeping the hydraulic unit in its own enclosure means oil stays cleaner across long shifts, and maintenance access does not require reaching over the vibrating table. This layout also lets the hydraulic lines run a short, direct path to the demolding cylinders, reducing pressure drop and response lag during the mould release stroke. [NEED_CITE: hydraulic station isolation in high-vibration block presses]
Reading the Numbers That Actually Matter
The vibration force of 80 kN at up to 60 Hz works together with hydraulic pressure to compact the mix into the mould cavity. Higher frequency alone does not guarantee block density — the force must be matched to the buyer’s specific aggregate gradation and cement content to achieve the rated compressive strength above 15 MPa. The 1100 × 550 mm pallet size determines how many blocks fit per cycle, and it also dictates the curing rack dimensions and forklift tine spacing downstream. The overall power of 32 kW covers the press itself; the full line with mixer, feeder, and stacker will draw additional load, so the site electrical supply must be sized for the entire station list, not just the host machine. Quick mould replacement lets the operator switch between hollow block, solid brick, and paver formats, but the changeover time must be factored into daily planning if the production schedule calls for multiple formats per shift.
The Hidden Cost of Mismatched Line Stations
When the quotation covers only the press and the buyer assumes the rest of the line is included, the project stalls at commissioning. Pallets pile up on the press table because no stacker was ordered, and workers resort to manual handling that erodes the cycle time advantage the QT5-15 was meant to deliver. A mixer that is too small forces the press into a wait state every few cycles, and a curing rack system that does not accept the 1100 × 550 mm pallet forces a costly pallet replacement or a rack rebuild. These are not equipment failures — they are specification gaps that surface only after the machine is on the floor. [NEED_CITE: common block line specification gaps at commissioning]
Why Buyers Source the Full Line Here
Block machinery is our single focus, which means the QT5-15 press, its moulds, pallets, and every handling station are specified as one matched system rather than assembled from separate suppliers. We set the configuration against your actual mix design and local aggregate, not a catalogue default, so vibration force and hydraulic pressure are tuned for your material. Mould design covers the formats your market actually sells, including custom drawings when standard cavities do not match. Automation level is selectable — you can start with the automatic press and add a stacker or cuber later as volume grows. Installation support includes operator training so the crew knows how the PLC coordinates each station before the first production shift.
Documentation & Verification
- Line layout and capacity calculation stating the block format assumed for every output figure
- Machine specification sheet covering the QT5-15 press and all connected line stations
- Mould drawing and format list showing cavity count per block type
- Pallet specification matching the 1100 × 550 mm size to your curing racks and forklift
- Voltage, frequency, and PLC display language confirmation before production begins
- Factory test record documenting cycle timing with your chosen block format
Installation, Commissioning & Support
- Foundation plan sized to the QT5-15 footprint of 7400 × 1950 mm with vibration isolation pads
- Electrical supply rated for 32 kW press load plus all auxiliary station motors on dedicated circuits
- Hydraulic station filled and bled on site after transport, with line pressure verified before first cycle
- PLC touch screen language set to operator preference during commissioning
- Mould change procedure trained on site so format switching fits within a planned shift window
- Wear parts list supplied with recommended reorder intervals for hydraulic seals and vibration elements
What to Share Before Quoting
To size an automatic block machine production line around the QT5-15, send us the block formats your market sells along with target daily output per format, your local raw material source and typical aggregate gradation, and the factory area available for the full line including curing space. Confirm the local voltage and frequency, the PLC display language your operators need, and which downstream stations — stacker, curing rack handler, cuber — you want included in the scope so the quotation covers every station from mixer to pallet return.
Frequently Asked Questions
Q: How is line capacity calculated and which block format does each output figure assume?
A: Every capacity figure on this page is tied to a specific block format, mould cavity count, and cycle time range. The hollow block 400×200×200 mm output assumes five pieces per mould at a 15–20 second cycle. When you request a proposal, we provide a capacity table that lists each format you plan to produce with its own realistic hourly and shift output, so there is no ambiguity about what the line will deliver.
Q: How do upstream and downstream stations need to be timed so the press cycle is not the bottleneck?
A: The mixer must discharge a full charge within the molding cycle window, the pallet feeder must place and align a pallet before the press is ready, and the stacker must clear pressed pallets before the next cycle completes. Our line layout document maps each station’s cycle against the QT5-15 timing, highlighting any station that needs a faster rating or buffer capacity.
Q: What factory area and utility requirements does the complete line need beyond the press?
A: The QT5-15 press alone requires part of a 1000 m² area, but the full line with mixer, raw material bins, pallet return conveyor, stacking station, and curing racks needs the entire footprint. Power supply must cover 32 kW for the press plus additional load for every auxiliary motor. We provide a layout drawing showing station placement and utility connection points before production starts.
Q: Which line stations are included in the quotation and which are optional?
A: Our quotation lists every station individually — raw material feeding, mixing, pallet feeding, the QT5-15 press, stacking, and curing rack handling — so you see exactly what is in scope. Stations you already have or plan to source locally can be excluded, and we note the interface specifications your existing equipment must meet to connect to the line.
Q: How is the PLC control language and electrical configuration confirmed before shipment?
A: During the quotation stage we collect your site voltage, frequency, and preferred PLC display language. These values are written into the production order and verified during the factory test. The touch screen is set to your language before packing, so operators can begin familiarization on day one of commissioning without waiting for a software change.