
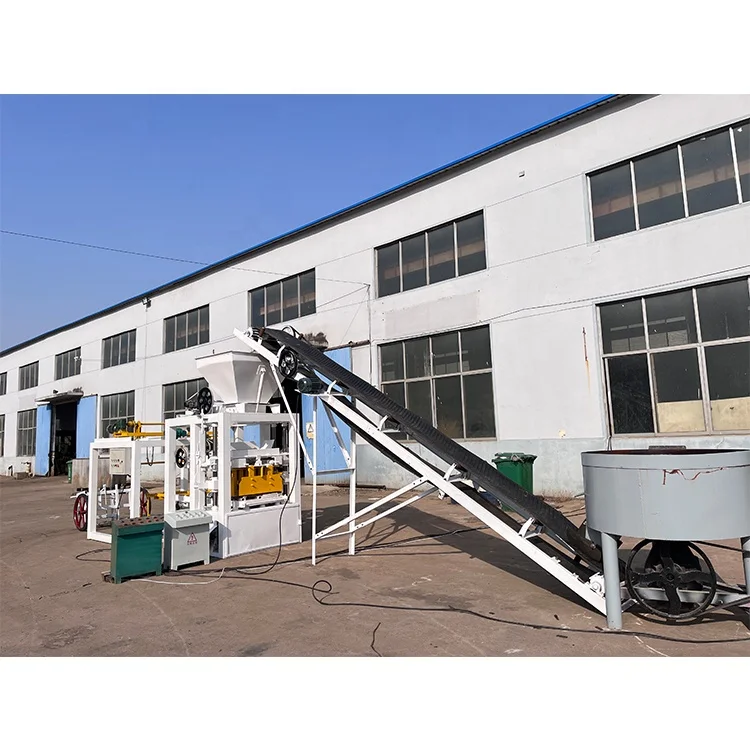
Matched line rhythm — We size the mixer, pallet feeder, and press around your actual curing rack and forklift, not a catalogue default, so the Semi-Automatic Block Machine production line never waits on upstream or downstream stations.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Semi-Automatic Concrete Block Making Machine |
| Model | Qt4-24 |
| Overall Dimensions (L×W×H) | 2060 × 1730 × 2580 mm |
| Molding Cycle | 26 s |
| Vibration Frequency | 4200 r/min |
| Vibration Force (Exciting Power) | 35.5 kN |
| Total Power | 14.25 kW |
| Mixer Model | JQ350 |
| Pallet Size | 850 × 450 × 20 mm |
| Net Weight | 1800 kg |
| Applied Products | Concrete blocks, hollow block (8 inch, 6 inch), solid brick |
| Raw Materials | Crushed stones, sand, cement, dust, fly ash |
| Output Capacity (Hollow Block 390×190×190mm) | 480 pcs/hr, 3800 pcs/8hr |
| Output Capacity (Hollow Block 400×150×200mm) | 600 pcs/hr, 4800 pcs/8hr |
| Output Capacity (Solid Brick 240×115×53mm) | 2100 pcs/hr, 17000 pcs/8hr |
| Automation Level | Semi-automatic (four guide pillars, automatic mould movement) |
| Standards | CE (basis not stated in source) |
Application Suitability
| Application | Material or Output |
|---|---|
| Small to medium concrete block plants | Crushed stone, sand, cement, fly ash blends for hollow and solid formats |
| On-site hollow block production for contractors | 8-inch and 6-inch hollow blocks from locally sourced aggregate |
| Solid brick runs for masonry supply | 240×115×53 mm solid bricks at high cycle frequency |
| First-plant entrepreneurs with limited footprint | Semi-fixed line layout with manual or semi-auto pallet handling |
What "480 Blocks per Hour" Actually Means on the Floor
Cycle time only holds when the mixer and pallet feeder keep pace with the press.
Buyers often see a rated output number and assume the entire block line and supporting equipment will naturally fall into step. In practice, a 26-second molding cycle demands that the JQ350 mixer delivers a fresh batch every cycle and that pallets are positioned without delay. When any station lags, the press sits idle, and daily tonnage drops well below the quoted figure [NEED_CITE: synchronization of station cycle times in semi-automatic block lines]. I have watched lines where the mixer was undersized for the press, turning a theoretical eight-hour shift into a ten-hour marathon just to hit the same pallet count.
How Station Timing Shapes Your Daily Pallet Count
The Semi-Automatic Block Machine production line works like a relay race. The press is the fastest runner, but if the JQ350 mixer takes longer than 26 seconds to discharge a homogenous batch, the press waits. We calculate mixer discharge time against your specific water-to-cement ratio and aggregate gradation, because a stiffer mix takes longer to release from the pan. Matching these intervals is the difference between a line that hums and one that stutters through every shift.
Pallet Flow and Curing Rack Alignment
Pallet size directly dictates how many blocks travel to the curing area per trip and how your existing forklift handles the load. The 850×450×20 mm pallet specified for the Qt4-24 fits common curing rack slots, but only if the rack spacing was planned around that exact dimension [NEED_CITE: pallet-to-rack clearance standards in block curing]. A mismatch means either wasted rack space or pallets that cannot slide in, forcing operators to restack by hand — exactly the bottleneck the line was supposed to eliminate.
Reading the Vibration and Pressure Numbers Together
The 35.5 kN exciting power and 4200 r/min vibration frequency work in concert to compact the concrete mix inside the mould cavity. Higher frequency with insufficient force leaves voids in the block core; higher force with low frequency risks over-compacting the bottom while the top stays loose. For the Qt4-24, these two values are balanced for standard crushed-stone and sand mixes. If your local aggregate contains a high clay fraction, the mix absorbs vibration differently, and we adjust the vibration duration rather than the force rating to maintain consistent density throughout the block cross-section.
The Hidden Cost of Ignoring Upstream and Downstream Rhythm
When the block line and supporting equipment is specified station by station without a unified cycle calculation, the consequences surface weeks after commissioning. Operators add extra mixing time to compensate for poor blend quality, which slows the entire line. Pallets pile up at the press exit because the curing area cannot absorb them fast enough, and green blocks get knocked off-stack by forklift traffic. These are not machine faults — they are planning gaps that no amount of on-site adjustment can fully correct [NEED_CITE: common commissioning failures in semi-automatic block plants].
Why Sourcing the Whole Line from One Supplier Matters
Block machinery as a single focus means the Qt4-24 press, JQ350 mixer, pallets, and handling gear are specified as one matched system. Configuration is set against your actual mix design, local aggregate, and target block format rather than a catalogue default. Mould design covers the formats your market actually sells, including custom drawings when standard cavities do not fit. Automation level is selectable, so you can start with semi-automatic pallet handling and add automatic stacking later. Installation support includes operator training on your specific raw material, not a generic video.
Documentation & Verification
- Line layout drawing stating pallet count per hour for your chosen block format
- Machine specification sheet confirming 14.25 kW total power and 35.5 kN vibration force
- Mould drawing with cavity dimensions matched to your target hollow or solid block
- Pallet specification confirming 850×450×20 mm size and load rating for curing racks
- Voltage and control language confirmation sheet signed before production begins
- Factory test record running your submitted aggregate sample through a full molding cycle
Installation, Commissioning & Support
- Foundation plan sized to the 2060×1730 mm footprint with anchor bolt positions marked
- Dedicated 14.25 kW circuit with voltage and frequency confirmed for your local grid
- Machine shipped partially assembled; press frame, mixer, and pallet feeder bolted on site
- First-run parameter setting using your local aggregate sample to dial in vibration duration
- Operator training covering mould change procedure on the four-guide-pillar system
- Wear parts list identifying vibration motor bearings and mould liner replacement intervals
Before You Request a Quote
Send us your target block format with exact dimensions, the daily pallet count you need to hit, and a sample of your local aggregate including sand and crushed stone. Tell us the voltage and frequency at your site, the language your operators read on a control panel, and the forklift model you already use so we can confirm pallet compatibility. If you have an existing curing area, share its rack spacing and total square meters.
Frequently Asked Questions
Q: How do I match the JQ350 mixer output with the 26-second press cycle?
A: We calculate the mixer discharge time based on your specific water-to-cement ratio and aggregate size. A stiffer mix with low slump takes longer to release from the pan. If discharge exceeds 26 seconds, we either adjust the batch size or recommend a larger mixer so the Qt4-24 press never waits for material between cycles.
Q: What pallet handling systems work with the 850×450 mm pallet?
A: Manual pallet carts, semi-automatic chain conveyors, and simple roller racks all handle this pallet size. The choice depends on your shift volume and available floor space. We confirm that your existing forklift fork width and curing rack slot spacing accept the 850×450×20 mm pallet before the line is finalized.
Q: How does vibration force affect block strength with my local aggregate?
A: The 35.5 kN exciting power is calibrated for standard crushed stone and sand. If your aggregate contains high clay or fine dust, the mix absorbs vibration differently, which can leave weak zones in the block. We test your submitted sample and adjust vibration duration to ensure uniform density without changing the motor rating.
Q: What floor area does a complete semi-automatic line require?
A: The Qt4-24 press itself occupies roughly 2060×1730 mm, but you also need space for the JQ350 mixer, raw material stockpile, pallet return path, and curing racks. A typical layout for this class of Semi-Automatic Block Machine production line fits within a modest workshop bay, though exact dimensions depend on your pallet count and curing time requirements.
Q: How should I plan the curing area around the pallet size?
A: Each 850×450 mm pallet holds a set number of blocks depending on the mould cavity. Multiply that by your target daily pallet count to find total curing rack positions needed. Allow enough aisle width for your forklift to maneuver, and factor in the curing duration your block strength specification demands before pallets can cycle back to the press.



